Cells in at one end, tested packs off the other — one takt across both segments +86 15327155363 [email protected]
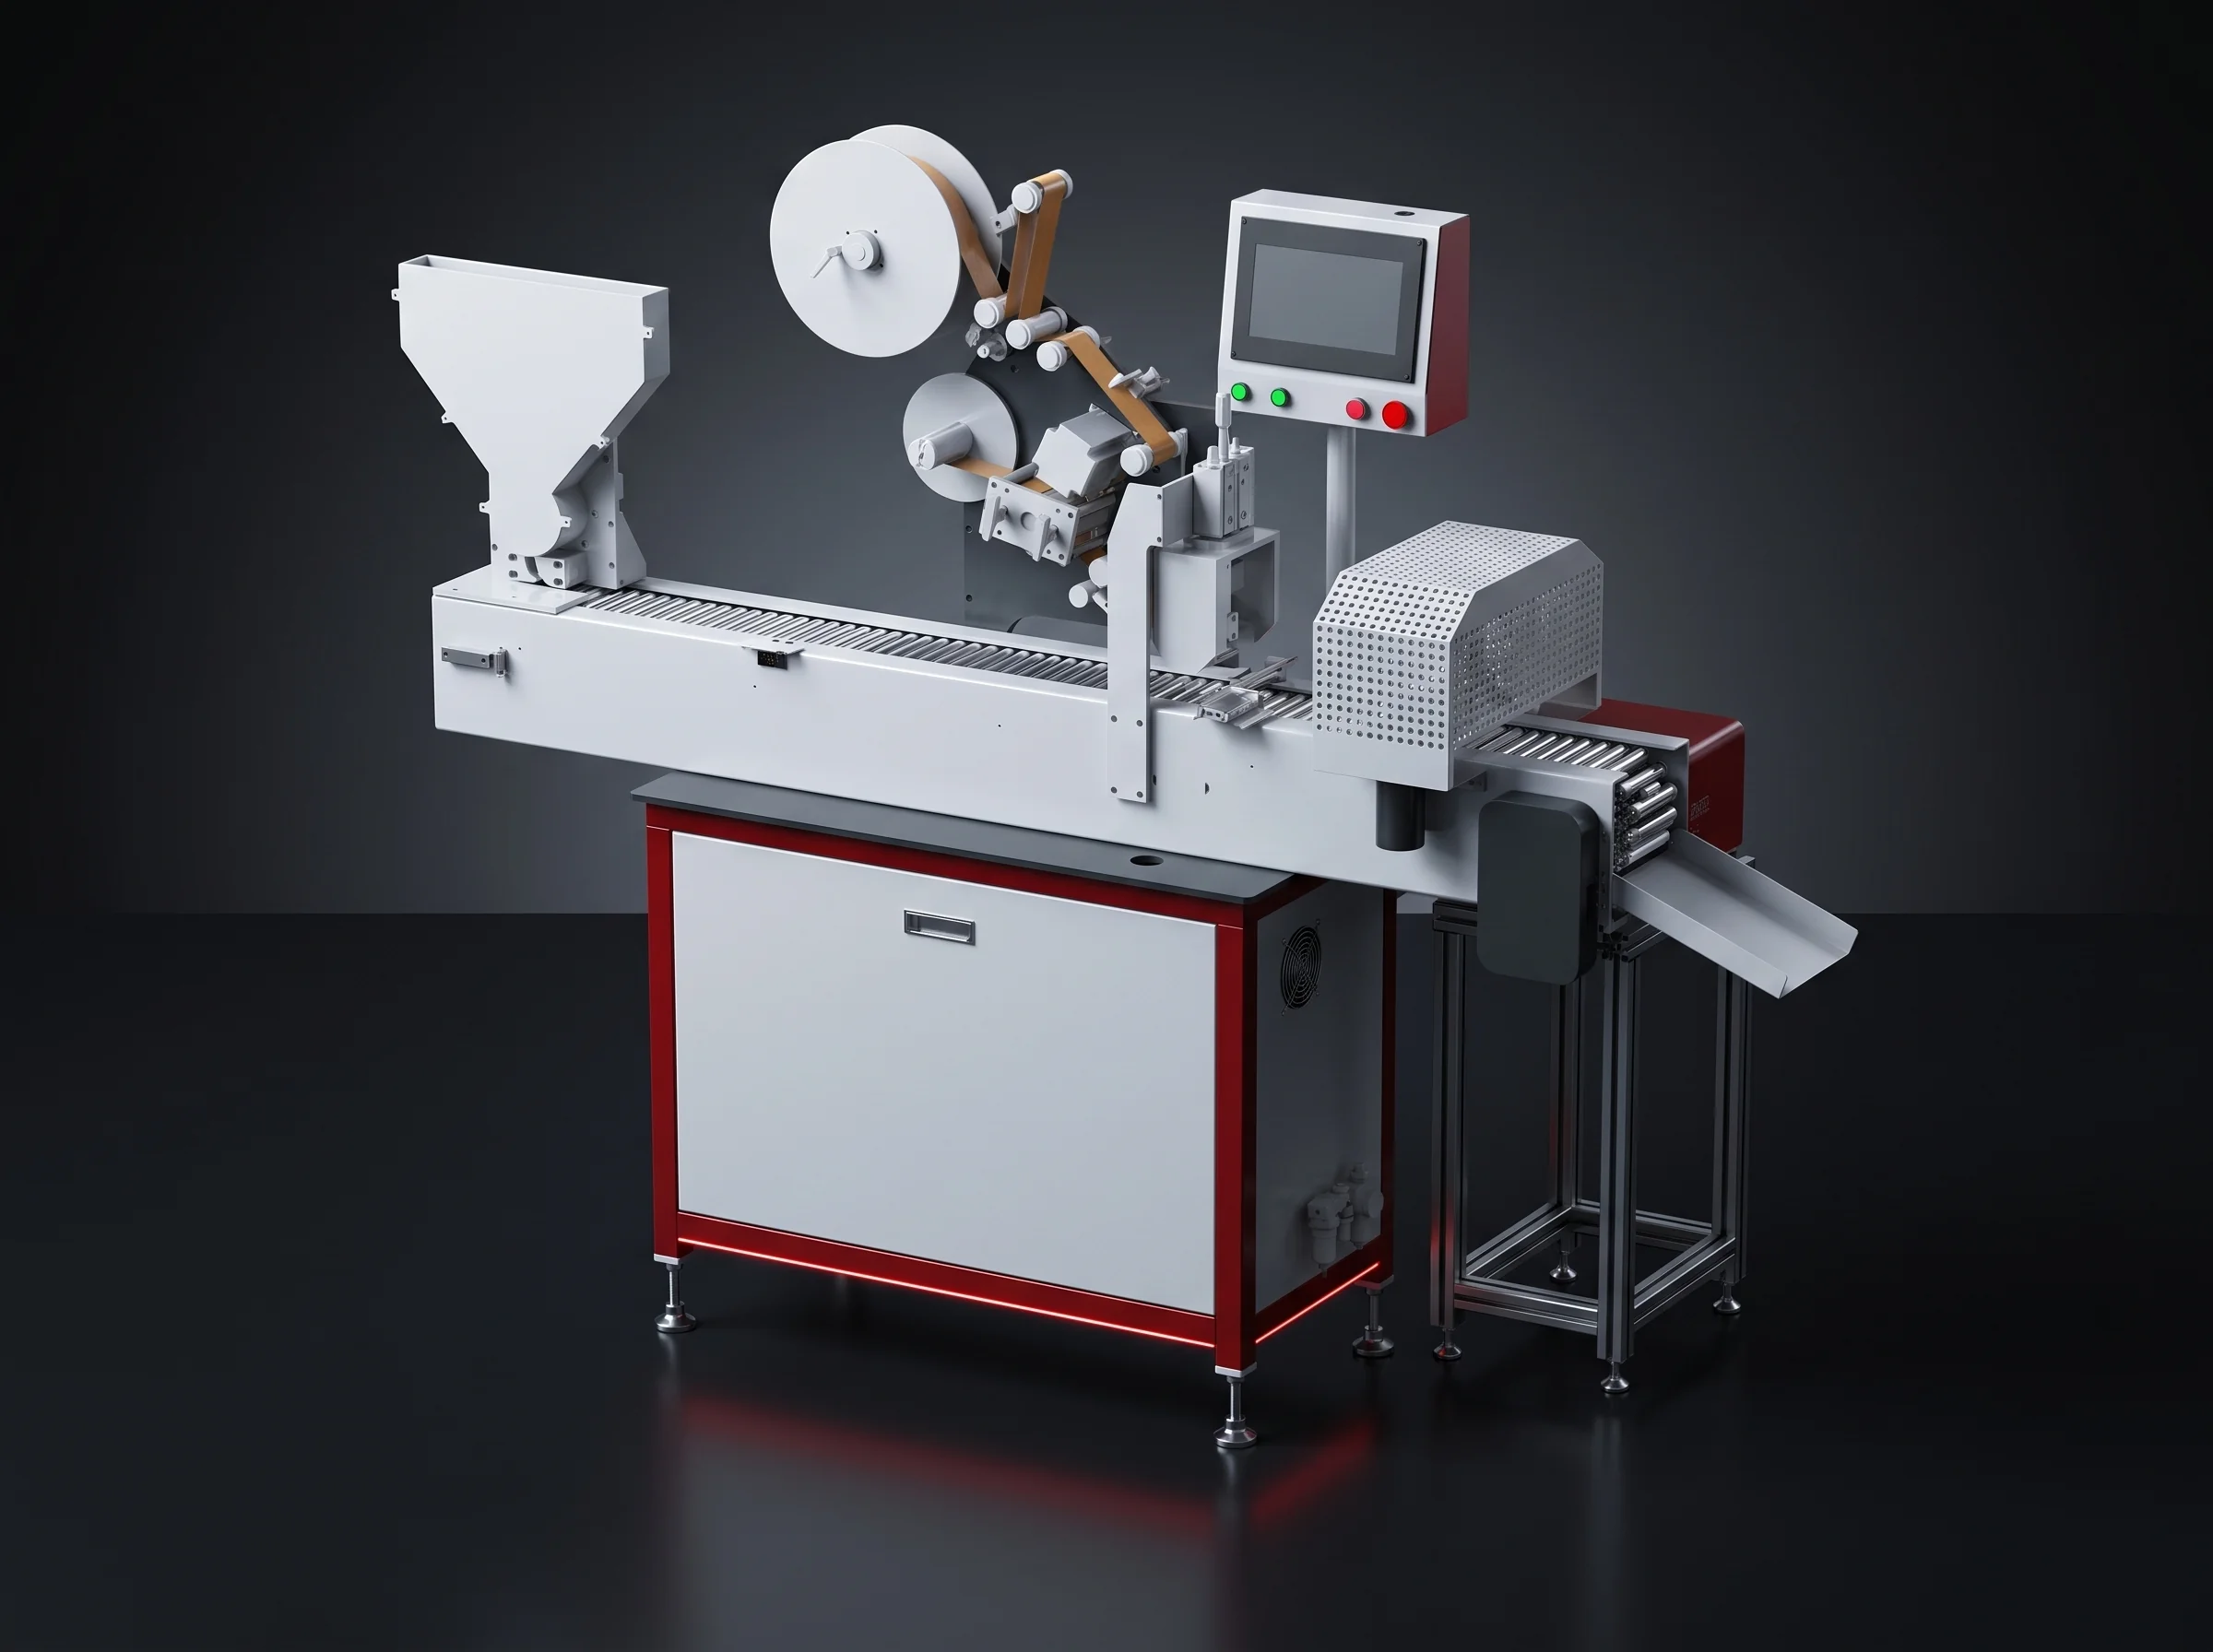
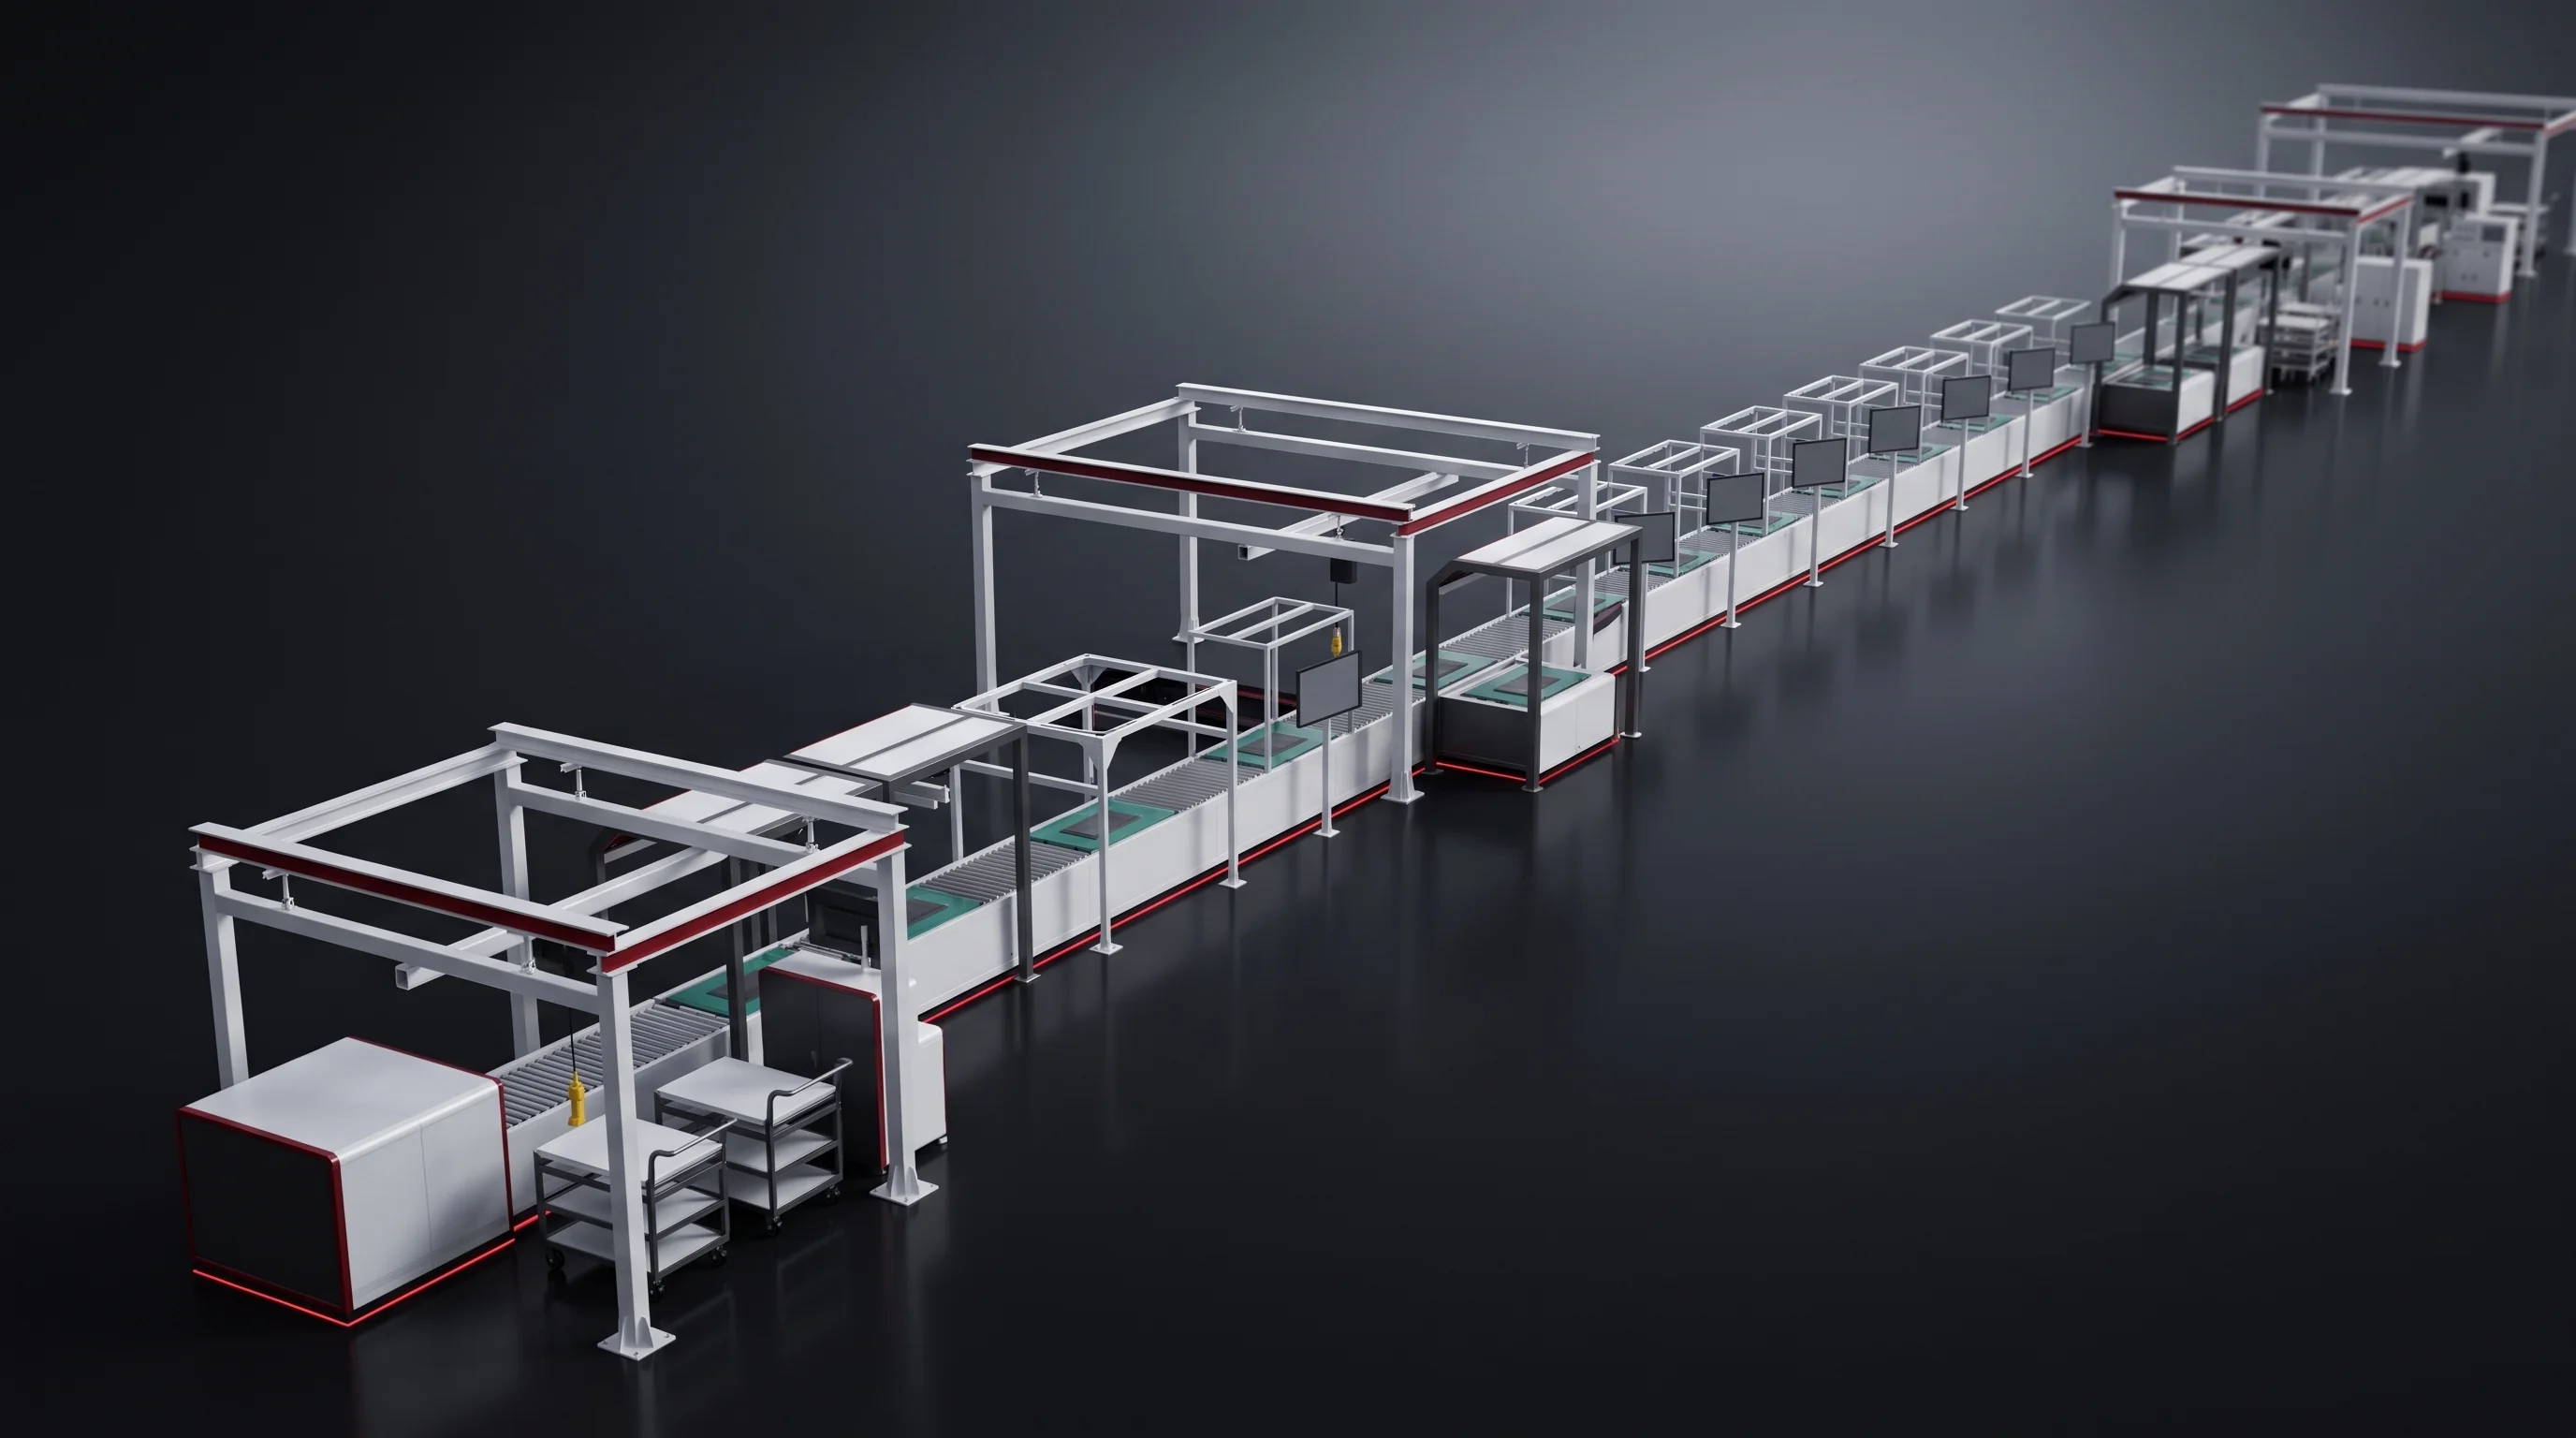
High-automation battery manufacturing equipment line seen along its full station sequence

Equipment catalogue

Battery Manufacturing Equipment, Station By Station

Nine workstations we design and build for prismatic module and pack lines, and nine more for the cylindrical branch. Each is shown at the position it occupies in the 17-station module or 15-station pack sequence, with the figures that decide the fit.

Module segment17 stations
  • 01BLP-UL
  • 02BLP-CS
  • 03
  • 04
  • 05
  • 06
  • 07
  • 08BLP-SP
  • 09
  • 10
  • 11BLP-AD
  • 12
  • 13BLP-W6
  • 14
  • 15
  • 16BLP-EOL
  • 17
Pack segment15 stations
  • 01
  • 02
  • 03BLP-GL
  • 04
  • 05
  • 06
  • 07
  • 08
  • 09
  • 10
  • 11
  • 12
  • 13
  • 14BLP-EOL
  • 15
BLP-CV Between stations, and into the pack segment BLP-WG Off the takt, beside the line Two of the nine sit outside the sequence.
  • BLP-UL Module 01
  • BLP-CS Module 02–03
  • BLP-SP Module 08–09
  • BLP-AD Module 11
  • BLP-W6 Module 13
  • BLP-EOL Module 16 & Pack 14
  • BLP-GL Pack 03
  • BLP-CV Between stations
  • BLP-WG Off the takt

Red positions are our own designs. The rest are handling, cleaning, taping, fastening and inspection stations supplied with the line.

Supply boundary

Battery Manufacturing Equipment Supply Boundary

The line begins where a finished cell arrives on a pallet and ends where a tested pack leaves the floor. Everything between is ours.
Cell in, tested pack outStated before the enquiry, not after the quotation.

Inside the scope

  • Unloading cells from trays, stacking the empty trays
  • Grading every cell to a window you sign
  • Stacking, servo pressing and steel banding, 300 to 1100 mm
  • Terminal addressing, polarity reading, laser cleaning
  • Inline busbar welding and off-line gantry welding
  • Cooling plate gluing, module insertion, pack assembly
  • End-of-line testing on the module and again on the pack

Outside it

  • Cell manufacturing: coating, winding, electrolyte filling
  • Formation and grading upstream of the pallet
  • Container-level assembly after the pack
  • Cell supply: the cells that run through acceptance are yours
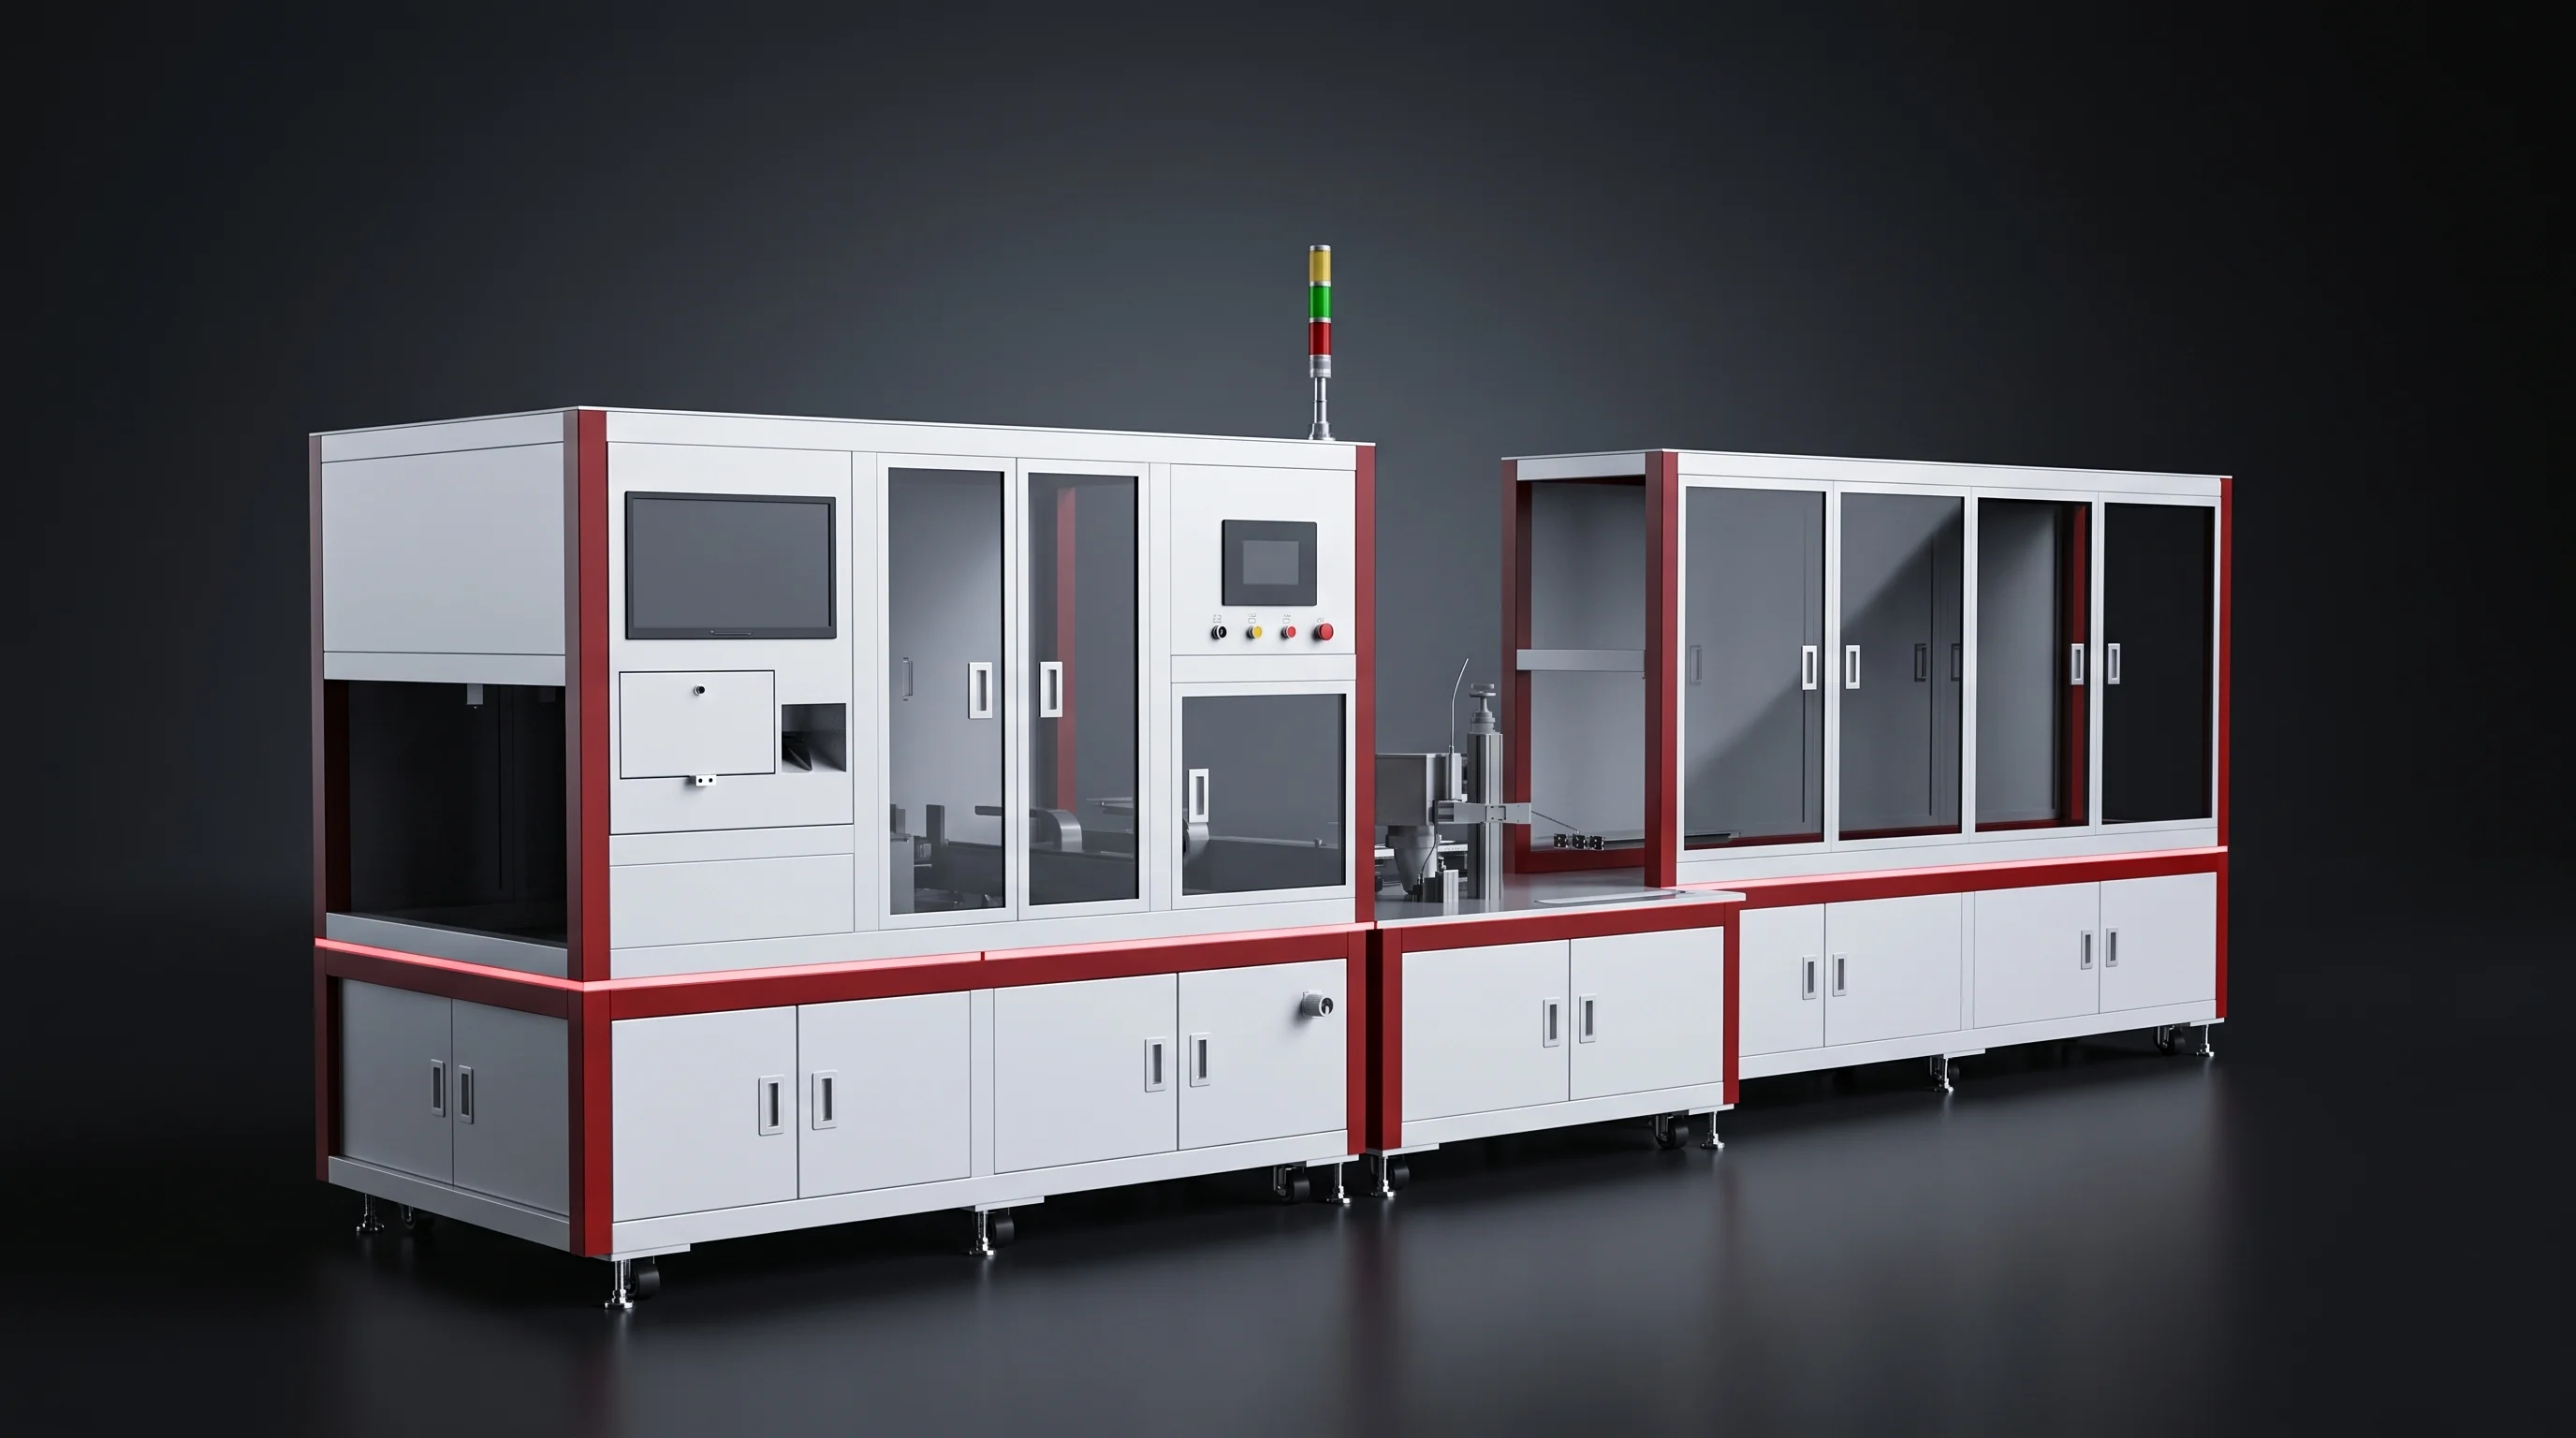
Module and pack battery manufacturing equipment laid out as one continuous line
Both segments run on one takt.
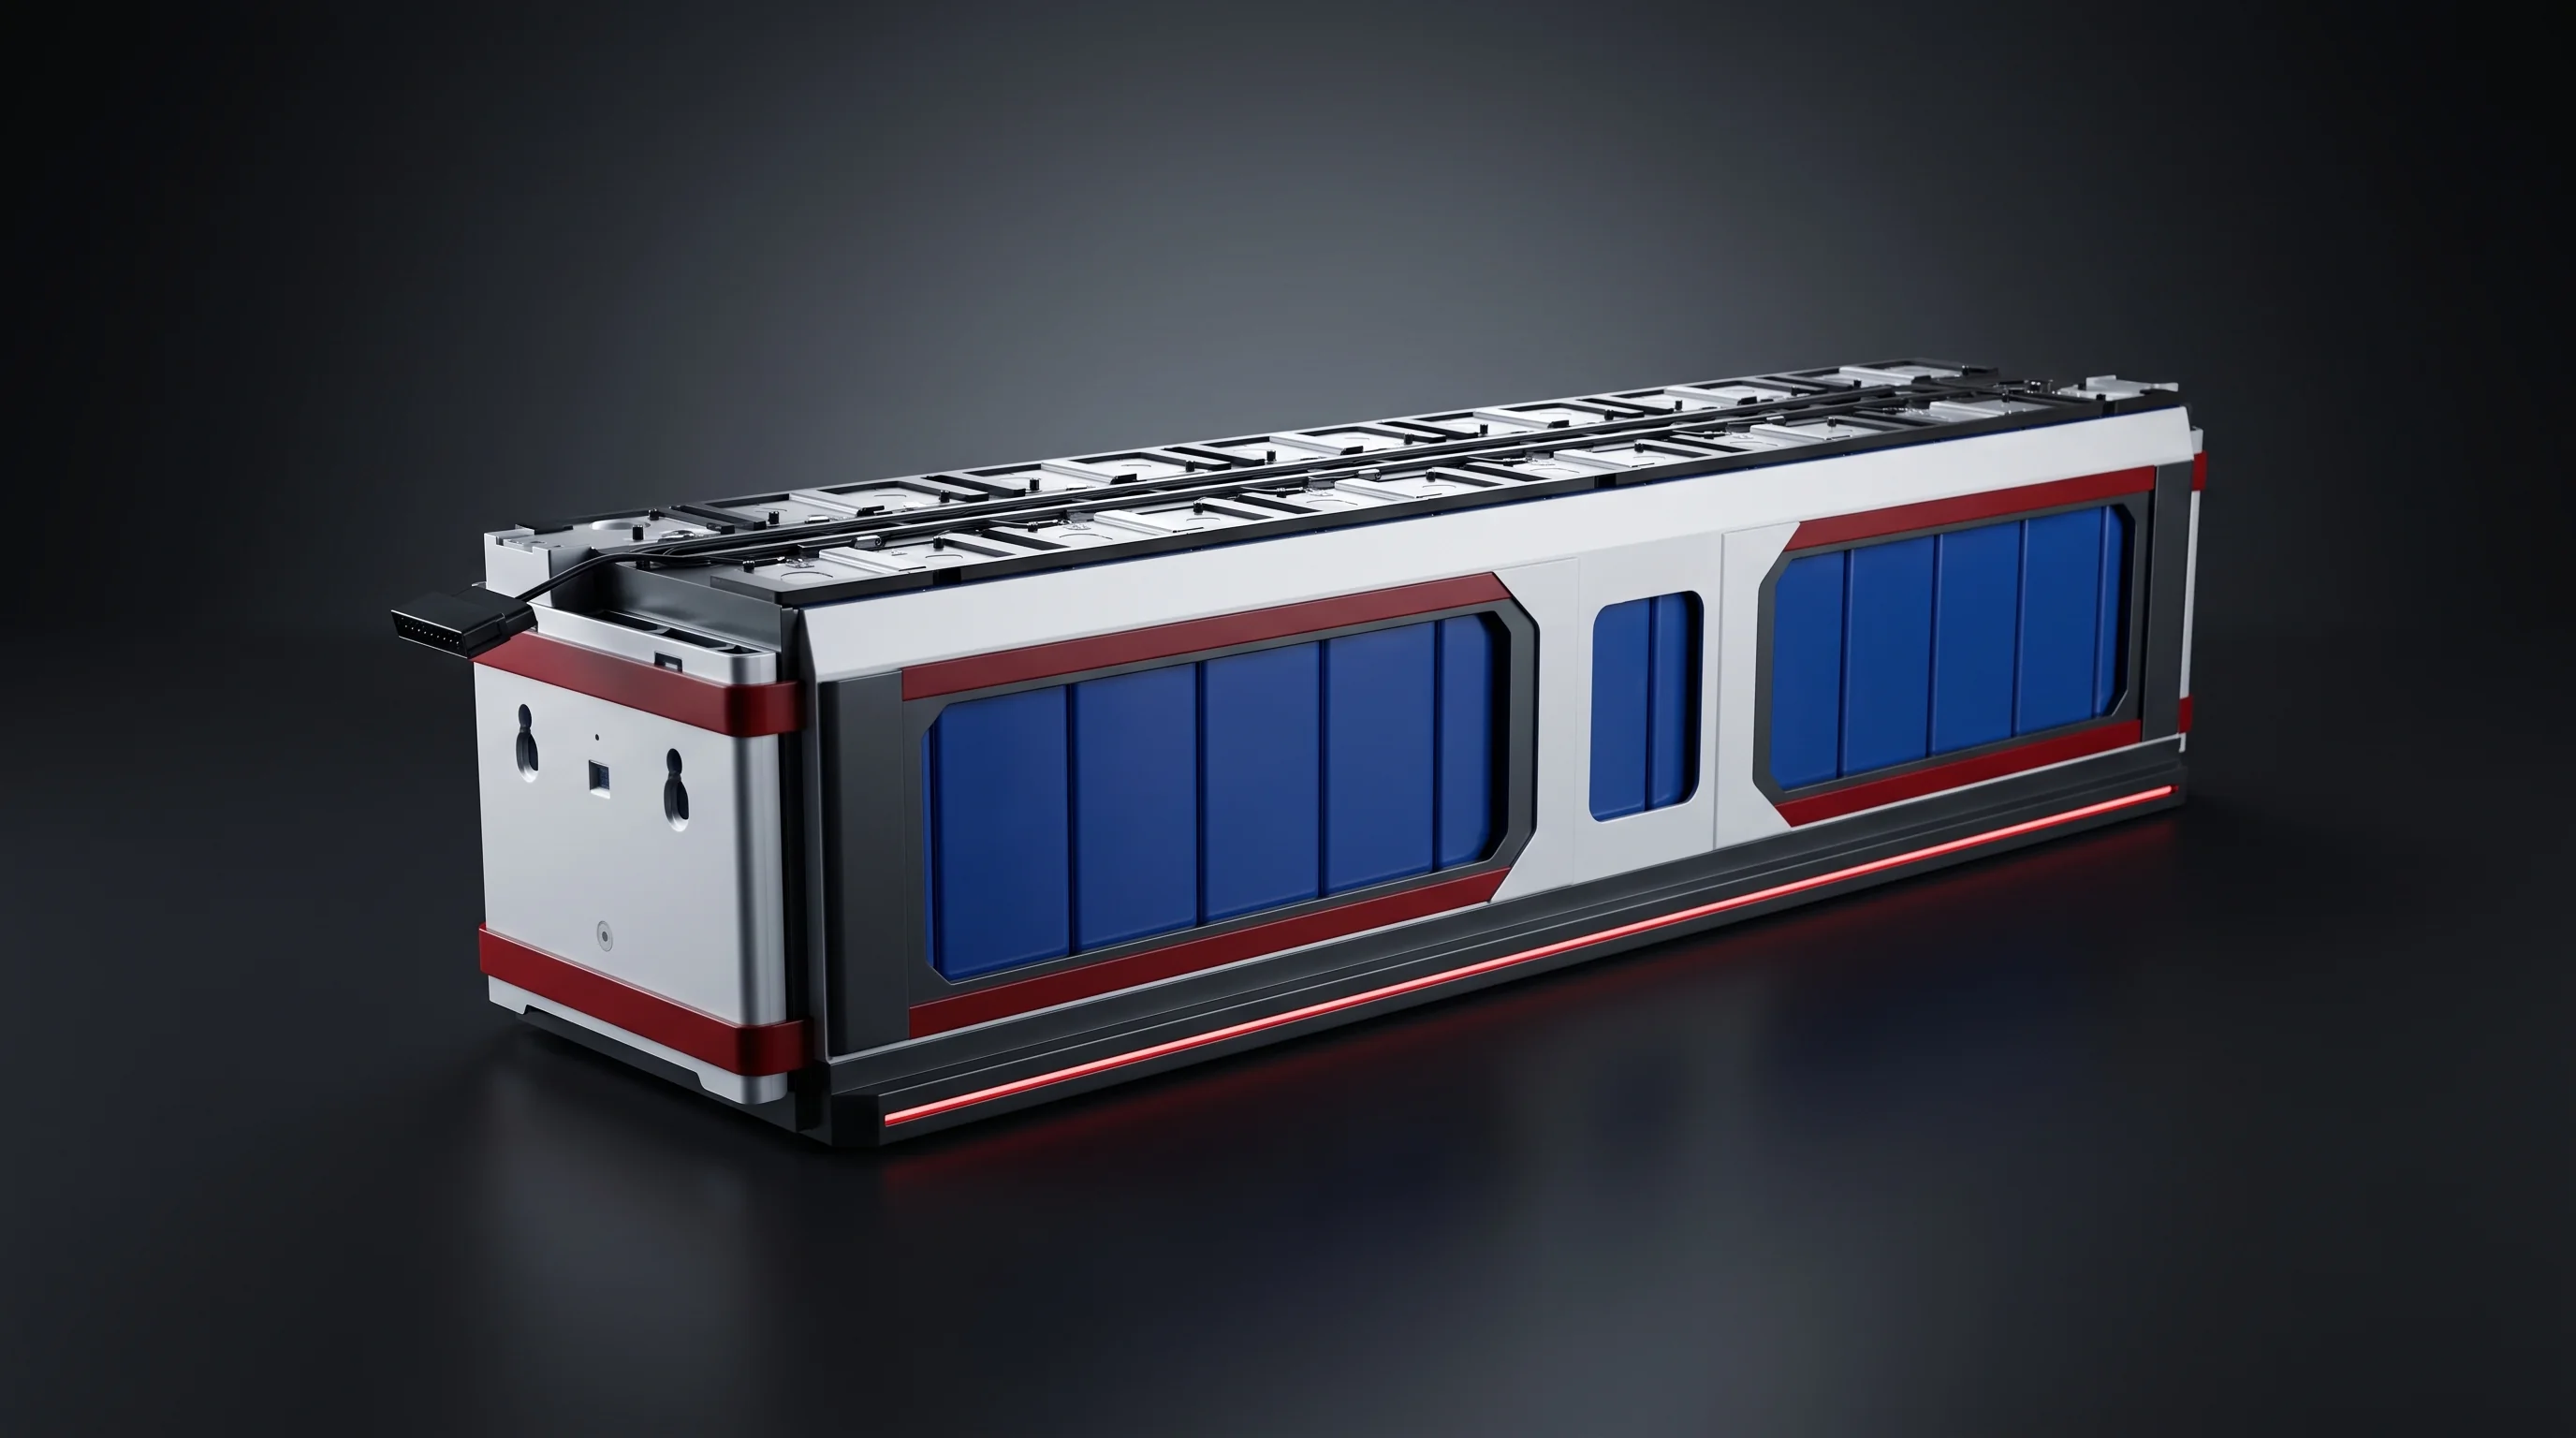
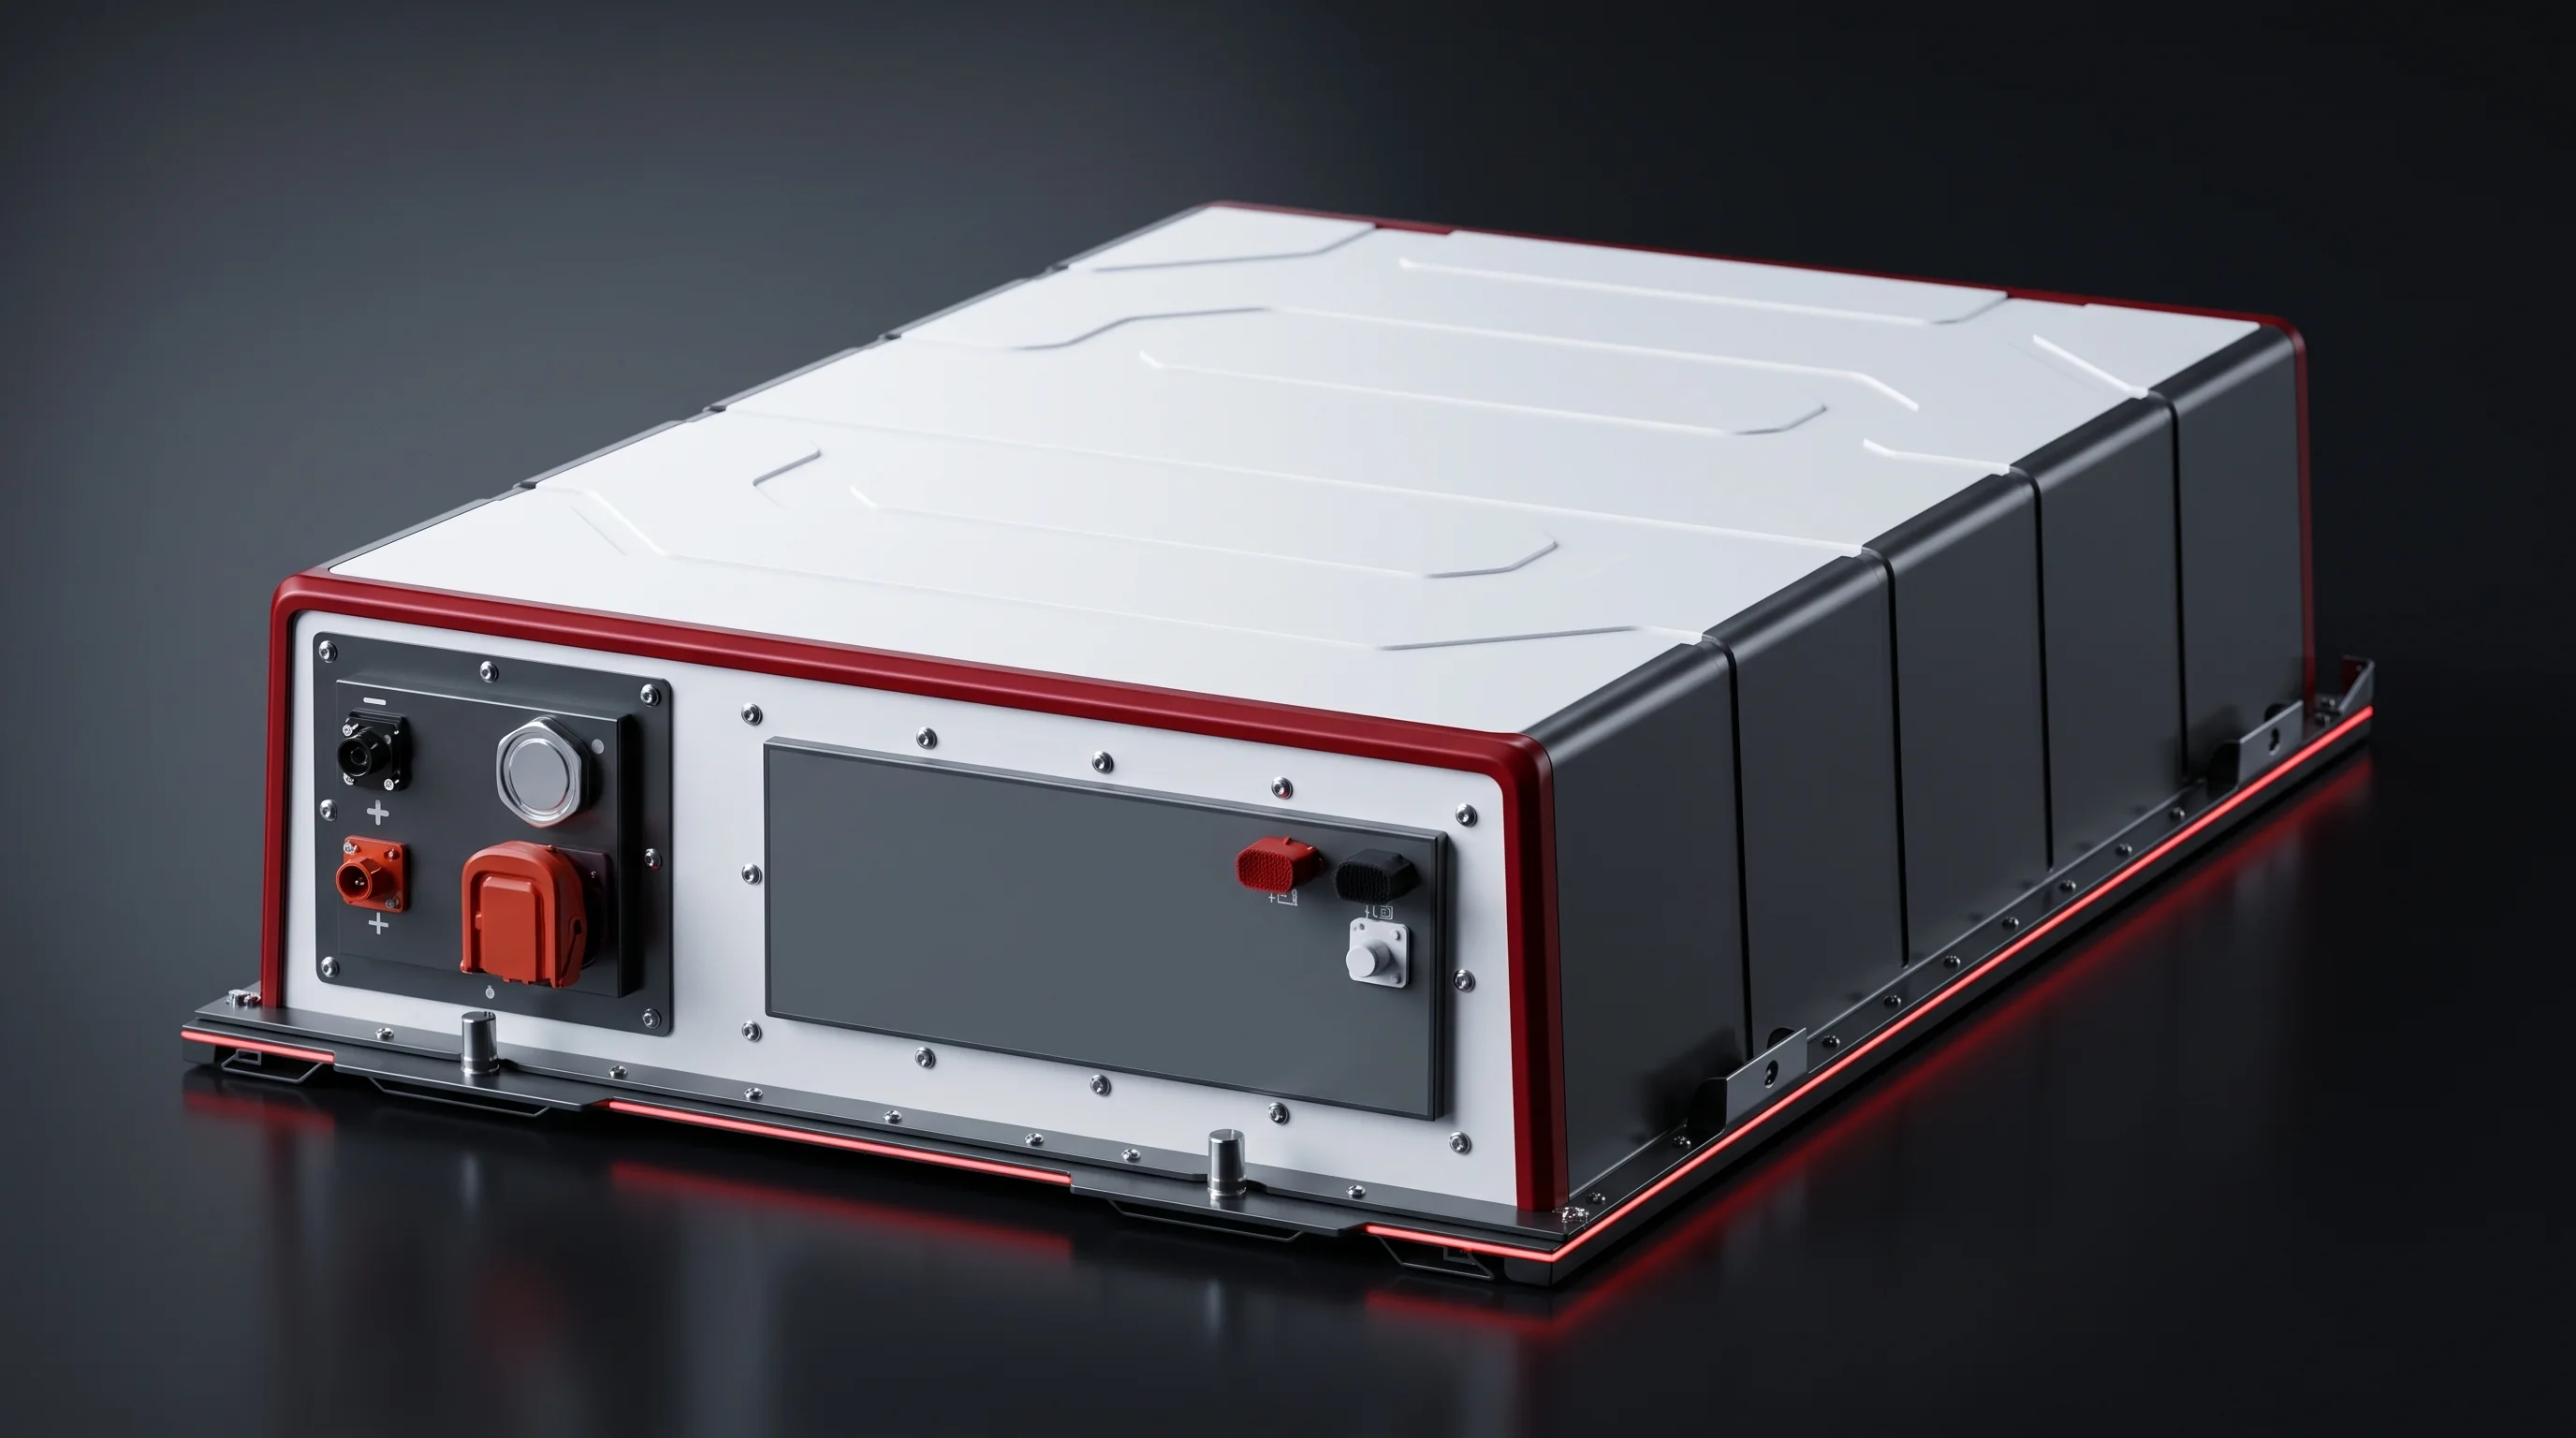
Finished battery pack of the kind that leaves the last station of the pack segment
1P52S blueprint pack: 1152 × 810 × 243 mm, ≤400 kg.

Three scopes

Three Buying Scopes: Line, Segment, Station

Most enquiries arrive as one of three shapes. Which one yours is decides how much layout work and acceptance sits around the machines, not which machines you get.

Complete battery manufacturing equipment line quoted as one project
Scope 01Complete line

A whole line against your building

One project at one of three takt tiers between 4 and 15 PPM, laid out against your bay dimensions, floor loading and utility drops.
Usual reader
First line
Acceptance
Both segments
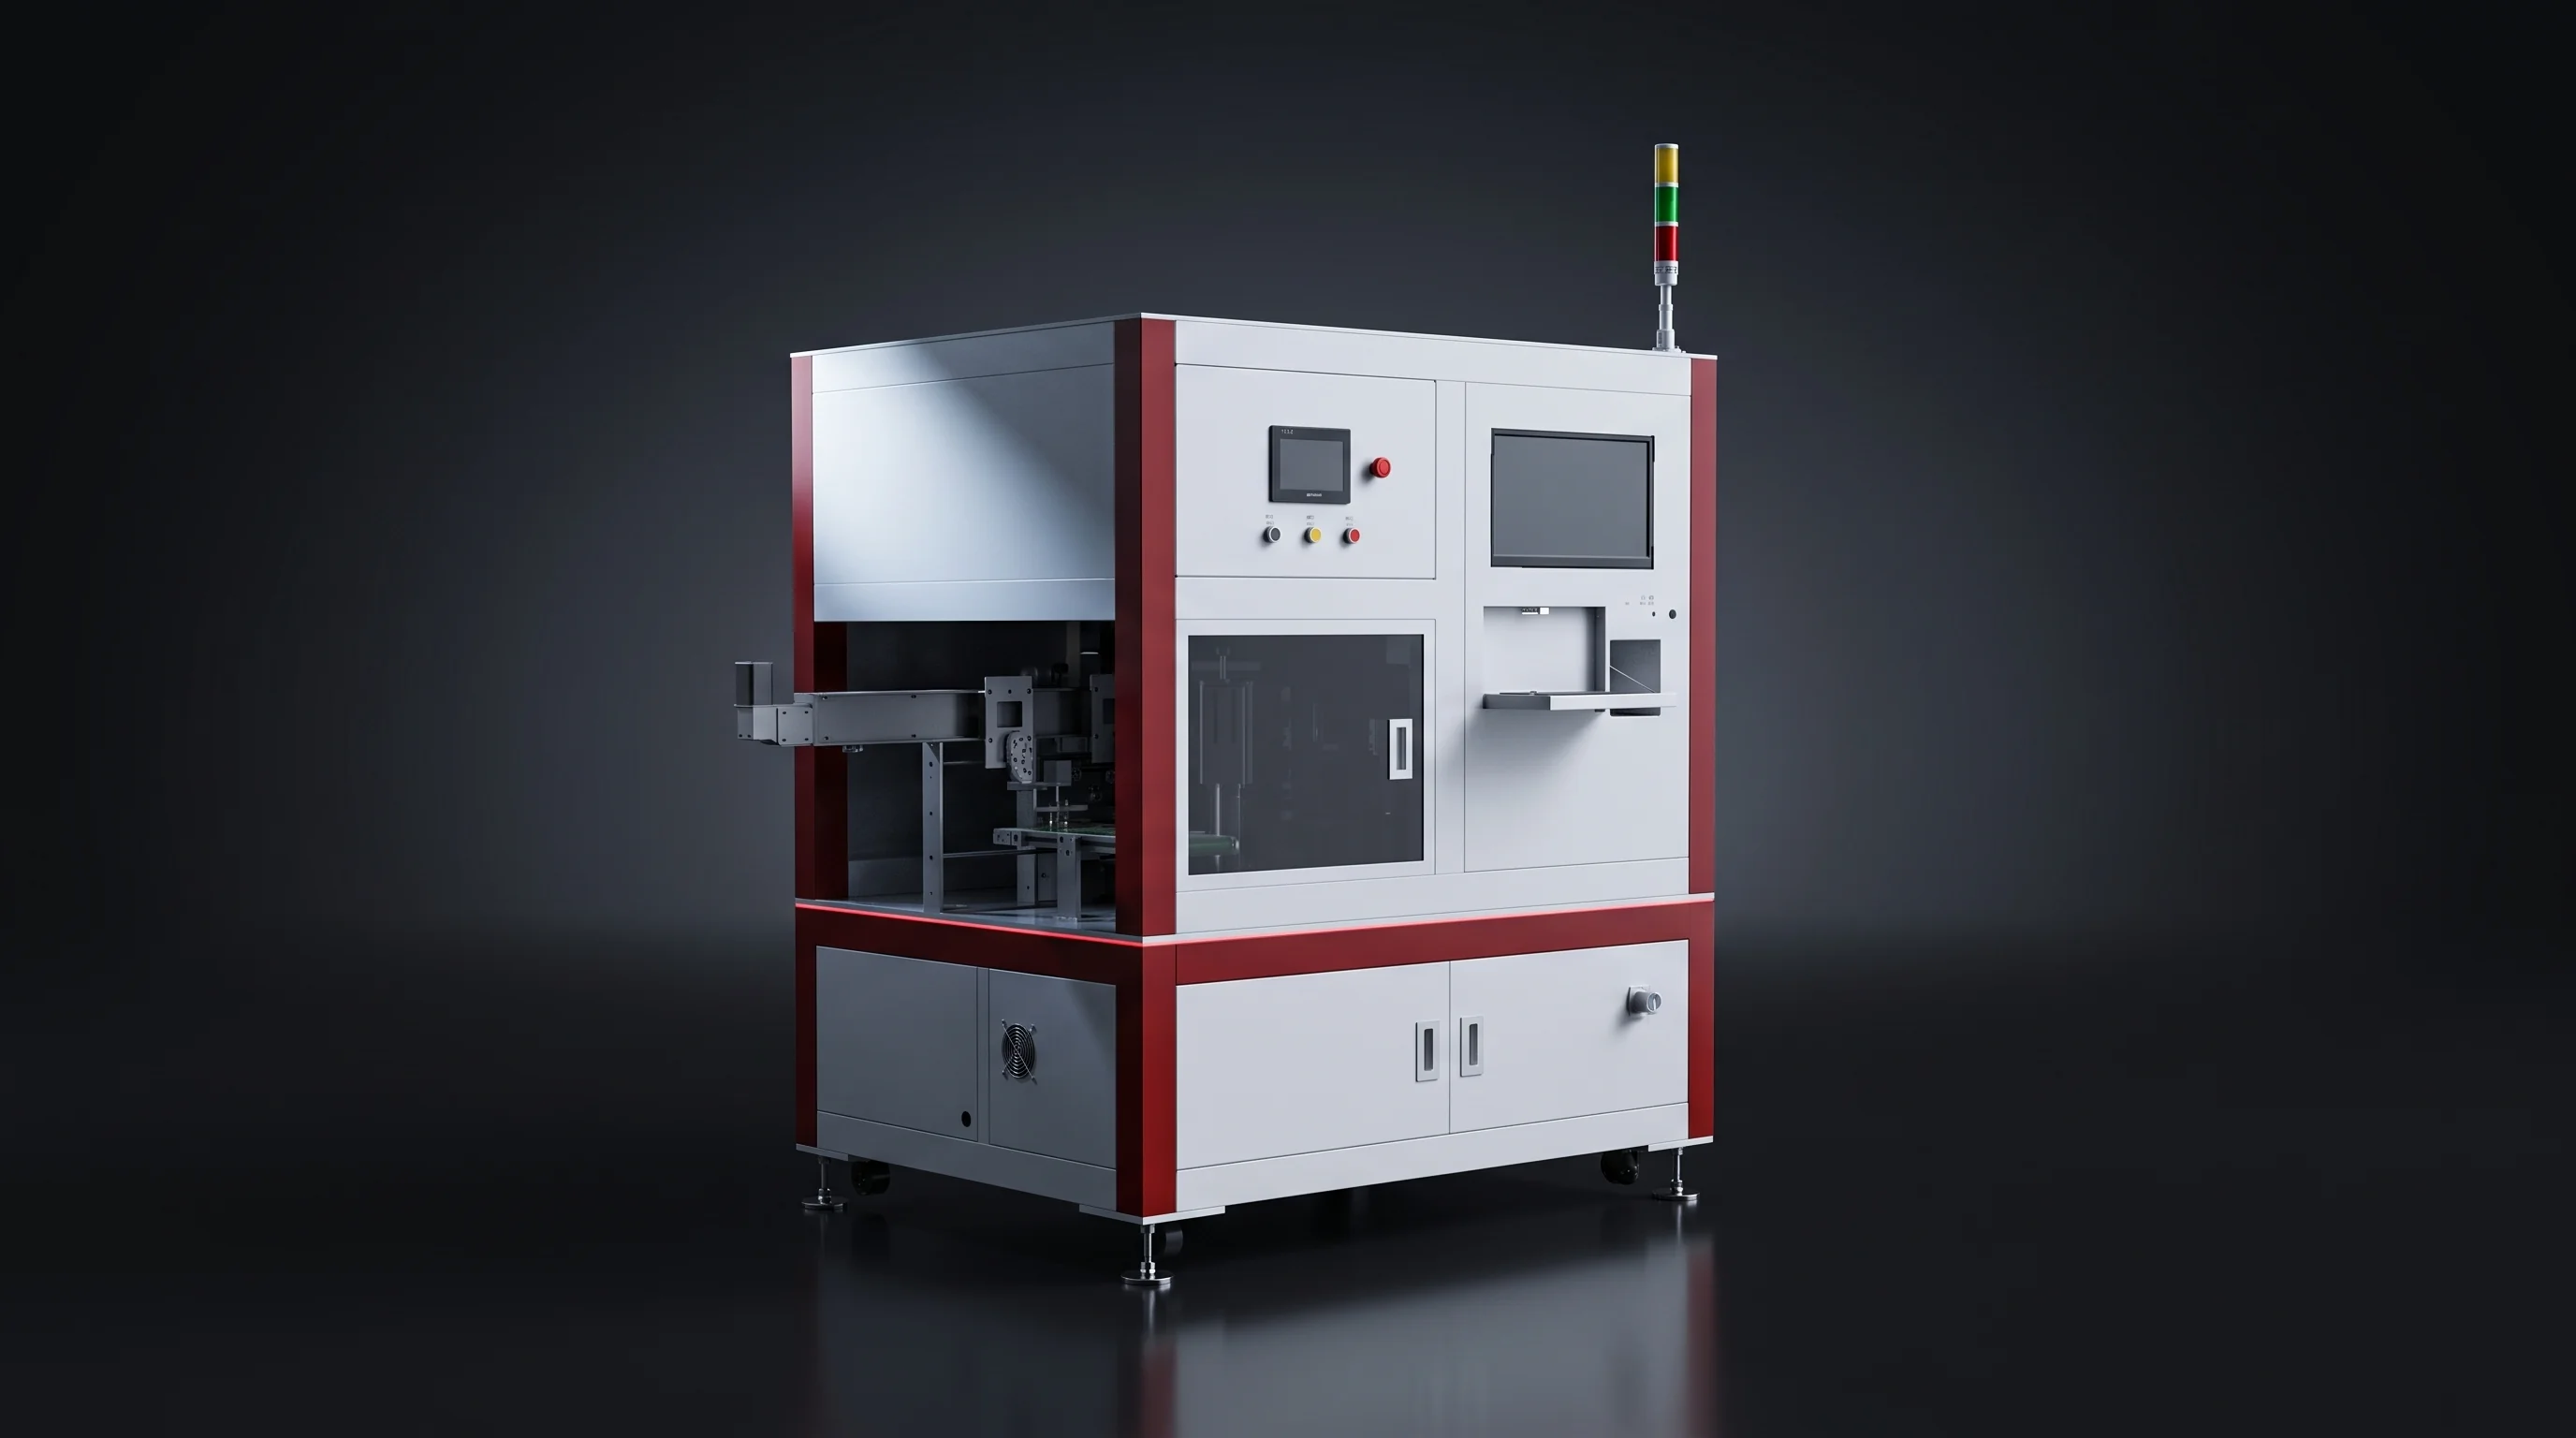
Segment of a battery module line rebuilt as a station sequence
Scope 02One segment

A segment holding the rest back

A station sequence with its own acceptance criteria — usually a module segment that cannot feed a pack segment already sized right.
Usual reader
Plant already running
Acceptance
At the existing takt
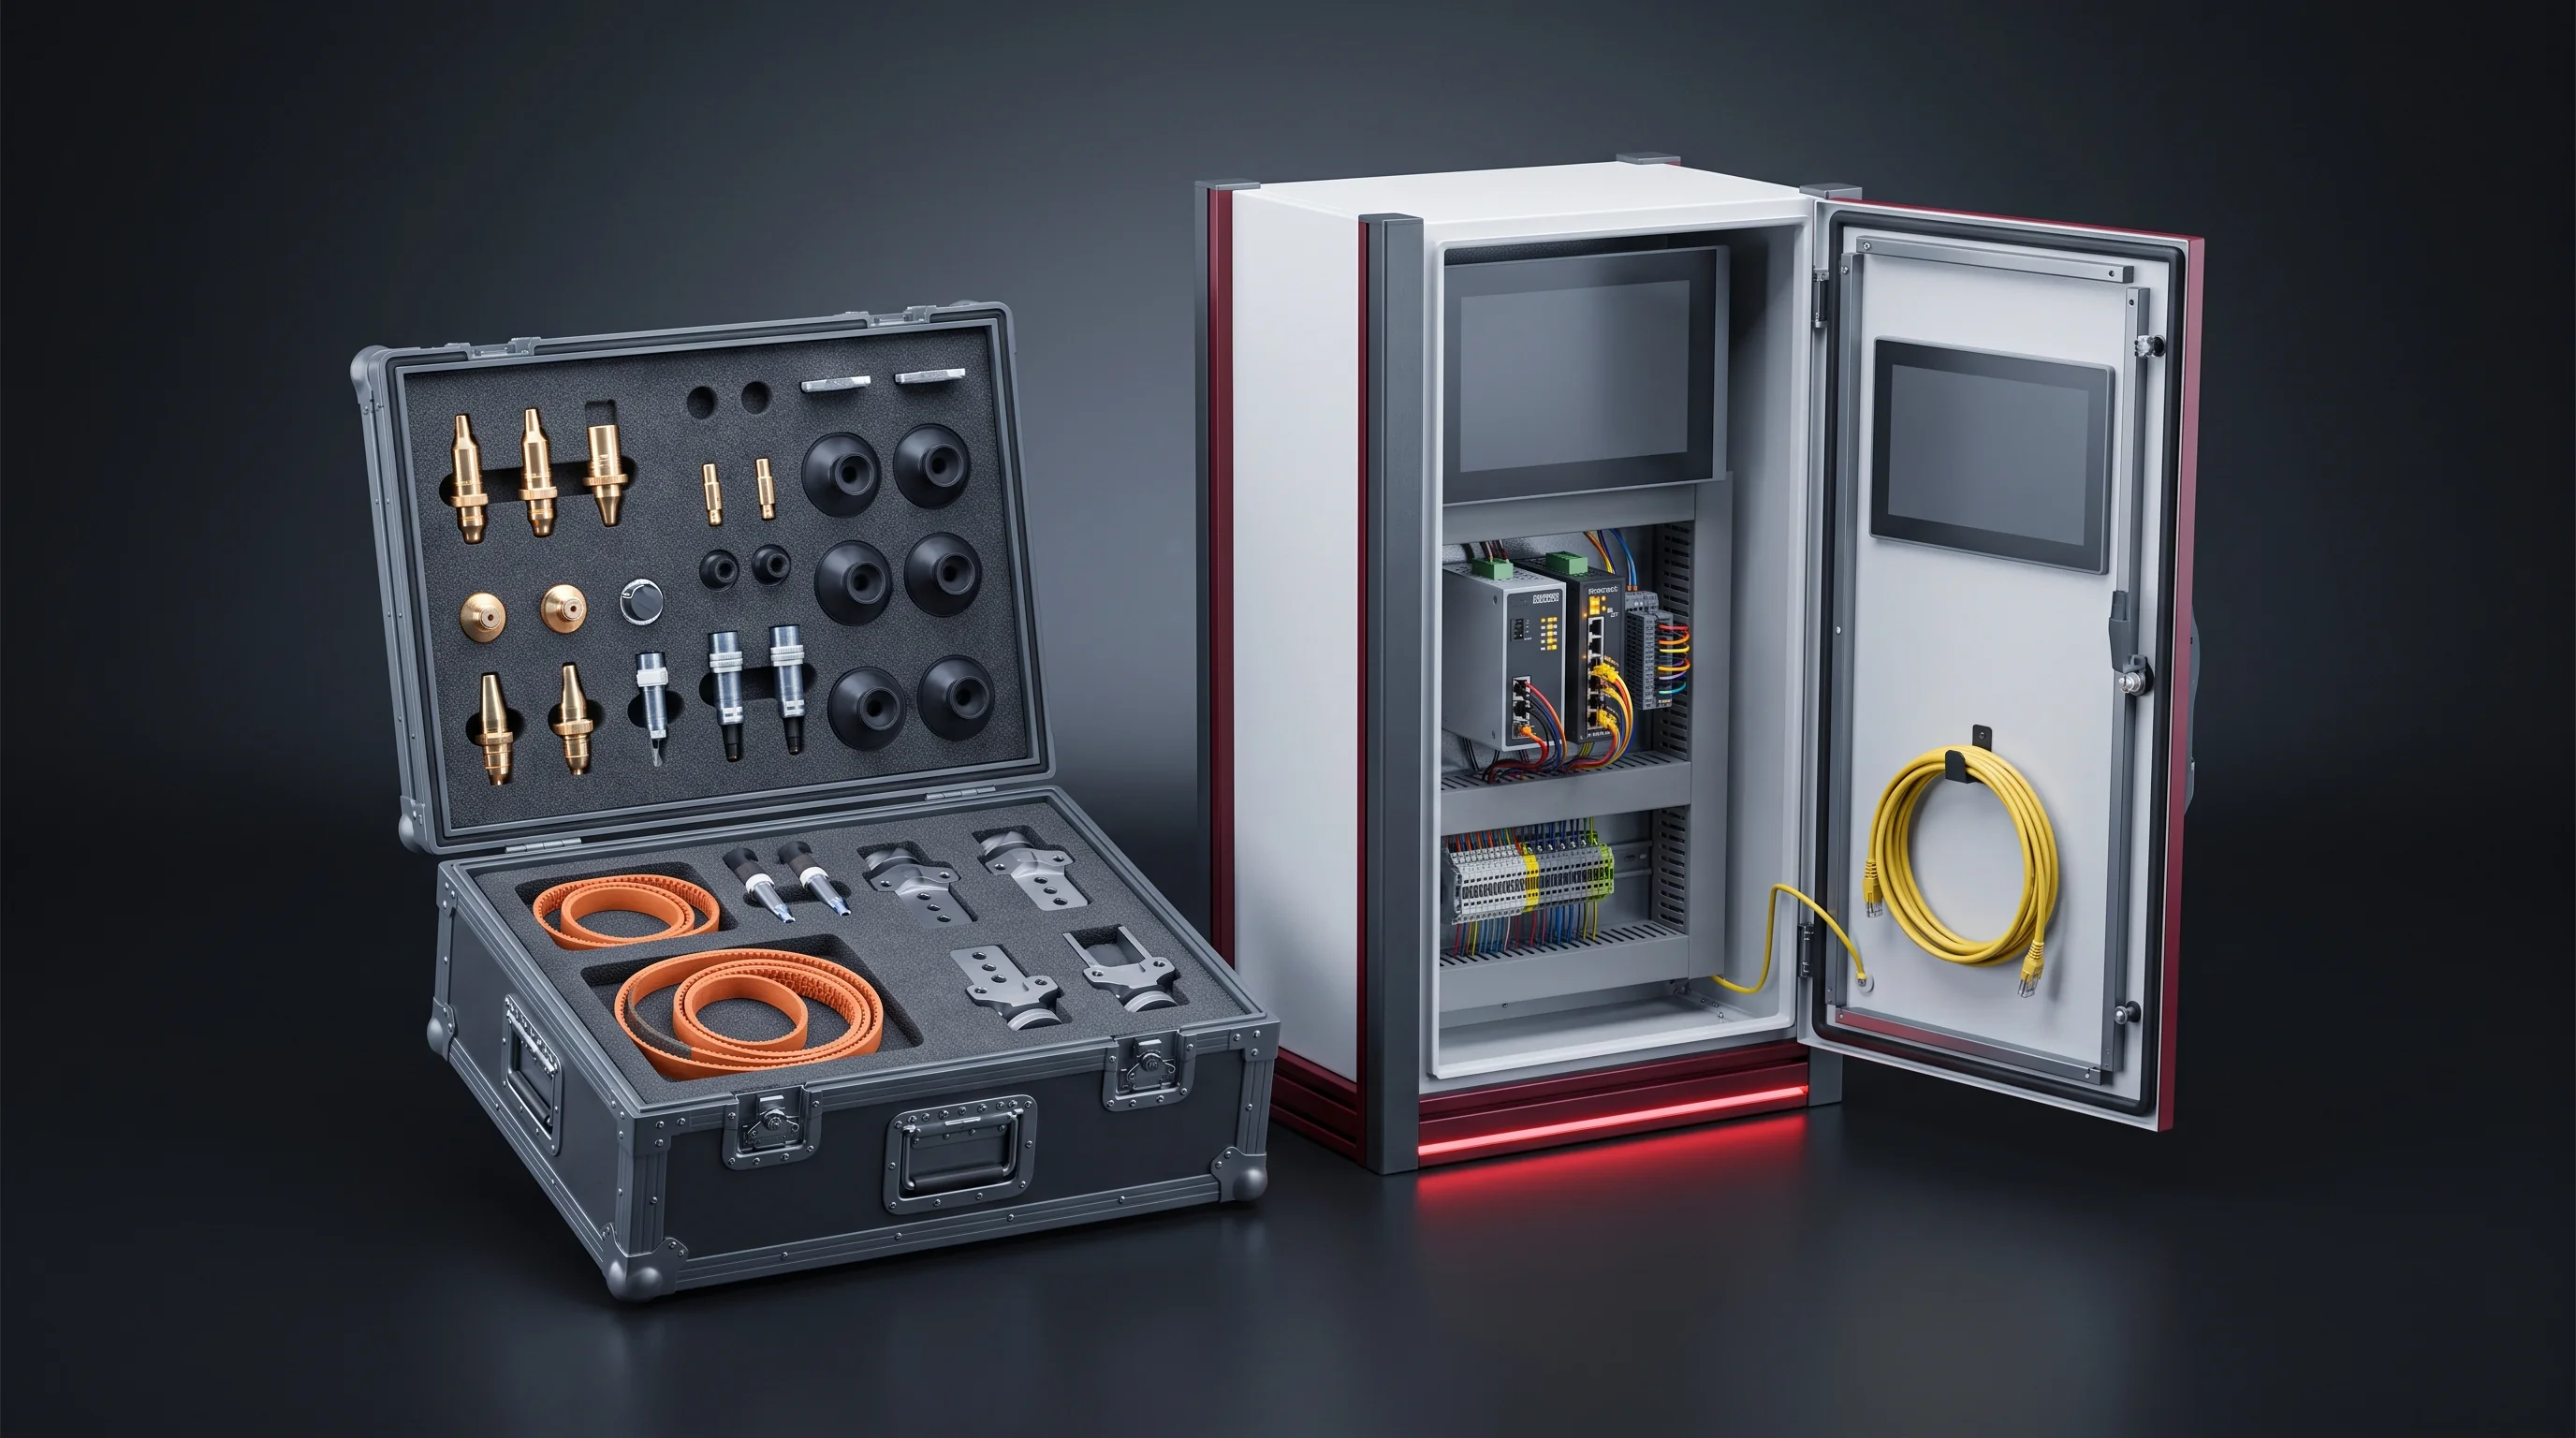
Single battery manufacturing equipment station prepared with its own spares and interface set
Scope 03One station

One machine into your line

Its own interface sheet: transfer height, supply, air and network figures, so it drops into a line somebody else built.

Usual reader
Adding one station
Acceptance
On your conveyor

The machine specifications are identical in all three cases. A press is the same press whether it arrives as station 08 of a new line or as a pallet on your dock. What changes is the layout work in front and the acceptance behind.

Layout against your building Signed acceptance criteria Installation and commissioning Interface sheet per station

The nine

Nine In-House Battery Manufacturing Equipment Stations

Nine workstations on the module and pack lines are our own designs, not bought-in units carrying our label. Each card gives the position, the two figures customers buy against, and the datasheet.
In-house workstations
9
Branch machines
9 more
Module stations
17
Pack stations
15
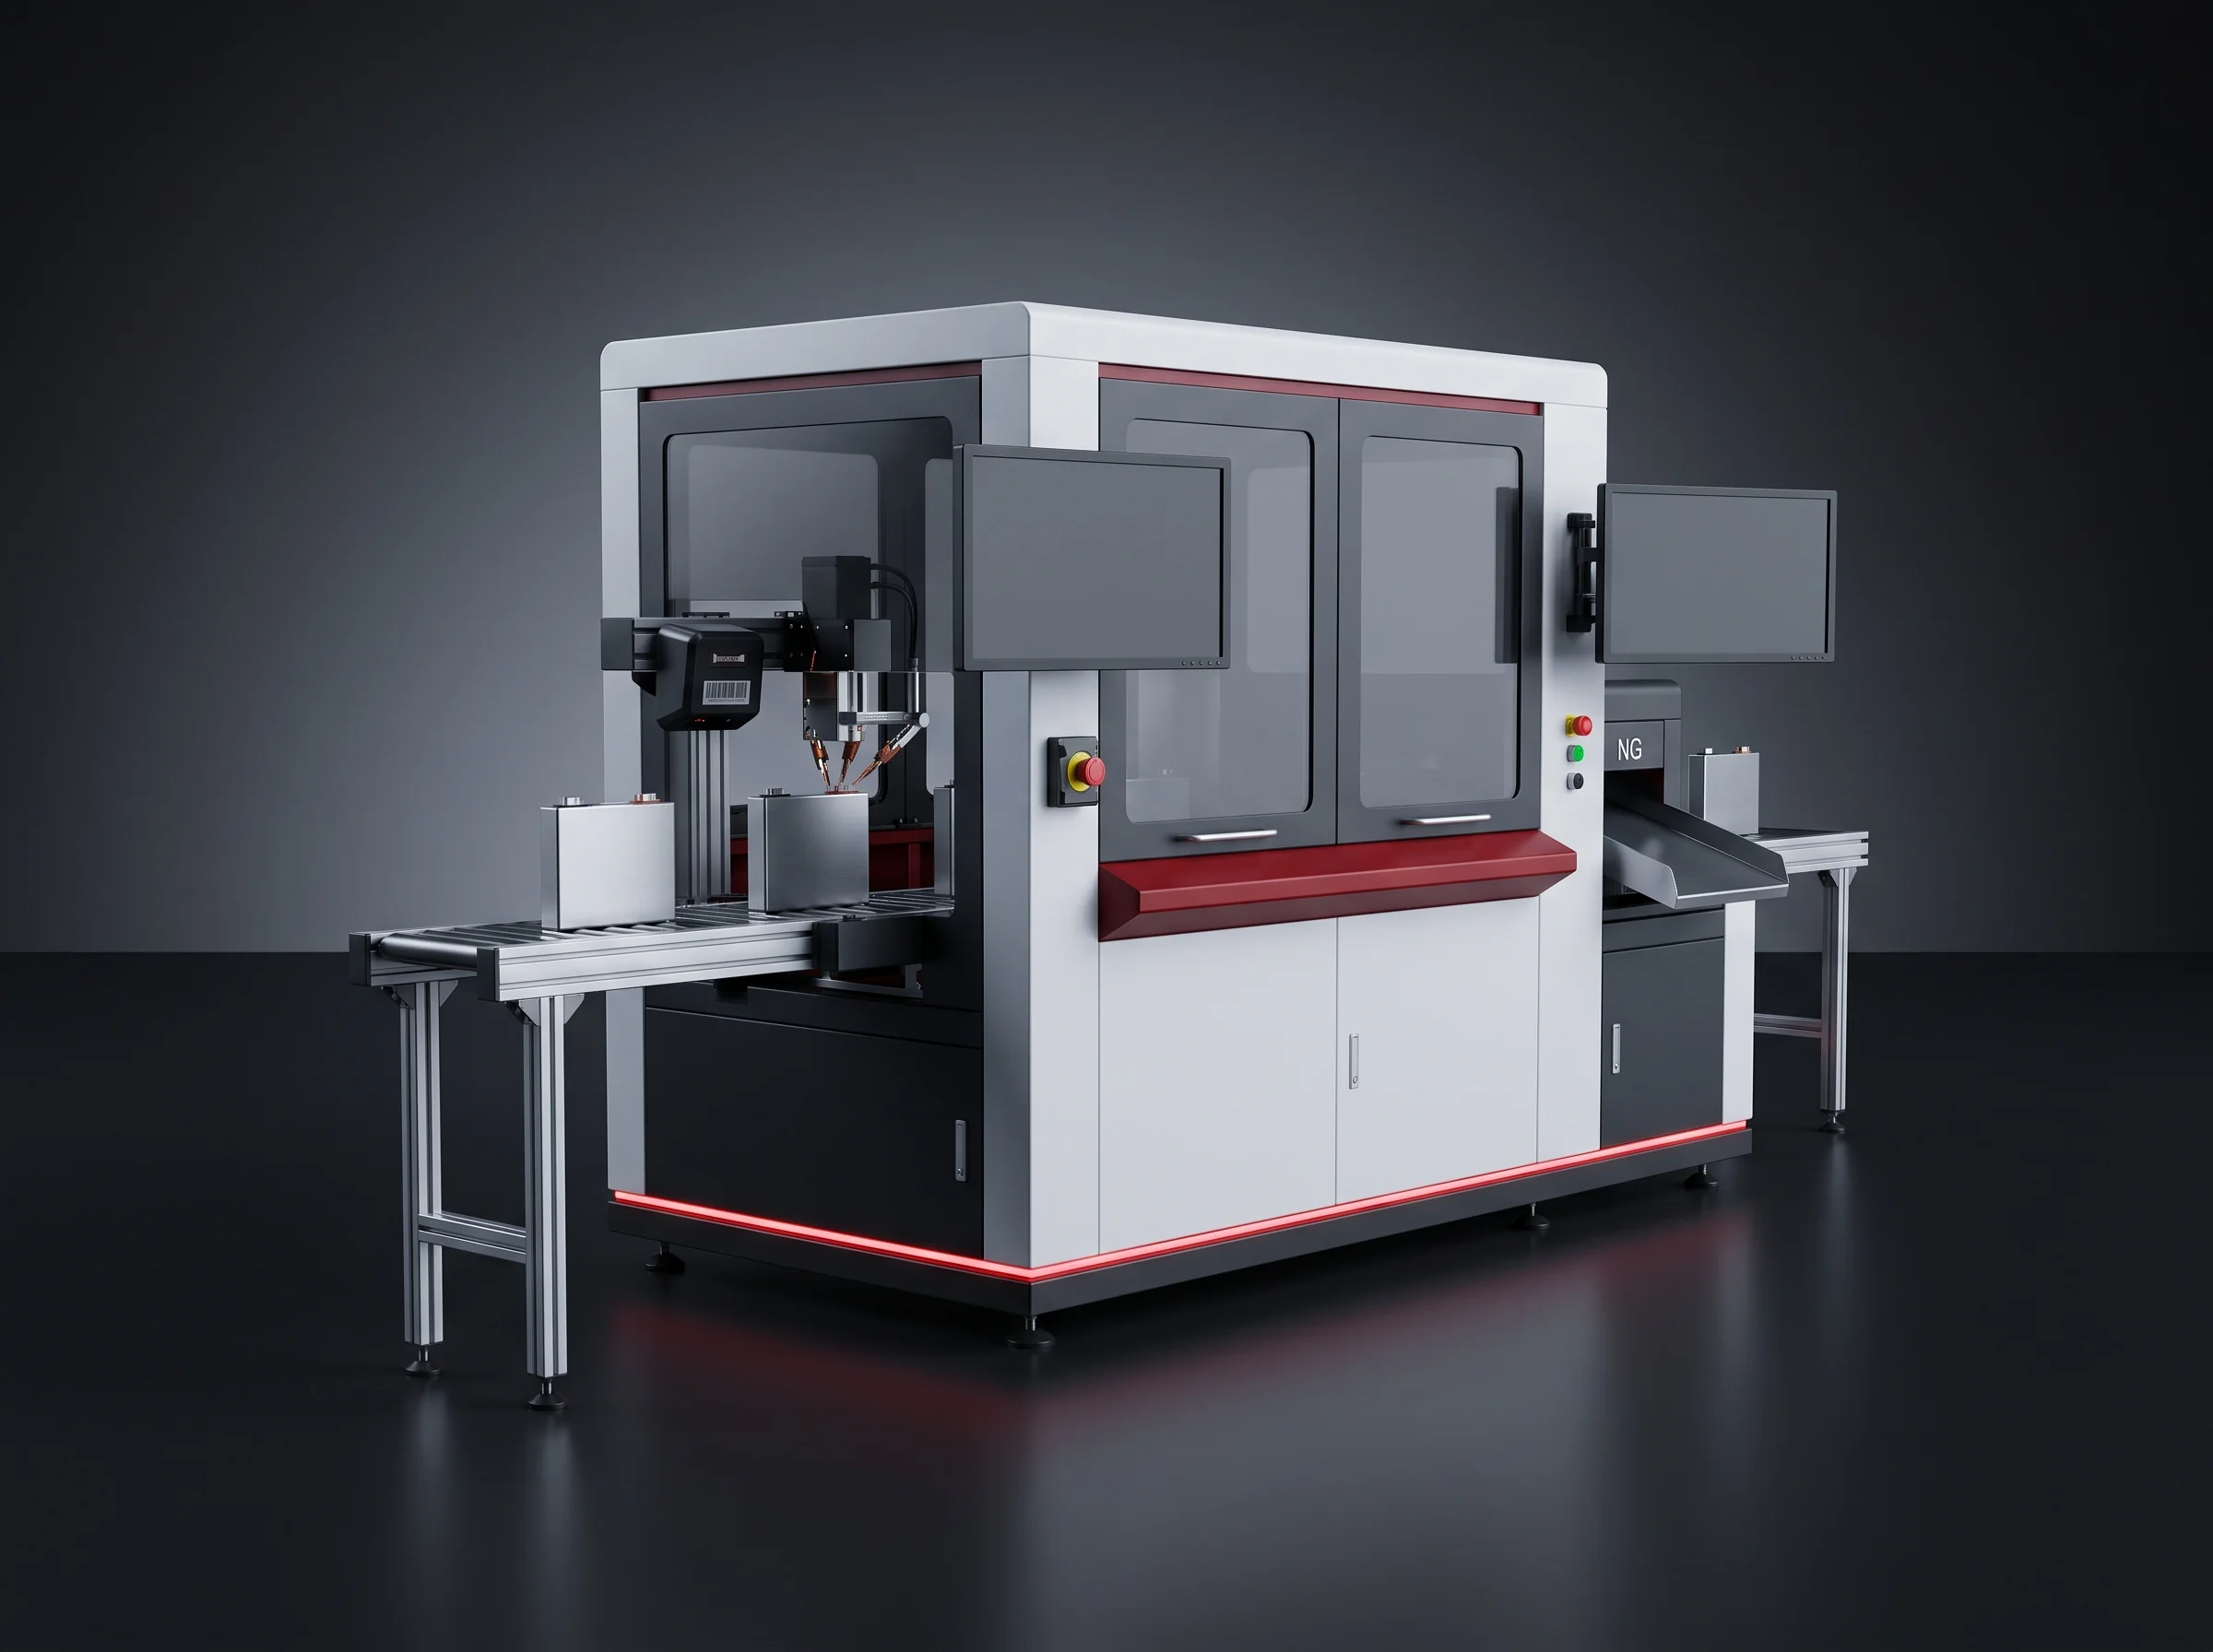
BLP-UL cell unloading robot at the front of the battery module line
BLP-ULModule 01

Cell unloading

A six-axis robot lifts five cells per pick off the tray, checks post orientation and stacks the empty trays.
  • 220 kgRobot payload
  • ±0.06 mmPositioning
Full datasheet
BLP-CS cell testing and sorting station measuring voltage and internal resistance
BLP-CSModule 02–03

Cell testing and sorting

Every cell scanned and sorted into up to ten settable grades. Rejects are ejected and the gap refilled from a buffer.
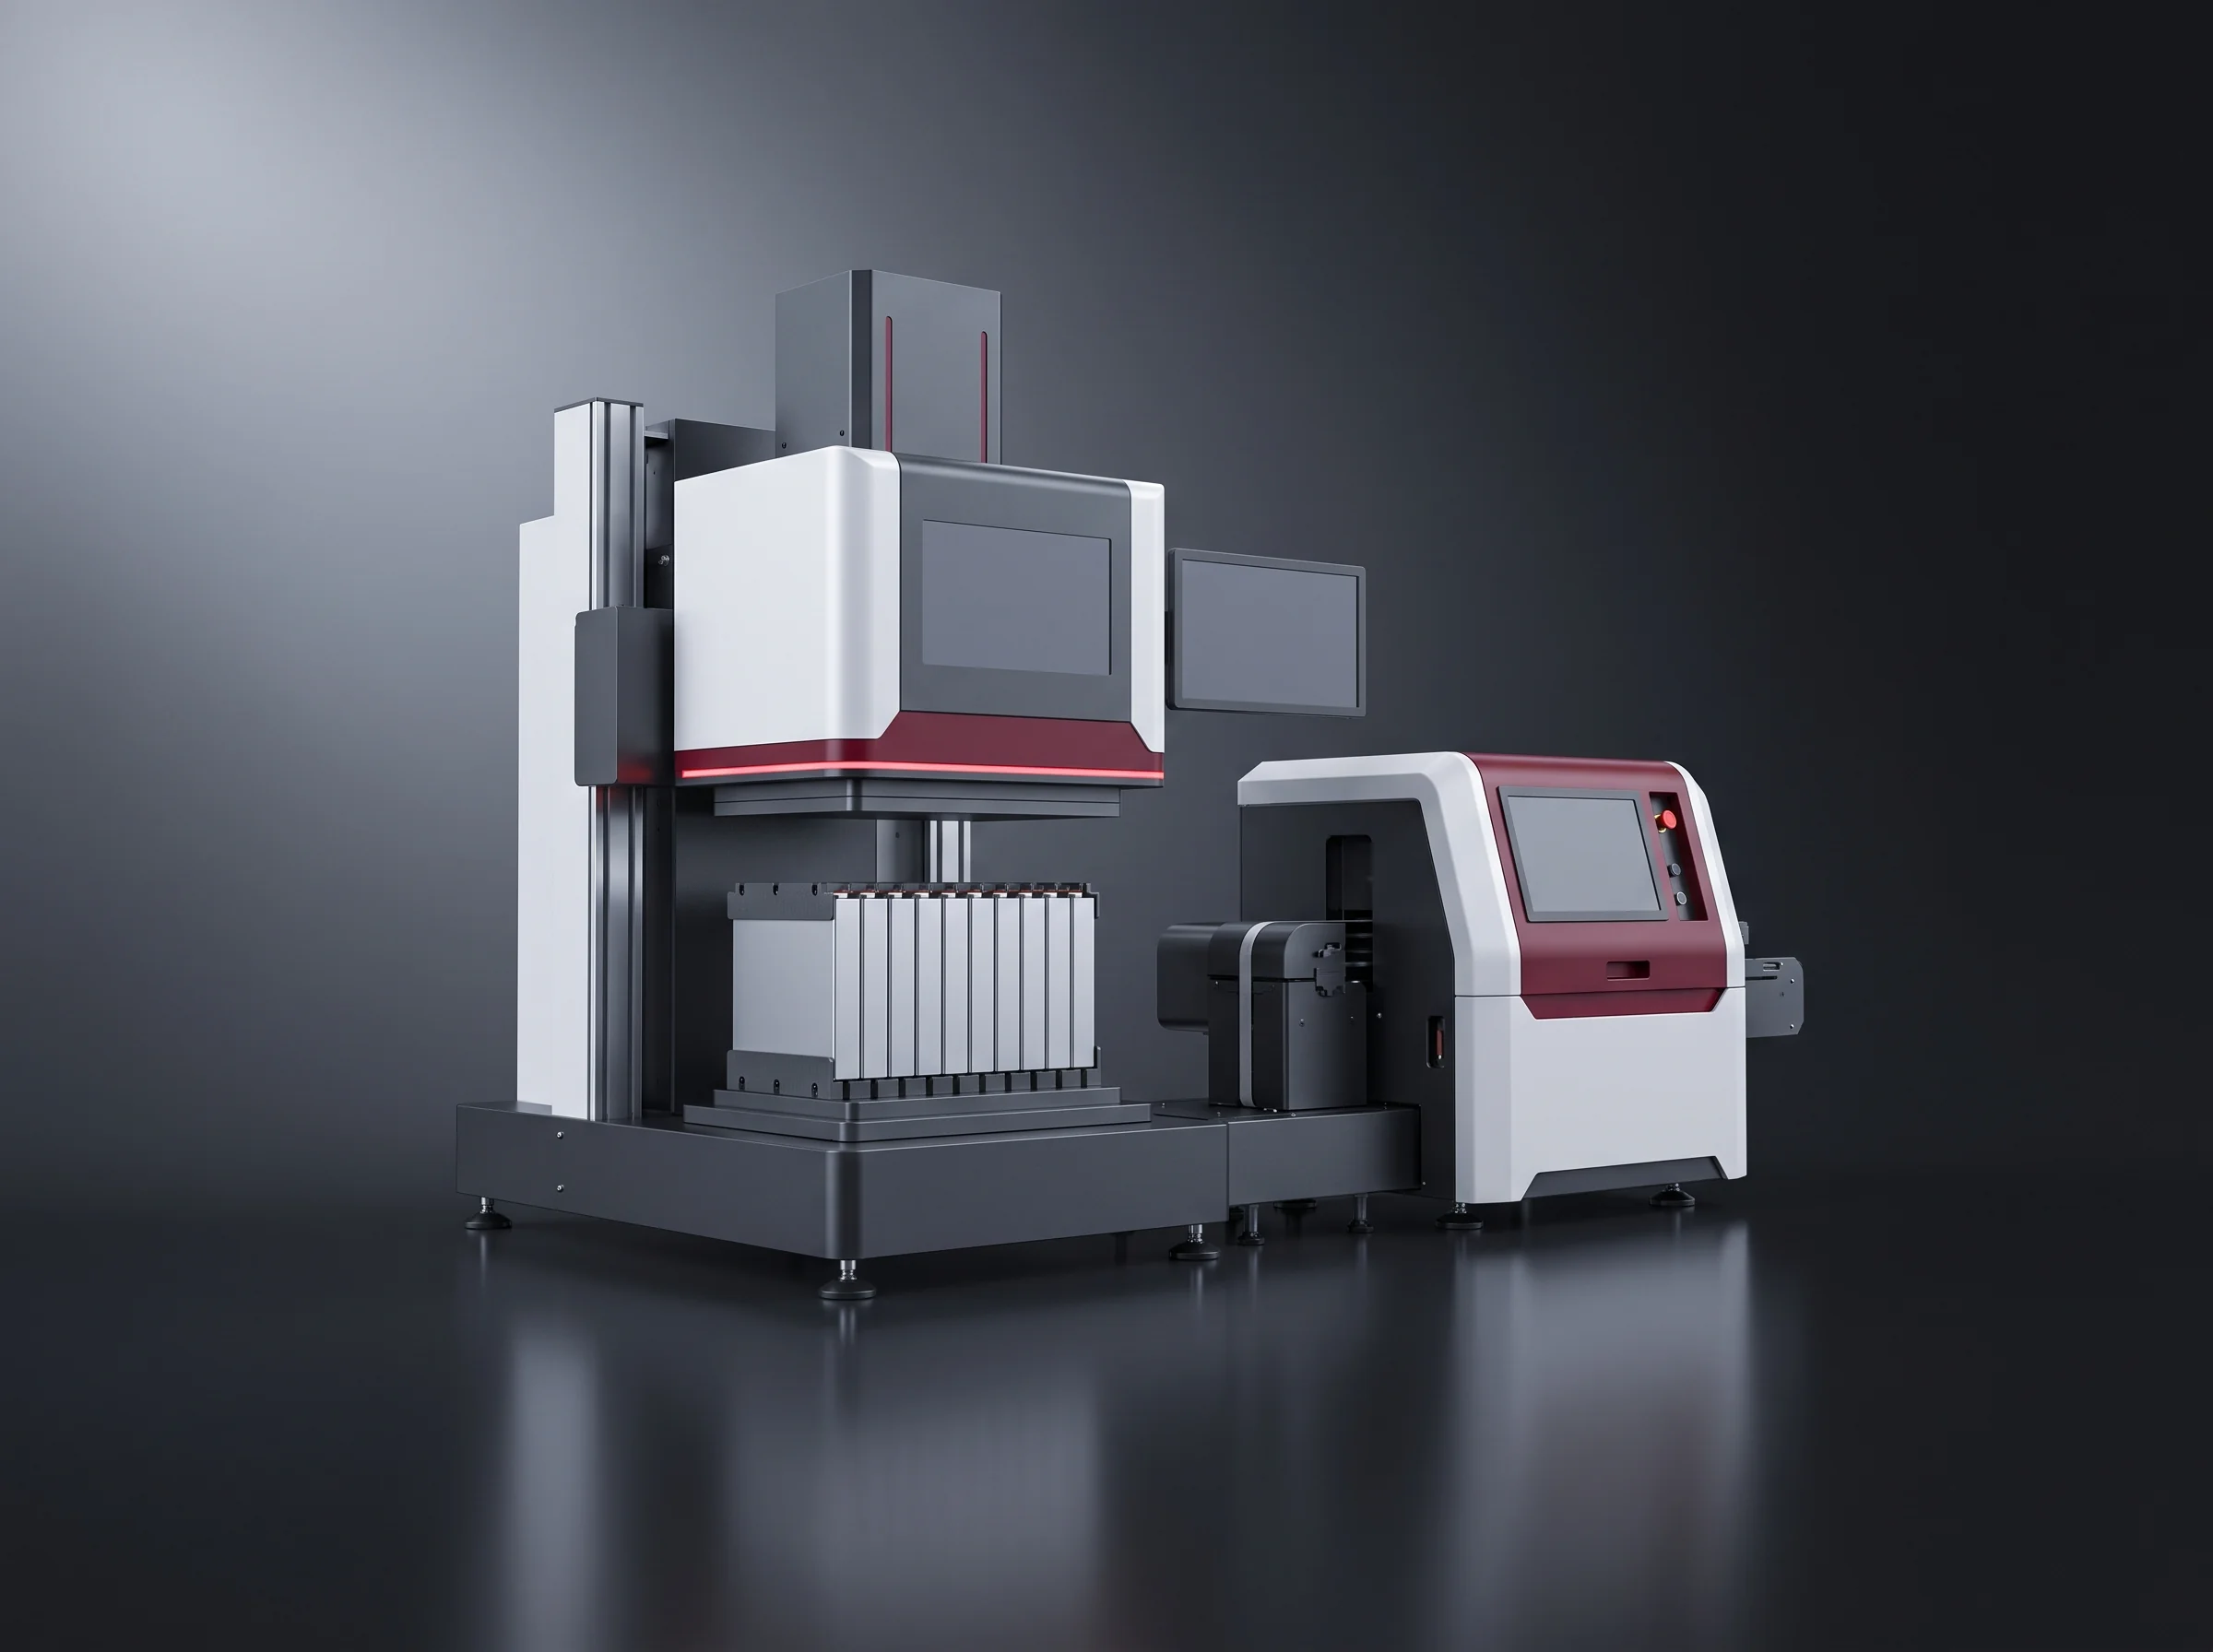
  • 99.9%Scan success
  • ±(0.5%rdg+10dgt)Resistance
Full datasheet
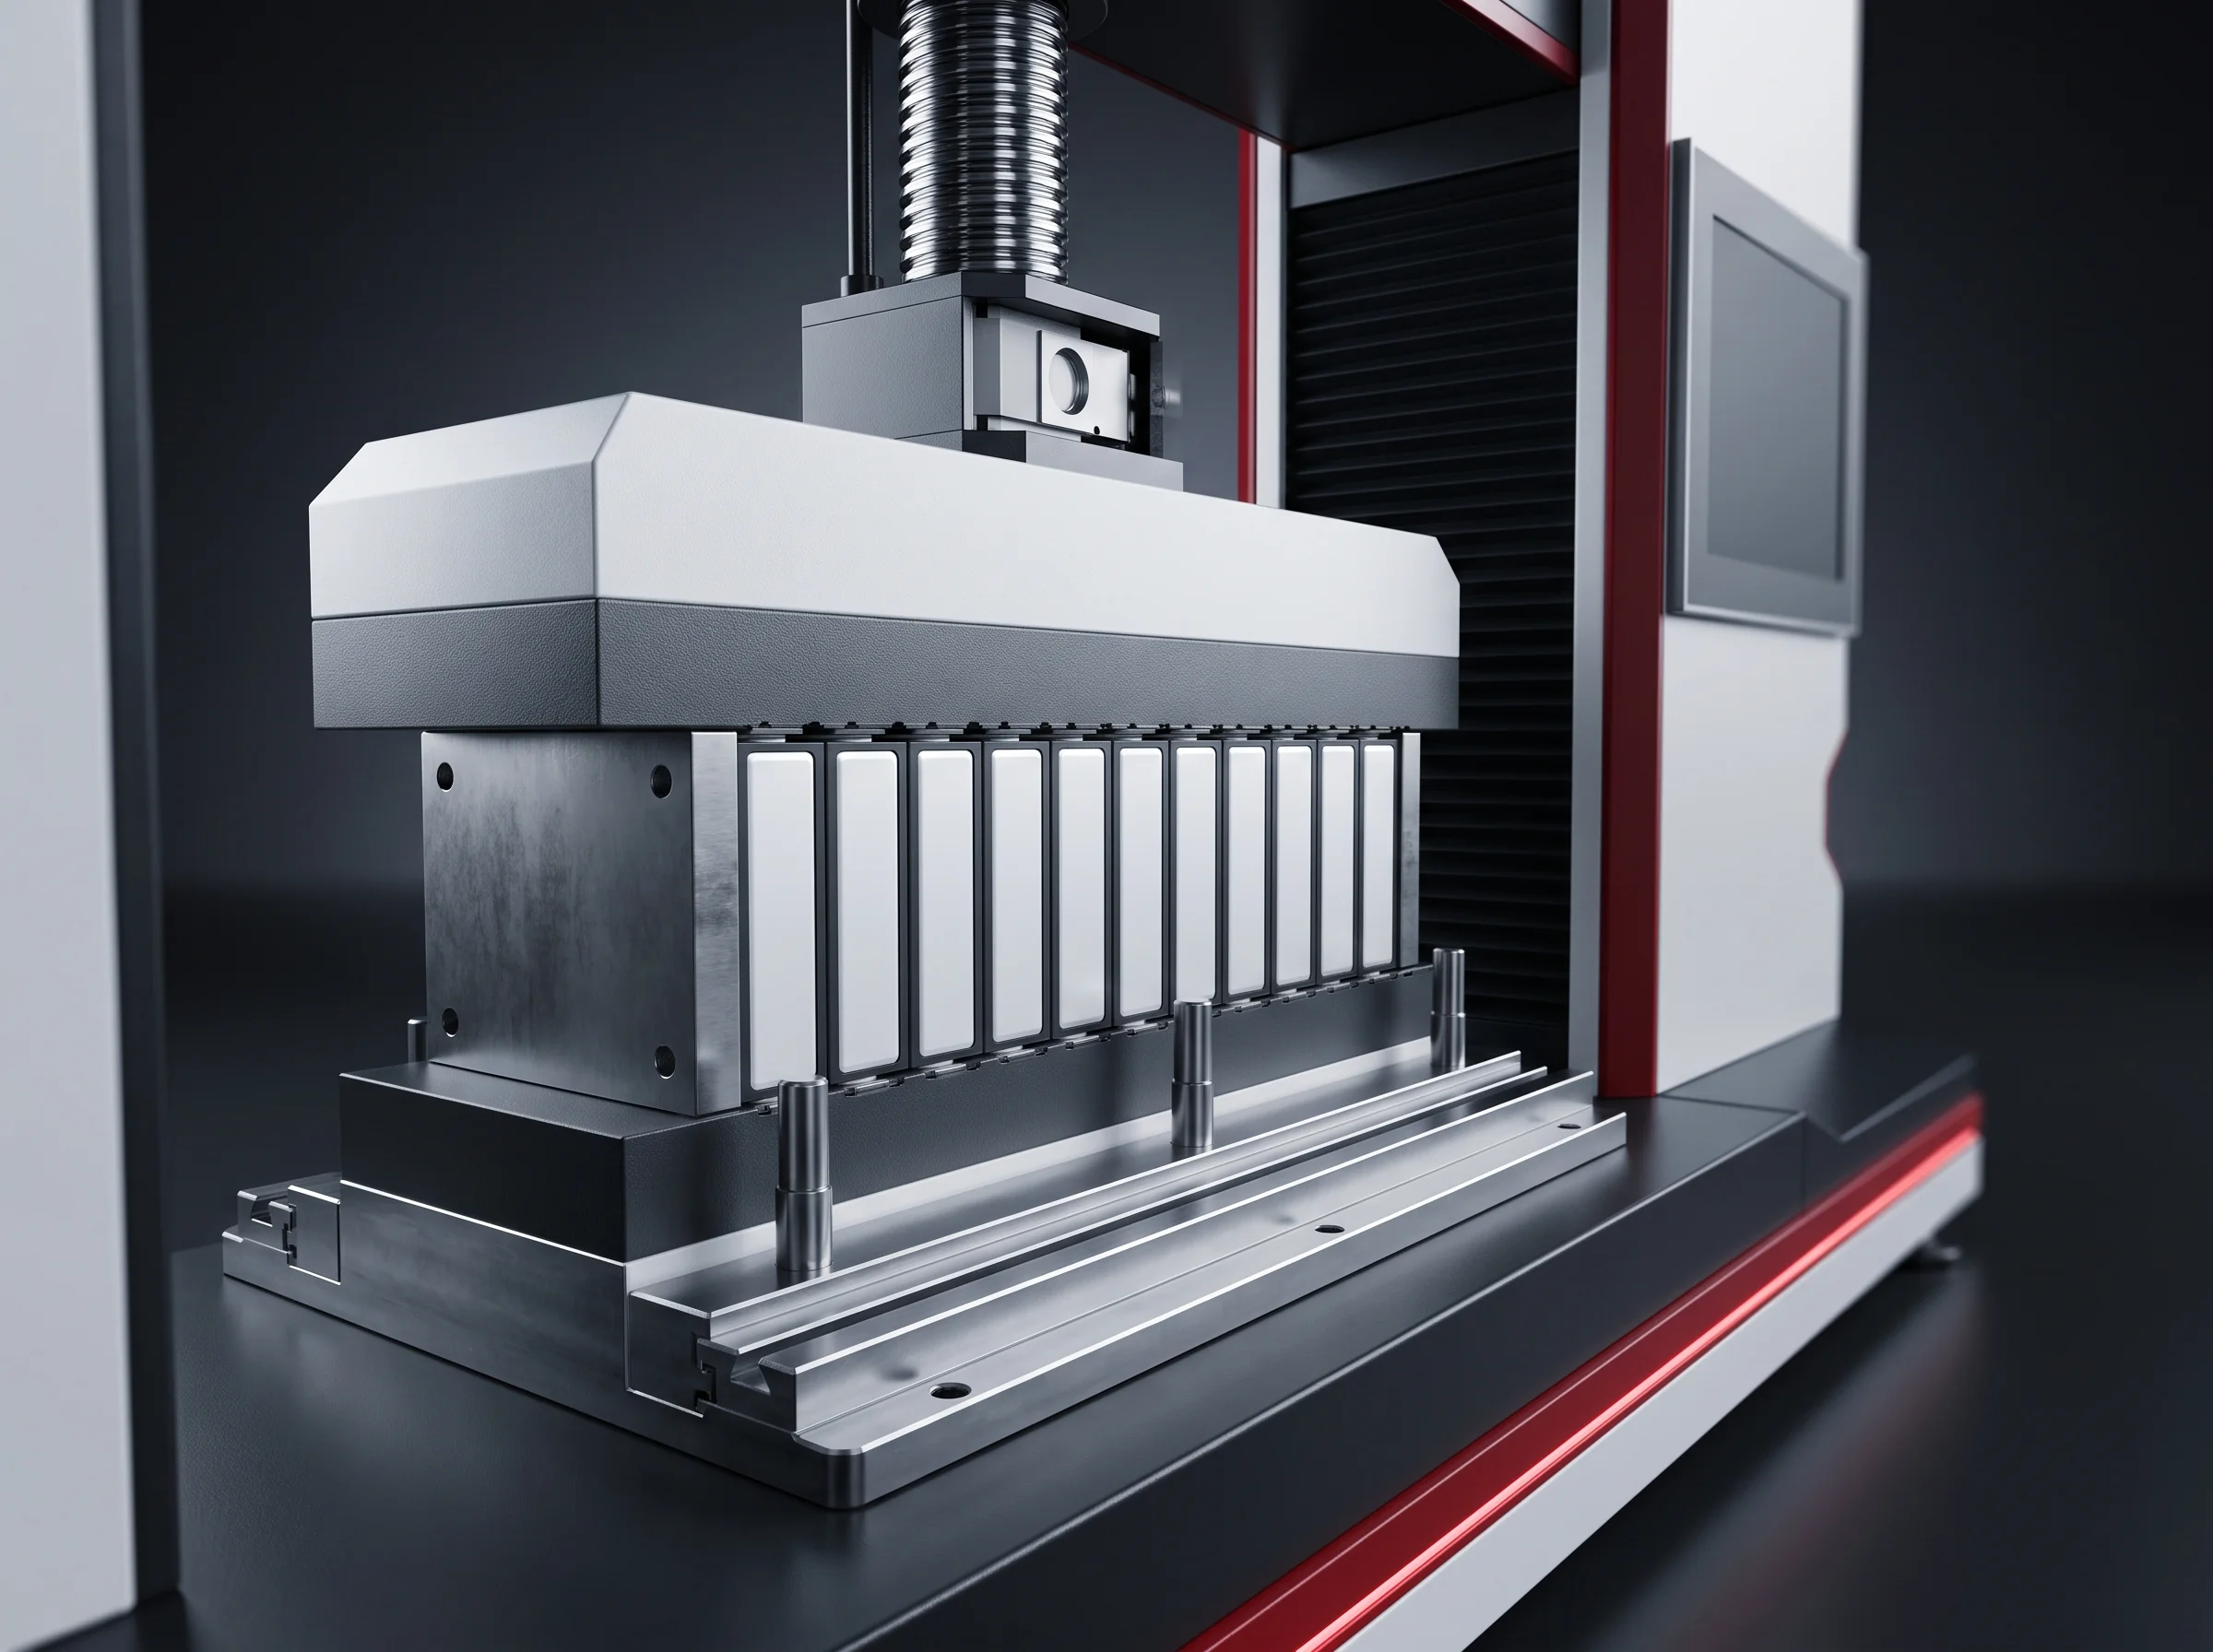
BLP-SP module stacking and pressing station with servo press and banding pass
BLP-SPModule 08–09

Stacking and pressing

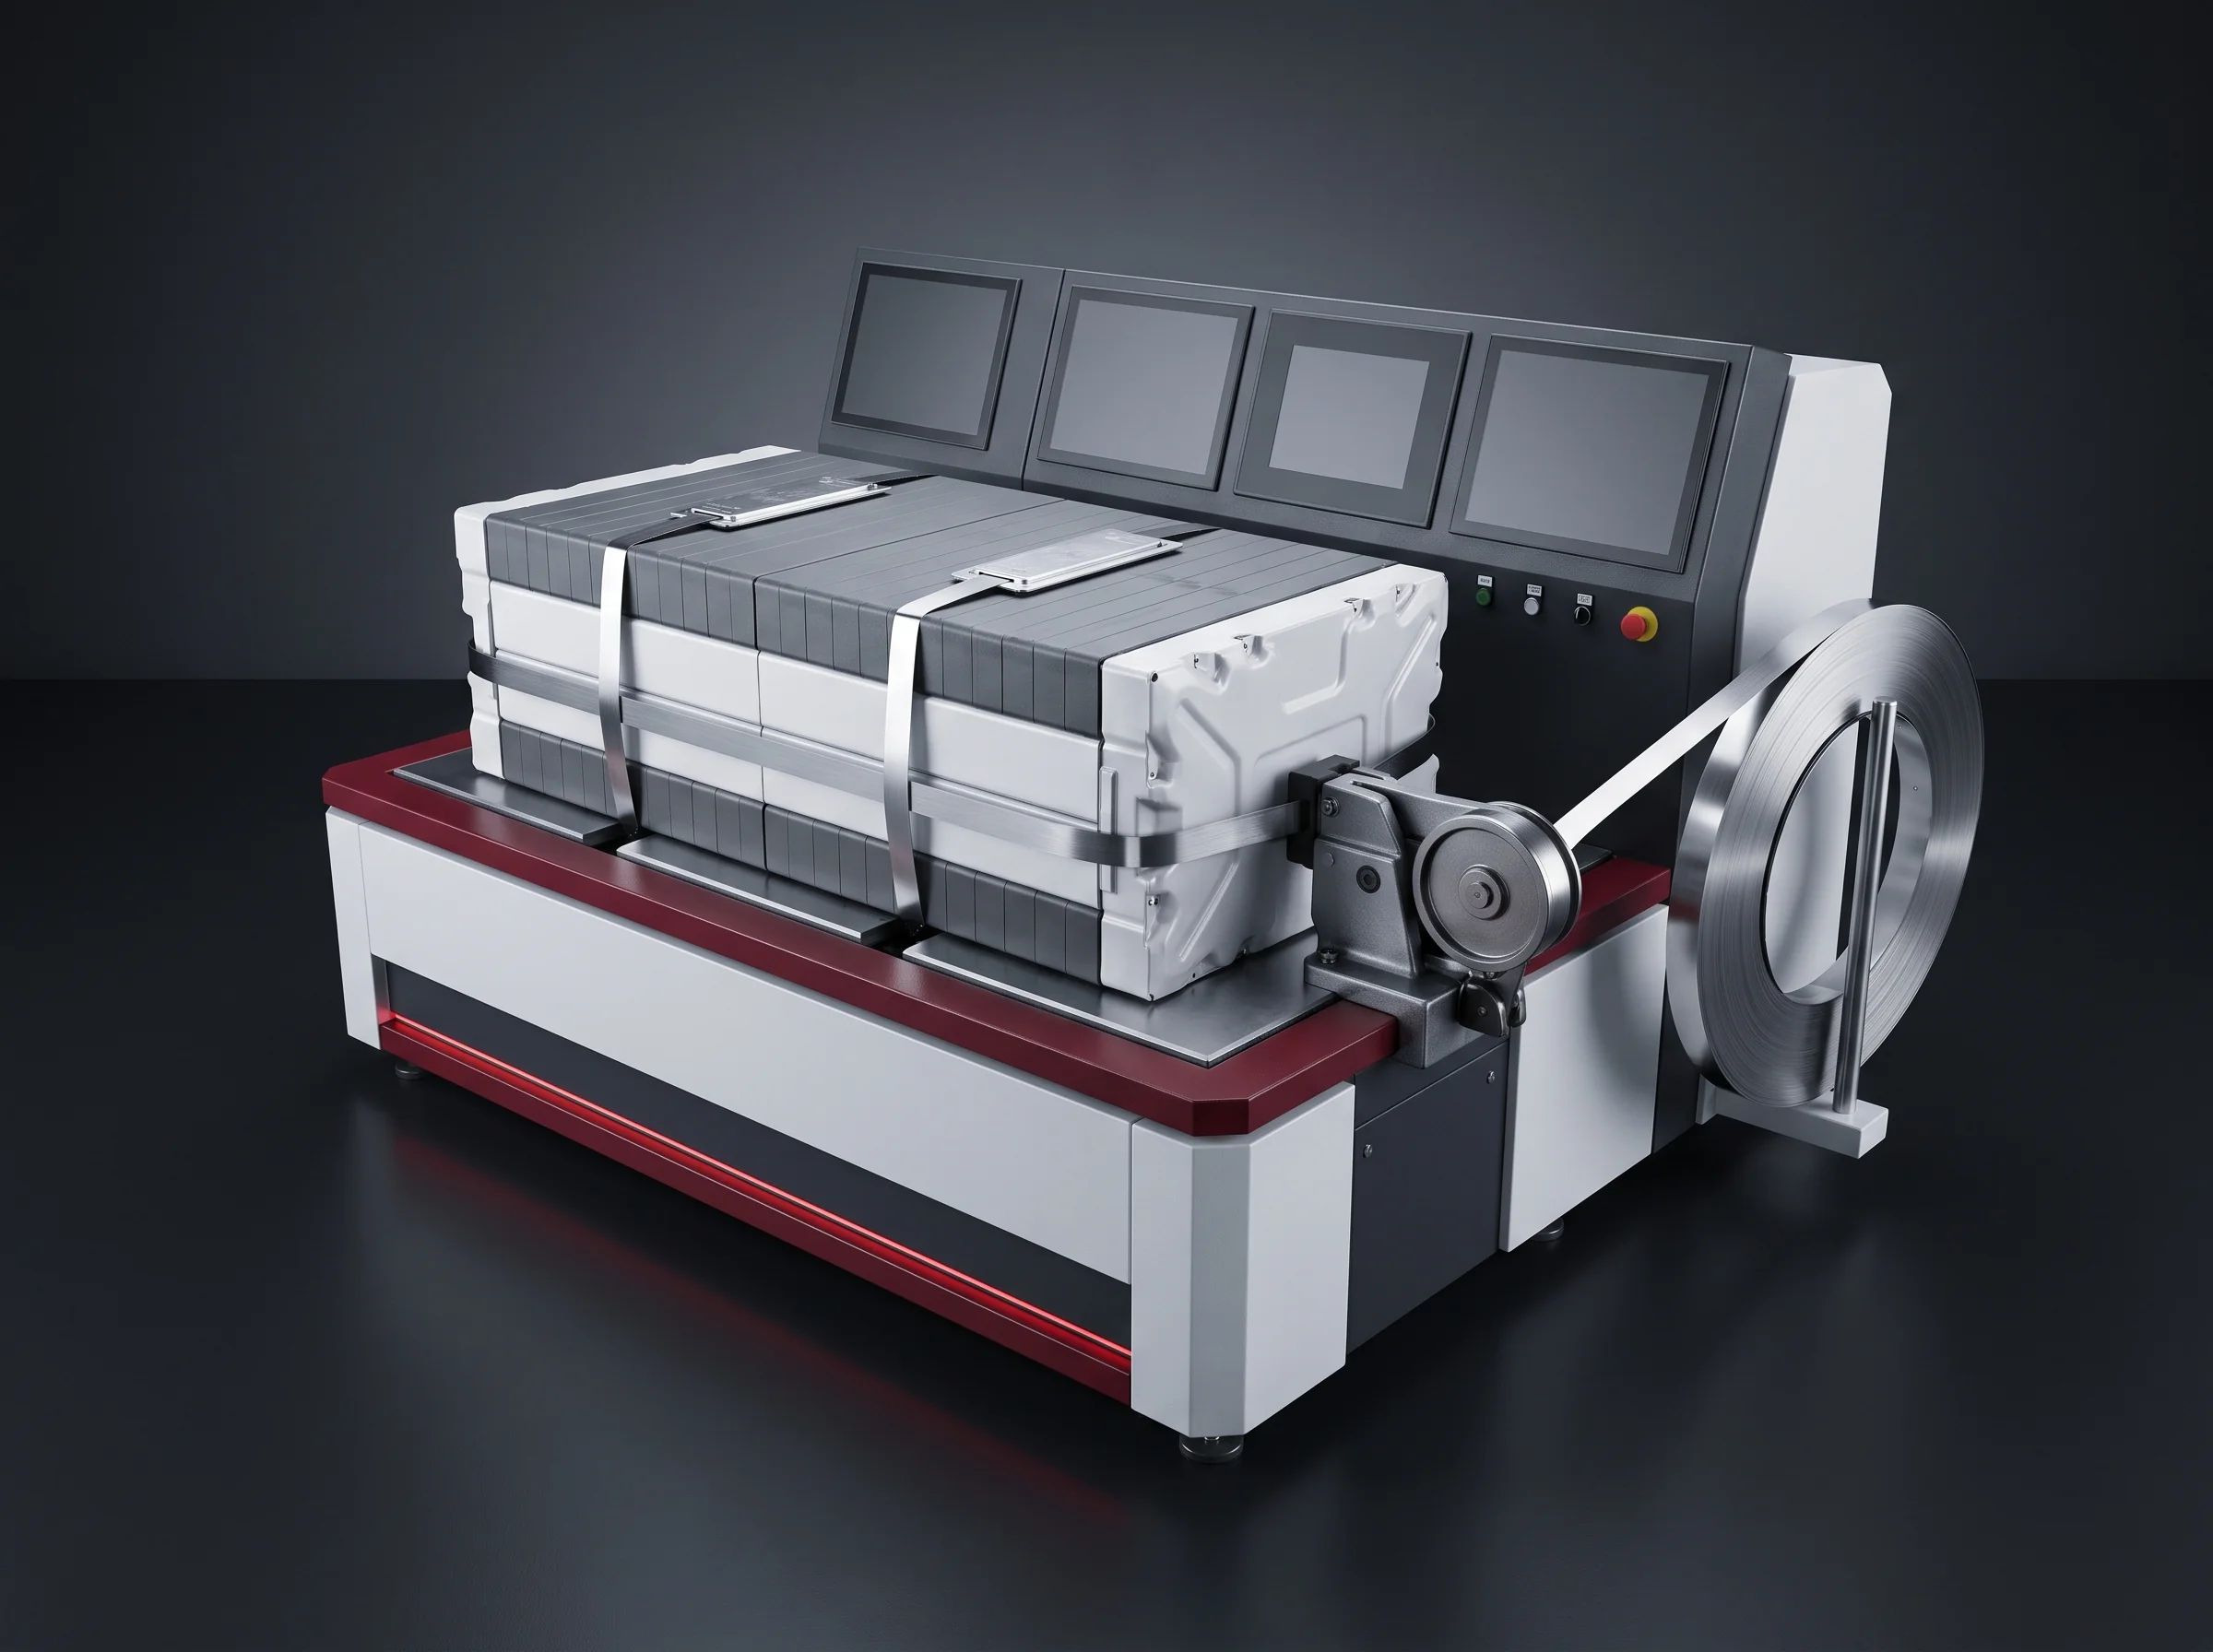
A servo press closes a stack of 8 to 24 cells, holds it by recipe, measures the length and bands it with steel.
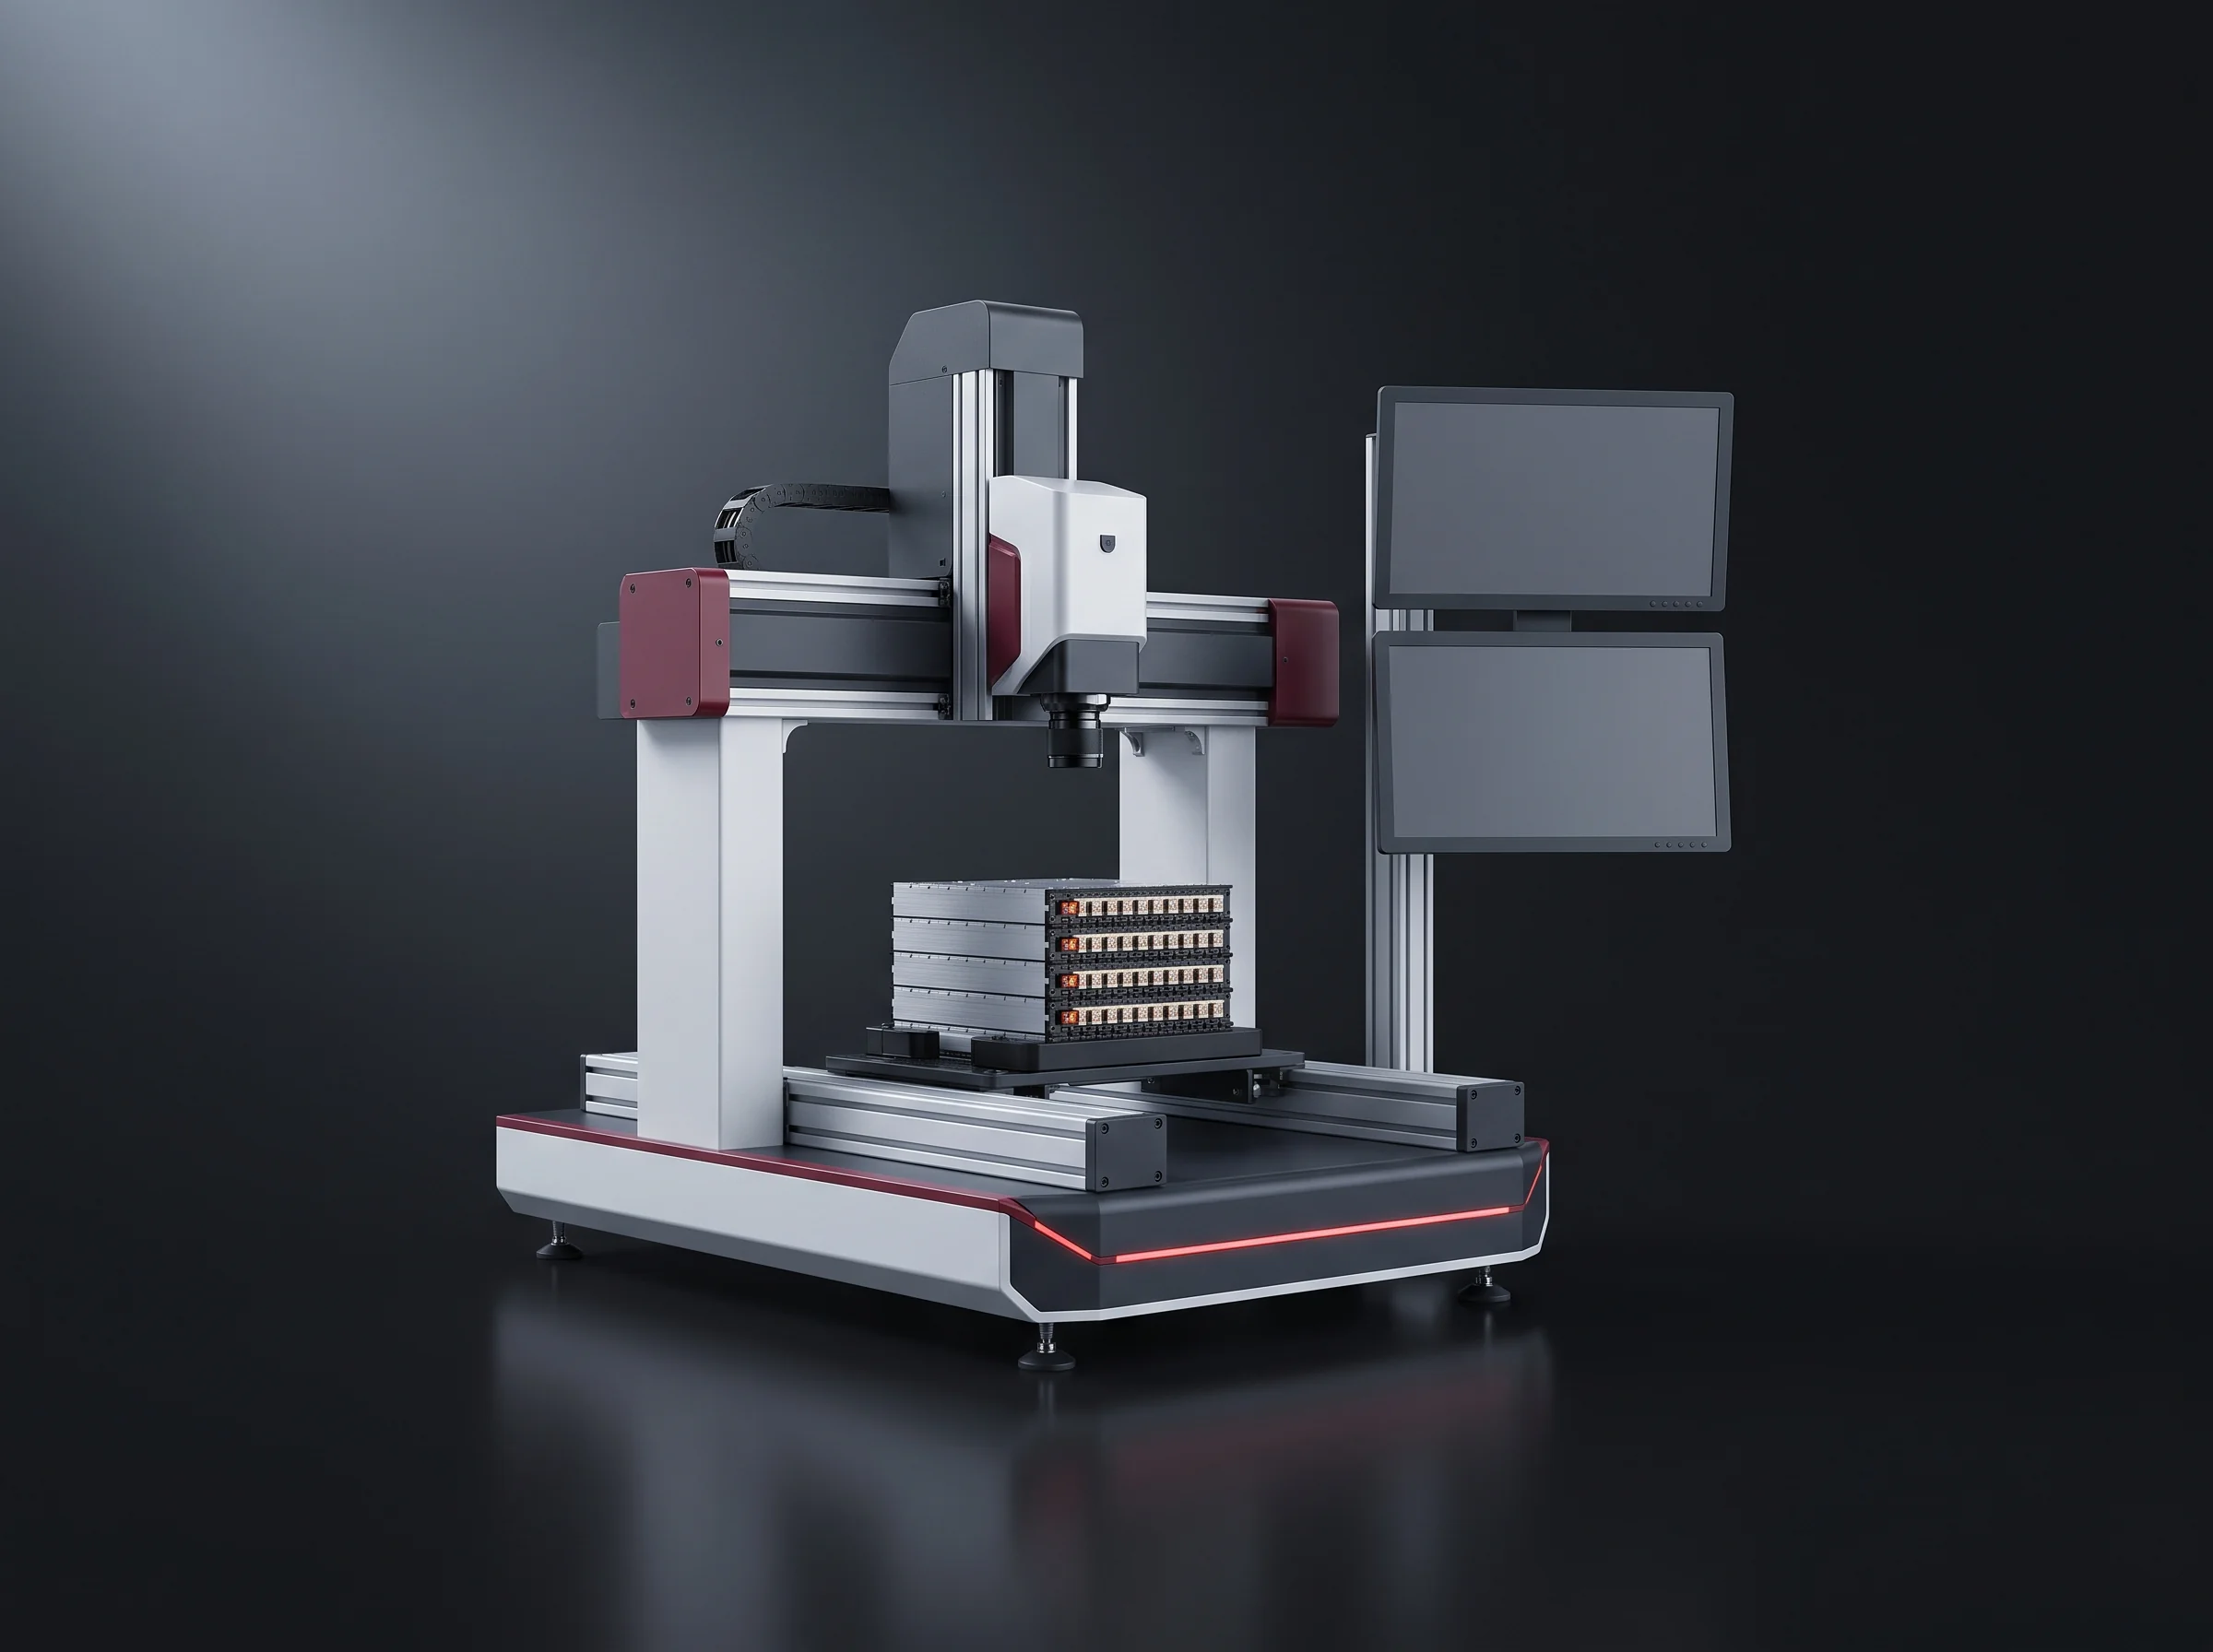
  • 0–8000 NPress force
  • ±0.5 mmModule length
Full datasheet
BLP-AD terminal addressing station reading terminal position and polarity
BLP-ADModule 11

Terminal addressing

One vision set finds each terminal centre and reads polarity in one shot; a pulsed laser cleans a 2 mm ring on the post.
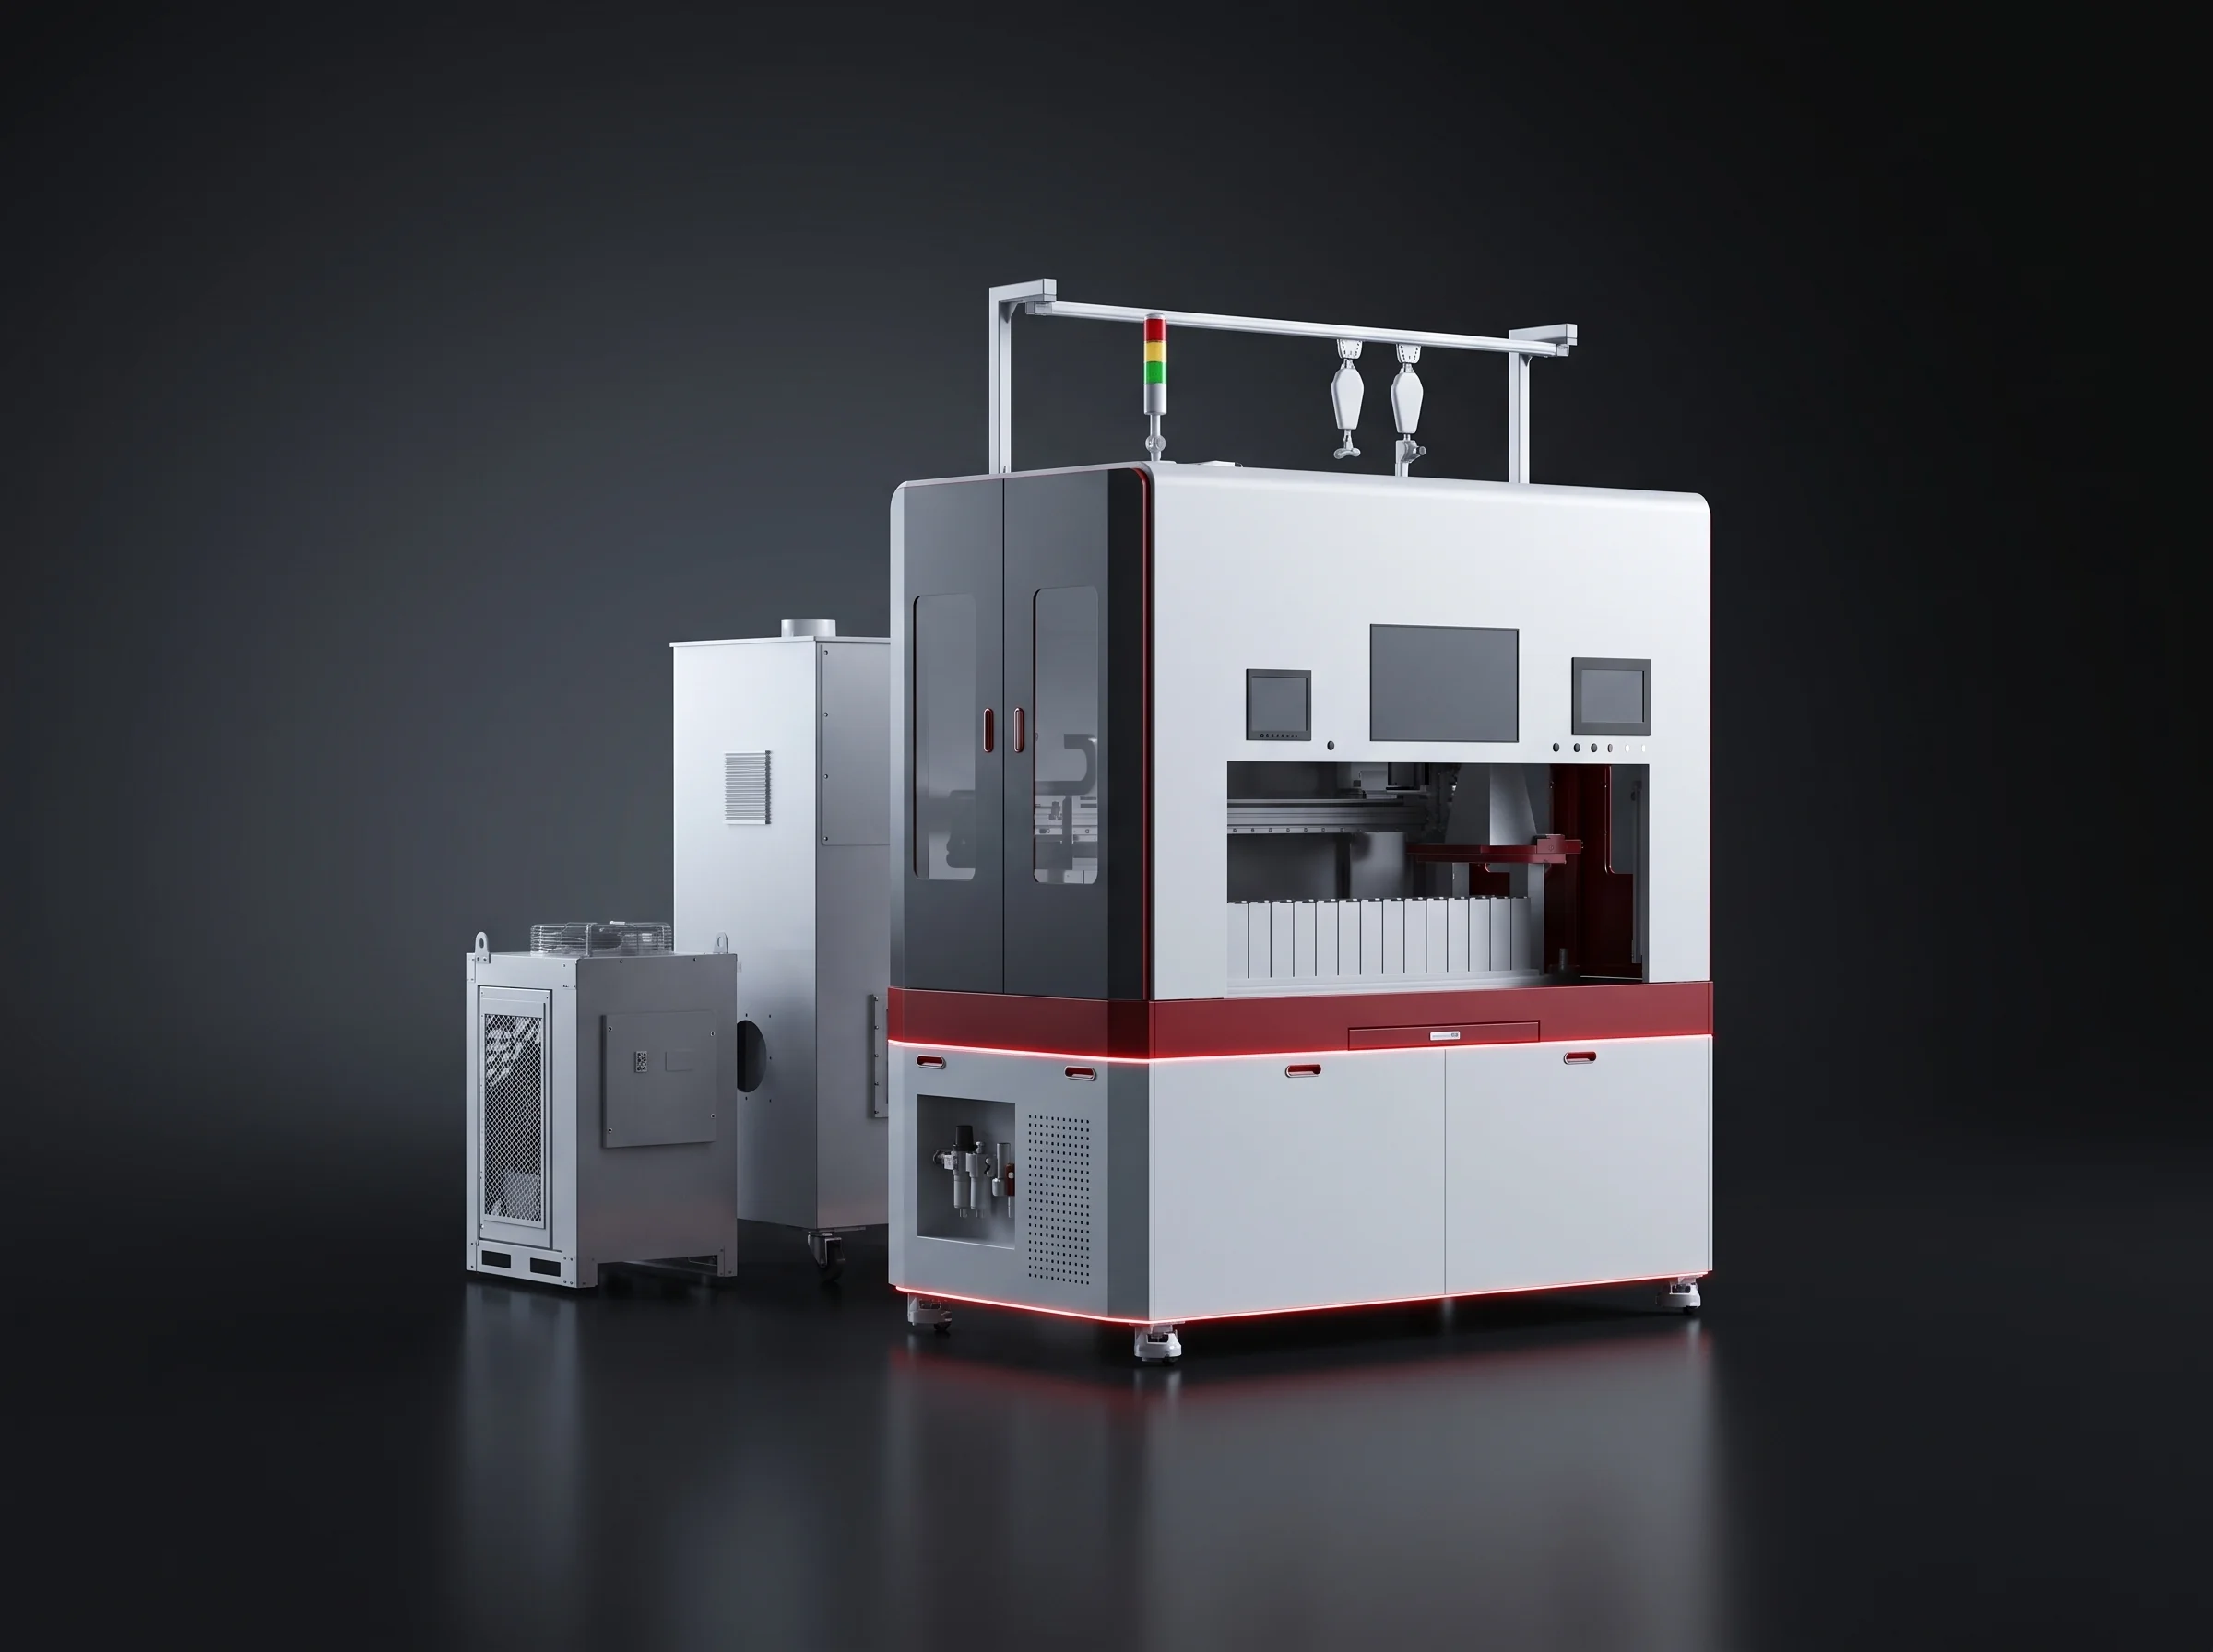
  • ±0.2 mmAddressing
  • 200–300 mm/sMotion
Full datasheet
BLP-W6 inline busbar laser welding station on the module segment
BLP-W6Module 13

Inline busbar welding

A 6 kW laser welds single-row and double-row modules at 50 to 100 mm/s, on the recipe stored against that busbar geometry.
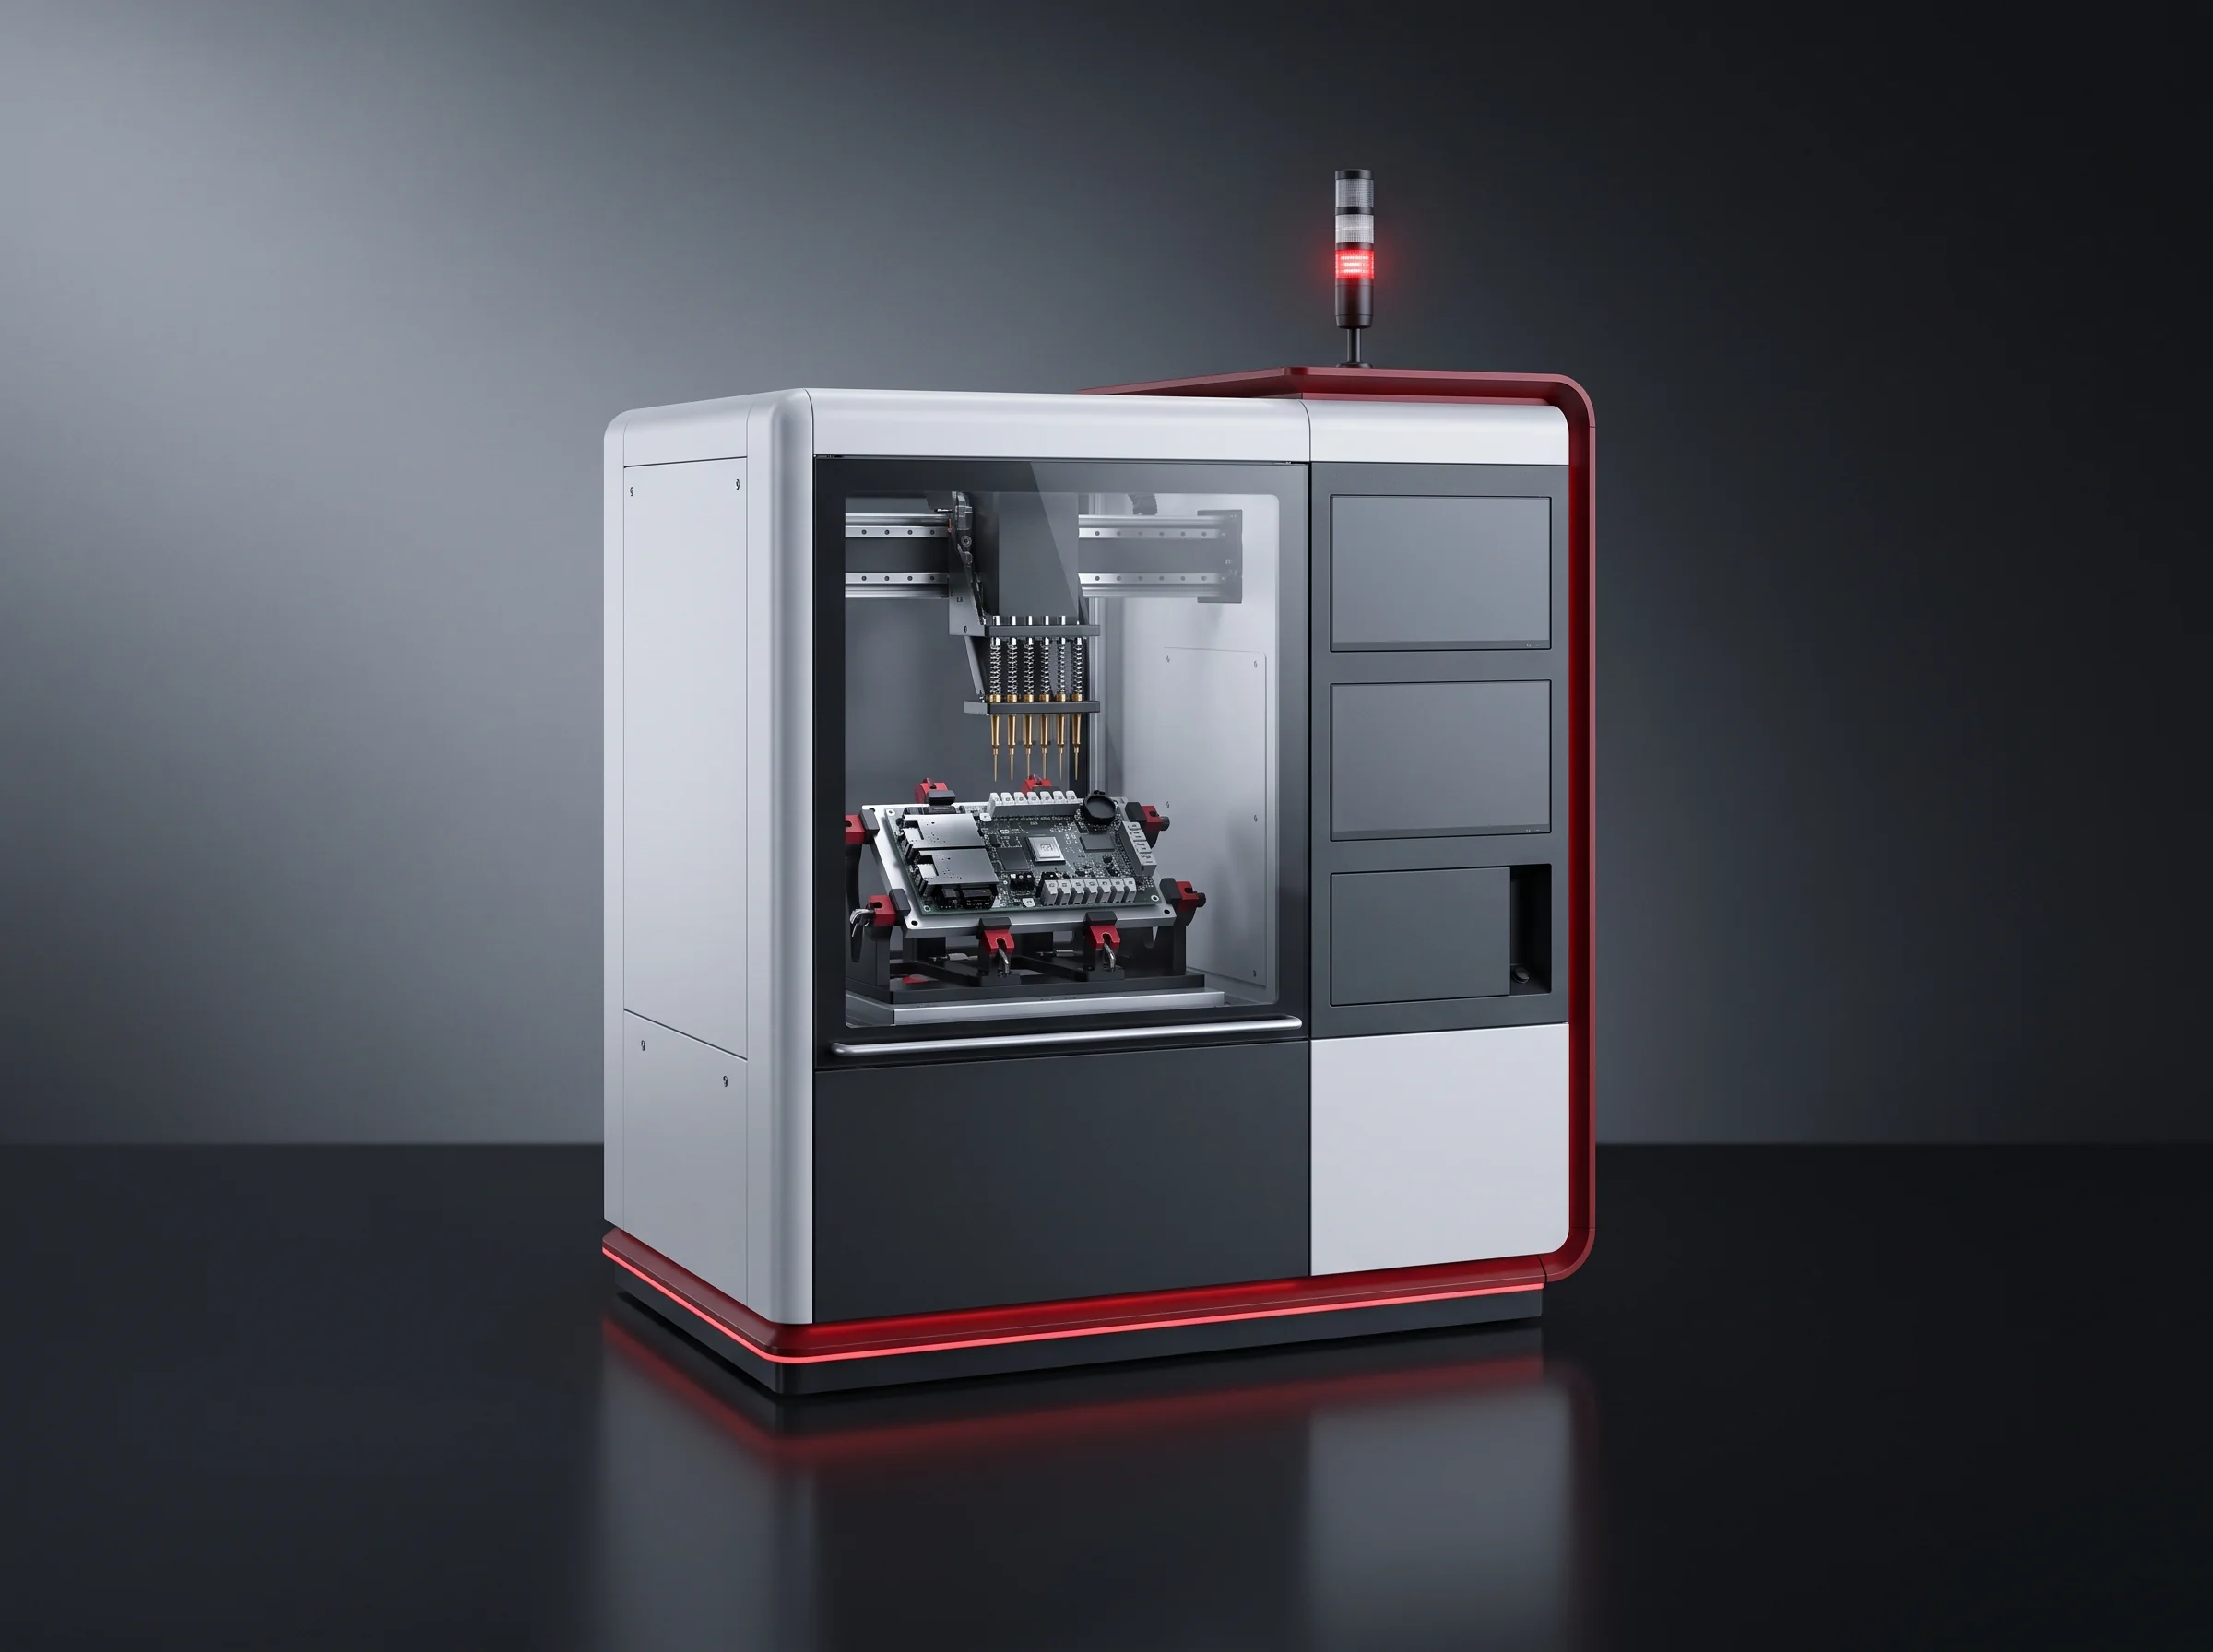
  • ≥1000 NJoint pull force
  • ≥1.0 mmPenetration
Full datasheet
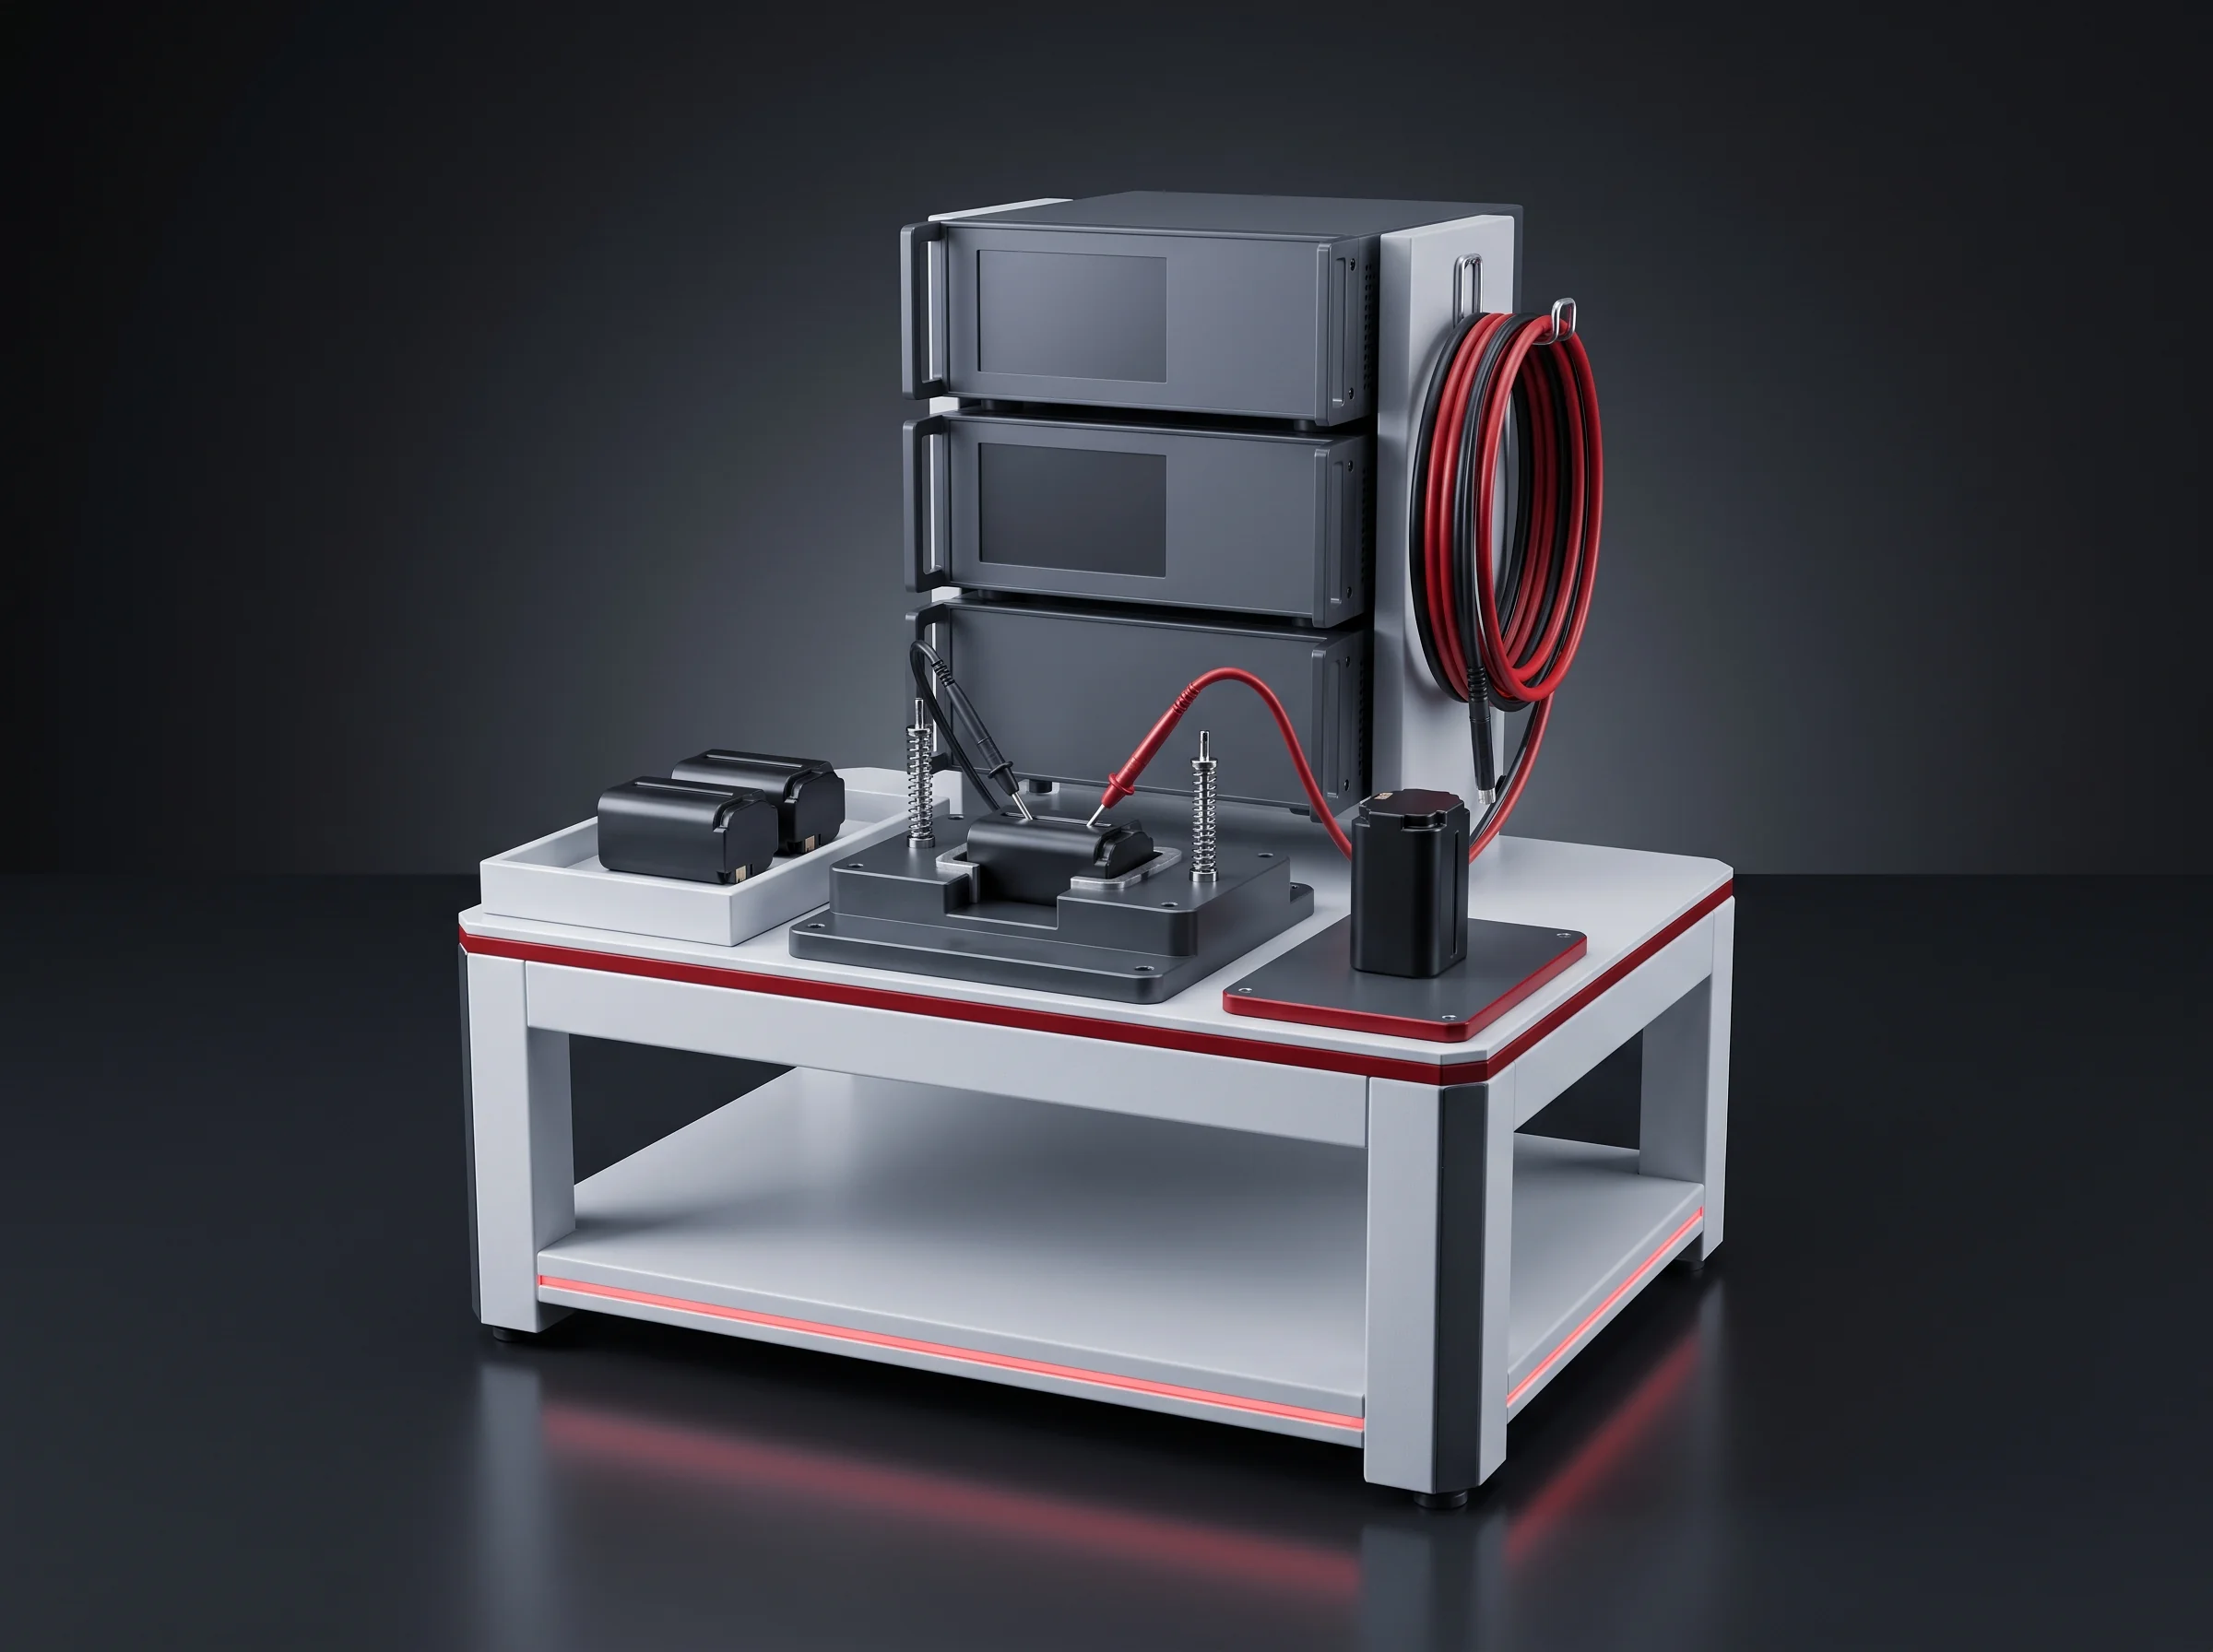
BLP-EOL end-of-line testing station used on both the module and the pack
BLP-EOLModule 16 & Pack 14

End-of-line testing

Insulation, hipot, voltage with resistance and continuity, run once on the module and again on the pack.
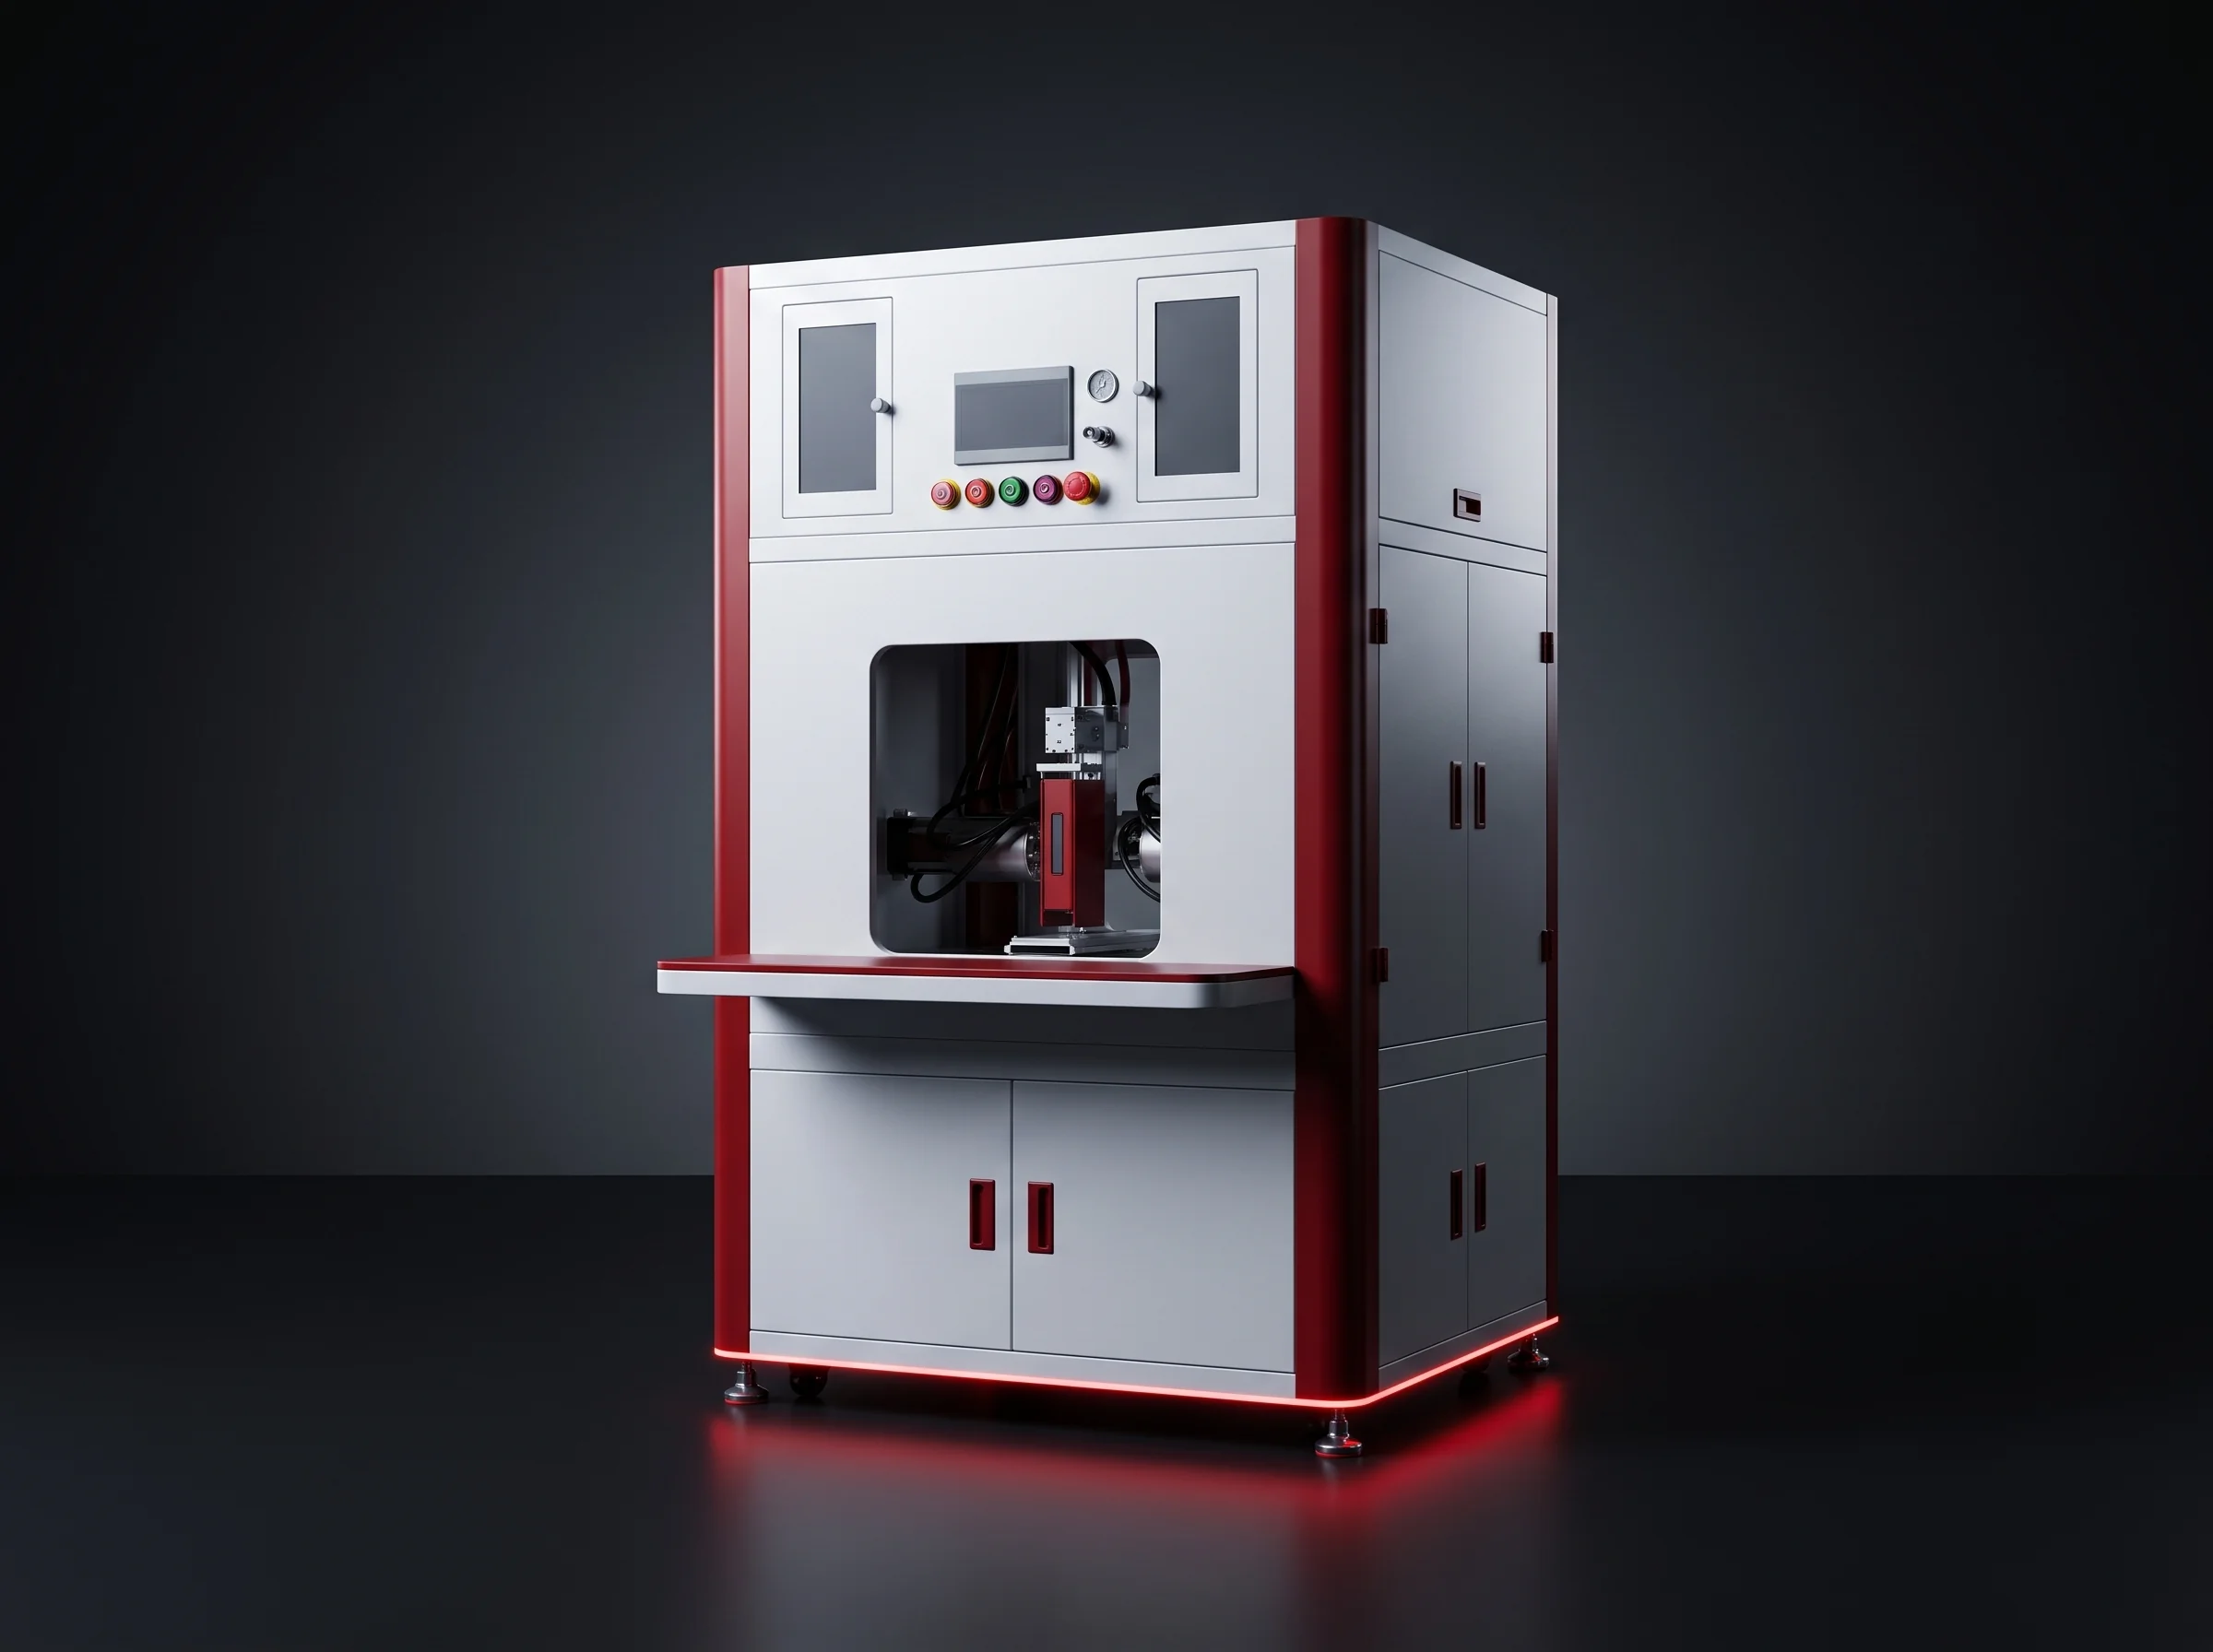
  • ≥500 MΩInsulation, DC 1000 V
  • DC 2800 VHipot, ≤10 mA
Full datasheet
BLP-GL dispensing station gluing the enclosure floor and cooling plate
BLP-GLPack 03

Cooling plate gluing

Twin servo pumps meter adhesive onto the cooling plate and enclosure floor, with a live pressure trace per pack.
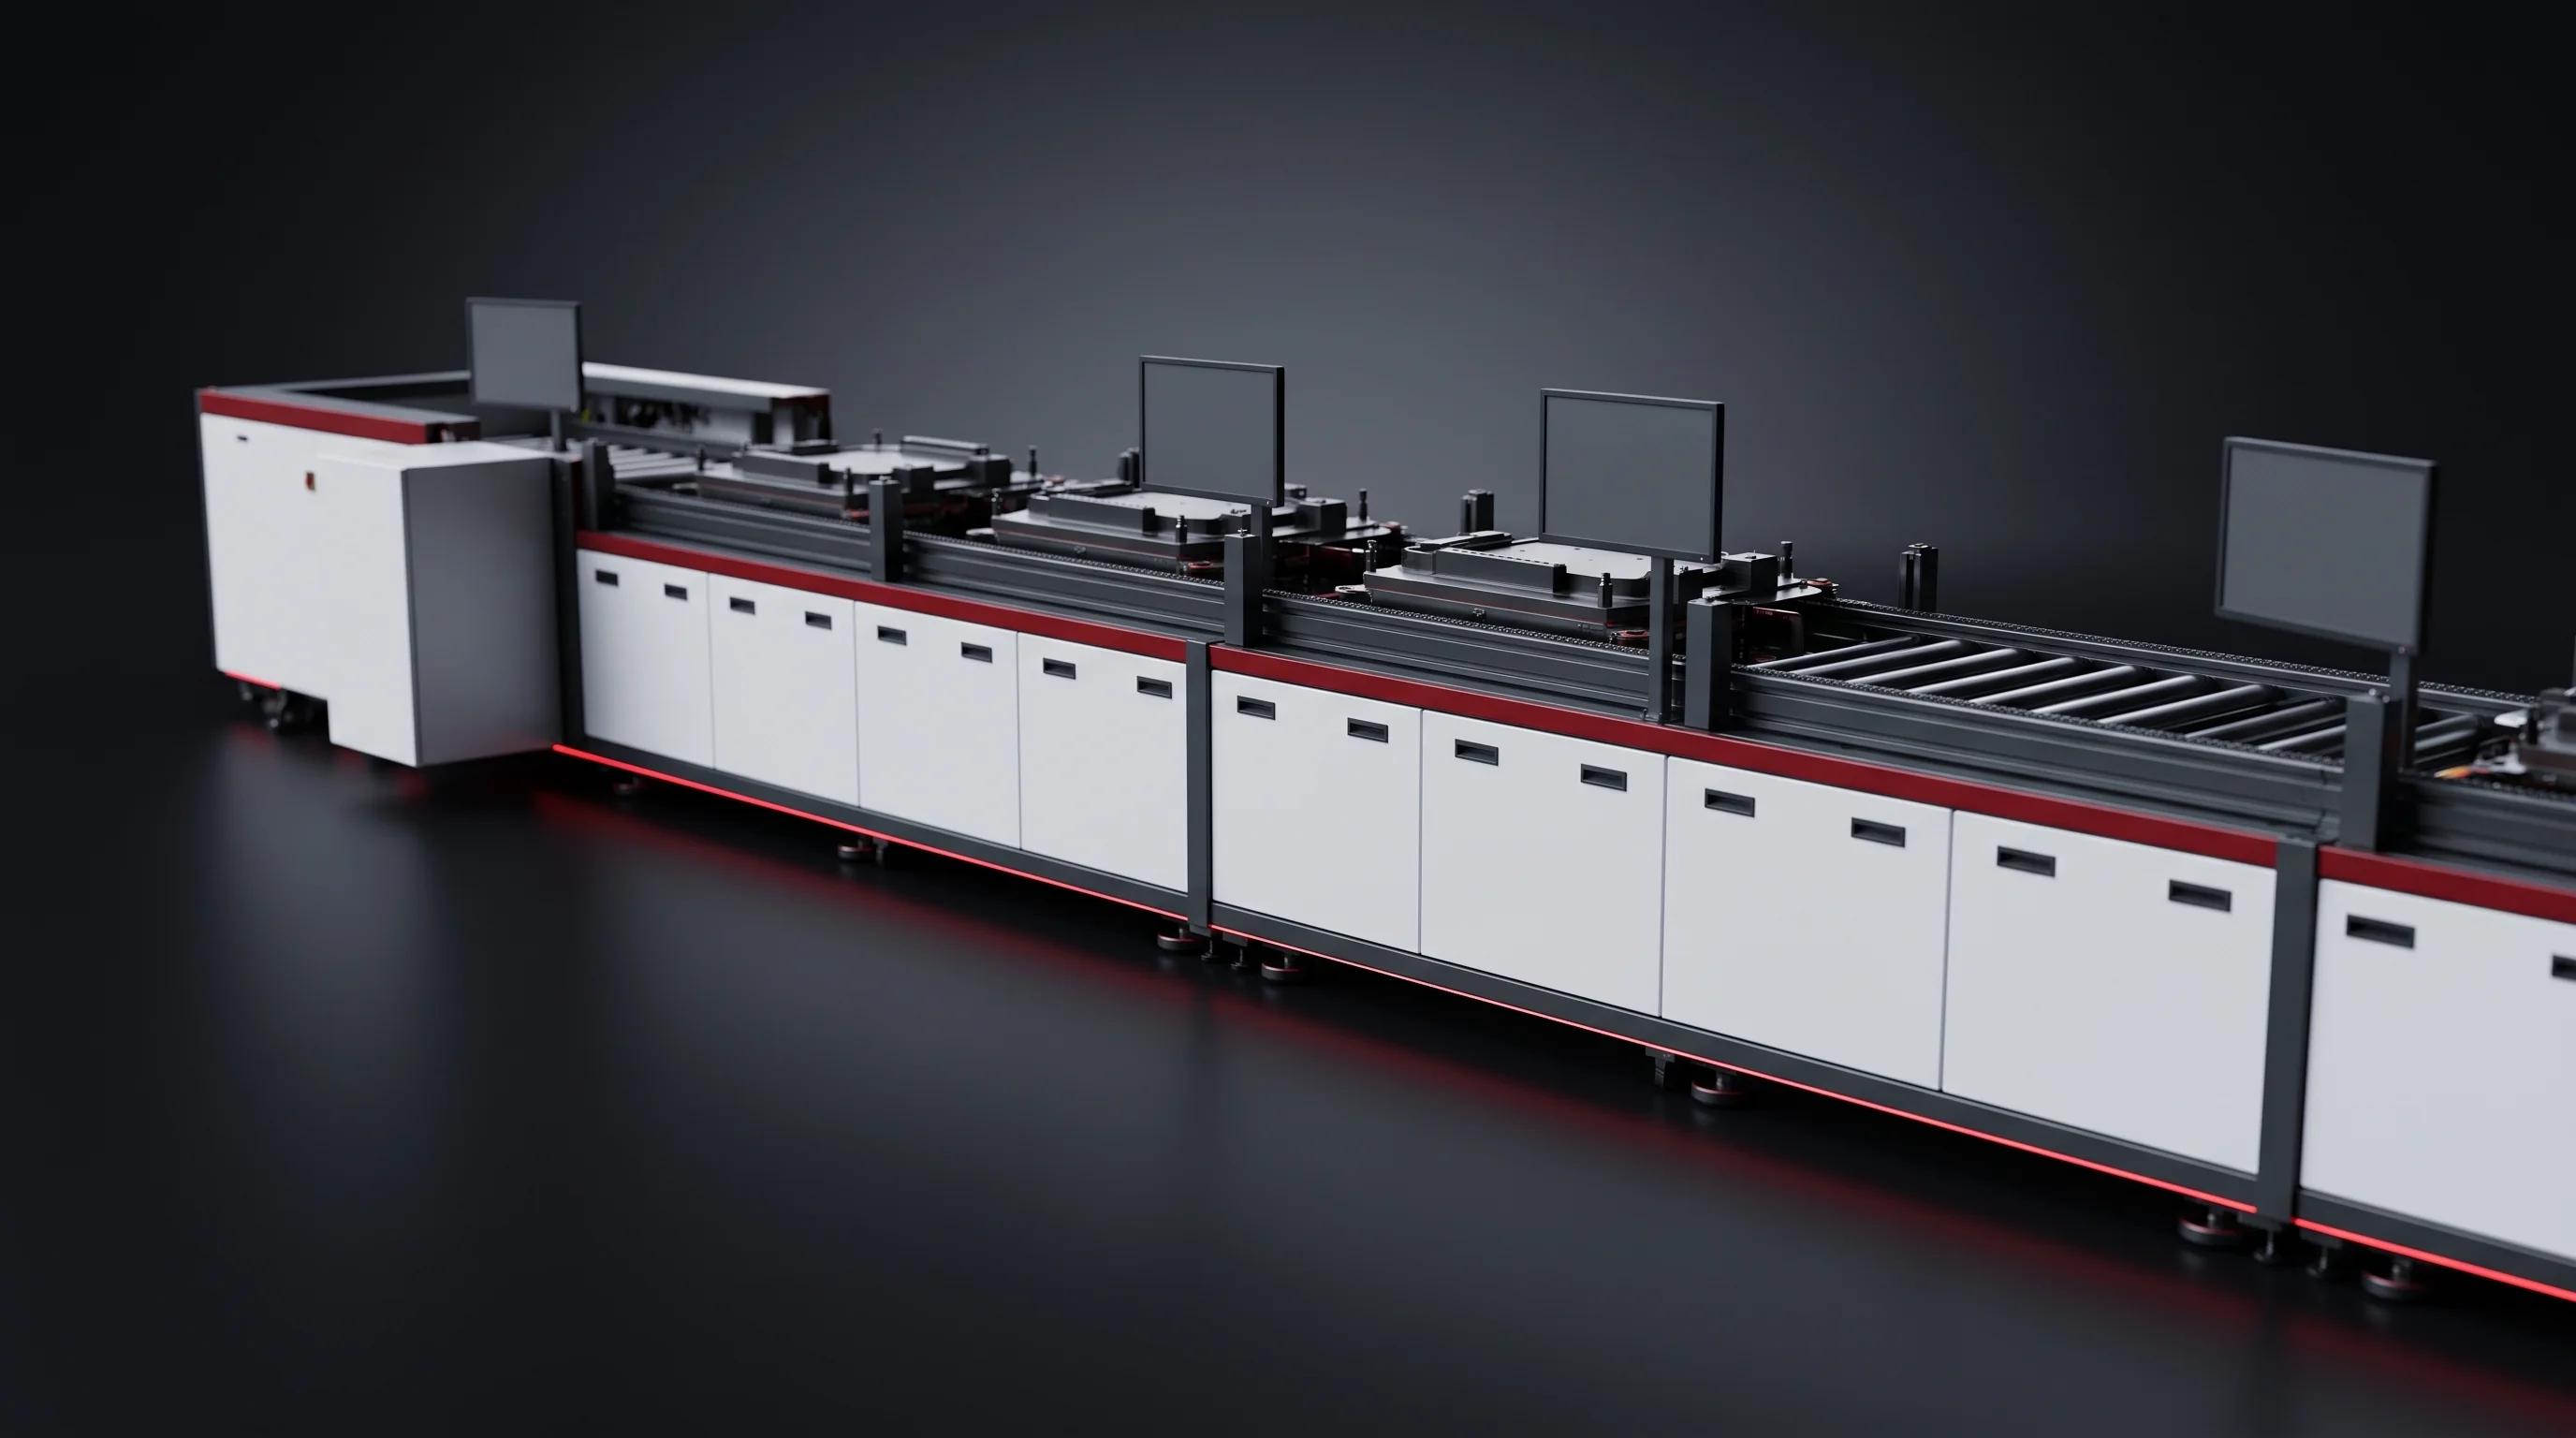
  • ±0.2 mmPhoto location
  • 5%Dispensed volume
Full datasheet
BLP-CV module conveyor with stop-and-lift positioning between stations
BLP-CVBetween stations

Module conveying

Double-speed chain moves modules on 1200 × 400 mm fixtures, each carrying an RFID tag.
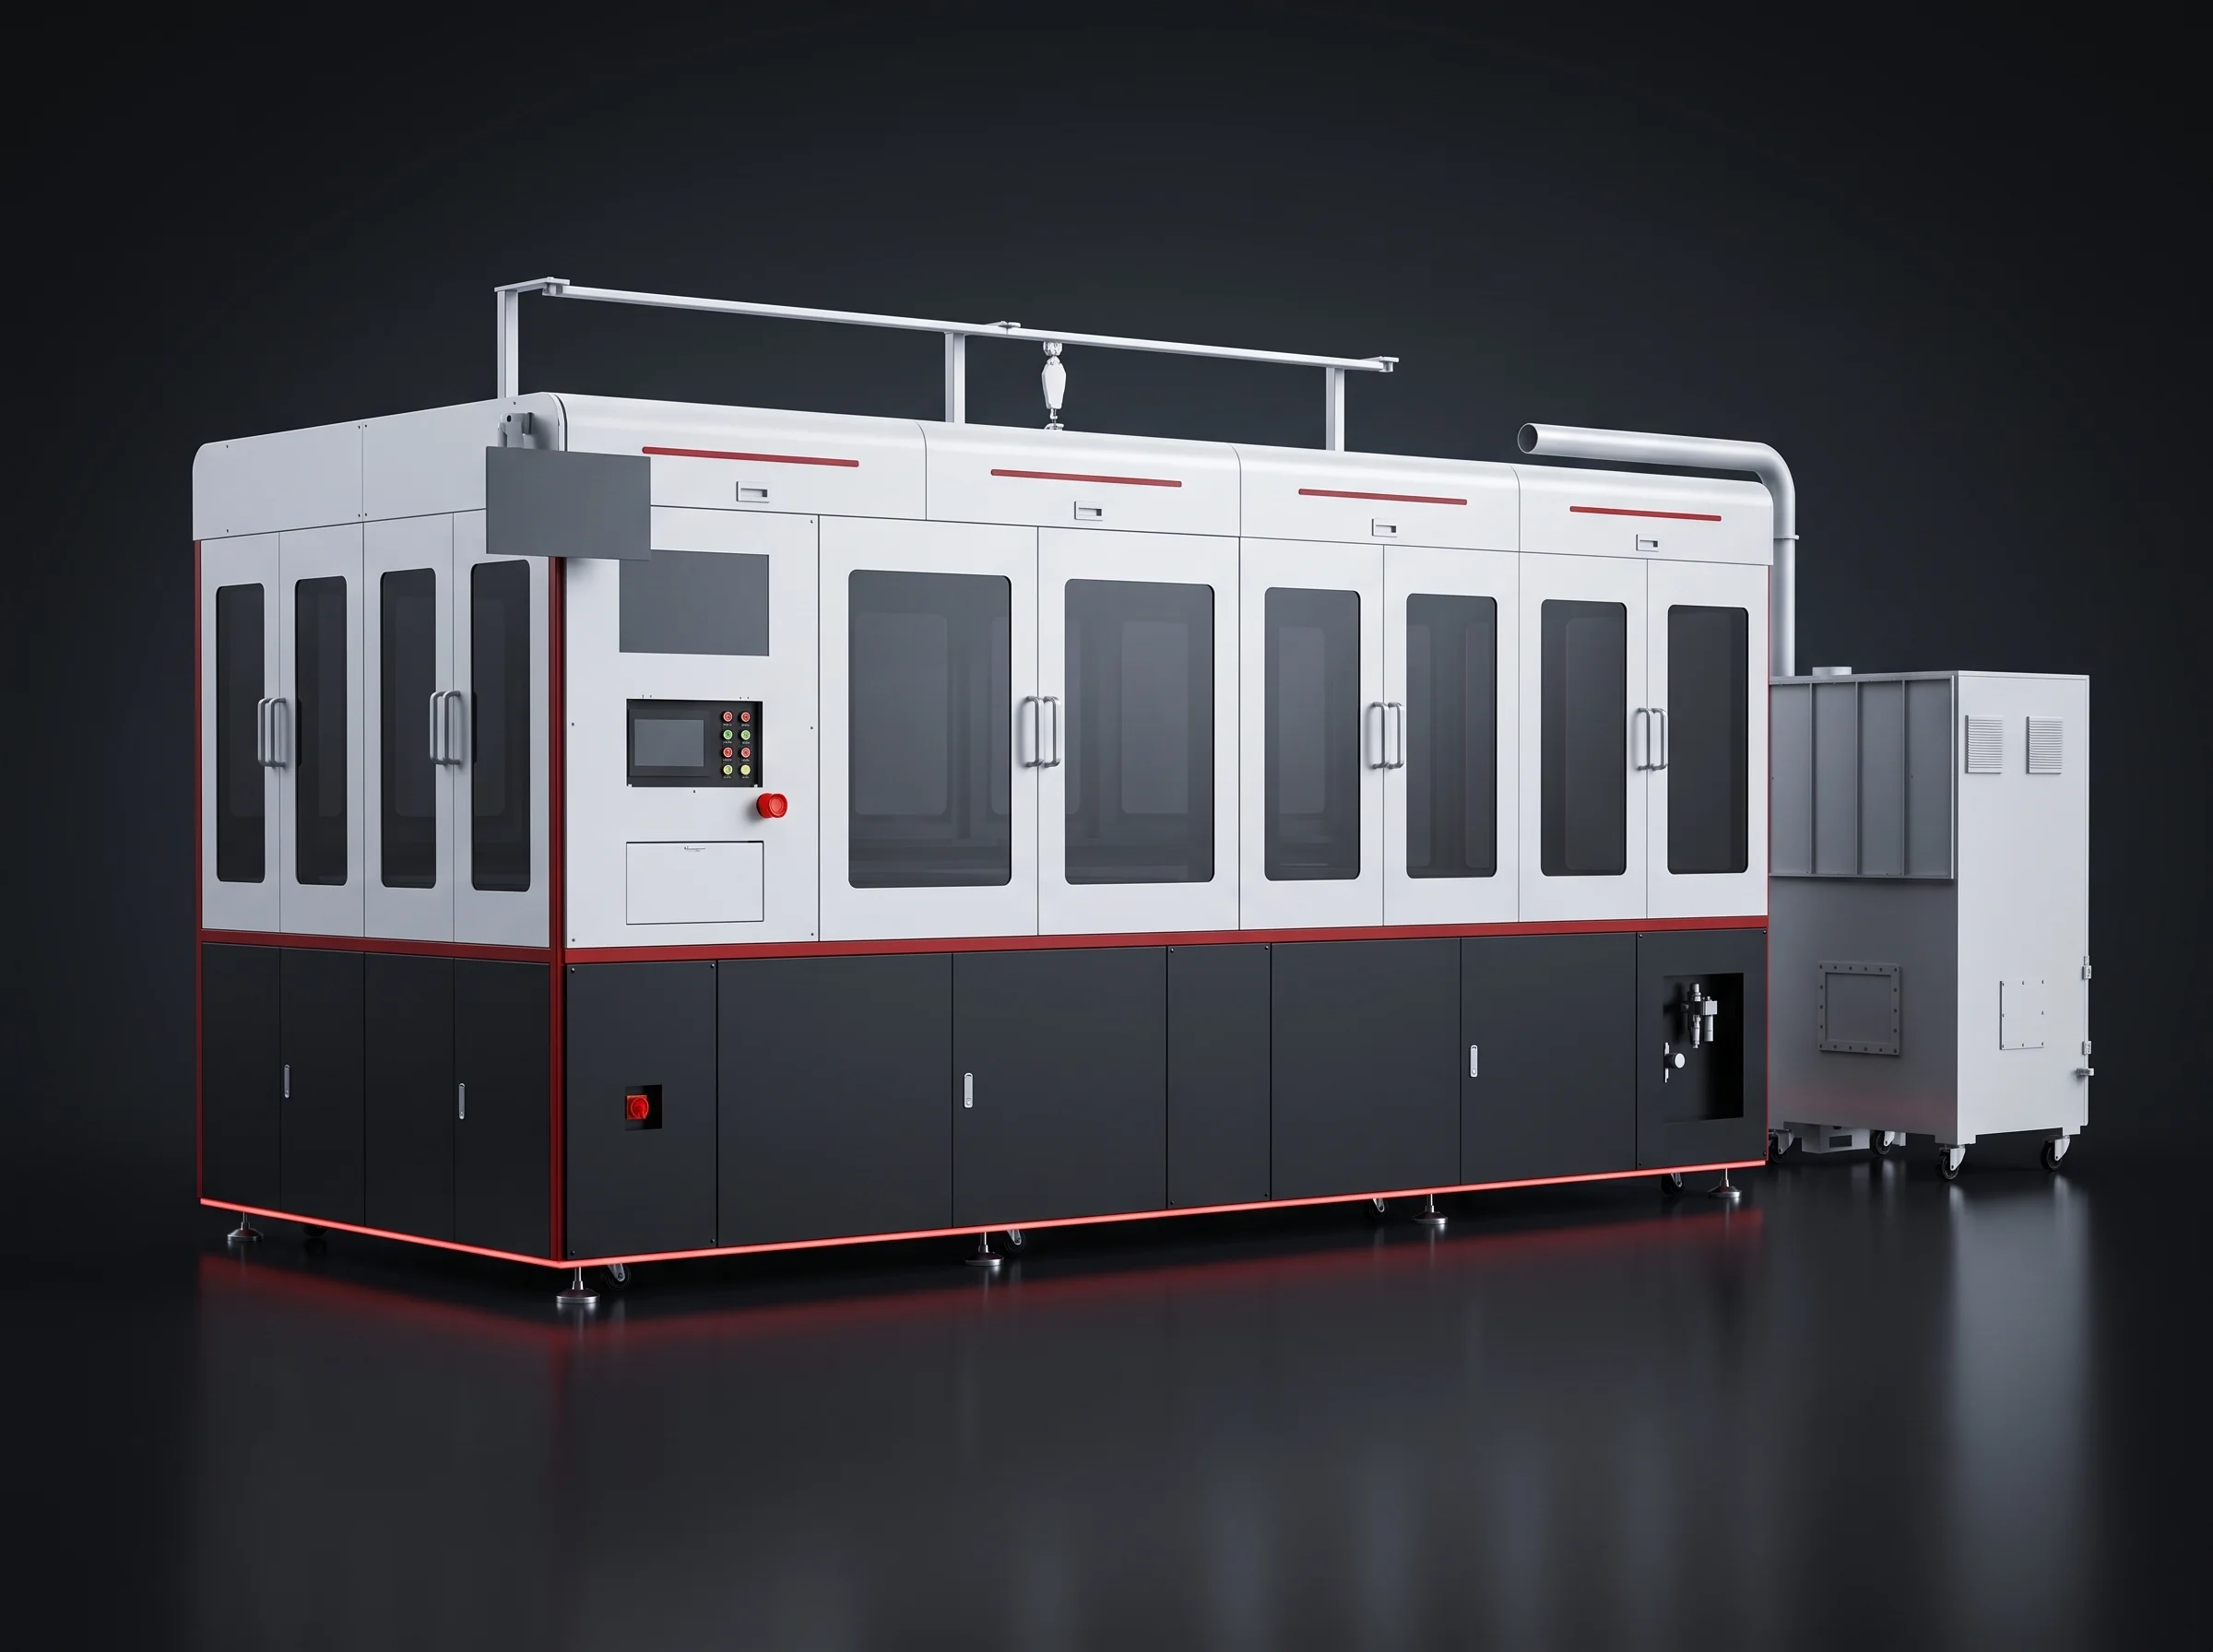
  • ≥200 kgLoad
  • ≤20 m/minSpeed
Full datasheet
BLP-WG four-axis off-line gantry laser welder standing beside the line
BLP-WGOff the takt

Off-line gantry welding

A four-axis gantry beside the line, where a new weld recipe is created and pull tested on samples.

  • ±0.01 mmRepeat positioning
  • 4–6 PPMReference part
Full datasheet

The rest are handling, cleaning, taping, fastening and inspection positions supplied with the line. Both sequences are walked station by station, with the automation label on each, on the module line and pack line pages.

17 module stations 15 pack stations 9 designed here

Station counts, module and pack.

  • 17Module stations
  • 15Pack stations
  • 9Designed in house
  • 9Branch machines
  • 3Takt tiers

Module 01–03

Cell Unloading, Testing And Sorting

The first three stations decide what the rest of the line works with. A group that reaches stacking complete but mixed passes every station after it and is still a bad module.

BLP-ULModule 01

Unloading, and the tray stack nobody wants to staff

A six-axis robot with 220 kg payload and 2650 mm reach picks five cells at a time to ±0.06 mm. Vision checks post orientation; a cell facing the wrong way never reaches sorting. Empty trays stack automatically and alarm out at twenty layers.

BLP-CSModule 02–03

Measured, graded, refilled from the buffer

Voltage is measured to ±(0.01%rdg + 3dgt) and resistance to ±(0.5%rdg + 10dgt), and each cell falls into one of up to ten settable grades. Cells outside the window are ejected and the gap refilled from a 60-cell buffer, same grade.

Barcode, voltage, resistance, grade and refill go to your MES by cell number. The grading window comes off your datasheet and grouping rules, signed by both sides before shipment.
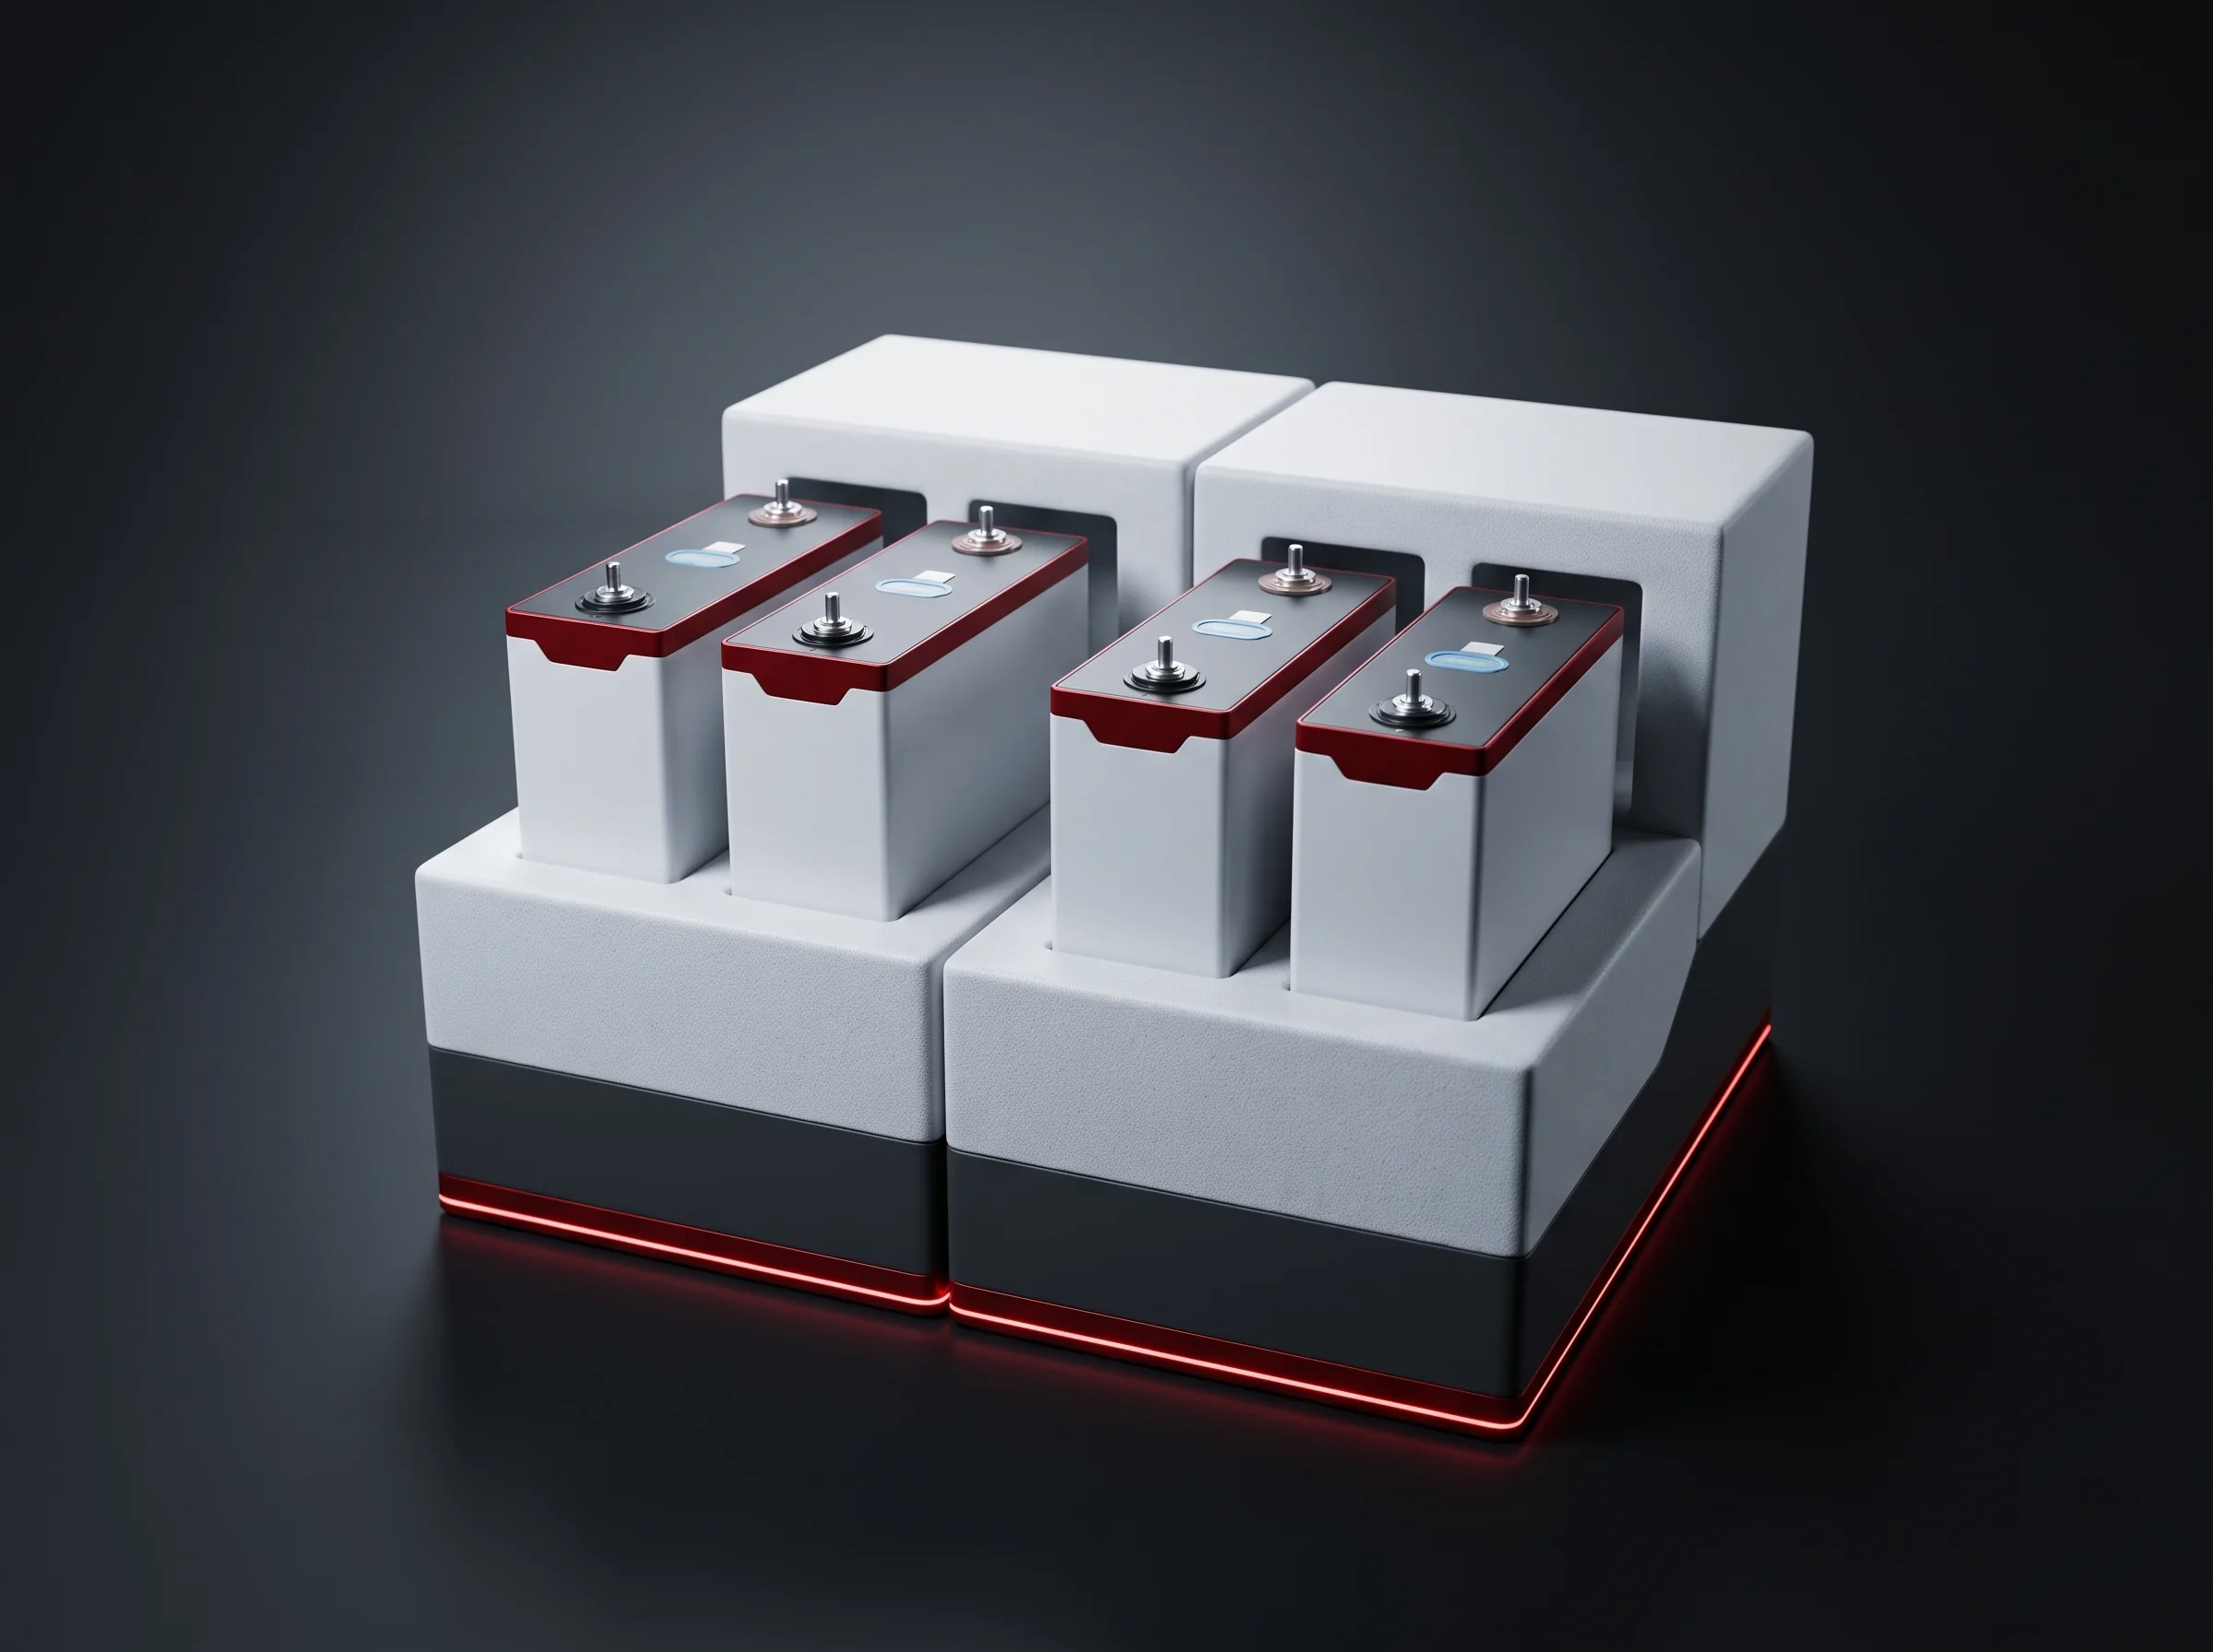
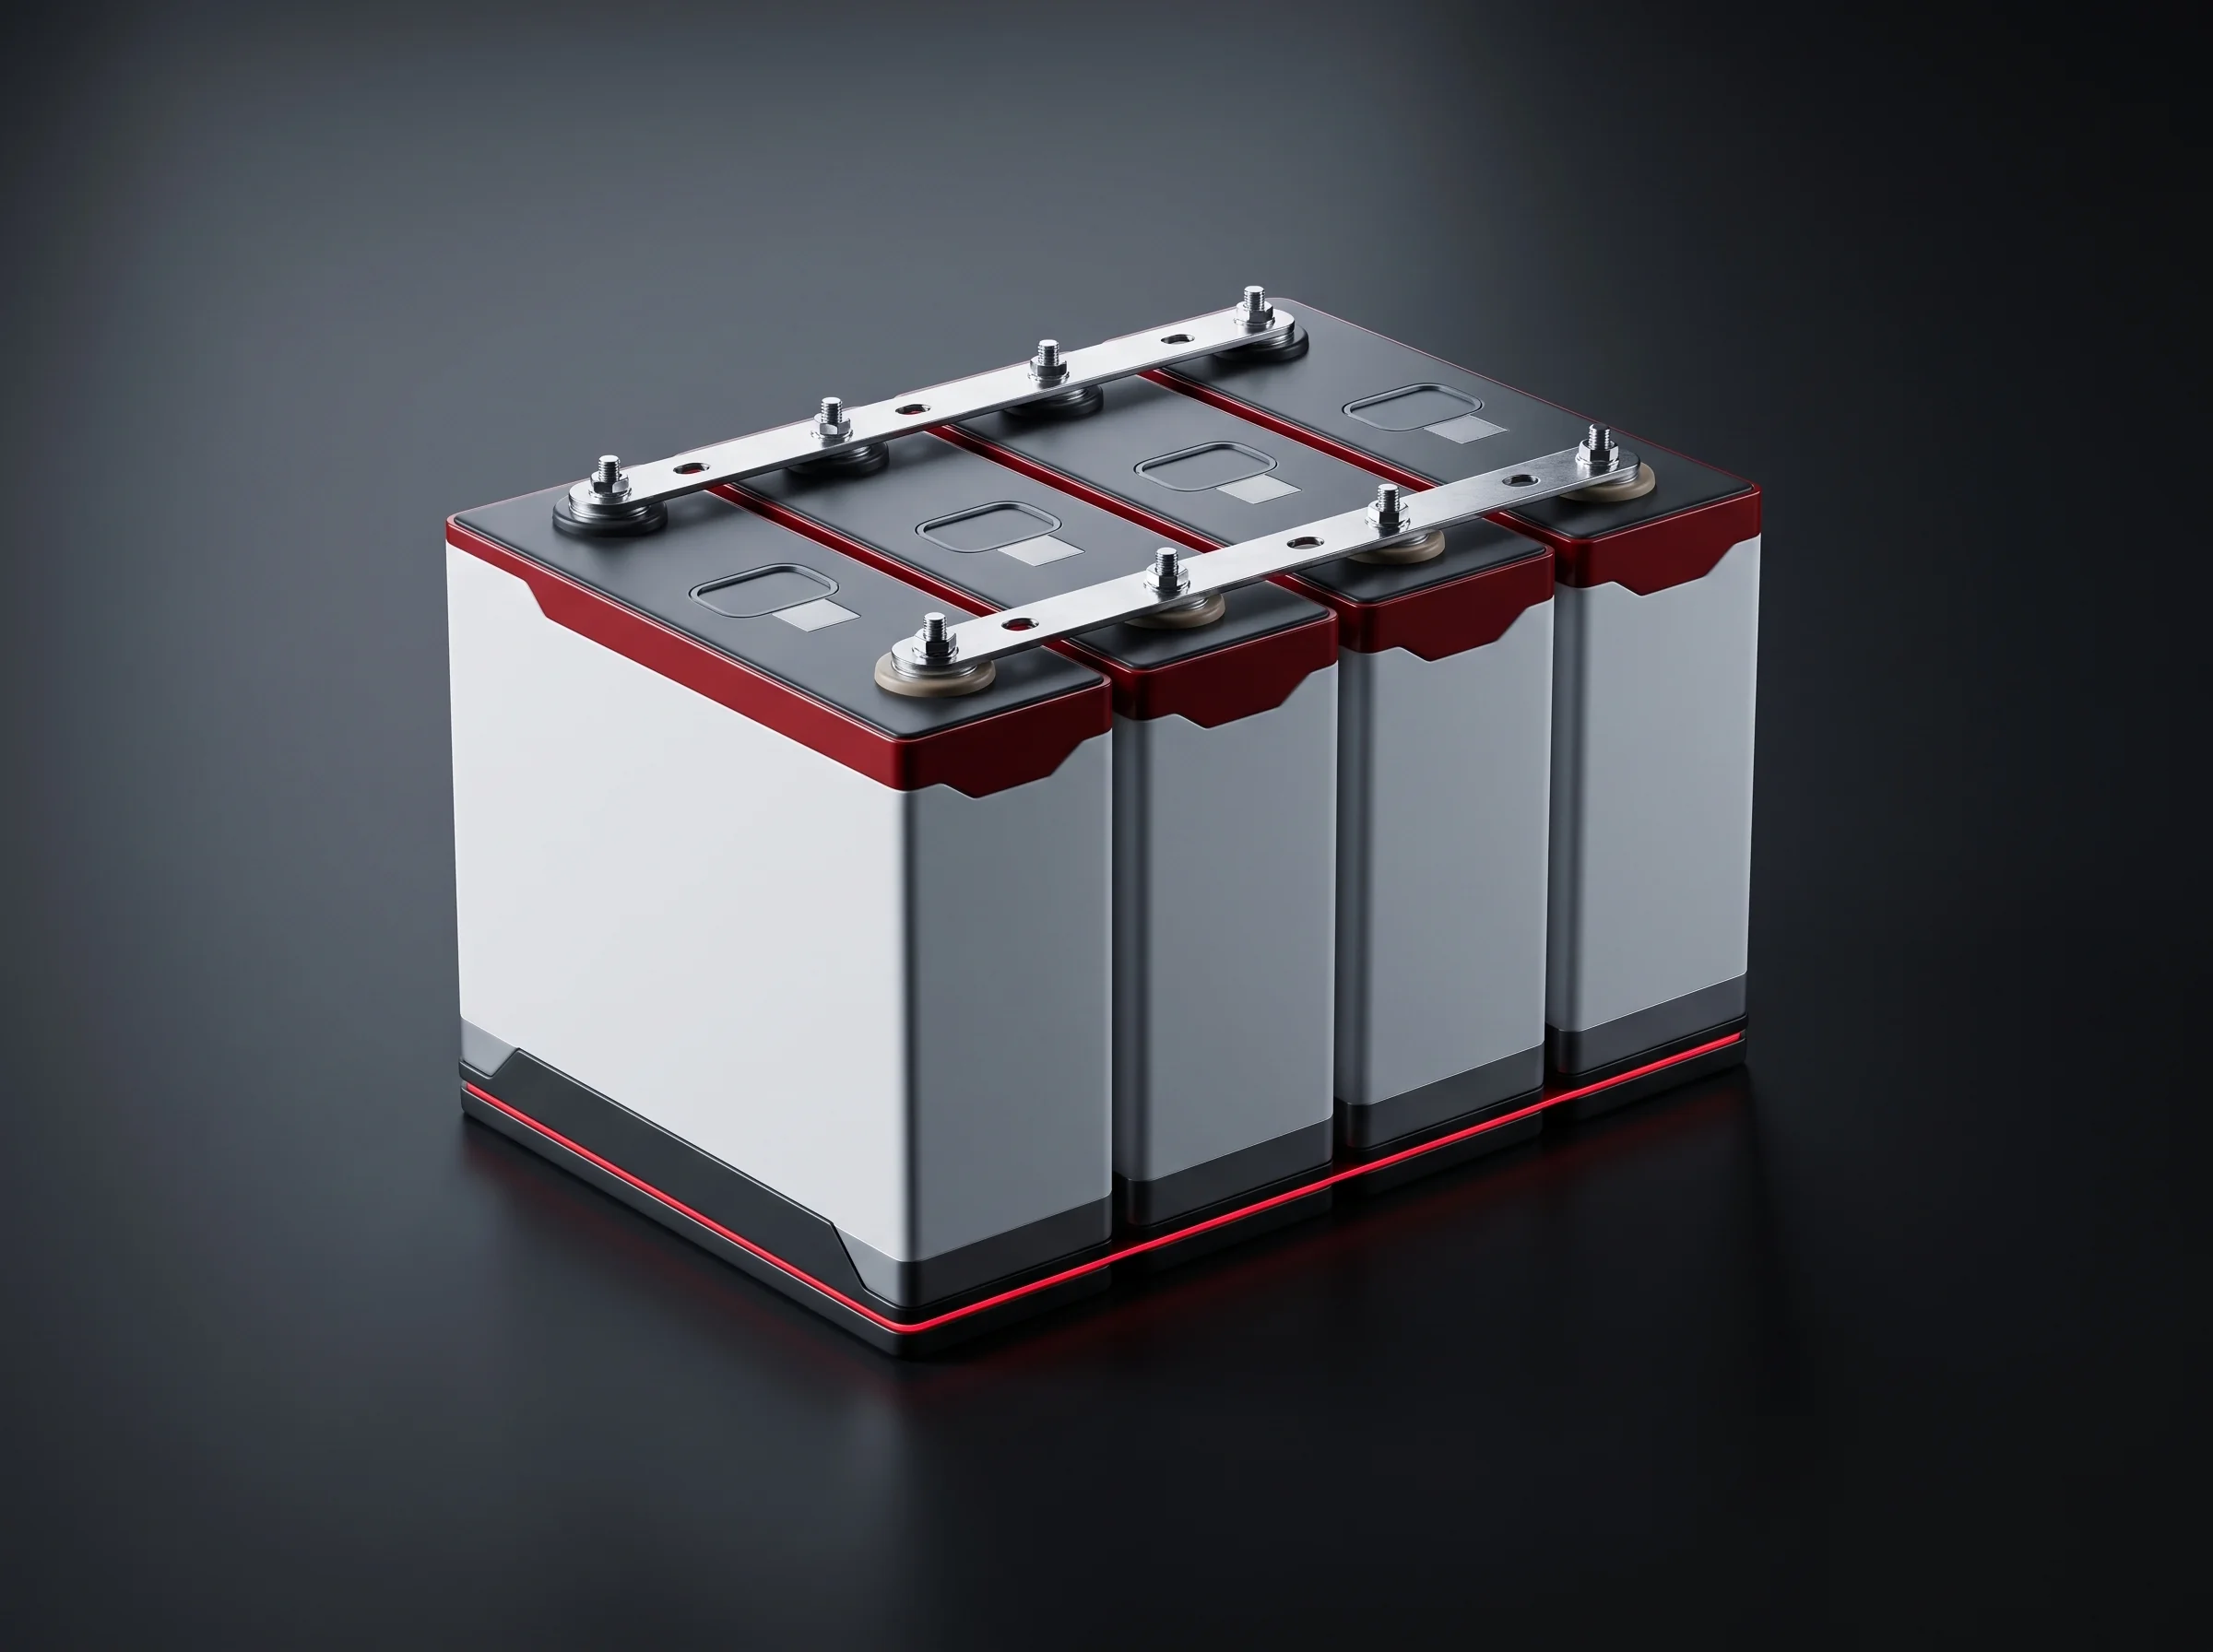
Prismatic cells arriving in foam trays at the unloading station
Five cells per pick.
Graded prismatic cells set out after open-circuit voltage and resistance sorting
Grading by voltage and resistance.
MeasuredAccuracy
Barcode99.9% or better
Open-circuit voltage±(0.01%rdg + 3dgt)
Internal resistance±(0.5%rdg + 10dgt)
Post orientationVision, pre-sorting

Module 08–09

Stacking, Pressing And Banding

BLP-SP takes a stack of 8 to 24 cells with end plates and sheets already placed, closes it, holds it, measures it and bands it — then writes one curve per module.

1 kHz, whole pressForce, platen position and time sampled through approach, dwell and release.
ParameterFigure
Press force0–8000 N servo, 10 N resolution
Dwell0–60 s by recipe
Post-press measurement±0.1 mm
Module length tolerance±0.5 mm
Pressing span300–1100 mm
Cycle, blueprint 1P13S≤90 s, banding included

The blueprint 1P13S module is 978.4 mm long, well inside the span. Recipes carry target force, dwell, target length and banding passes.

Two stations, two automation labels

Station 08 · Auto

Stacking of 8 to 24 cells, end plates and sheets in place.

Station 09 · Semi-auto

Press, dwell, measurement and steel banding, operator on the banding pass.

Station 09 is written as semi-automatic rather than letting “automatic” cover a position where somebody is standing.

Auto Semi-auto Manual Labelled per station

Full sequence on the module line page; the station on the stacking and pressing page.
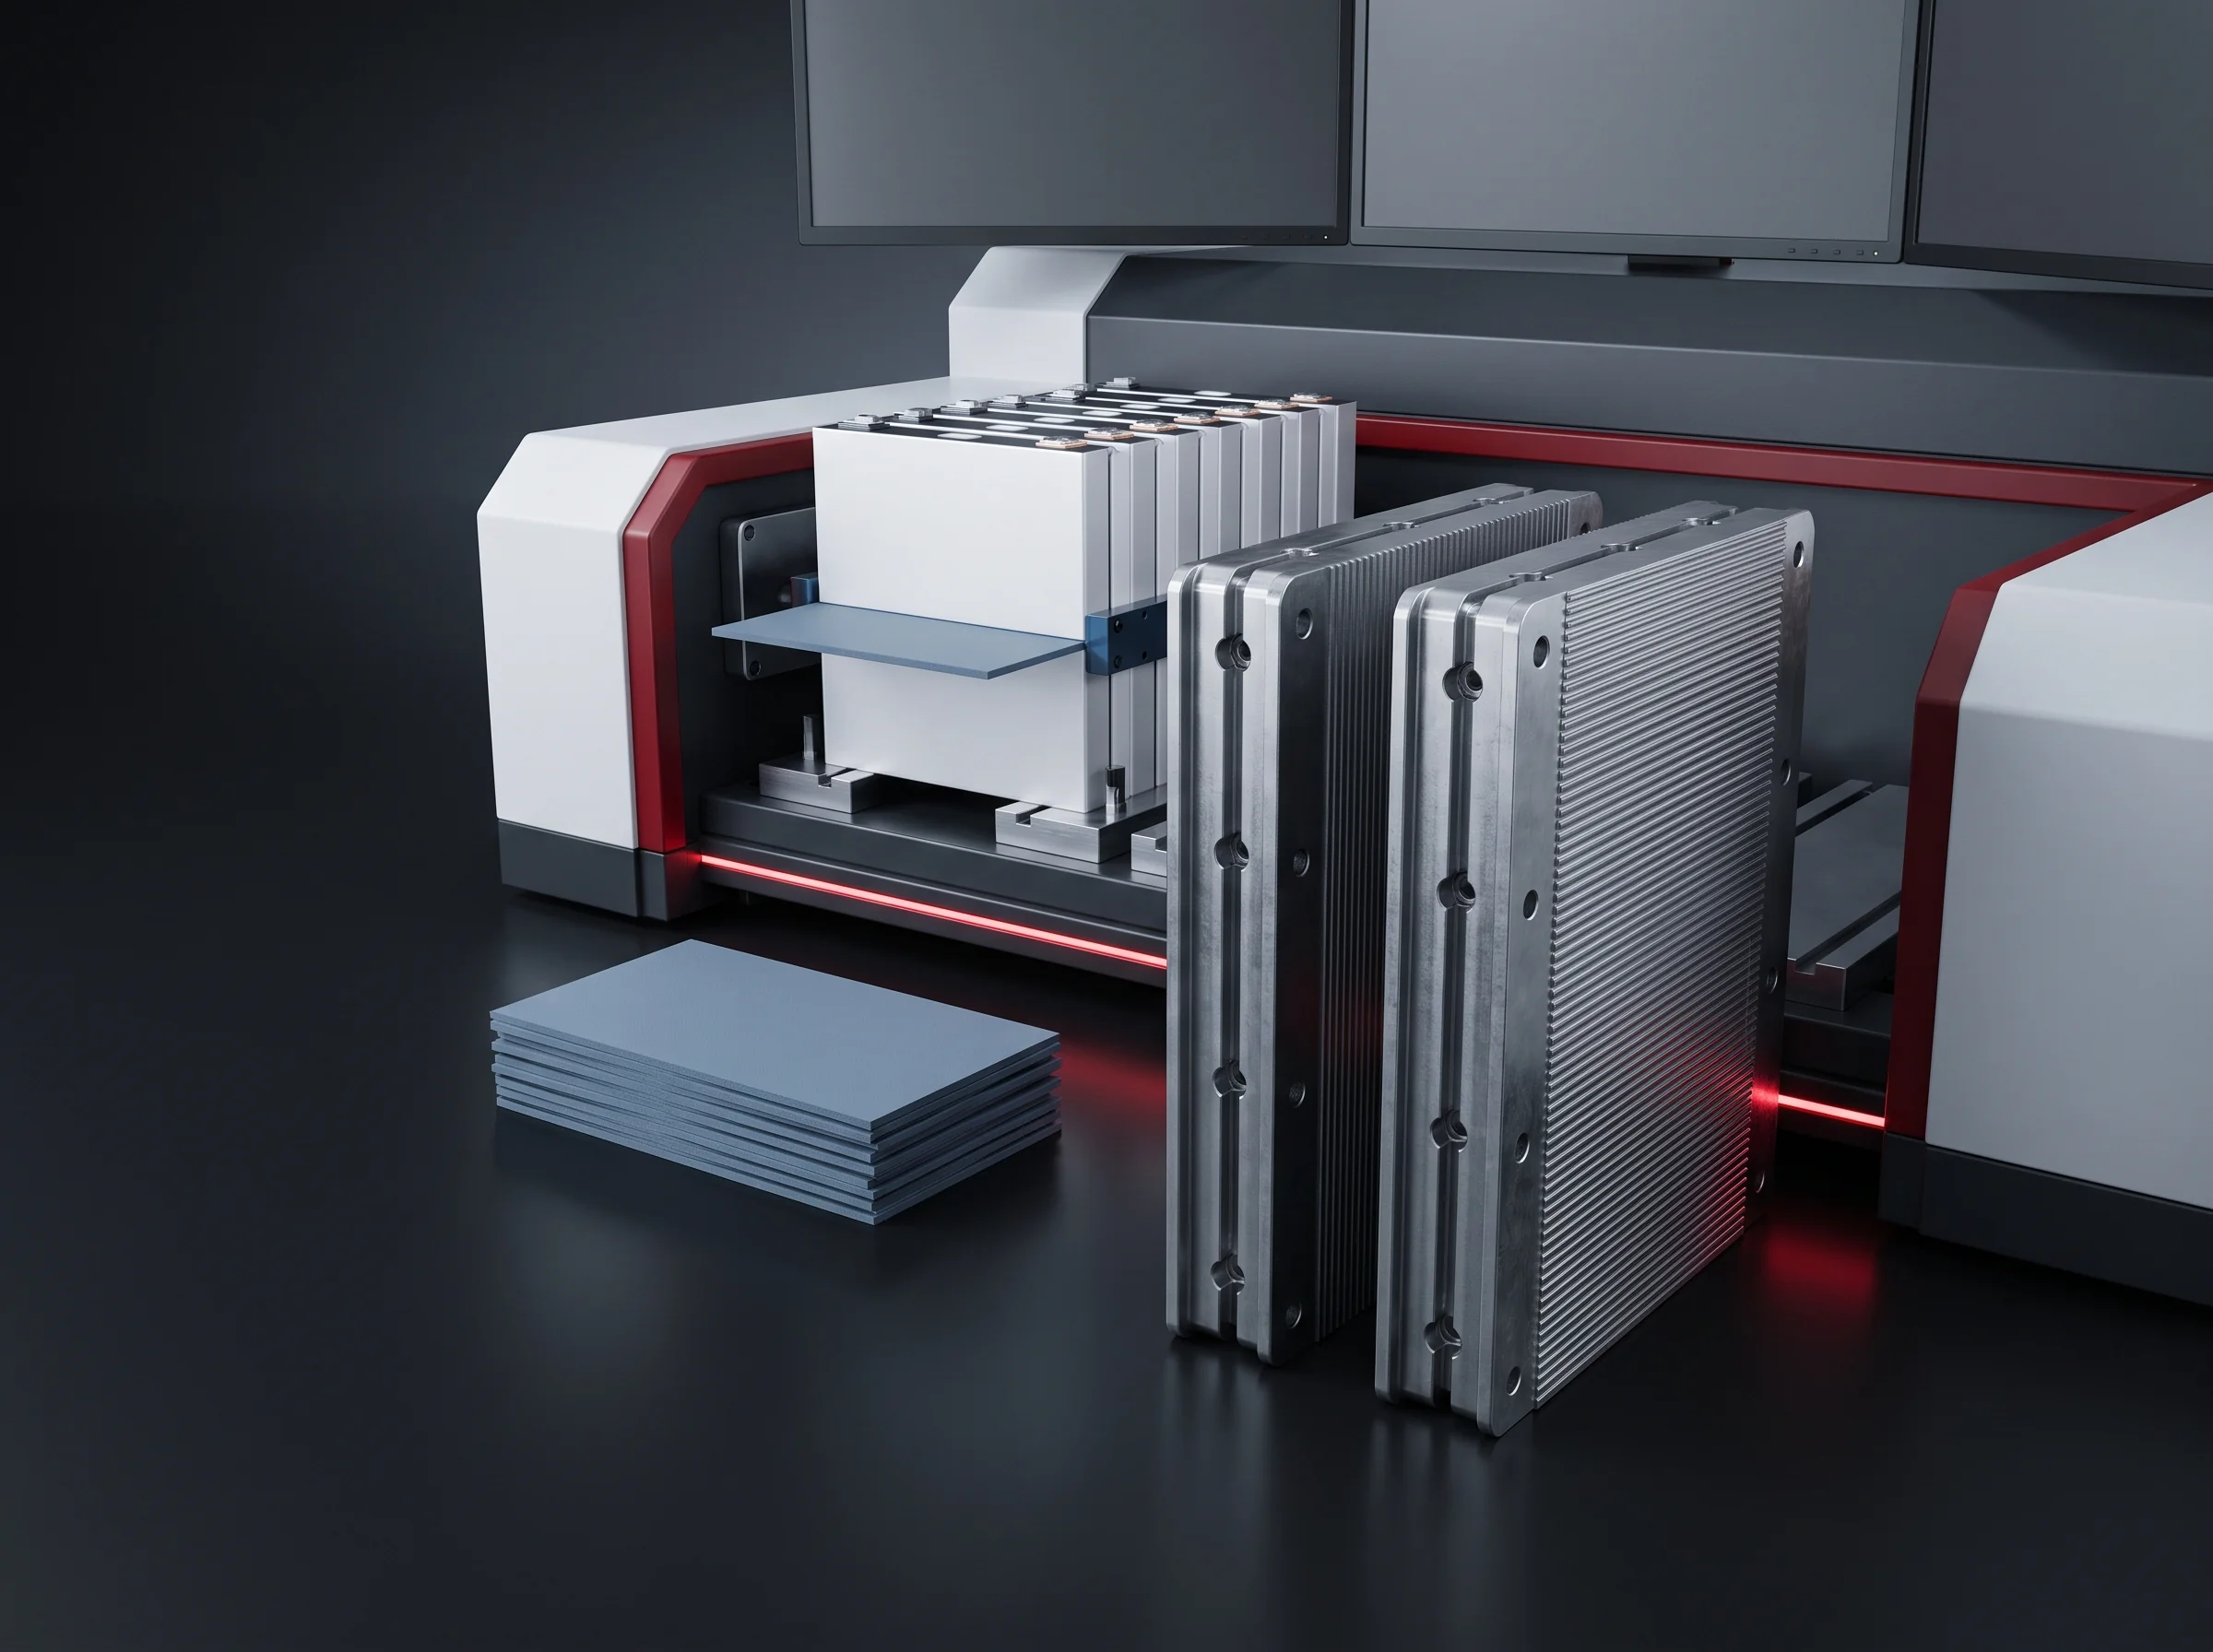
End plates and insulation sheets placed before the module reaches the press
End plates and sheets placed upstream.
Servo press platen and locating fixture closing on a prismatic cell stack
Platen and fixture, changed in about two hours.
Steel banding pass closing the pressed battery module at station 09
The banding pass — why station 09 is semi-automatic.

Module 11 → 13

Addressing And Inline Welding, One Pair

These two are quoted together more often than separately, and the reason is worth spelling out.

BLP-ADModule 11

Where every terminal actually is

One vision set finds the terminal centre and reads polarity in the same shot; a 100 W pulsed laser then cleans a 2 mm ring on the post. Three seconds or less per terminal, and the coordinates leave as a joint map.
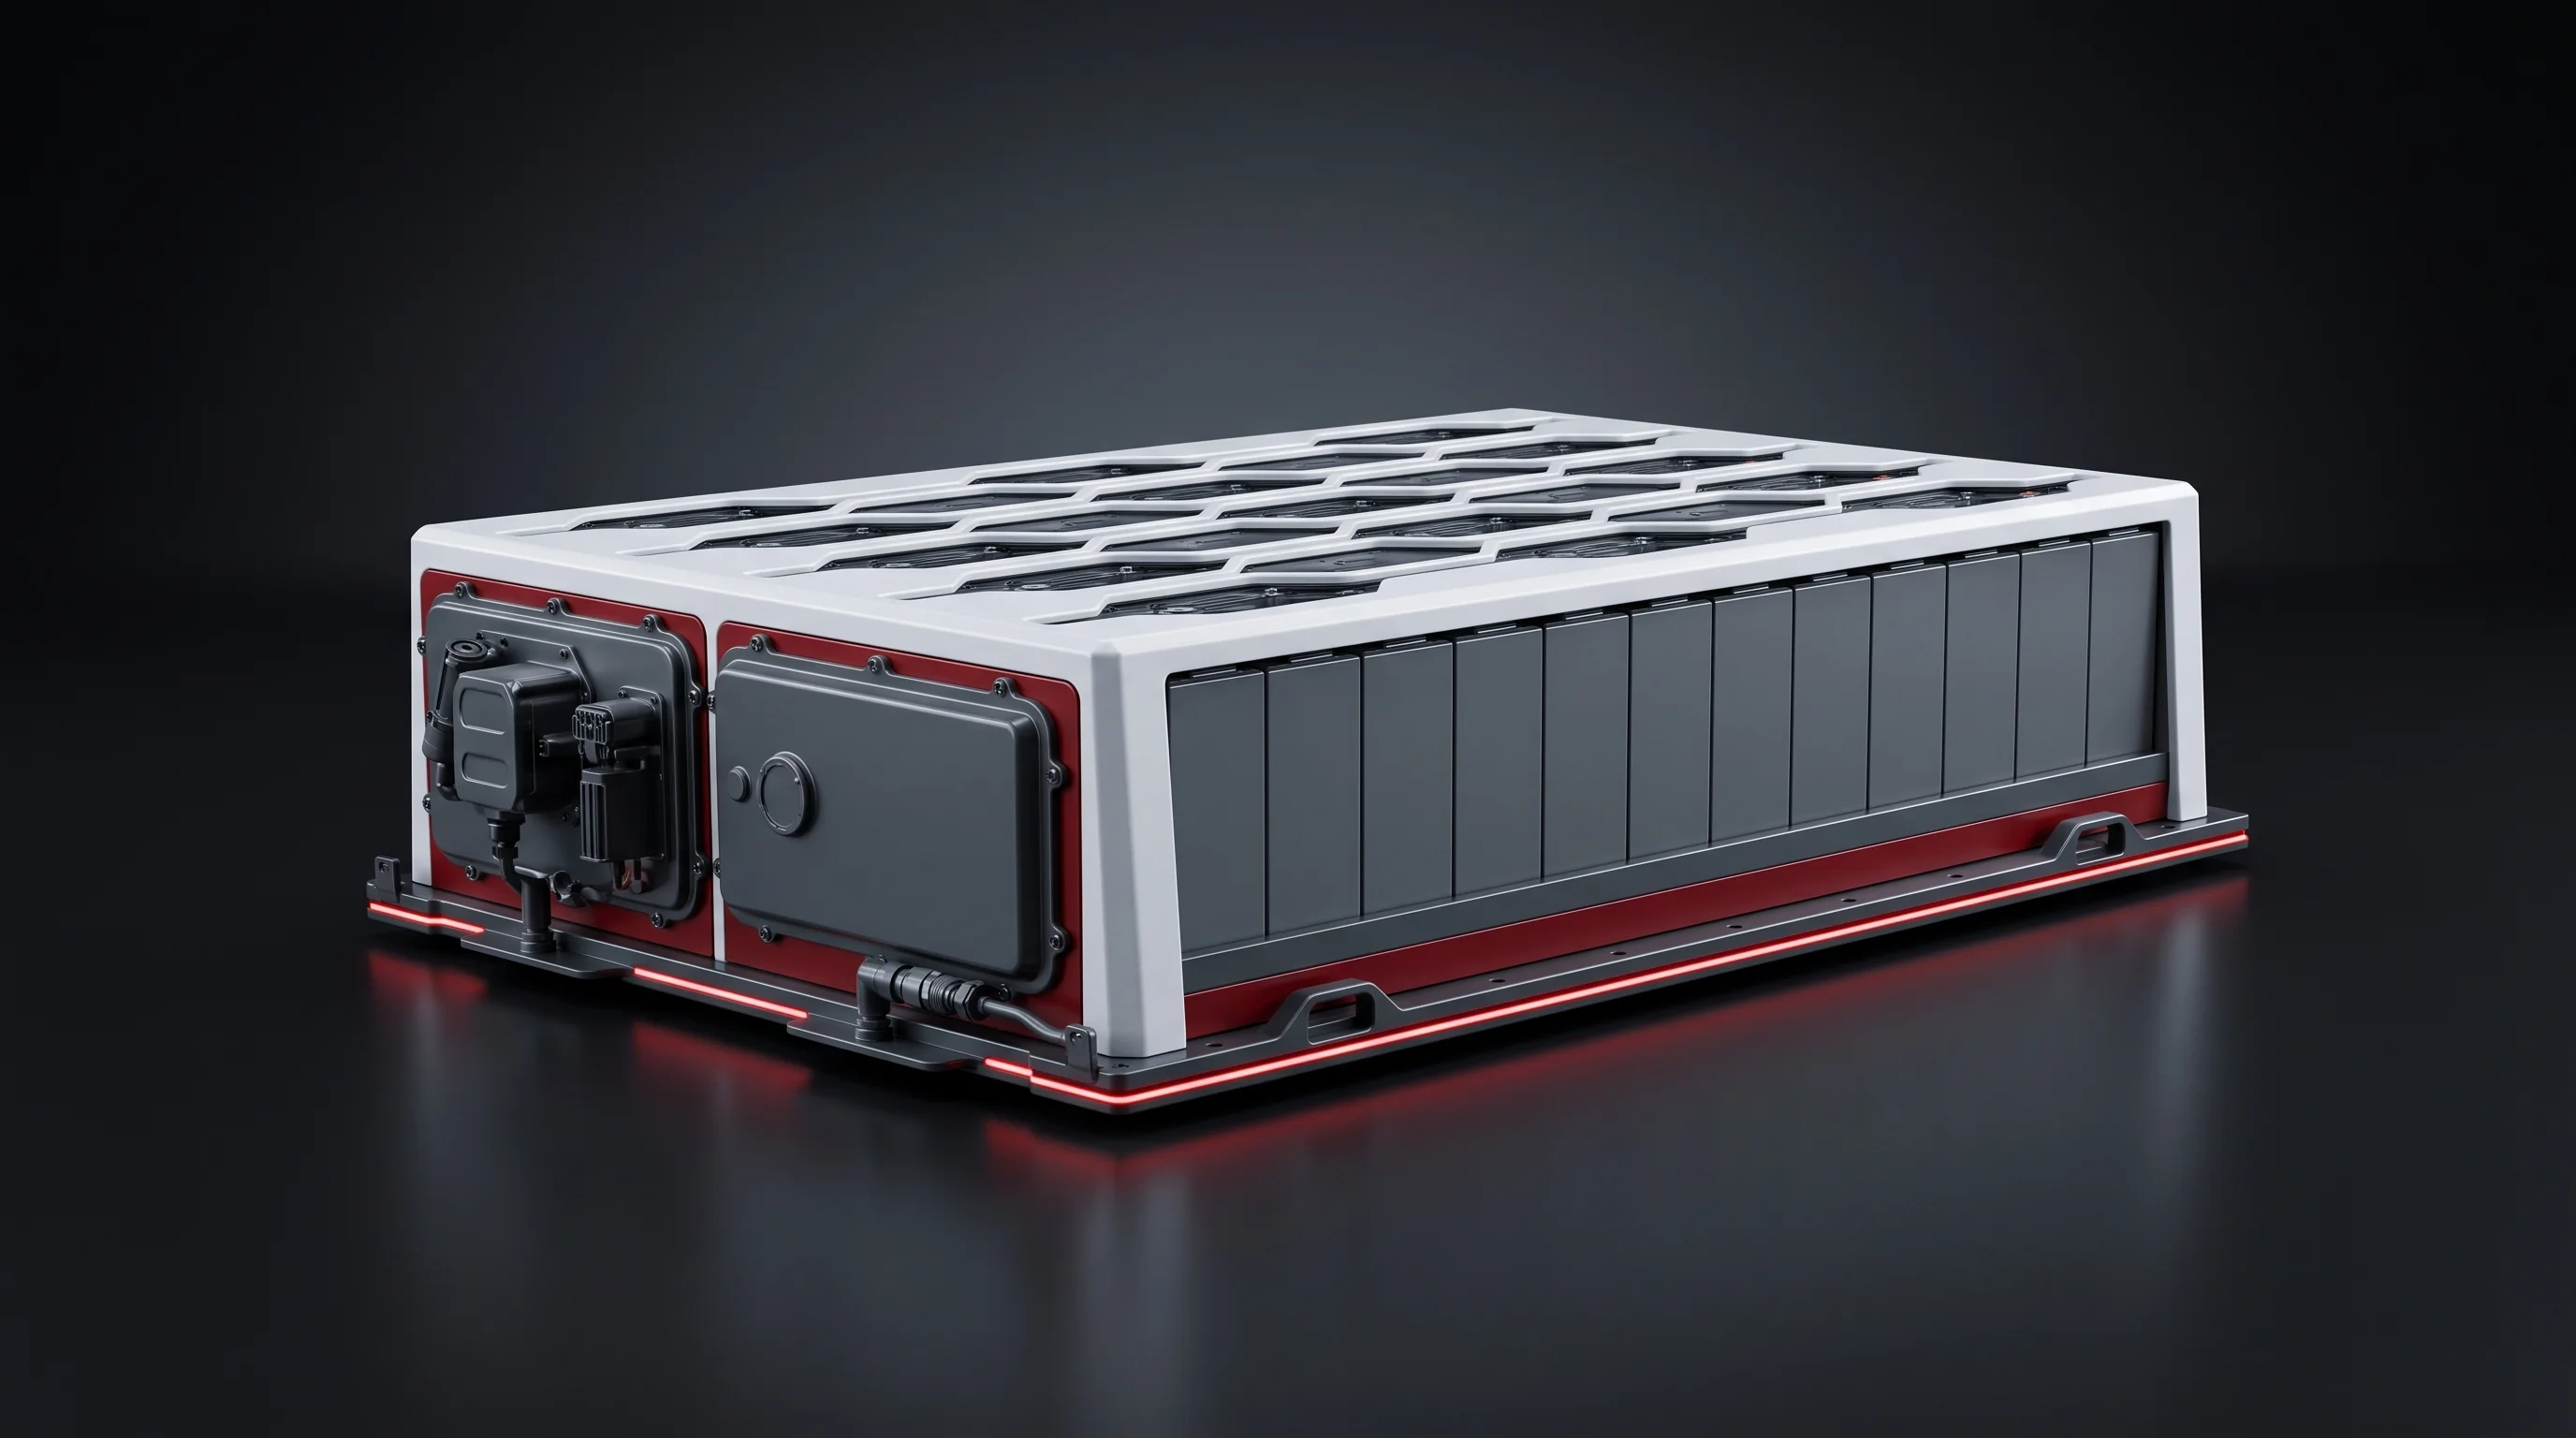
Module terminal layout of the kind addressed and mapped at station 11
  • ±0.2 mmAddressing accuracy
  • ≤4 hOpen time after cleaning
BLP-W6Module 13

What the recipe is allowed to assume

A 6 kW laser welds the busbars at 50 to 100 mm/s, to a penetration of 1.0 mm or more, a width of 1.5 mm or more and a pull force of 1000 N or more — single-row and double-row on one station.
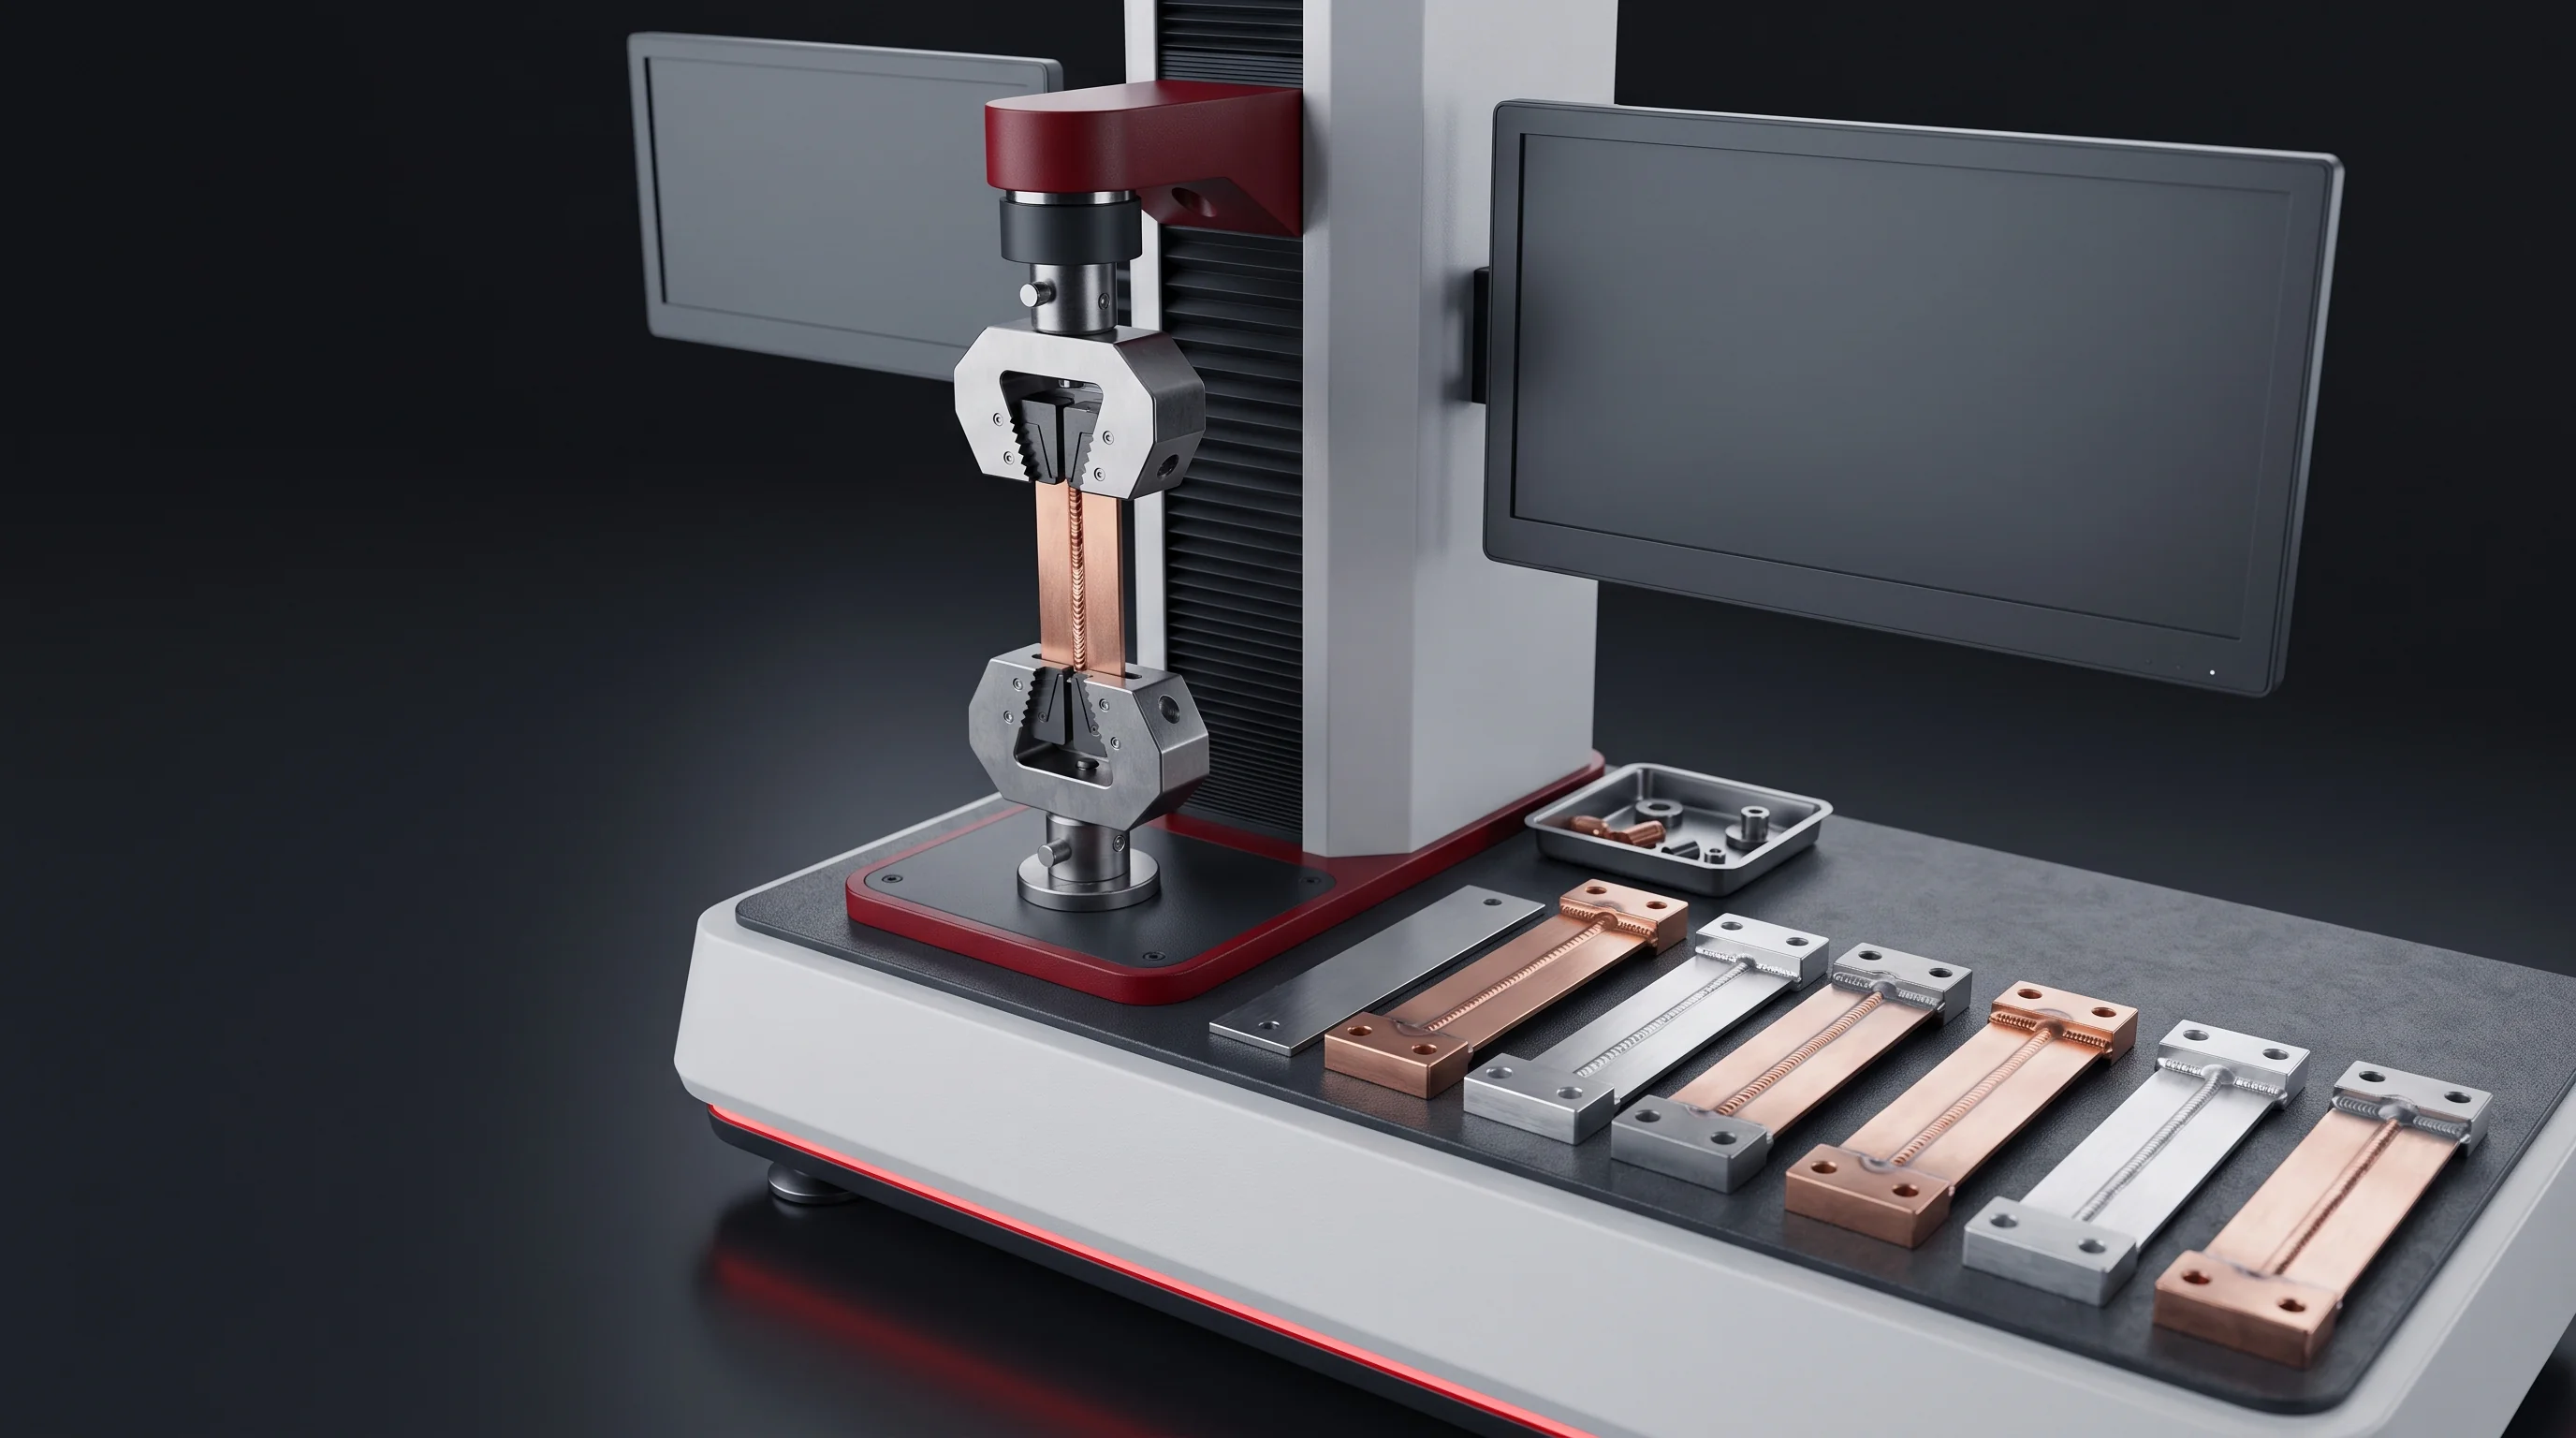
Welded sample coupons of the kind pulled to destruction against the 1000 N criterion
  • ≥1000 NJoint pull force
  • ≥1.5 mmWeld width

Why the pair holds

A recipe fixes beam power, speed and focal position against one joint geometry. If the terminal is half a millimetre from where the recipe assumes, it is running against a different joint — and the pull number stops describing what came out.

What acceptance measures

  • Addressing repeatability at station 11, against a standard module
  • Destructive pull tests on joints from station 13, against the signed criterion

What gets recorded

  • Recipe number, power, speed, defocus and nitrogen flow
  • Sequence and timestamp of every weld, by module number
  • Station 14 measures weld width on 100% of joints

Datasheets: terminal addressing and busbar welding.

Off the takt

The Off-Line Gantry Welder

A four-axis gantry laser welder standing next to the line rather than in it. Plants running our lines usually take it too; the reason is in the first card below.

±0.01 mmRepeat positioning; CCD location to the same figure available.
ParameterFigure
Wavelength1070 ±10 nm
Rated power1000 / 2000 / 4000 / 6000 W
Fibre core14 / 20 / 50 / 100 µm
Power adjustment10–100%, stability ≤3%
TravelX 800 / 1000, Y 400 / 600, Z 200 / 400 mm
Takt, reference part4–6 PPM

What the takt figure is measured on

One clamping, weld length of 600 mm or less, a module-level part with a single busbar row. For anything else we convert to a shift output against your own fixture drawing rather than publish a second headline number.
4 × 2 m footprint External chiller 5–45 °C ambient Recipes leave from here
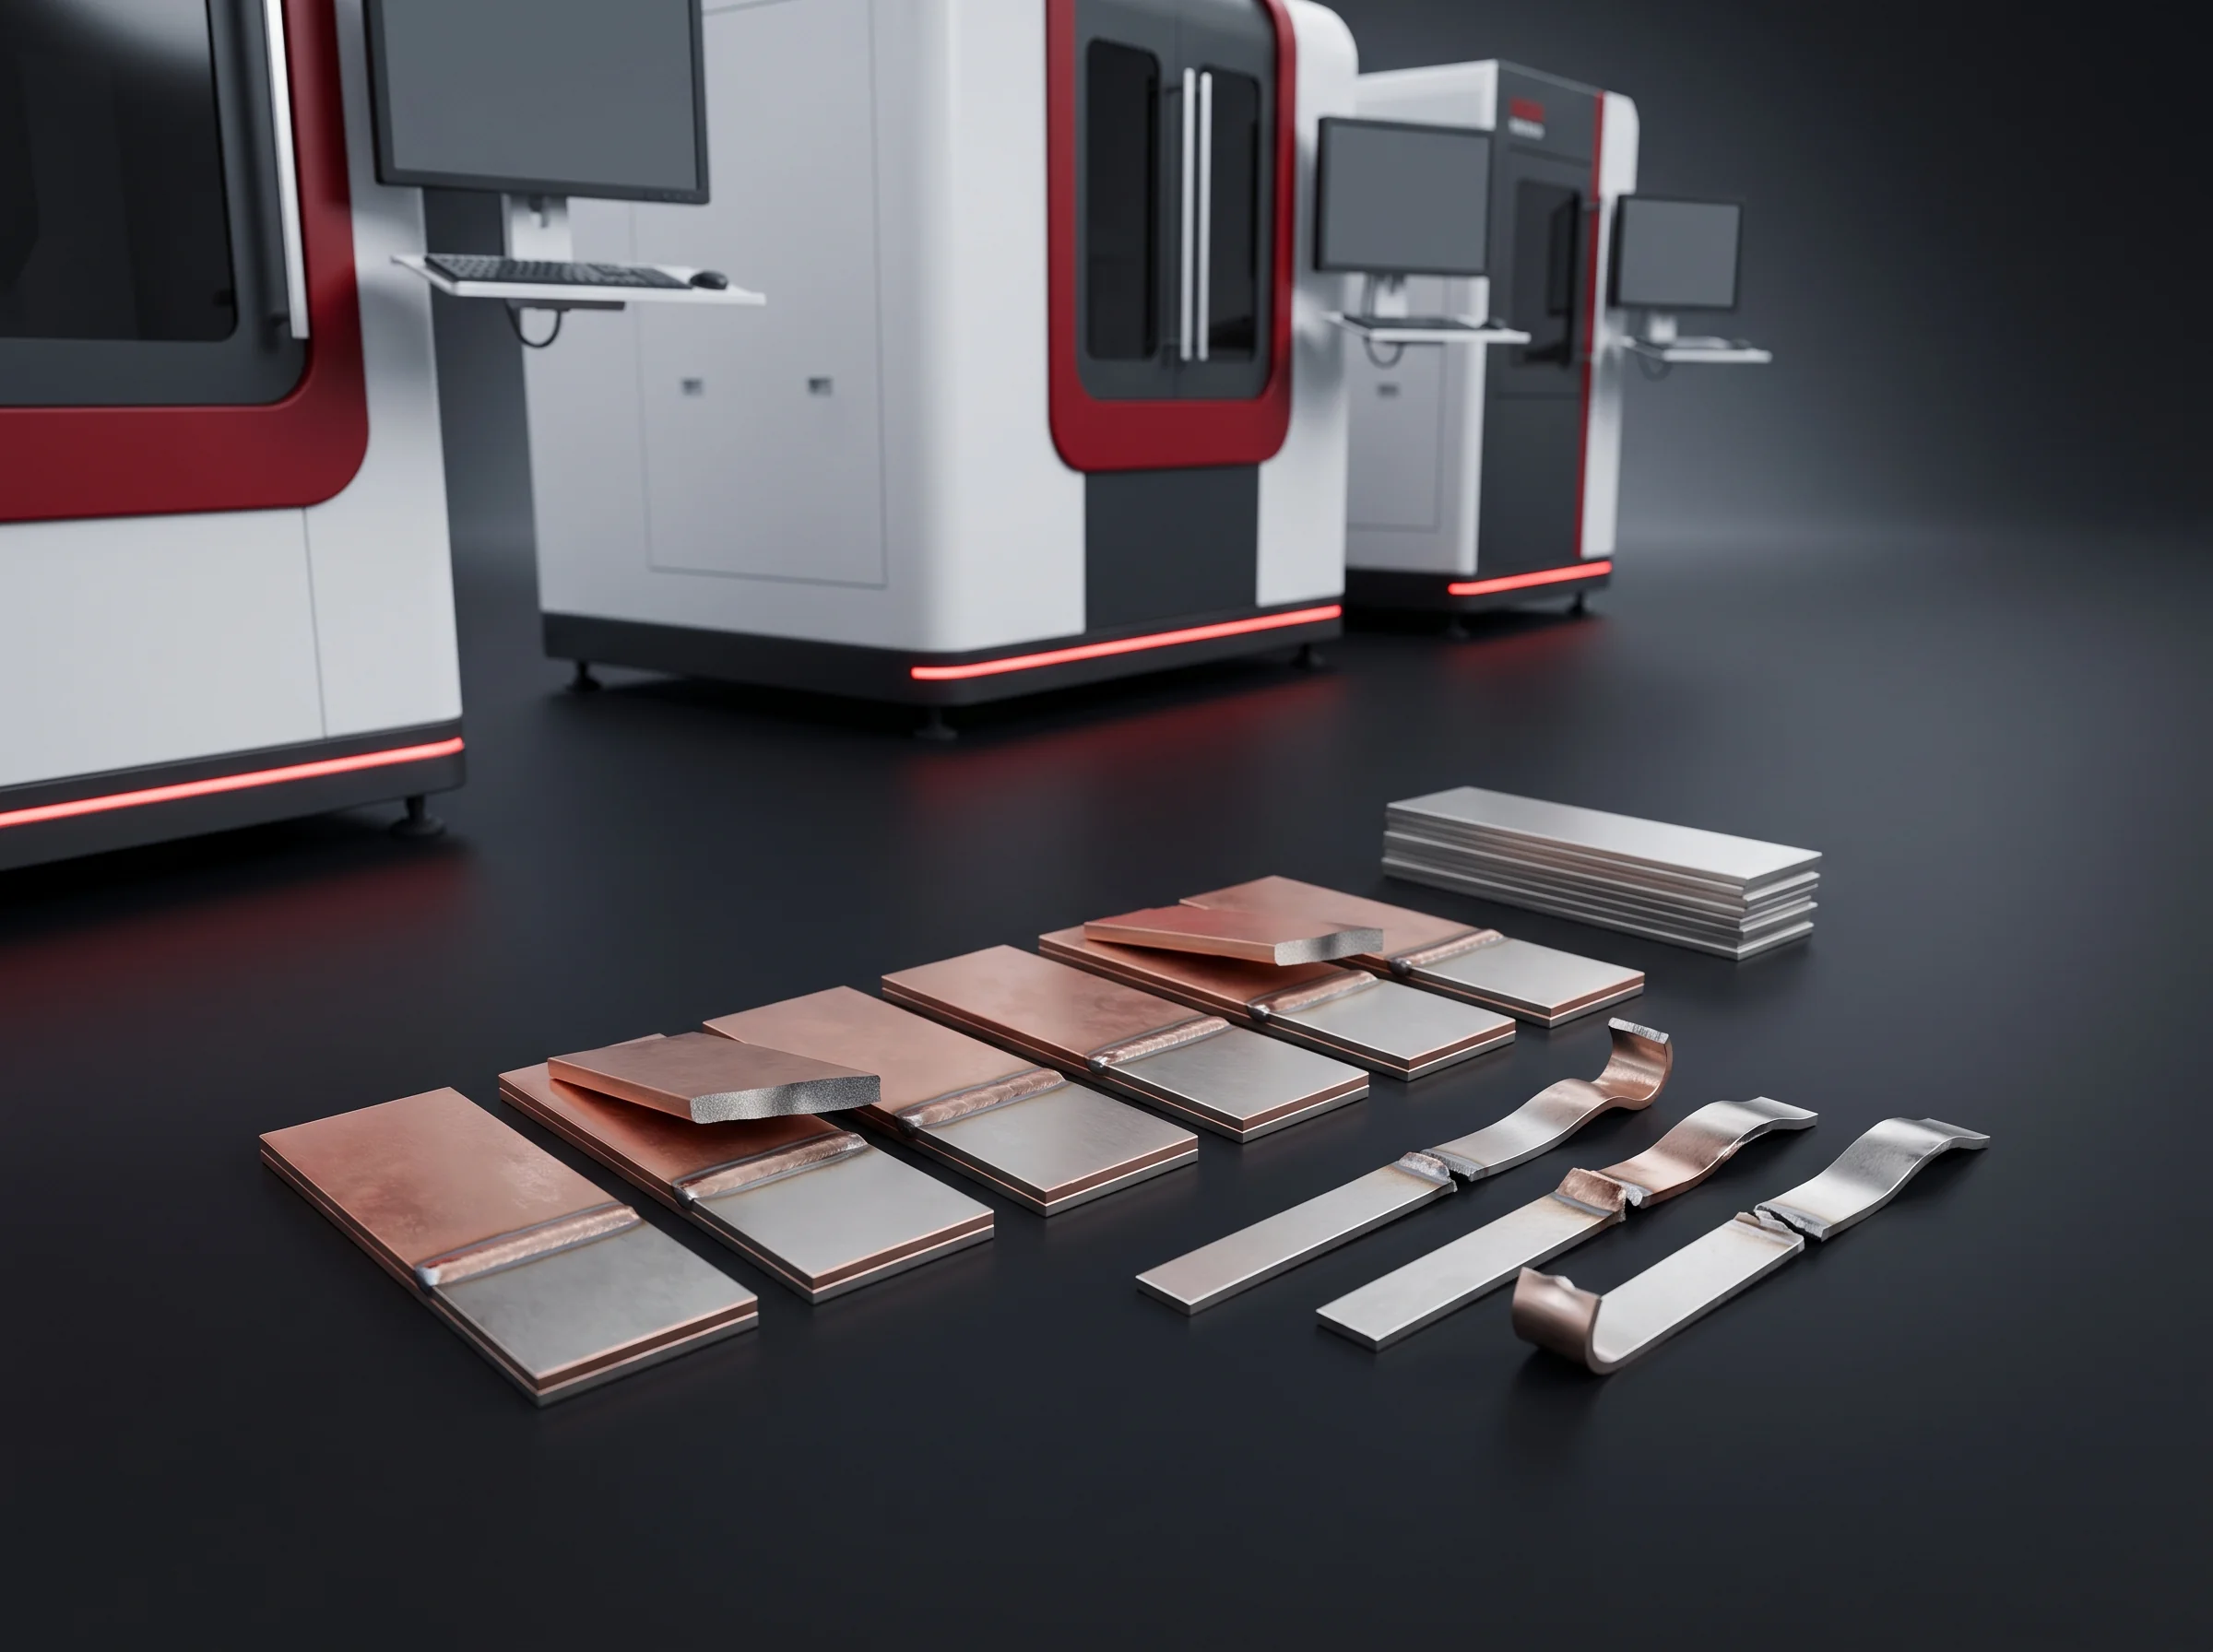
First-article sample coupons welded on the gantry before the recipe reaches the line

First articles

A new busbar recipe is created here, welded onto samples and pull tested before it goes near the takt.
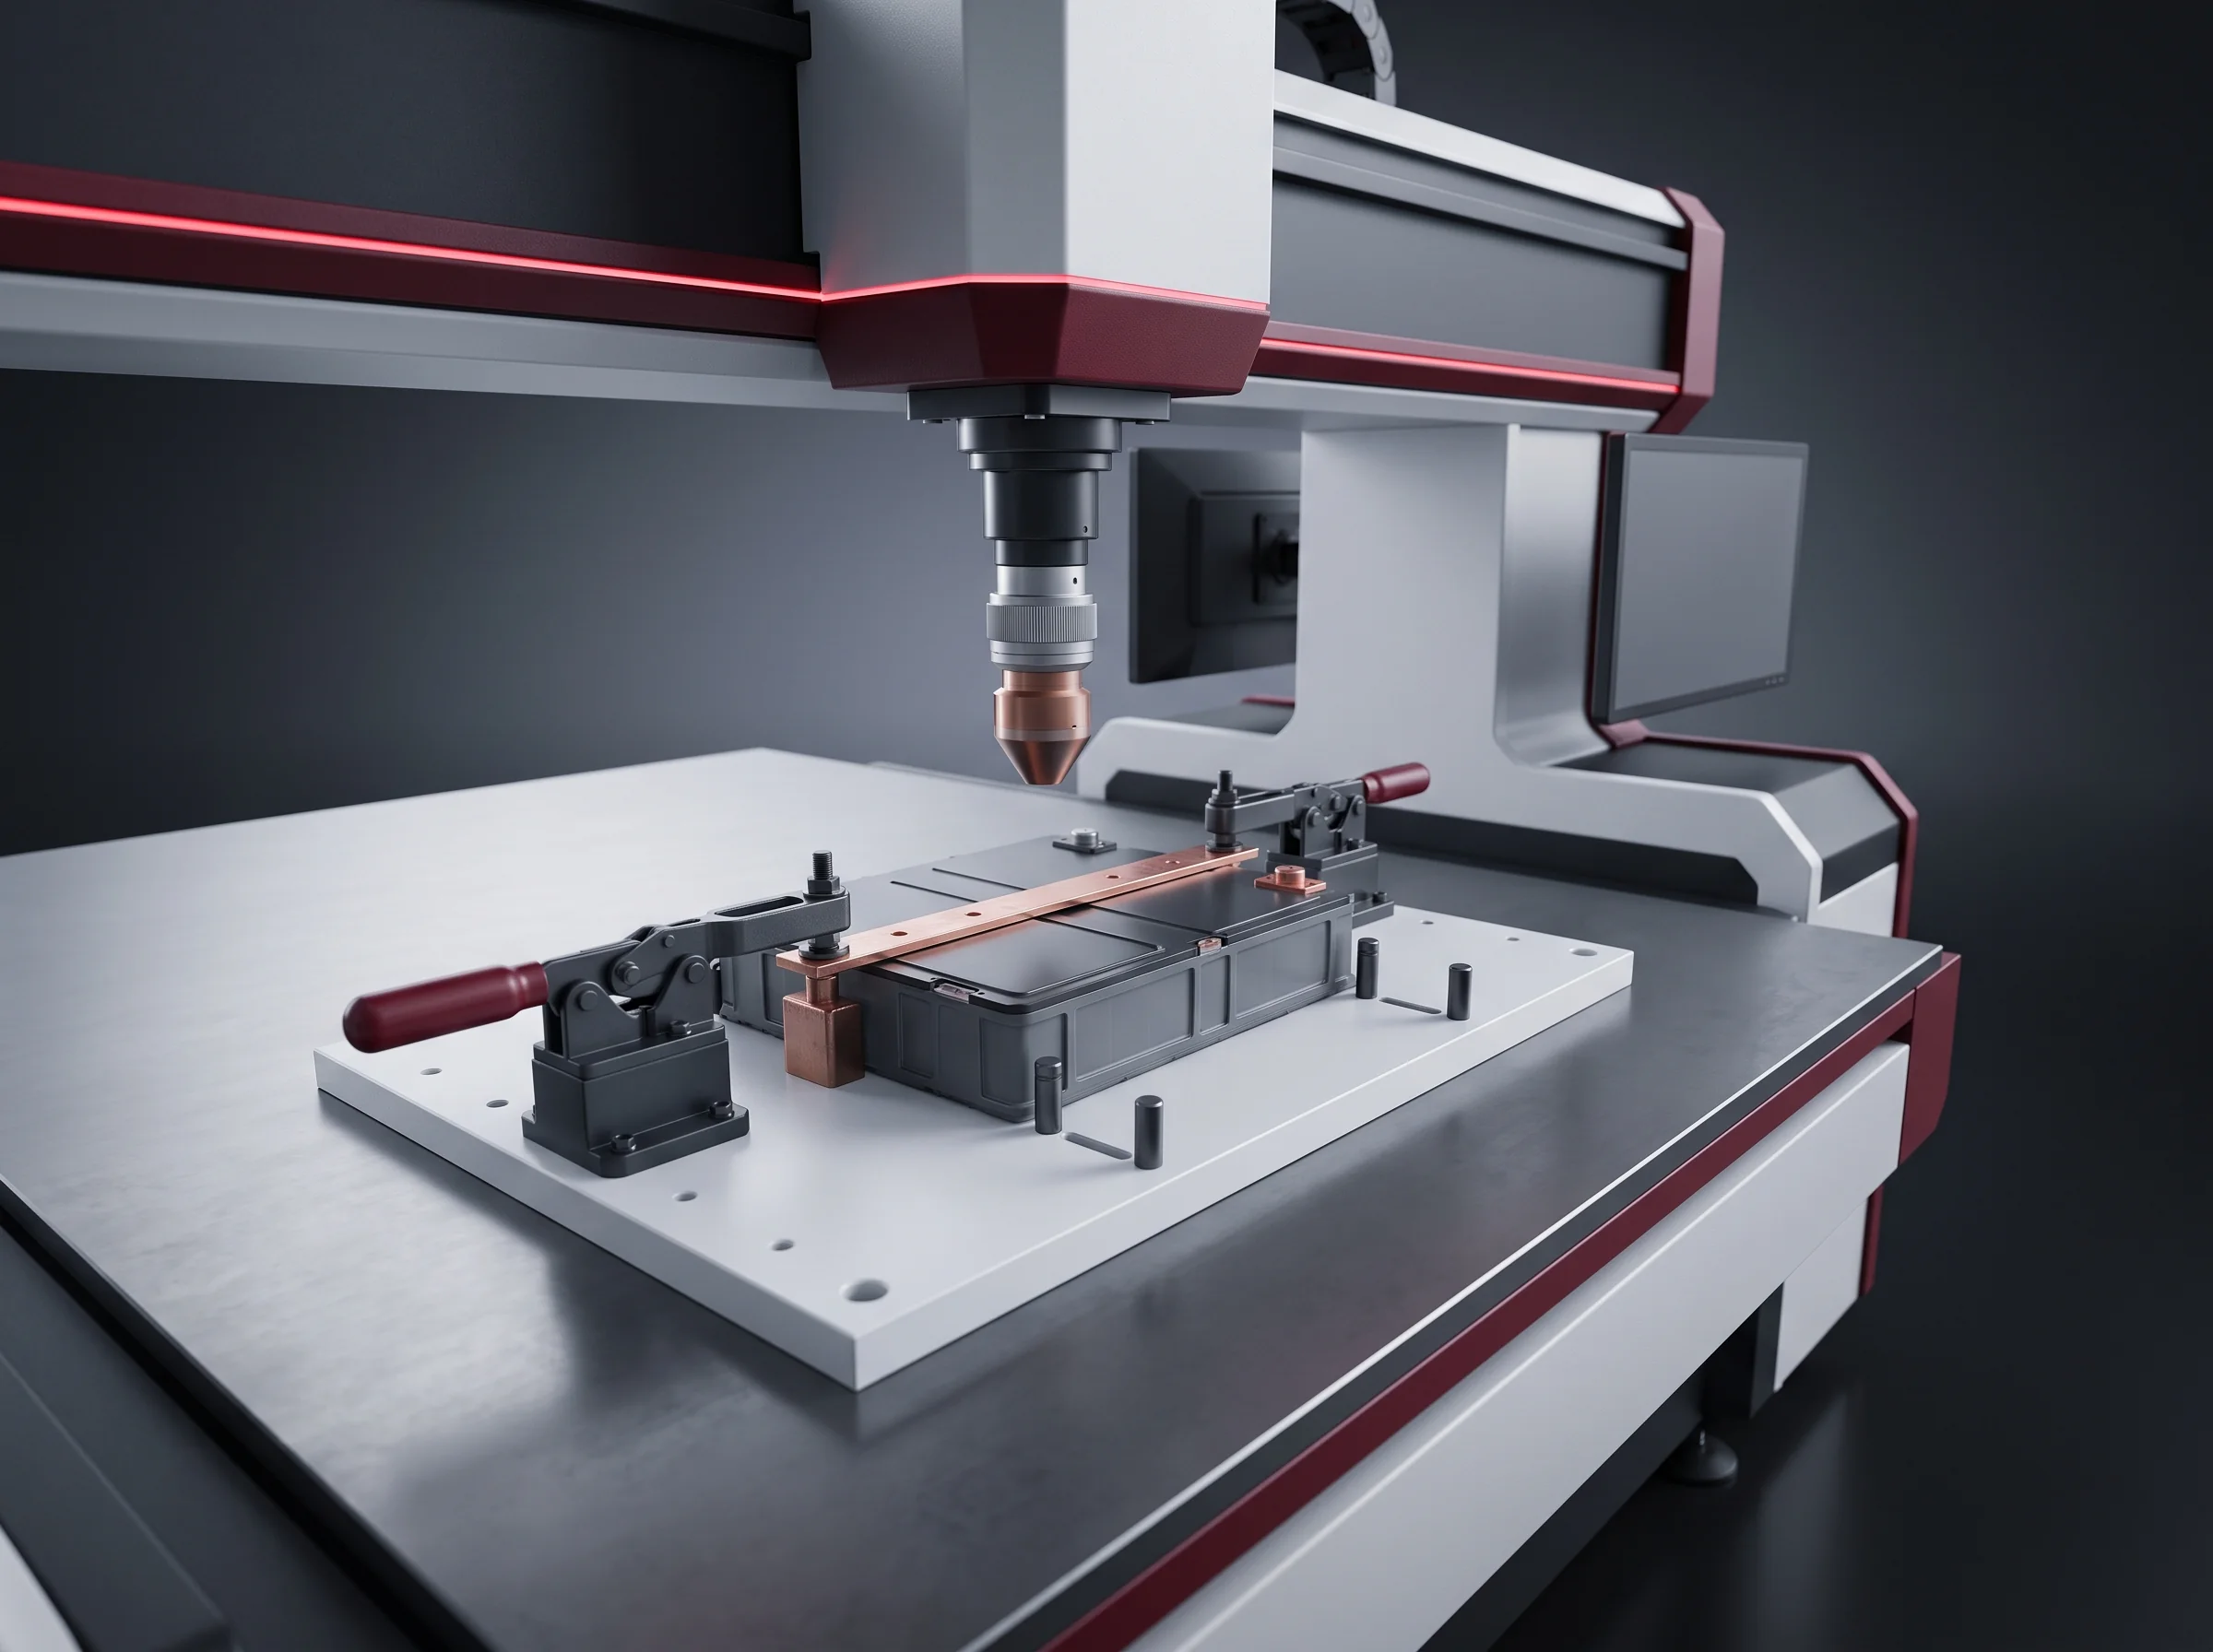
Part clamped in its fixture on the gantry welding table for rework

Rework under a part number

Parts pulled off the line are rewelded here to the recipe stored against their own part number, not to whatever is convenient on shift.
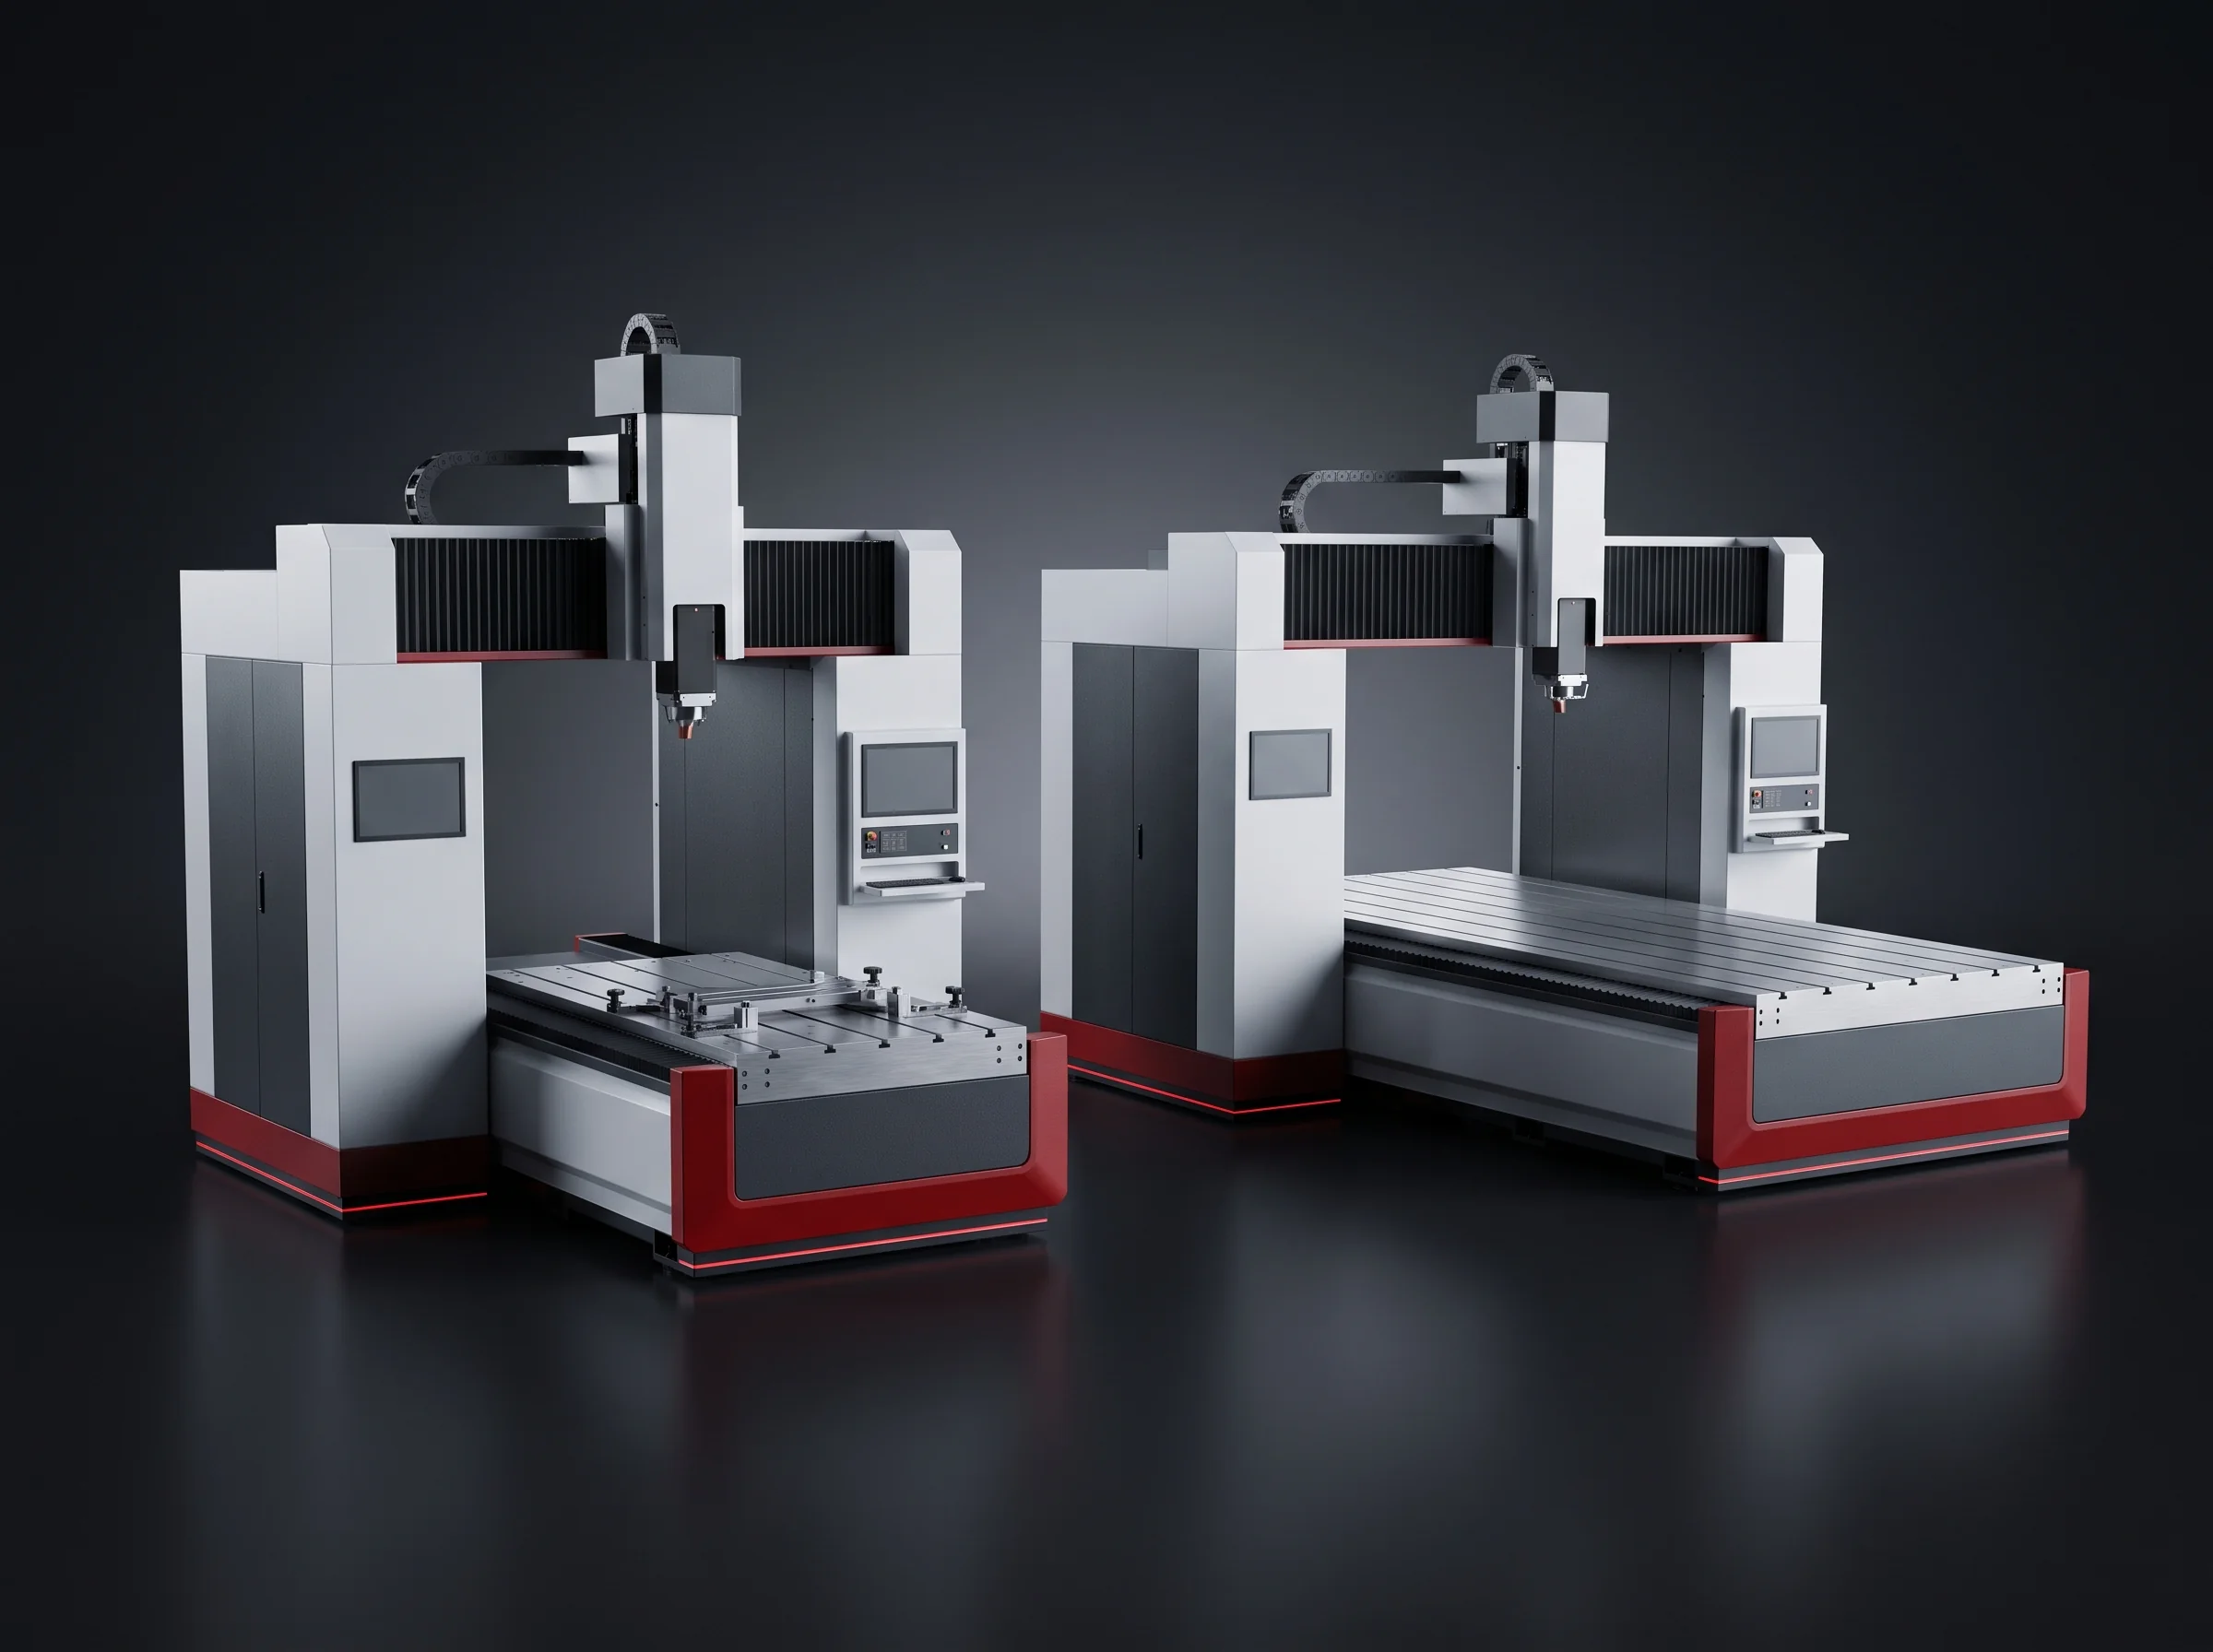
Two gantry frame sizes offered for module and bracket welding work

Low-volume welding

Module or bracket welding for a plant that does not yet need an inline welder, on either of two frame sizes. Detail on the gantry page.

Module 16 & Pack 14

End-Of-Line Testing, Module And Pack

BLP-EOL appears twice on a line, and reading that as duplication is the commonest misreading of the station list.

 Module station 16Pack station 14
Object under test One module — 13 cells in series on the blueprint 1P13S, its own busbars and barriers A complete 1P52S pack: enclosure, cooling plate, BMS, MSD, connectors, harness
Insulation path Cell group to module structure Runs to a metal enclosure absent at module 16 New path
Failures it catches Cell and module level: a bad joint, a displaced barrier, a cell out of grade Assembly: a pinched harness, a fastener through a barrier, a connector not seated
What a failure costs One module, held before it is glued in and wired to twelve others A pack opened again after gluing, fixing and harness dressing
Items run Insulation at DC 1000 V against 500 MΩ or better · hipot at DC 2800 V, leakage 10 mA or less · total voltage with resistance · continuity

Why the module run earns its place

  • It separates a problem the cells or module segment created from one the pack line created.
  • Without it, every failure at pack 14 is an argument about whose station caused it.
  • On the branch, packs at 60 V or under get DC 500 V insulation instead of a DC 2800 V hipot.
Insulation Hipot Voltage and resistance Continuity

Thresholds and fixtures on the end-of-line testing page.
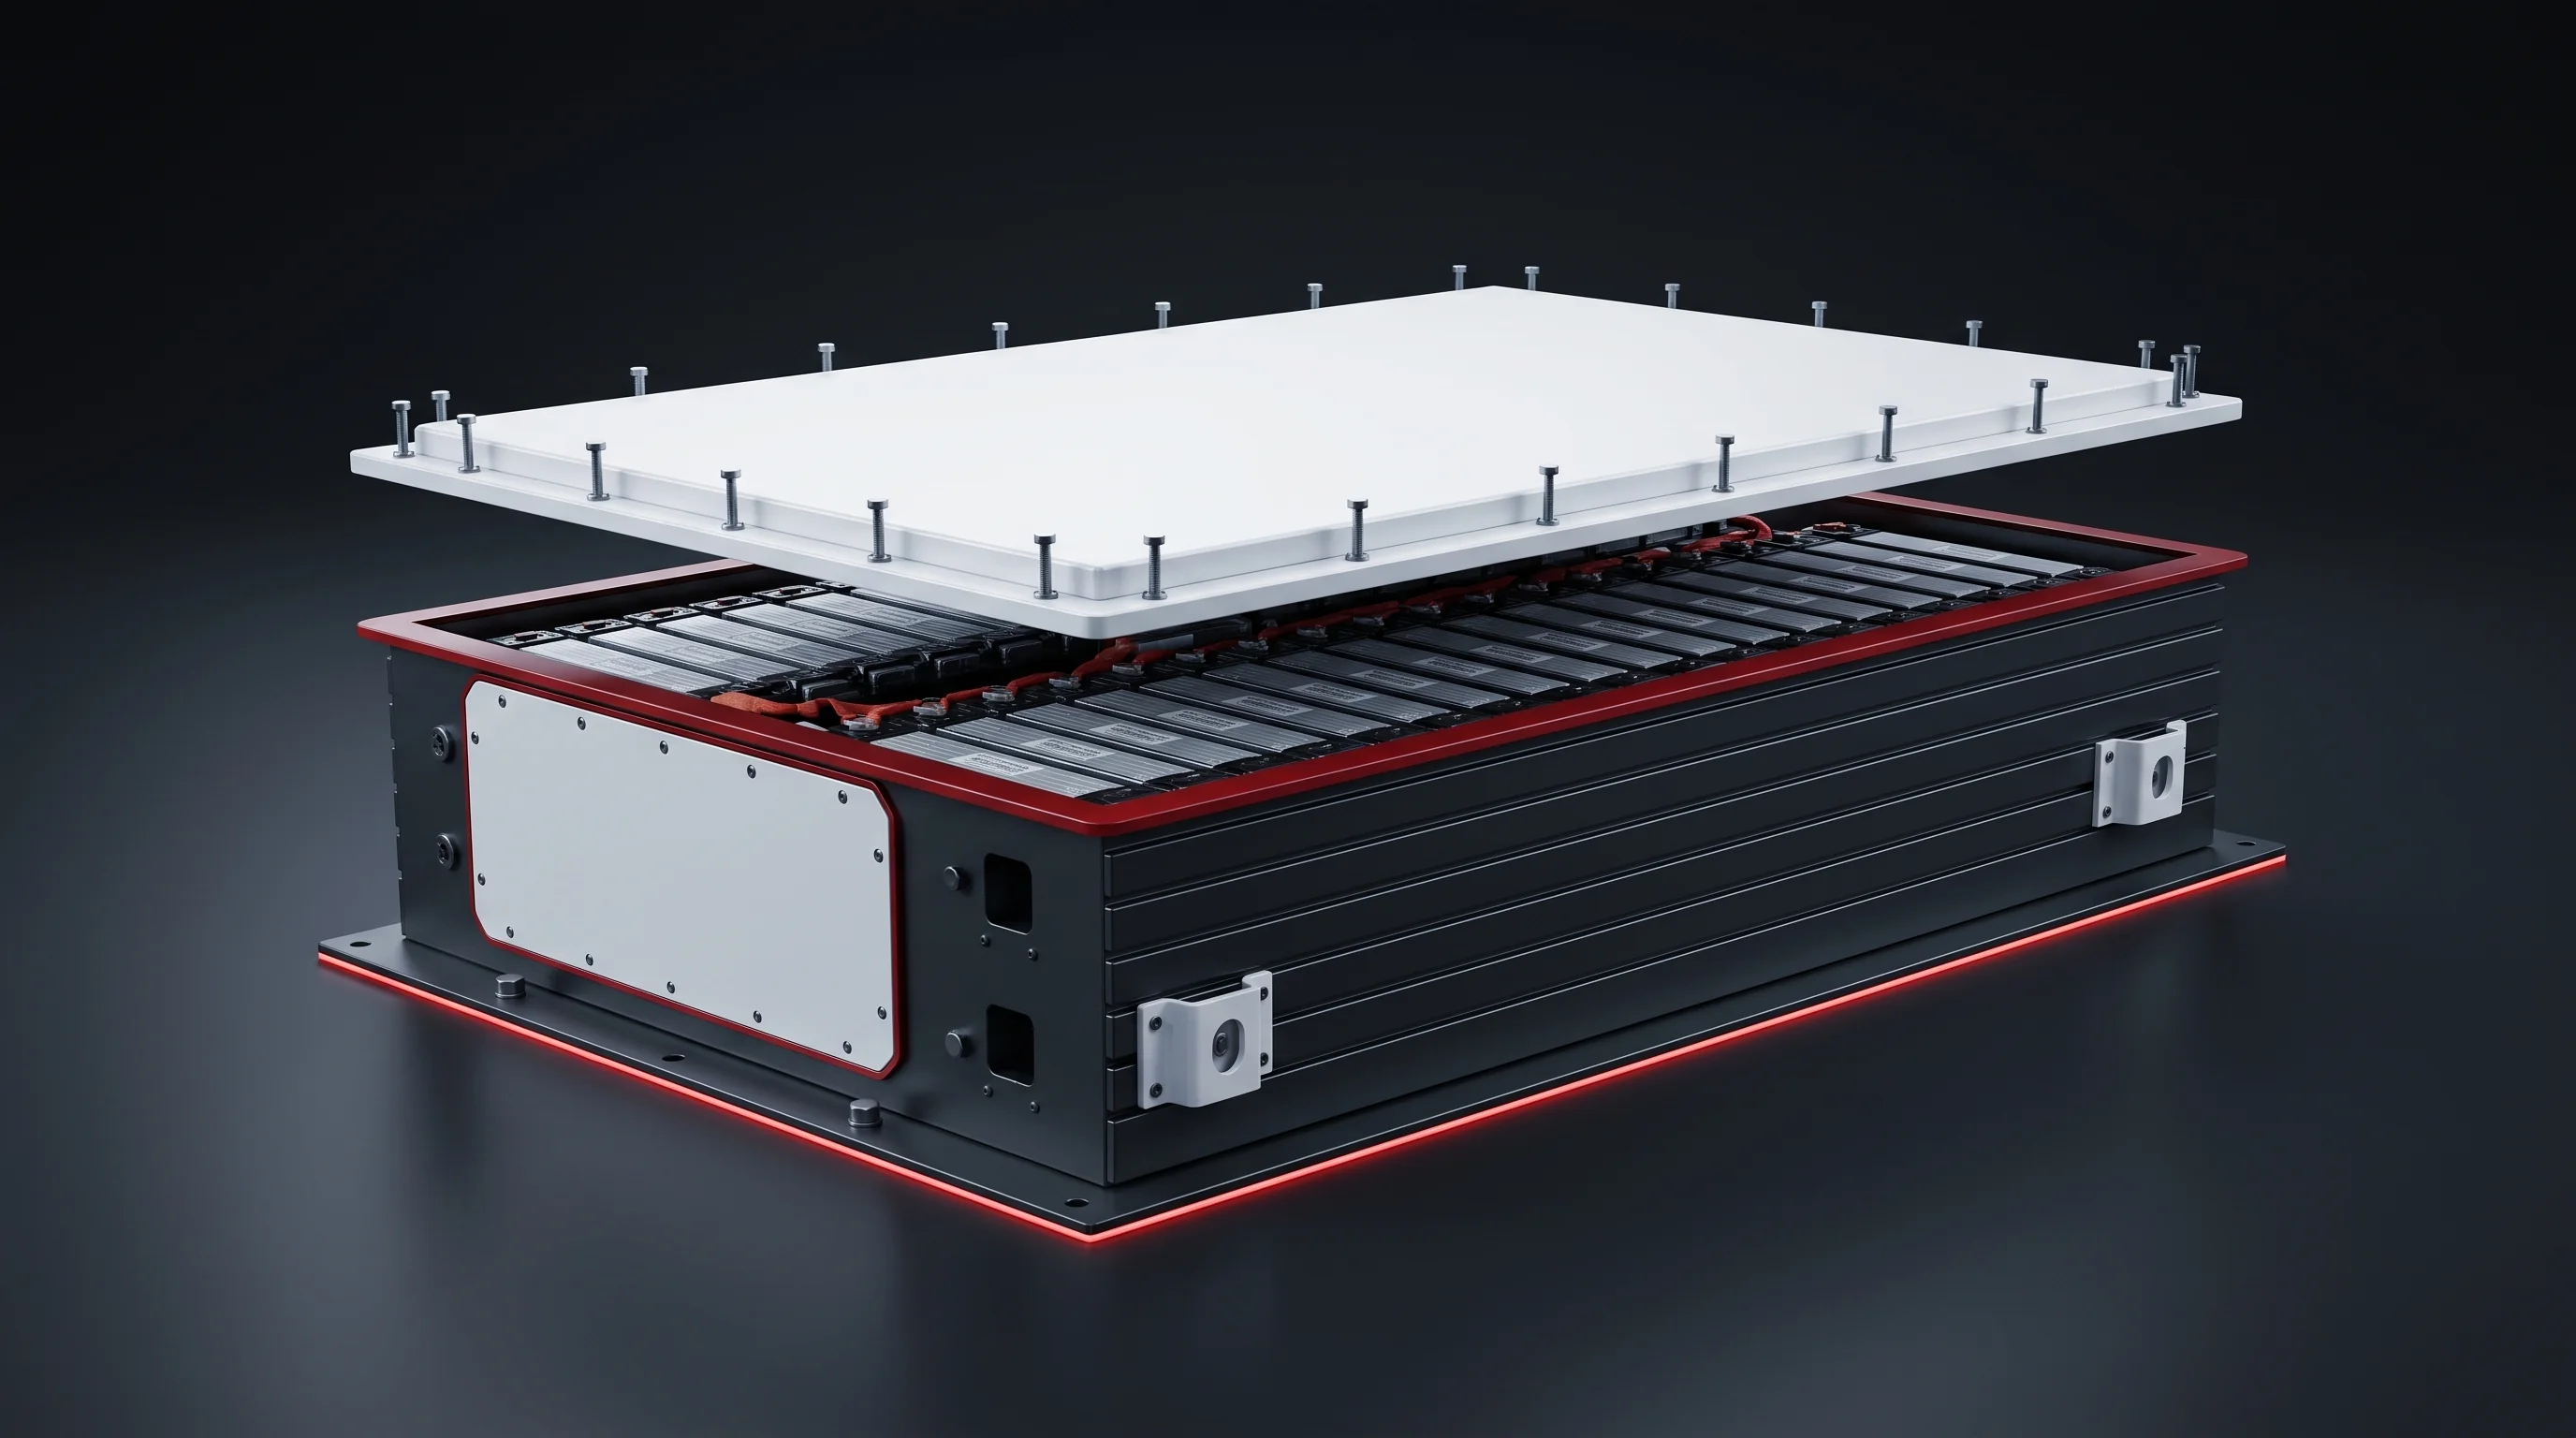
Pack enclosure and lid closed before the pack-level end-of-line test
At pack 14 the enclosure joins the insulation path.
End-of-line test bench used for lower voltage class packs on the branch
The branch bench, lower class.

Send four things

An Equipment List, Named Station By Station

Your cell datasheet, module and pack configuration, target takt, and what is on your floor now. Back within 24 hours: every machine named, its position in the two sequences, and whether this reads as one station, a segment or a whole line.

Cell datasheet Module and pack configuration Target takt or annual output Your existing line, if any

Pack 03

Gluing And The Pack Segment

BLP-GL applies adhesive to the enclosure floor and cooling plate before modules go in. It is also one of only four automatic stations out of fifteen on the pack segment.

Volume, not speedA fast thin bead covers the same path as a correct one.

What the station controls

  • Camera location ±0.2 mm, bead path ±2 mm, volume to 5% on twin servo pumps
  • Two-component adhesive, ratio settable 1:1 to 2:1, static mixer changed in line
  • Path, volume and pressure to your MES over PROFINET, by pack number

The pressure trace exposes a partially blocked nozzle: the path completes, pressure climbs, delivered volume drops below the window, and the part is held rather than passed on looking finished.

Open time is counted, not assumed

A part past the stored open time is held: uncured, cleaned and recoated in the station; cured, sent to rework under its enclosure number.

Dispensing station applying adhesive to a cooling plate with twin servo pumps
Twin servo pumps, volume to 5%.
Pack segment of a high-automation battery manufacturing equipment line
The pack segment, quoted as it is.
Cooling plate Enclosure floor One pressure trace per pack

Pack segment, all fifteen stations labelled

Auto Semi-auto Manual
  • 01
  • 02
  • 03
  • 04
  • 05
  • 06
  • 07
  • 08
  • 09
  • 10
  • 11
  • 12
  • 13
  • 14
  • 15
  • 4 of 15Auto: leak test, gluing, pack leak, EOL
  • 3 of 15Semi-auto: insertion, tightening, offload
  • 12–14People on a P8S or P15 pack segment

Module fixing, copper bar mounting, BMS and MSD installation, harness dressing and lid fitting are hands. Station by station on the pack line page.

Between stations
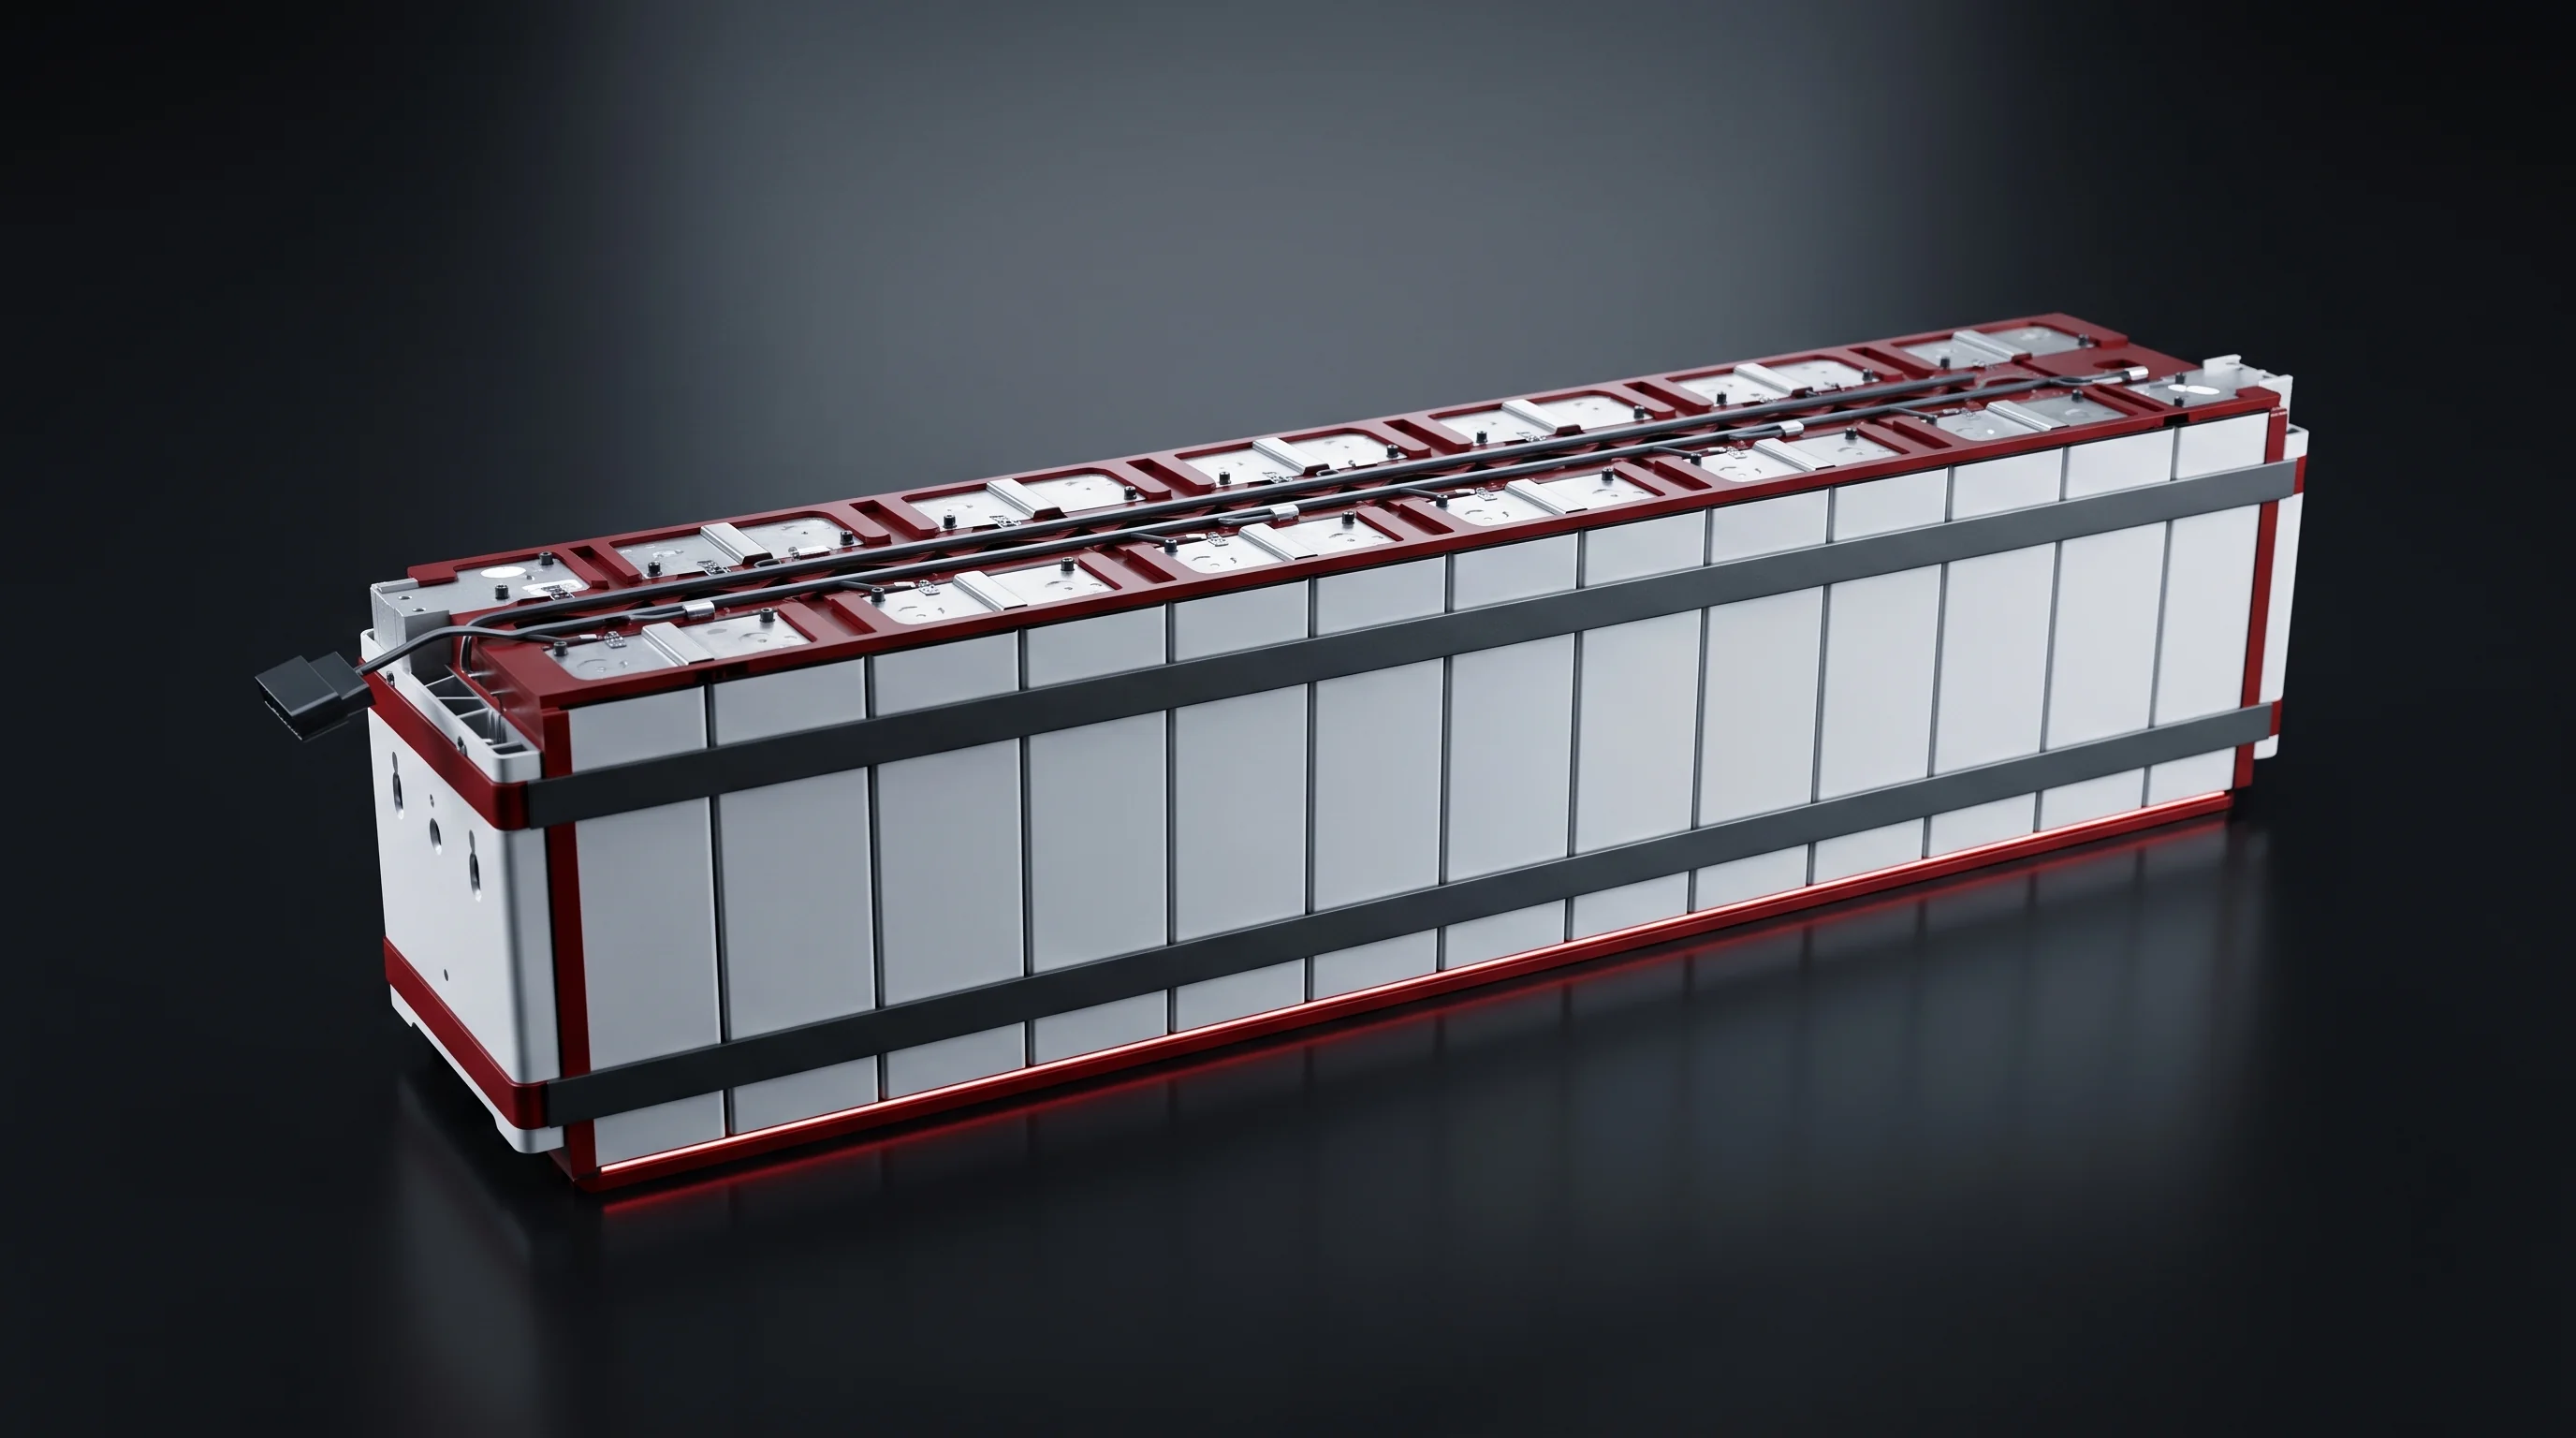
Module Conveying

Modules on fixtures, not finished packs

Load
200 kg or more
Speed
20 m/min or less
Stop repeat
±0.5 mm
Lift pin
±0.1 mm, 30 mm stroke
It does not carry packsThe blueprint module is 100 kg or less, so the rating carries roughly a factor of two. The 1P52S pack is 400 kg or less and moves on pack-segment handling.
Module conveyor with panelled sides and stop-and-lift positioning units
Panelled both sides.
Battery module of the kind carried on the conveyor fixture between stations
RFID by module number.

Sections and transfer heights on the conveyor system page.

Cylindrical branch

Nine More Machines For Cylindrical Packs

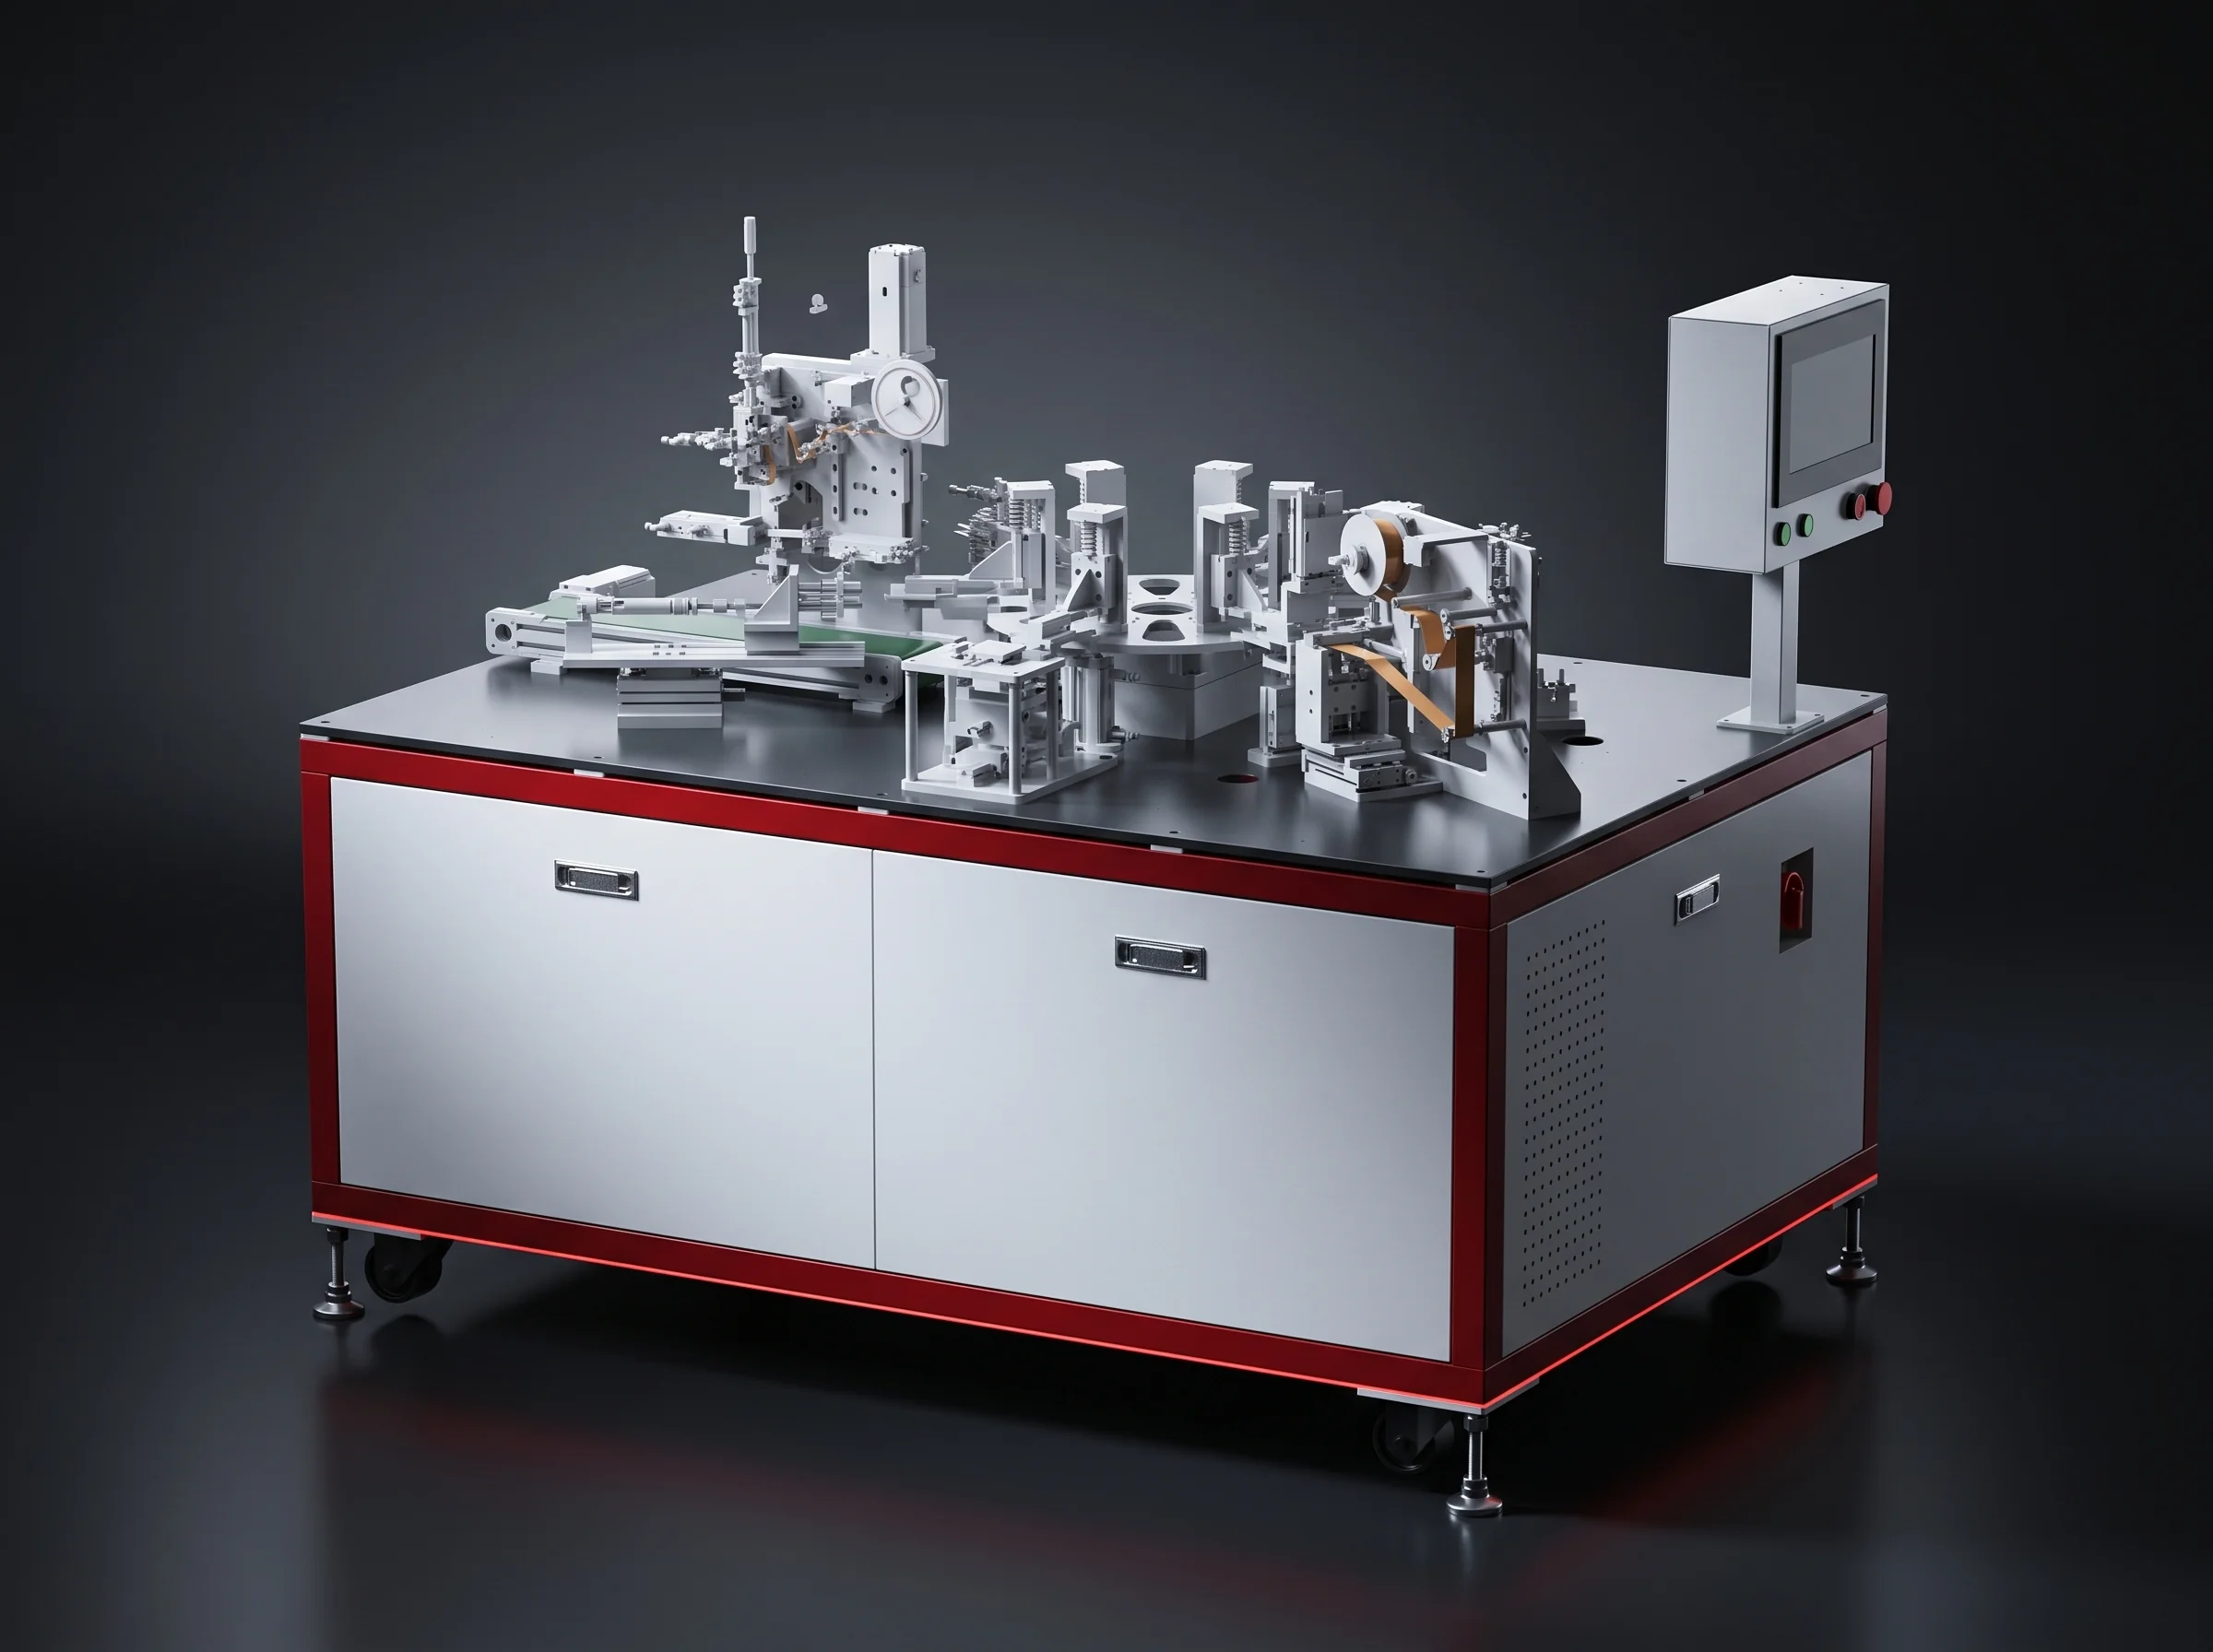
Power tools, light electric vehicles and portable storage are built from 18650, 21700 and 26650 cells. Seven single stations, two complete lines.
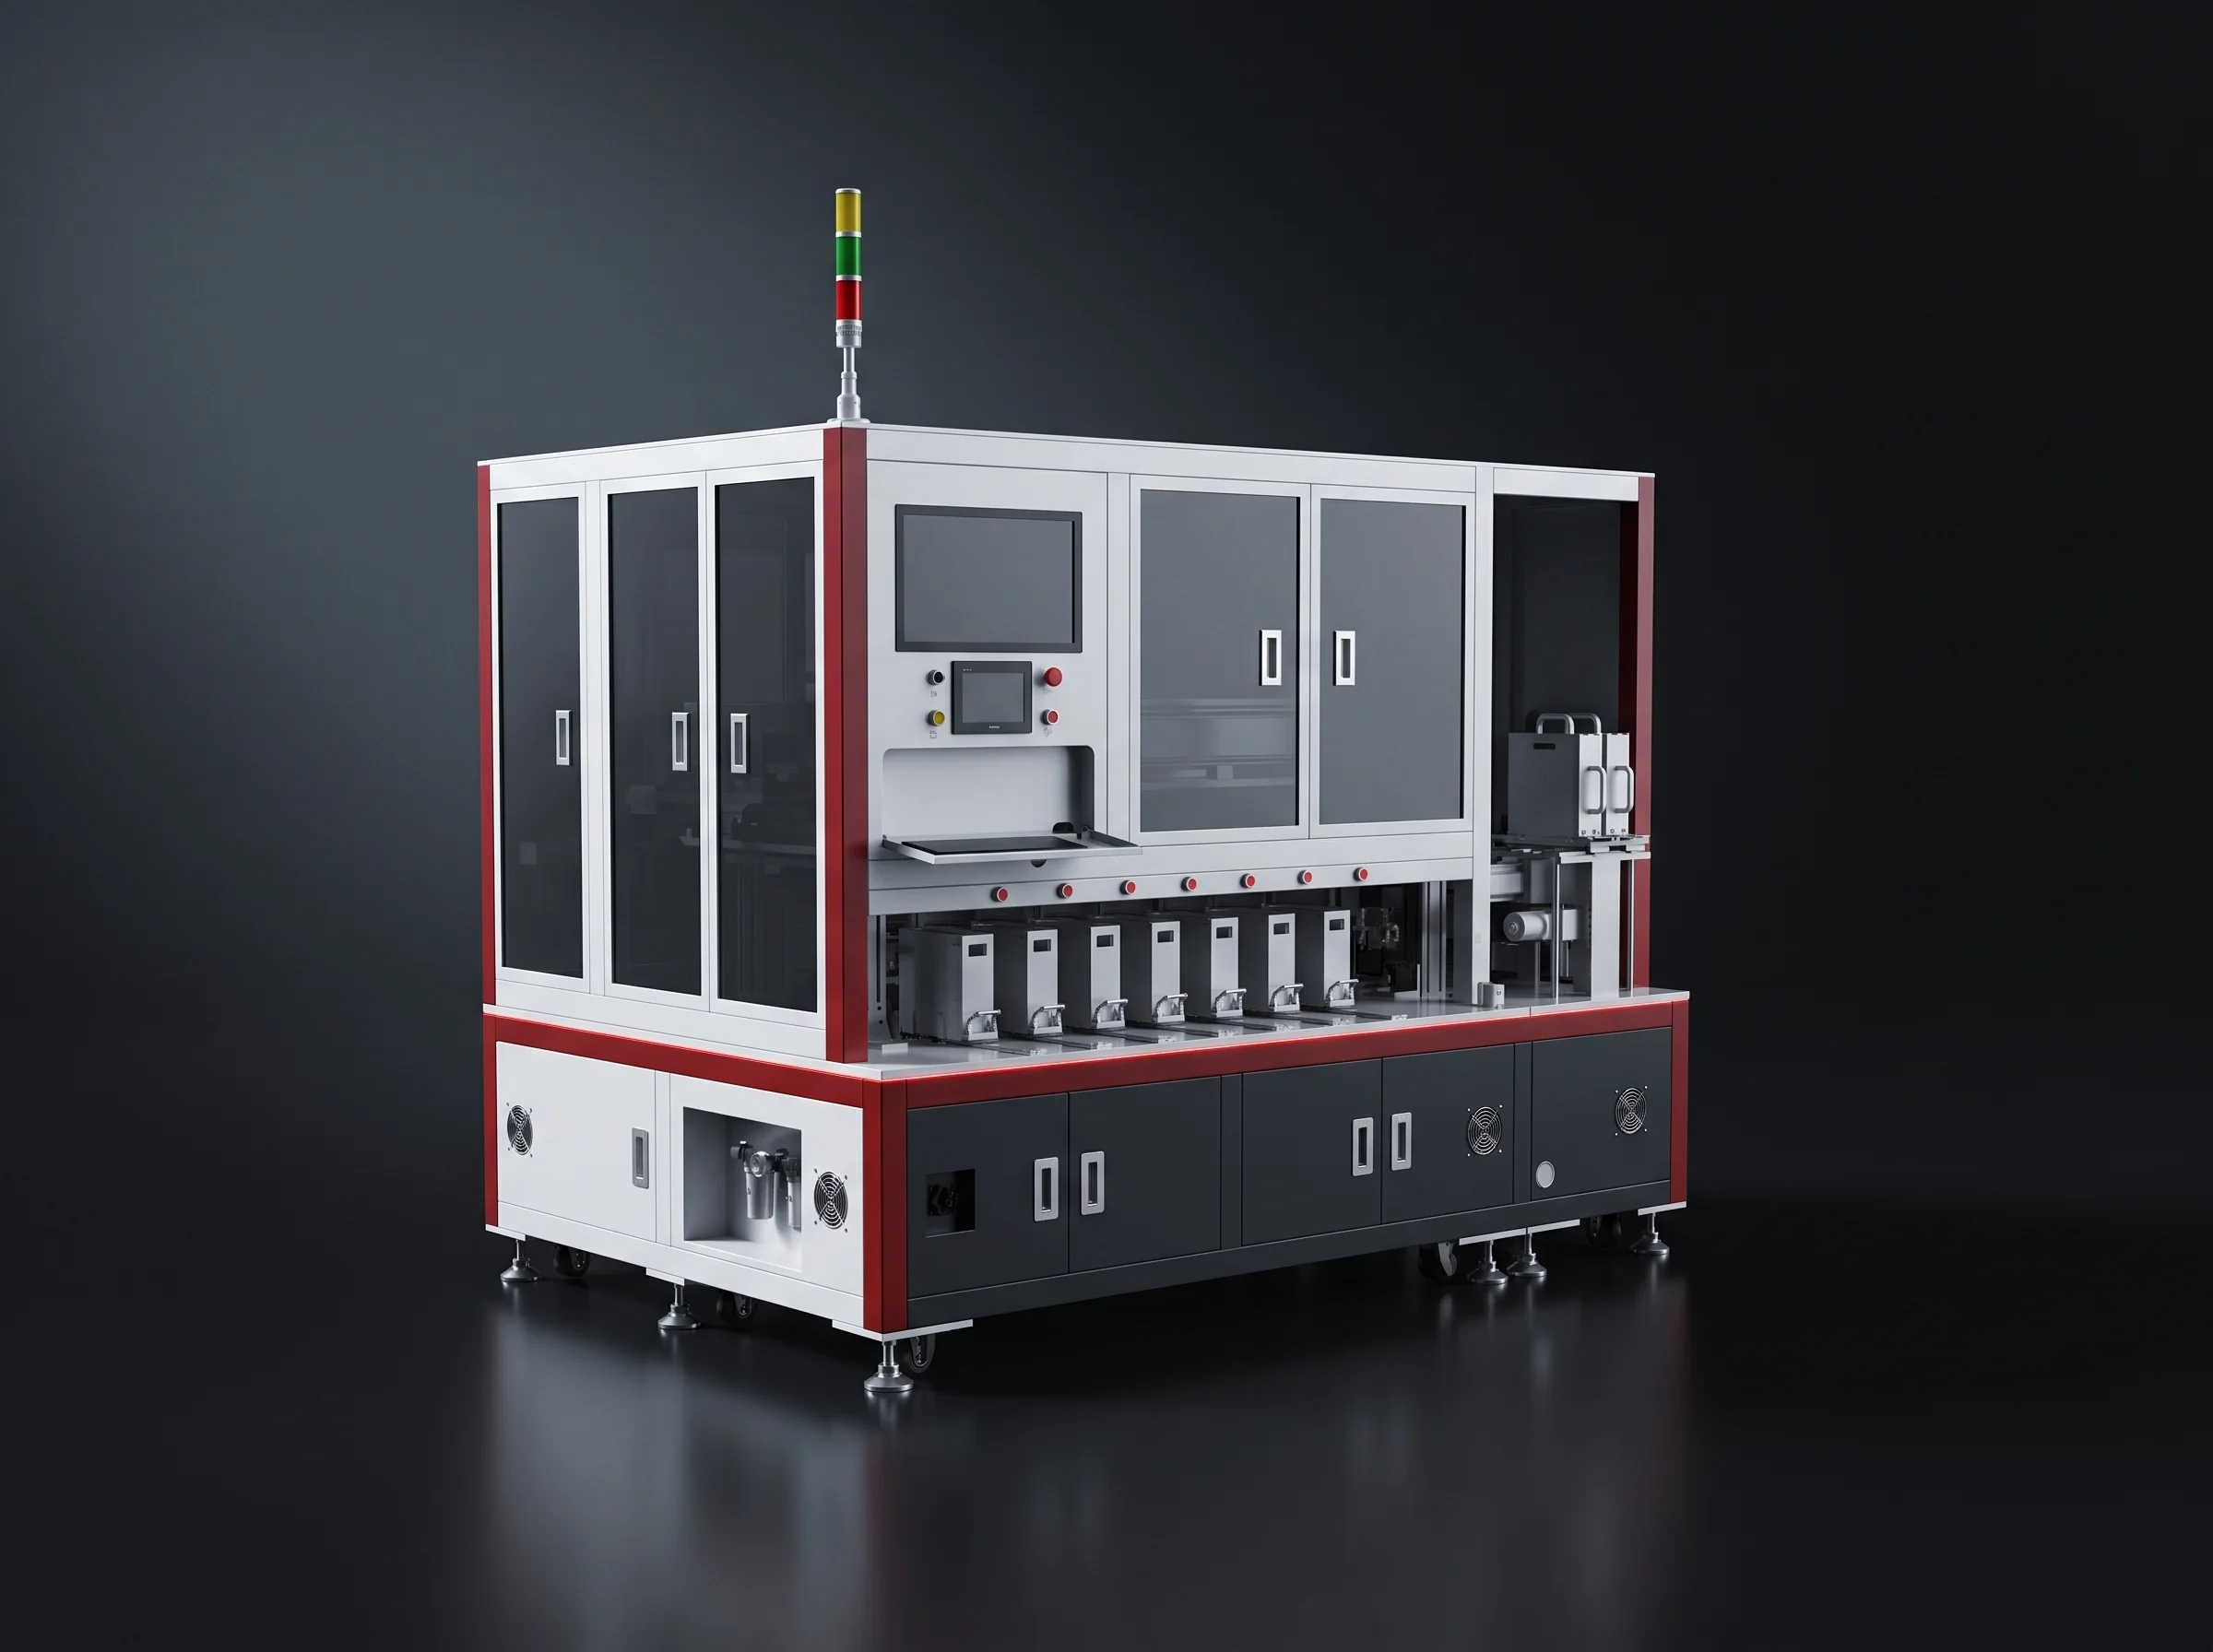
Automatic cylindrical cell sorter grading 18650 and 21700 cells
BLP-CS18

Cell sorter

4,000–6,000 cells/h · 10 grades
Insulation washer taping machine for the positive face of cylindrical cells
BLP-CT

Insulation washer

≤0.3 mm offset · 40–60/min
PVC sleeving and shrink machine for cylindrical cells
BLP-CP

PVC sleeve and shrink

Zoned heat · 40–60/min
Station applying side double-sided tape to cylindrical cells for bracket loading
BLP-CB

Side tape

Per bracket · 40–60/min
Nickel tab welder and bender with twin-pin precision welding heads
BLP-CW

Nickel tab weld and bend

0.1–0.3 mm · 60–90 welds/min
Bracket and nickel strip assembly receiving structural adhesive
BLP-CD

Bracket adhesive

±0.2 mm · ±5% metering
Heat sealing machine closing consumer pack shells
BLP-CE

Shell heat sealing

15–25 pieces/min
Finished power tool battery packs built on the cylindrical branch line
BLP-CL

Cylindrical pack line

300–600 packs/shift
Protection board welded and taped on the consumer pack line
BLP-CM

Consumer pack line

500–1,000 packs/shift
BLP-CLSemi-automatic line

Sorting through to packing

Sorting, bracket loading, nickel welding, BMS assembly, testing and packing, on 5S2P to 13S4P builds. Sampled pull testing at 30 N or more.

300–600 packs per shift

BLP-CMSemi-automatic line

Protection board through to test

Protection board welding, taping, bending, packing and testing — voltage, resistance, charge and discharge function, insulation.

500–1,000 packs per shift

The branch shares three rules with the main line: the sorting window is agreed in writing, welding parameters live in recipes, and operators do not hold them. Both lines on the cylindrical and consumer page.

One rule, four machines

Recipes And Signatures Across Stations

Every station that puts energy into a part runs from a stored recipe, and three rules cover all of them.

Operators select, never editThe process engineer writes recipes; quality countersigns each change.

The three rules

  • Stored by part number. A busbar geometry, a bracket and strip specification, a module type — each has its own set, and the machine will not run one against another.
  • Selected, not edited. The shop-floor account calls a recipe and releases a held part; it cannot change a number.
  • Two signatures per change. Process engineer writes, quality countersigns, both names recorded.

Off-line to inline, unchanged

A recipe for a new busbar geometry is created on BLP-WG, welded onto samples and pull tested. Once the samples meet the criterion, it moves to BLP-W6 unchanged — same format, same part number, same two signatures.
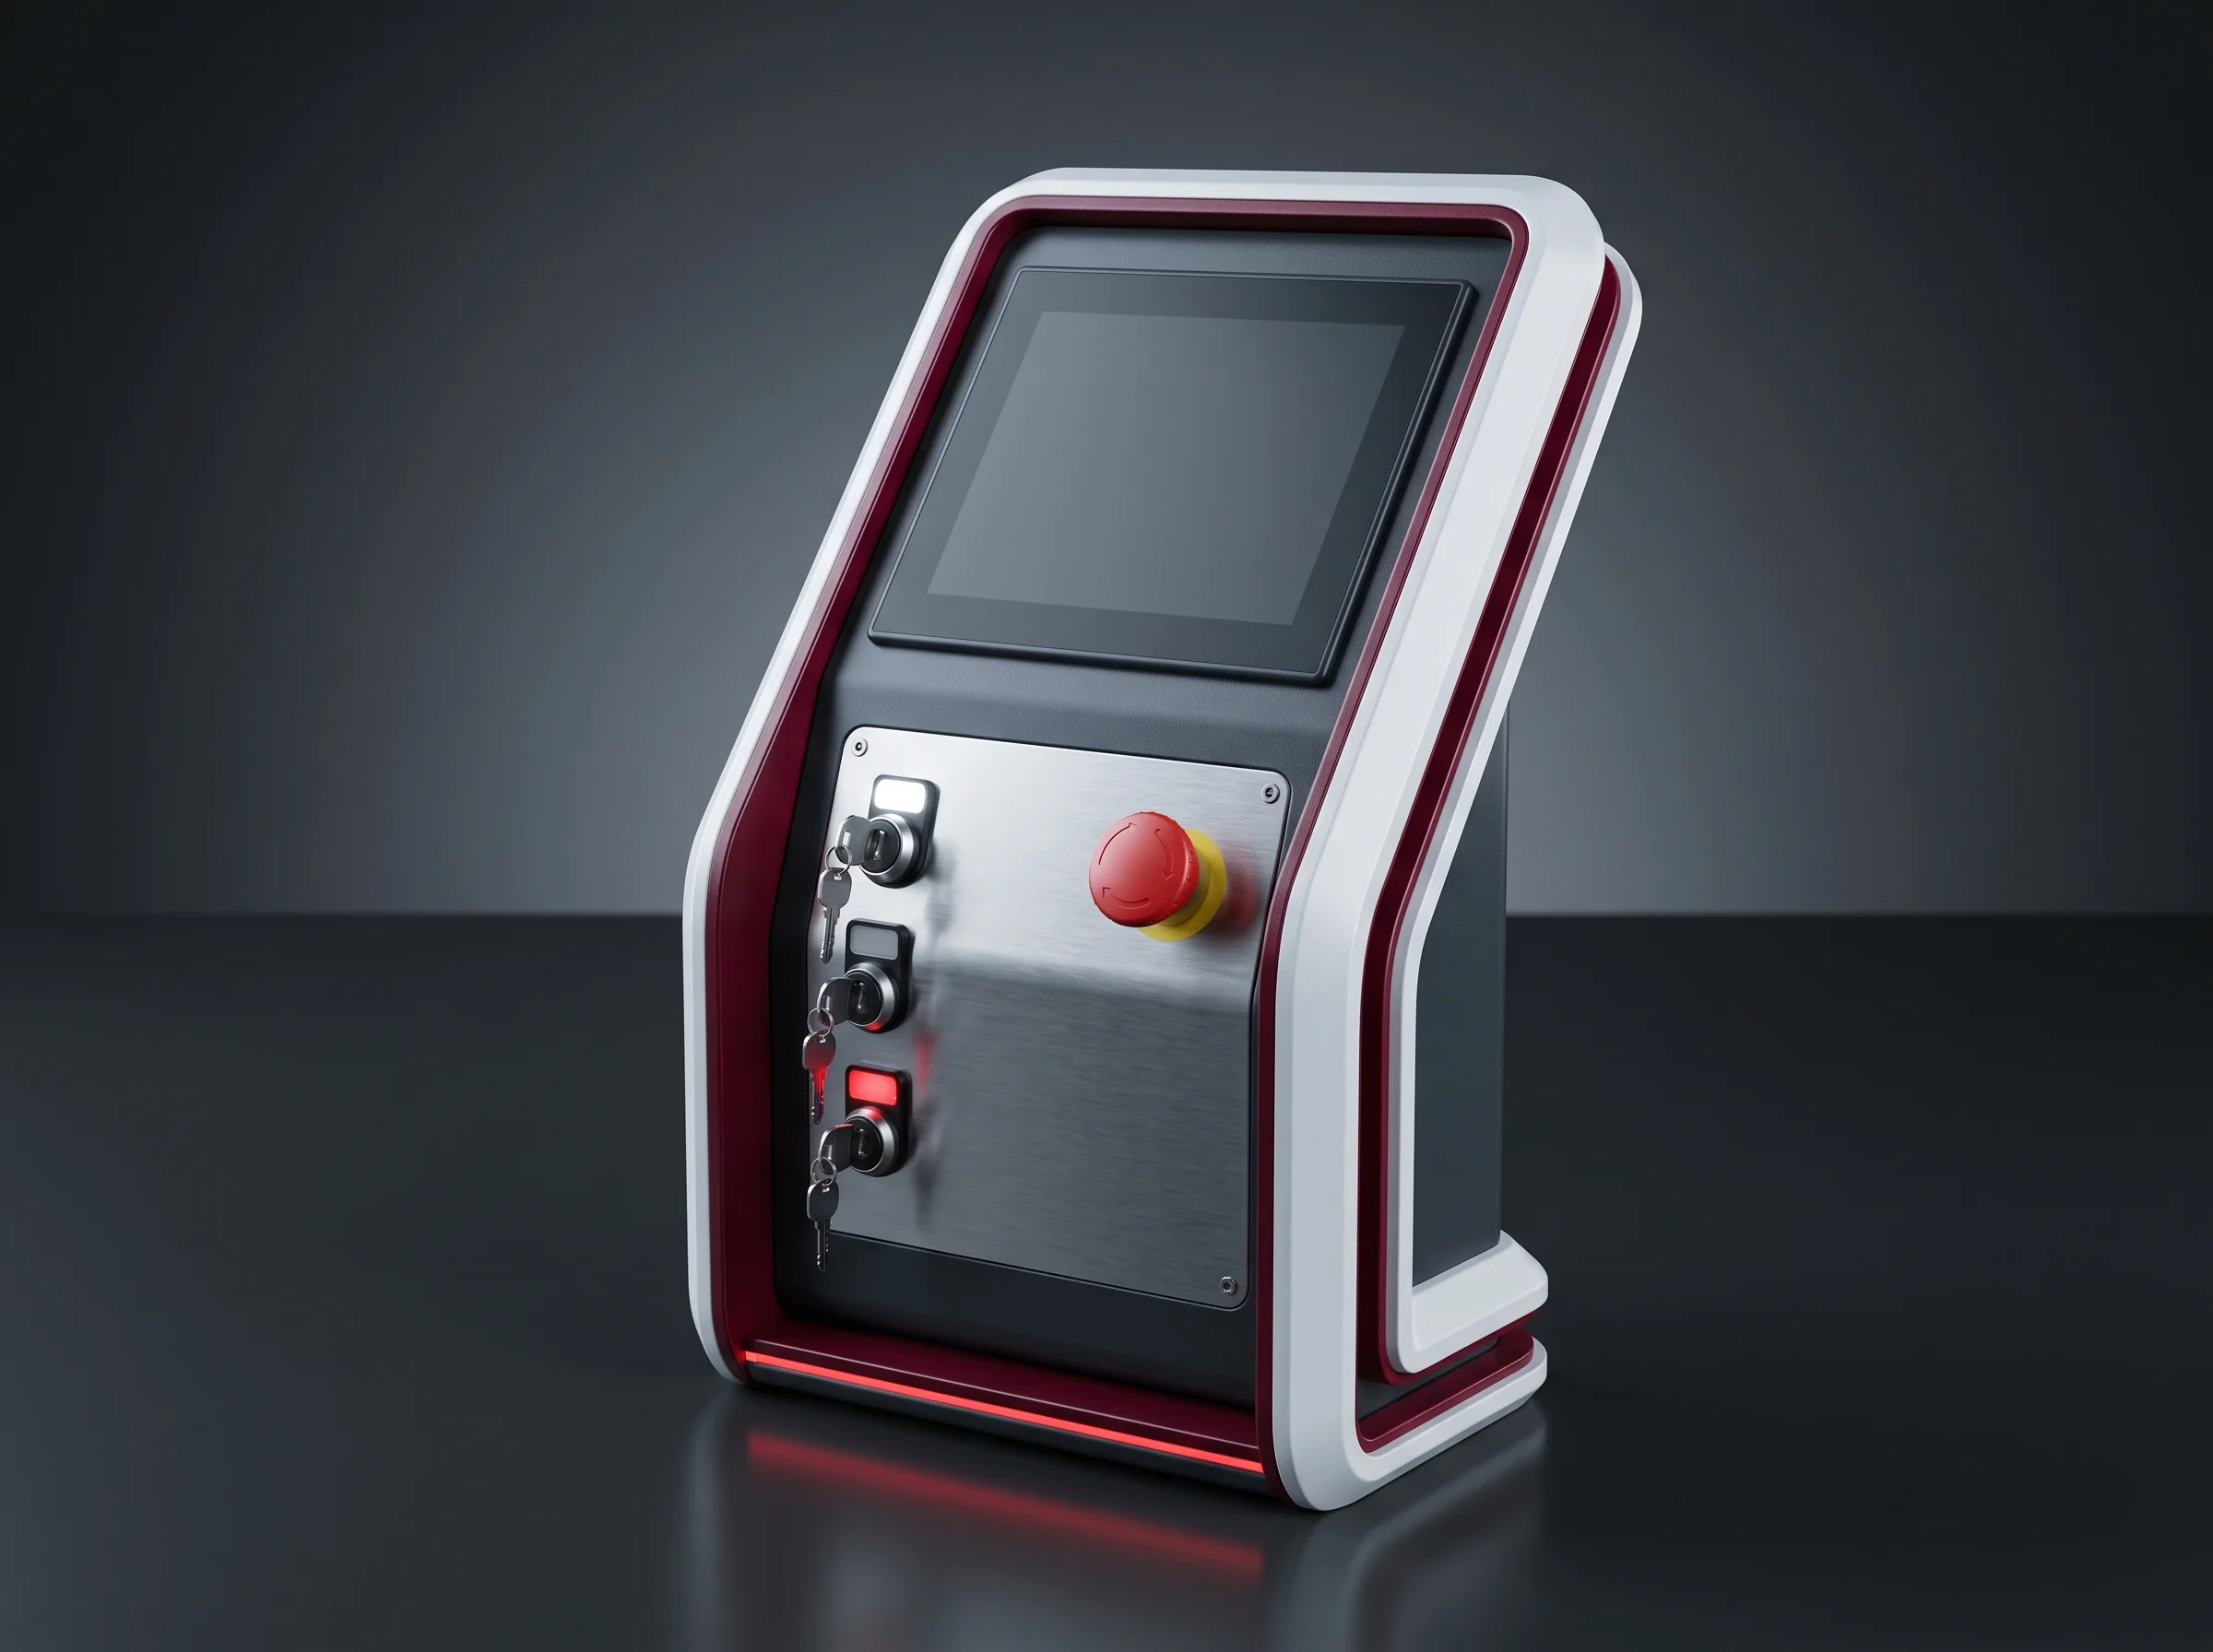
Station panel showing the account levels that separate selecting a recipe from editing one
Three account levels per station panel.
Laser source cabinet holding the parameter set a recipe calls up
What a recipe number resolves to.
BLP-W6Inline busbar welding — power, speed, focal position, nitrogen.
BLP-WGOff-line gantry — where recipes are created and proved.
BLP-CWBranch nickel welder — bracket and strip instead of busbar.
BLP-SPPress — target force, dwell, target length, banding passes.

You receive a recipe list covering every welded and pressed part number, plus a change record: what changed, by whom, when.

Scope 03, in detail

One Station Into An Existing Line

A machine specification is half of what decides whether a station fits a line somebody else built. The other half is the interface sheet, different for every machine.

One sheet per stationYou get the sheet for the station you are buying, marked up against your line.

BLP-SP as the worked example

Transfer height is 900 ±50 mm, adjustable against your existing conveyor. Modules travel on their fixture, handed over by BLP-CV. Communication is PROFINET, force curve and pressed length by module number.

Those figures belong to BLP-SP and nothing else. BLP-WG is 4 × 2 m, 10 to 25 kW, external chiller. One house standard for both would be wrong for at least one.

Send four things, get the sheet back

The layout it is joining, conveyor height and pitch either side, and the fixture drawing.

Reply
Within 24 hours
Minimum order
One machine
Acceptance
On your conveyor
BLP-SP interfaceFigure
Transfer height900 ±50 mm, adjustable
HandoverModule on fixture, from BLP-CV
CommunicationPROFINET, by module number
Rated power8 kW, 380 V, 50 Hz
Compressed air0.5–0.7 MPa, ≤200 L/min
ChangeoverPlaten, fixture, stops — about 2 h
Layout desk where a customer floor drawing is marked up against a station interface sheet
Your layout against the interface sheet.
Fixtures cut to a module envelope for a station joining an existing line
Fixtures cut to your envelope, not ours.

Envelope ranges on the cell compatibility page; bay dimensions on the layout and utilities page.

Before it ships

Battery Manufacturing Equipment, Run Before Shipment

A line is set up in your ordered configuration, powered and run in a pre-assembly bay — not shipped as crates to be discovered on your floor.

The bay, and who stands in it

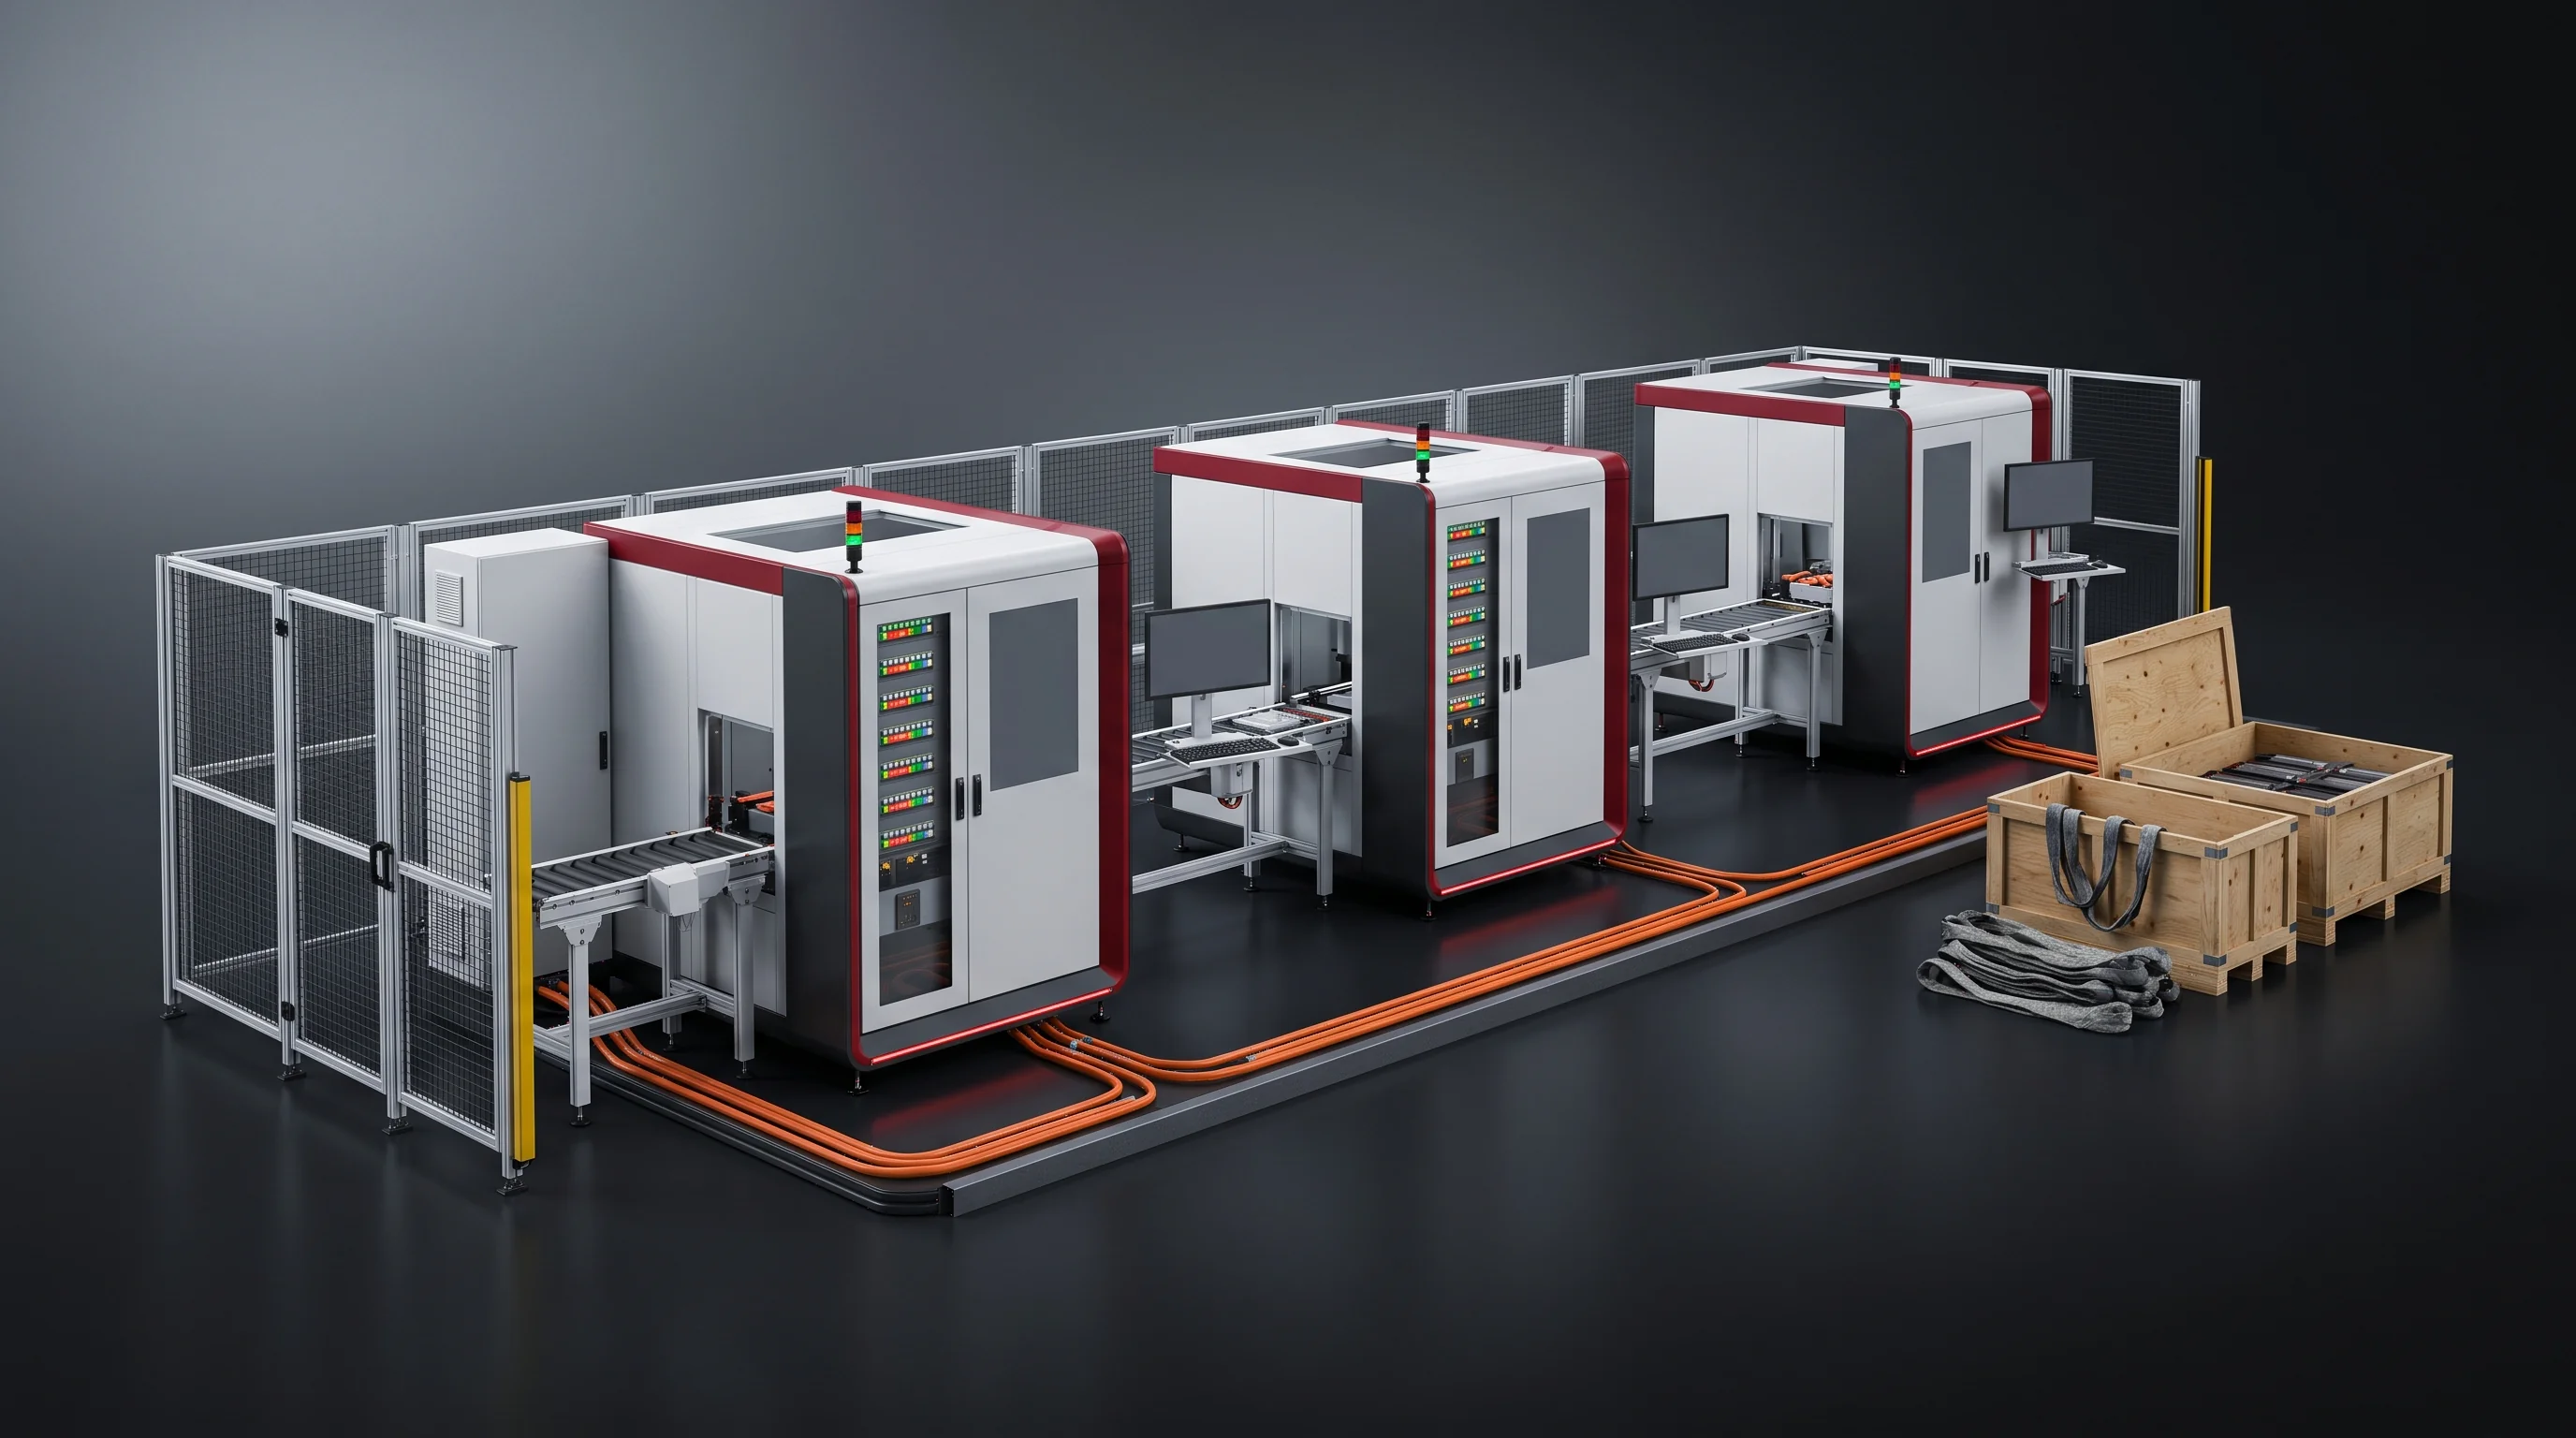
The assembly hall is 6,000 square metres with three pre-assembly bays. Factory acceptance happens there, on your cells, busbars, end plates, enclosures and cooling plates, against criteria signed before shipment.
  • 8Mechanical
  • 6Electrical and controls
  • 4Laser and vision process
  • 8Field installation
26 engineers 3 pre-assembly bays 40+ line segments into 12 countries
Line pre-assembly bay where a complete line is powered and run before shipment
One of three bays, in your configuration.
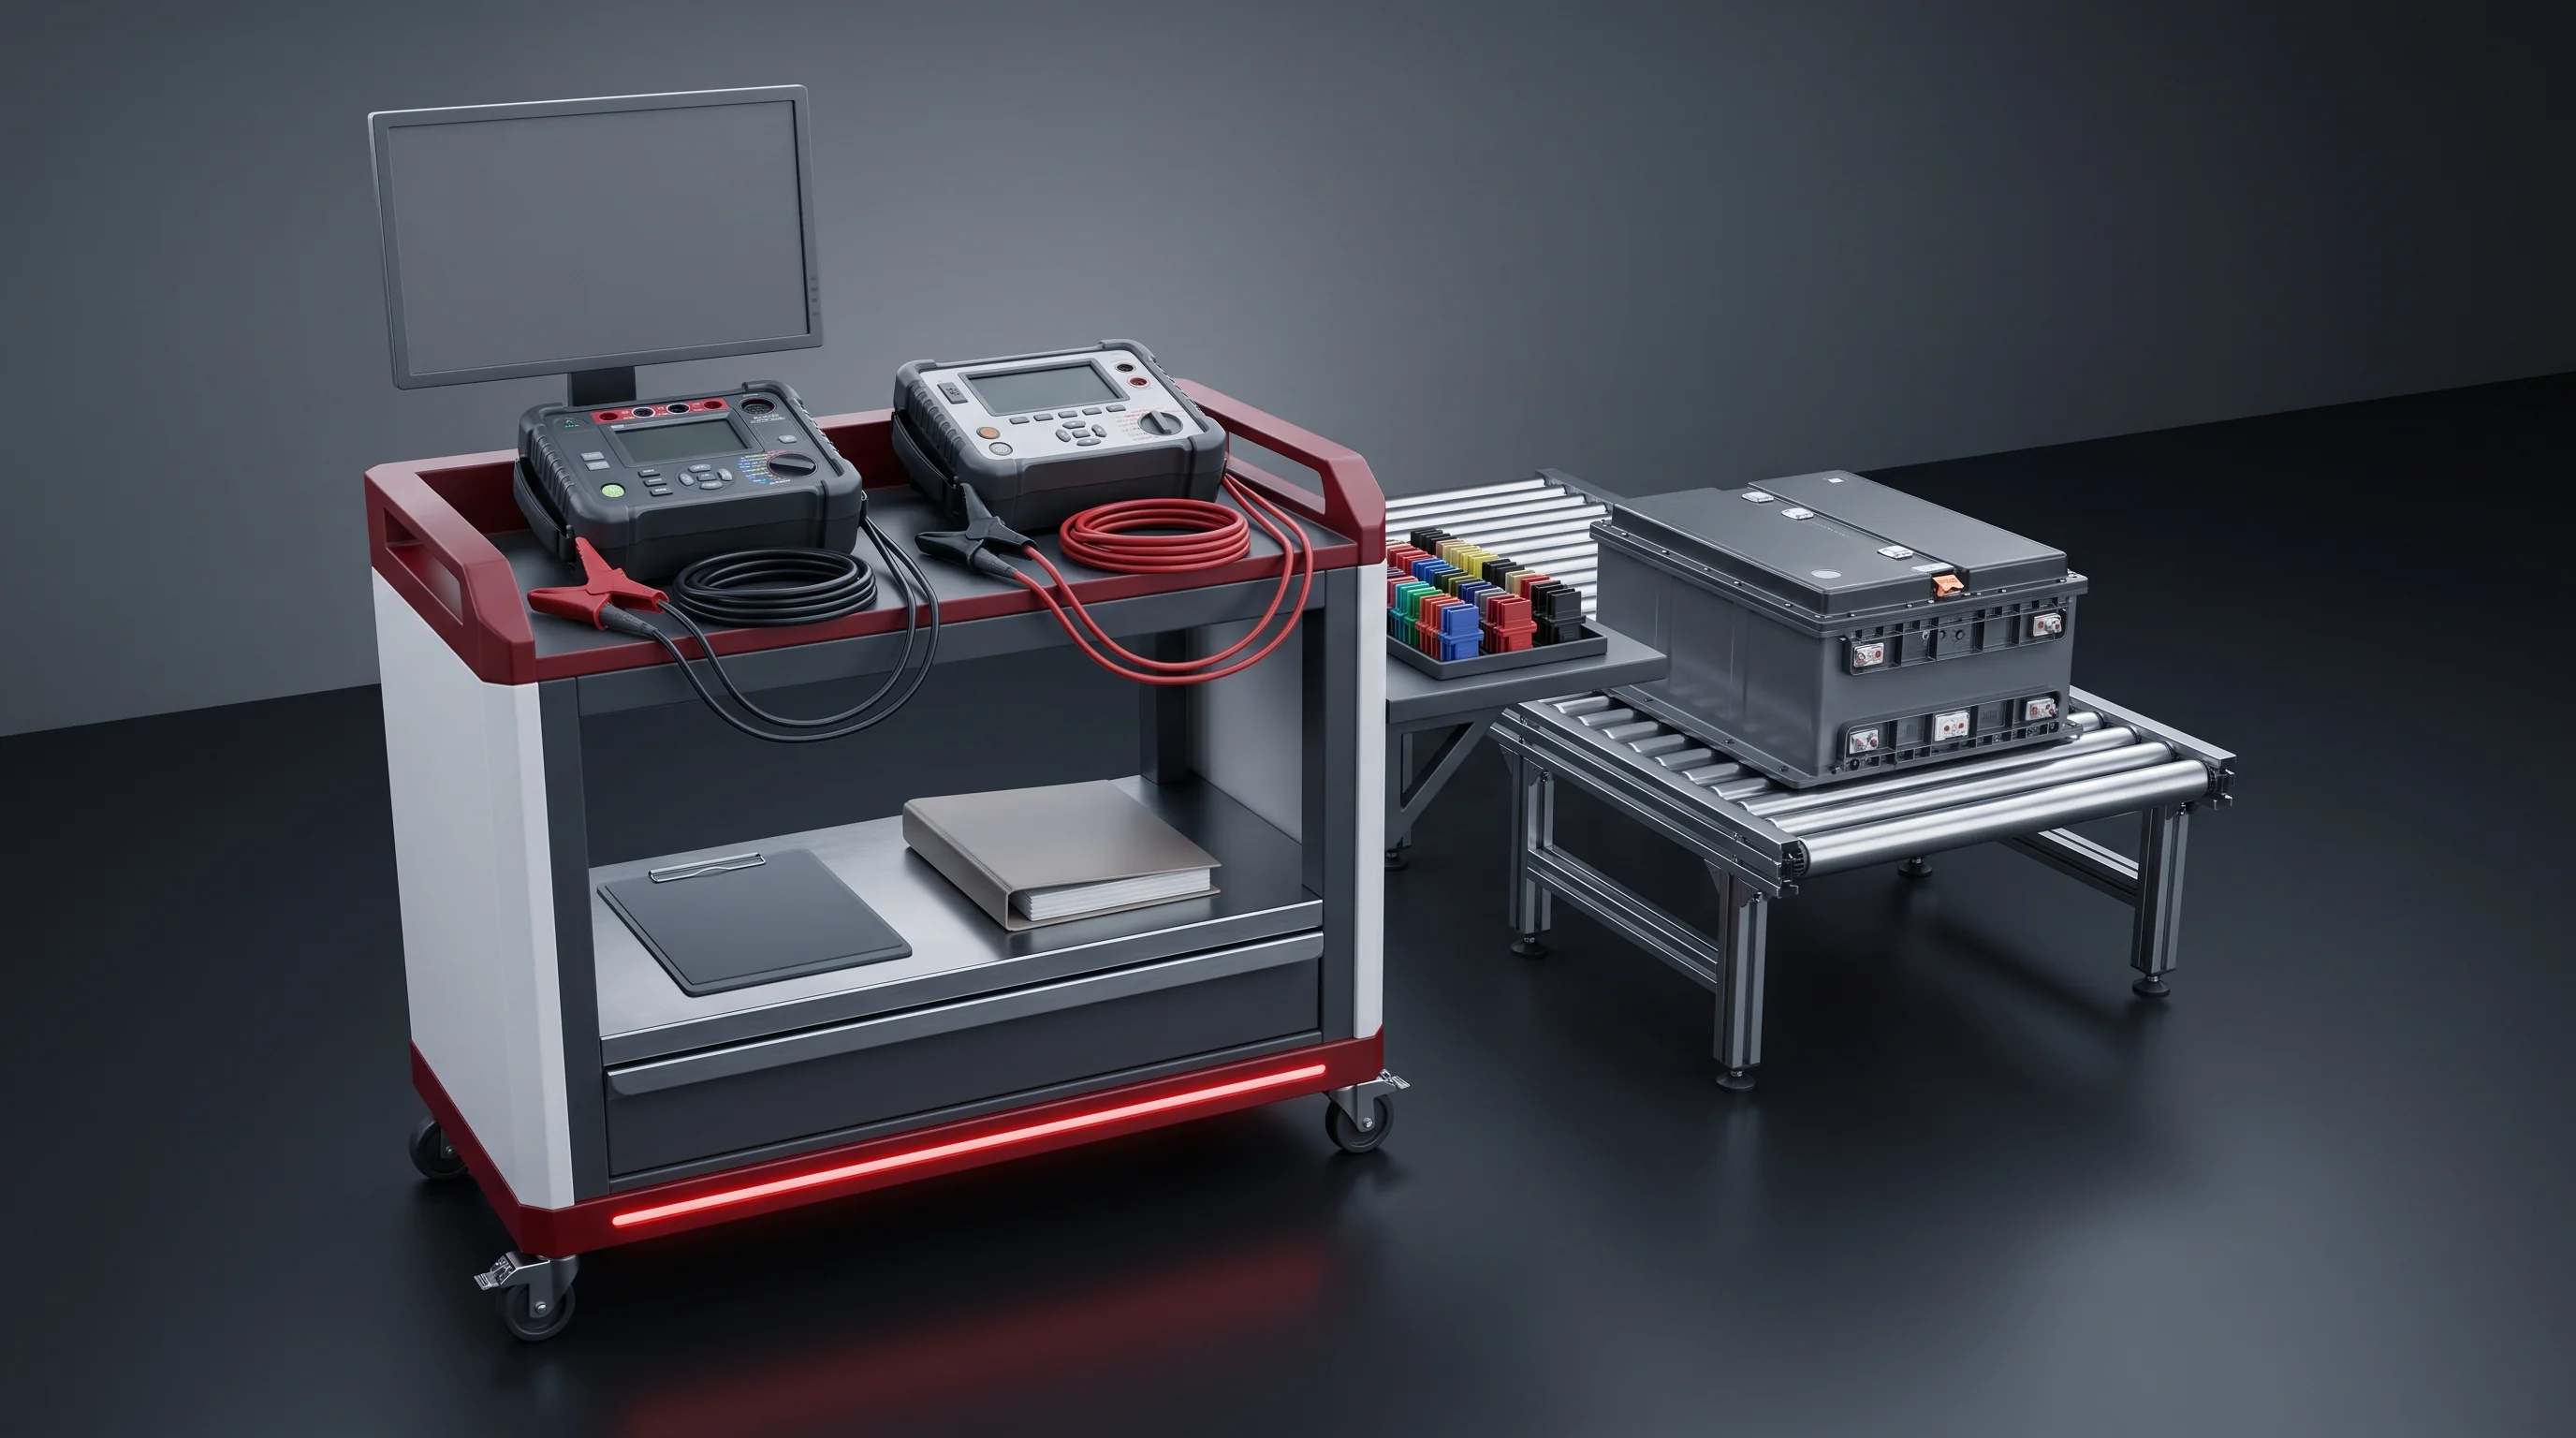
Acceptance bench where measured values are written beside the criteria they are judged against
Measured values beside their criterion.
  • Send your cell drawing, configuration and takt two weeks ahead and a bay is set up for your visit.
  • Wear parts ship within 48 hours; remote diagnostics connect for fault work.
  • Acceptance step by step on the FAT and SAT page; the team on about.

How to reach you

[email protected]

Start a project

Battery Manufacturing Equipment List In 24 Hours

Four lines to our engineering team and an equipment list naming each machine, its position in the two sequences, and whether this is one station, a segment or a complete line comes back within 24 hours.

Phone / WhatsApp
Address
Wuhan, Hubei, China
Response
Within 24 hours