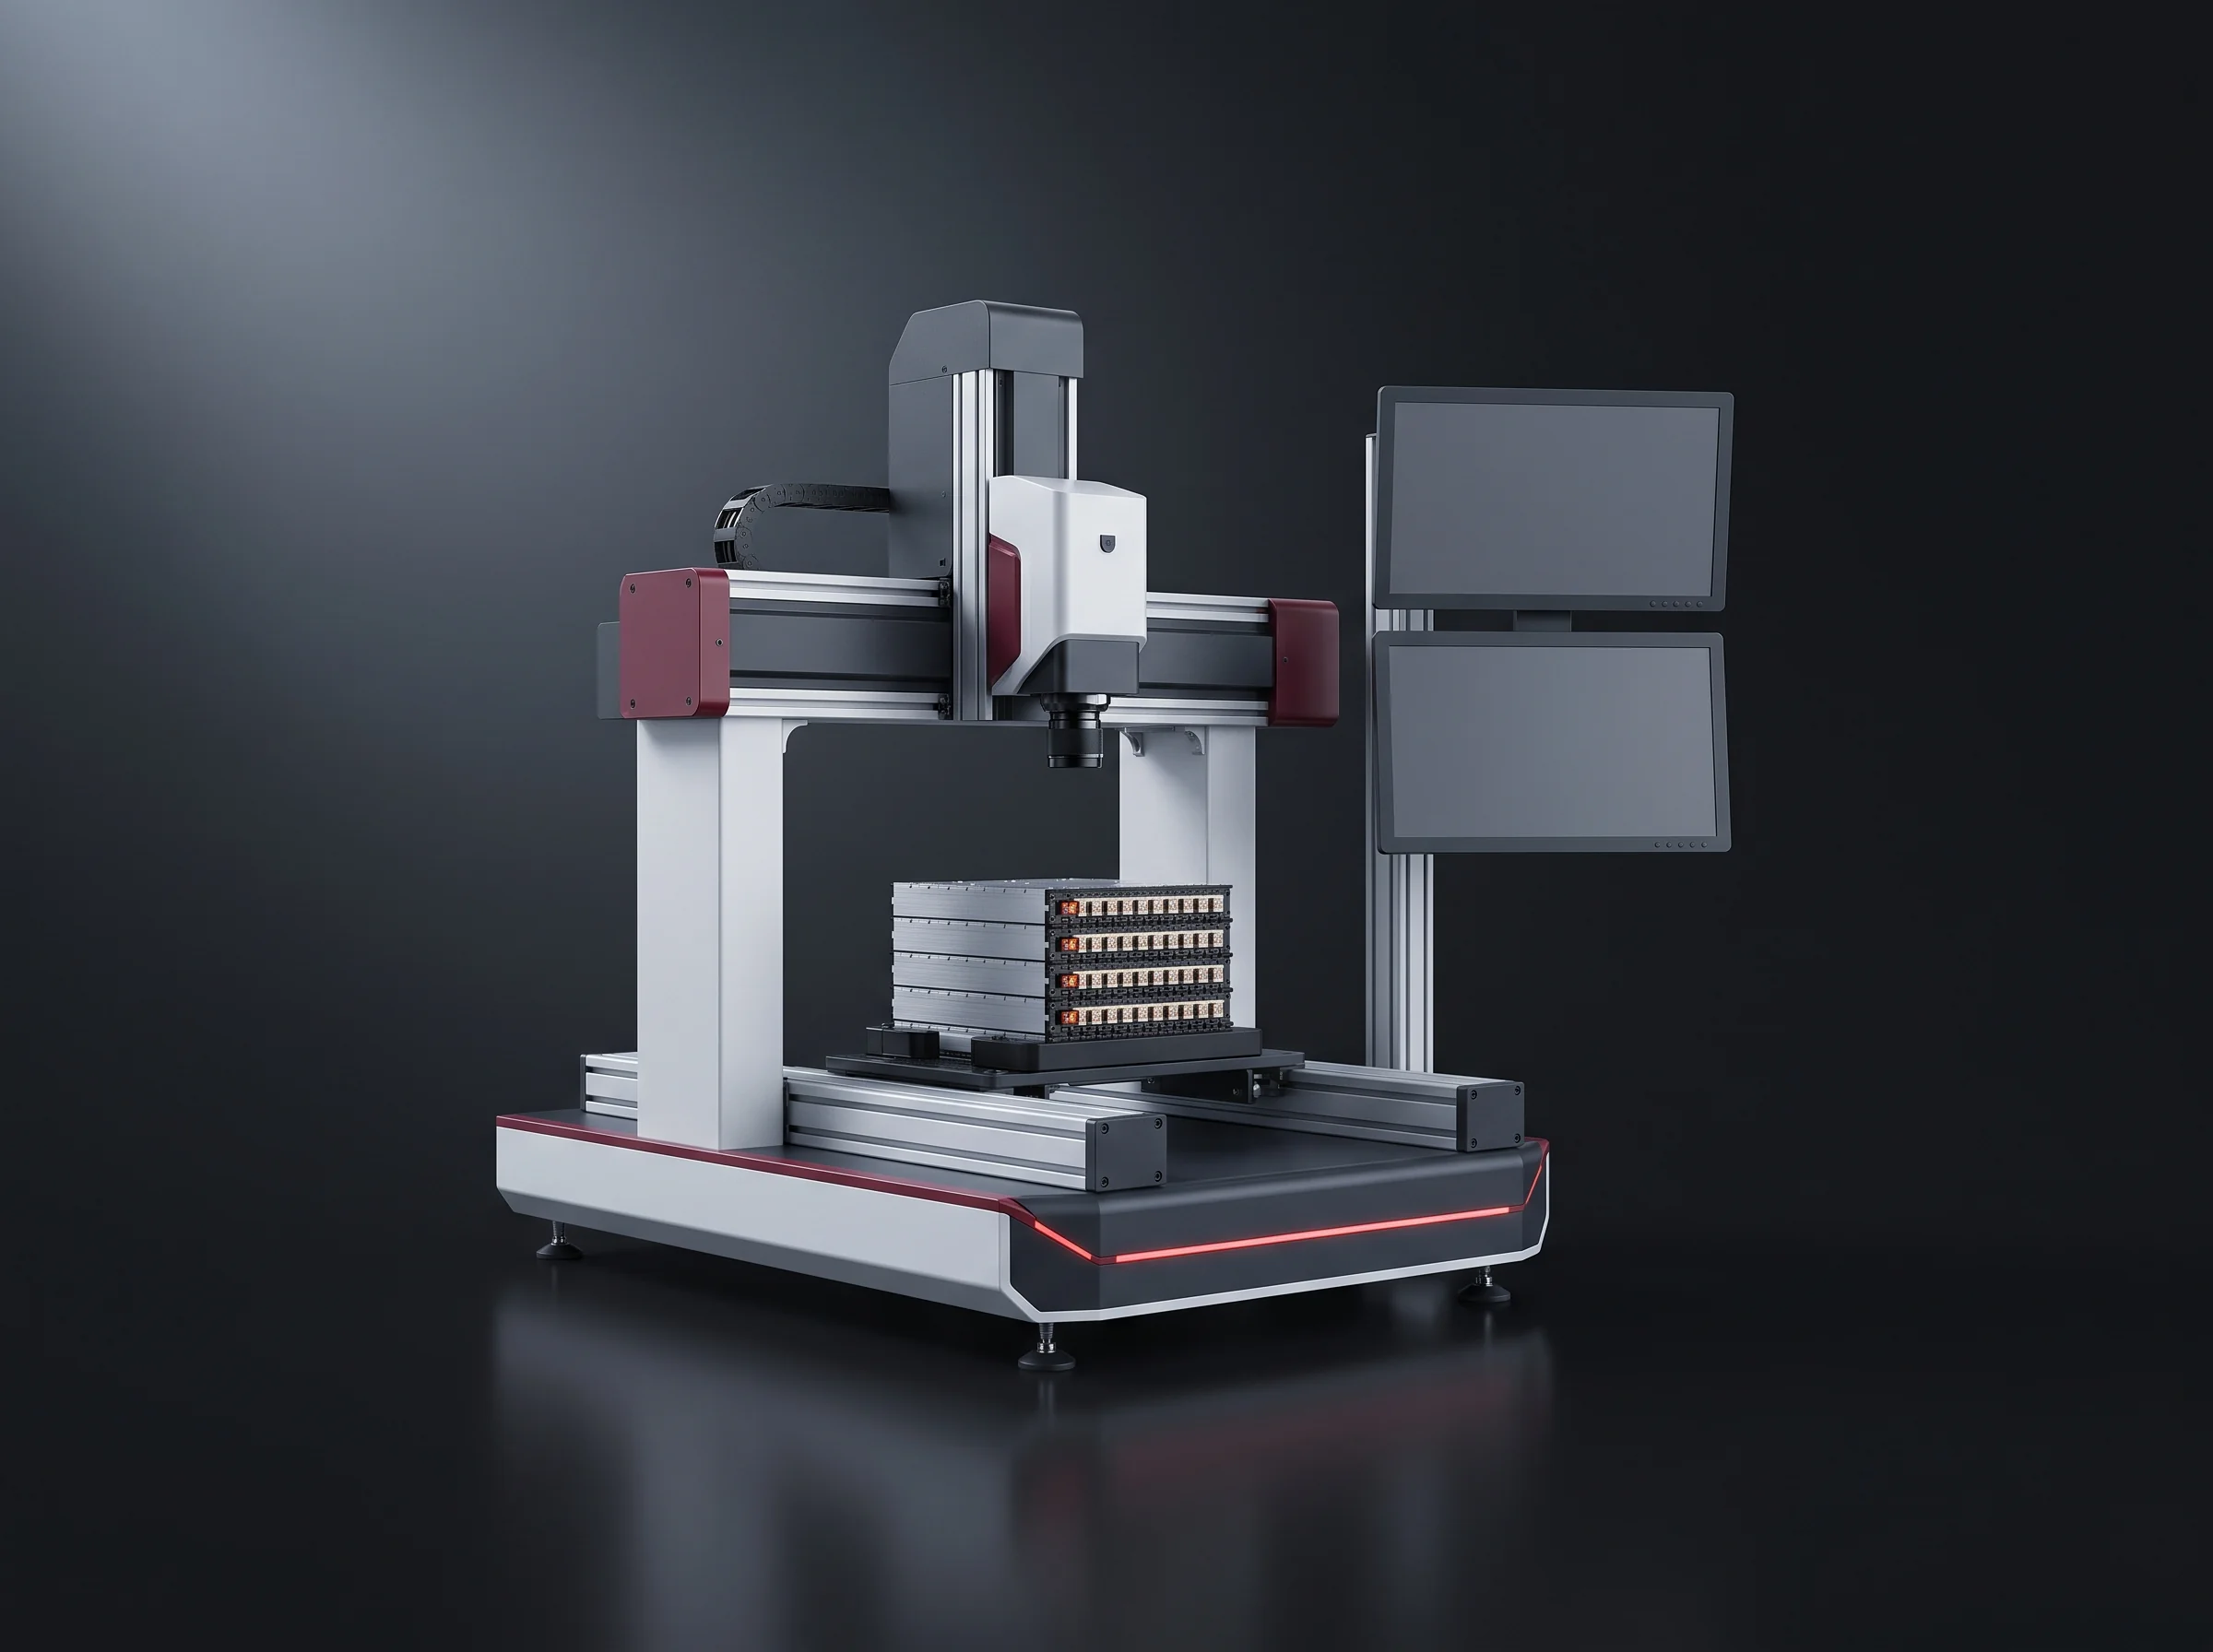
STATION 11
Terminal addressing
BLP-AD vision at 200–300 mm/s locates every terminal to ≤±0.2 mm, checks polarity, laser-cleans the faces.
AUTO
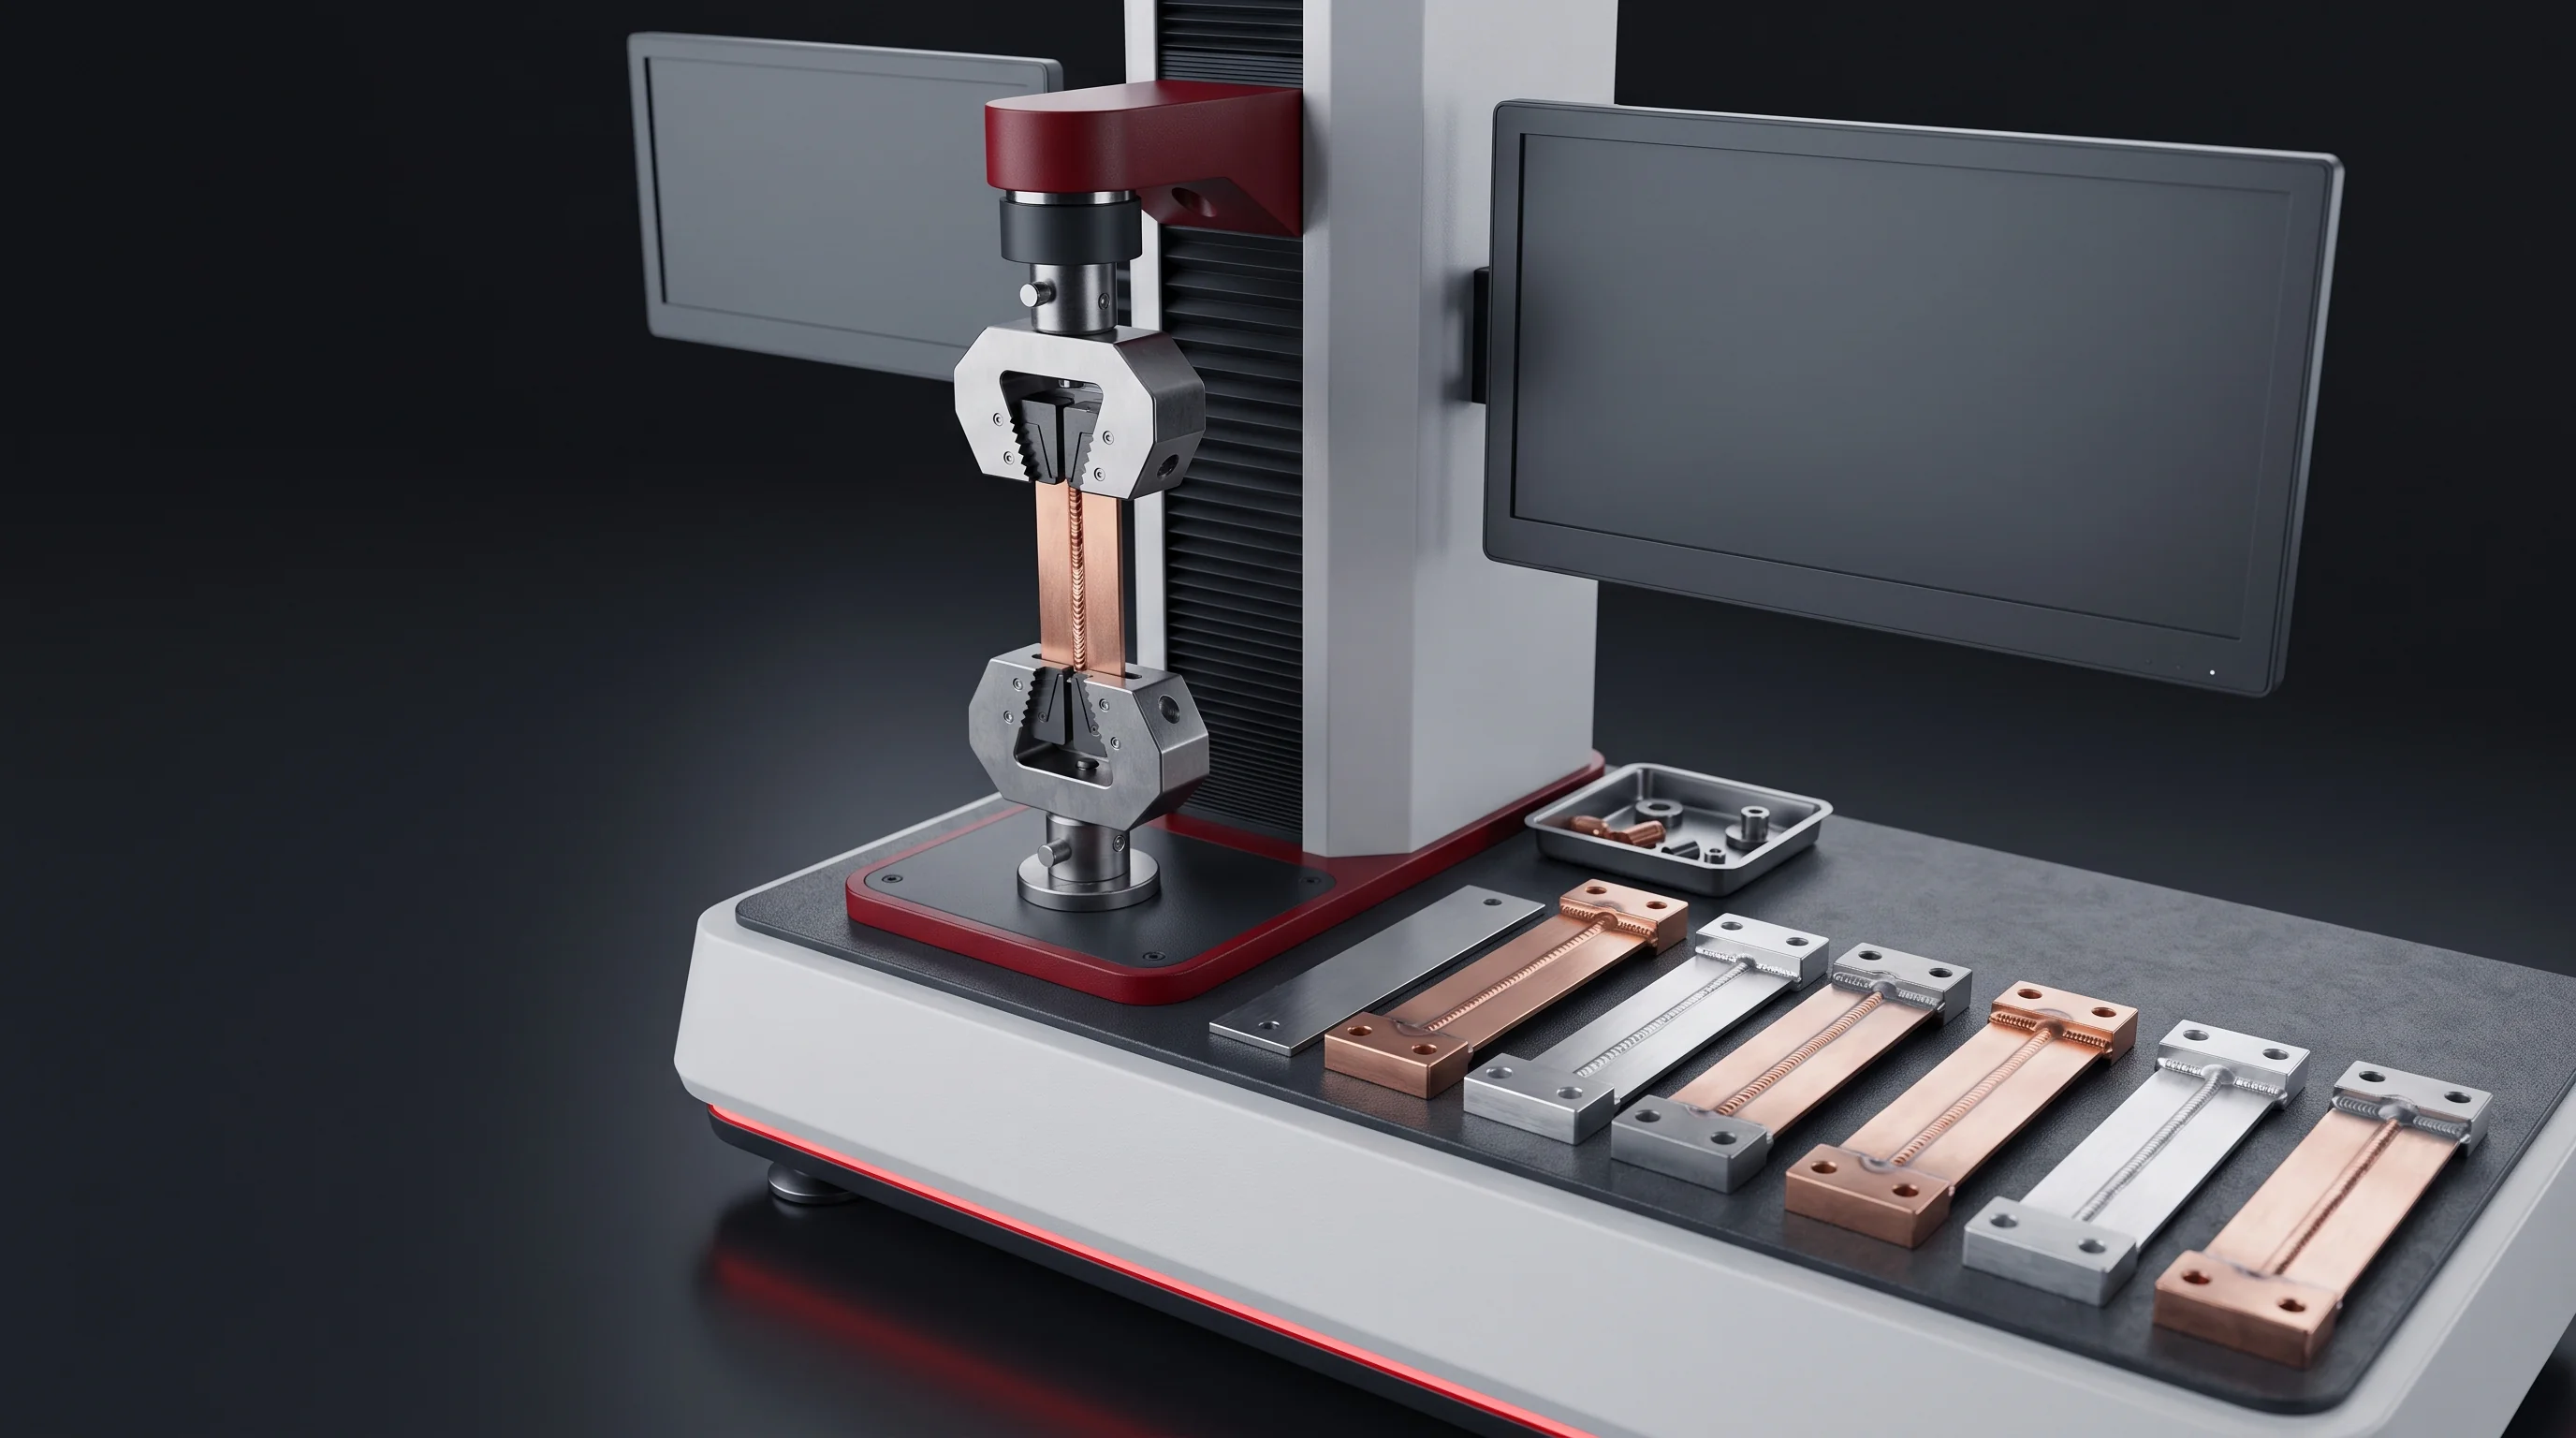
BLP-W6 — station 13 of seventeen, in-line
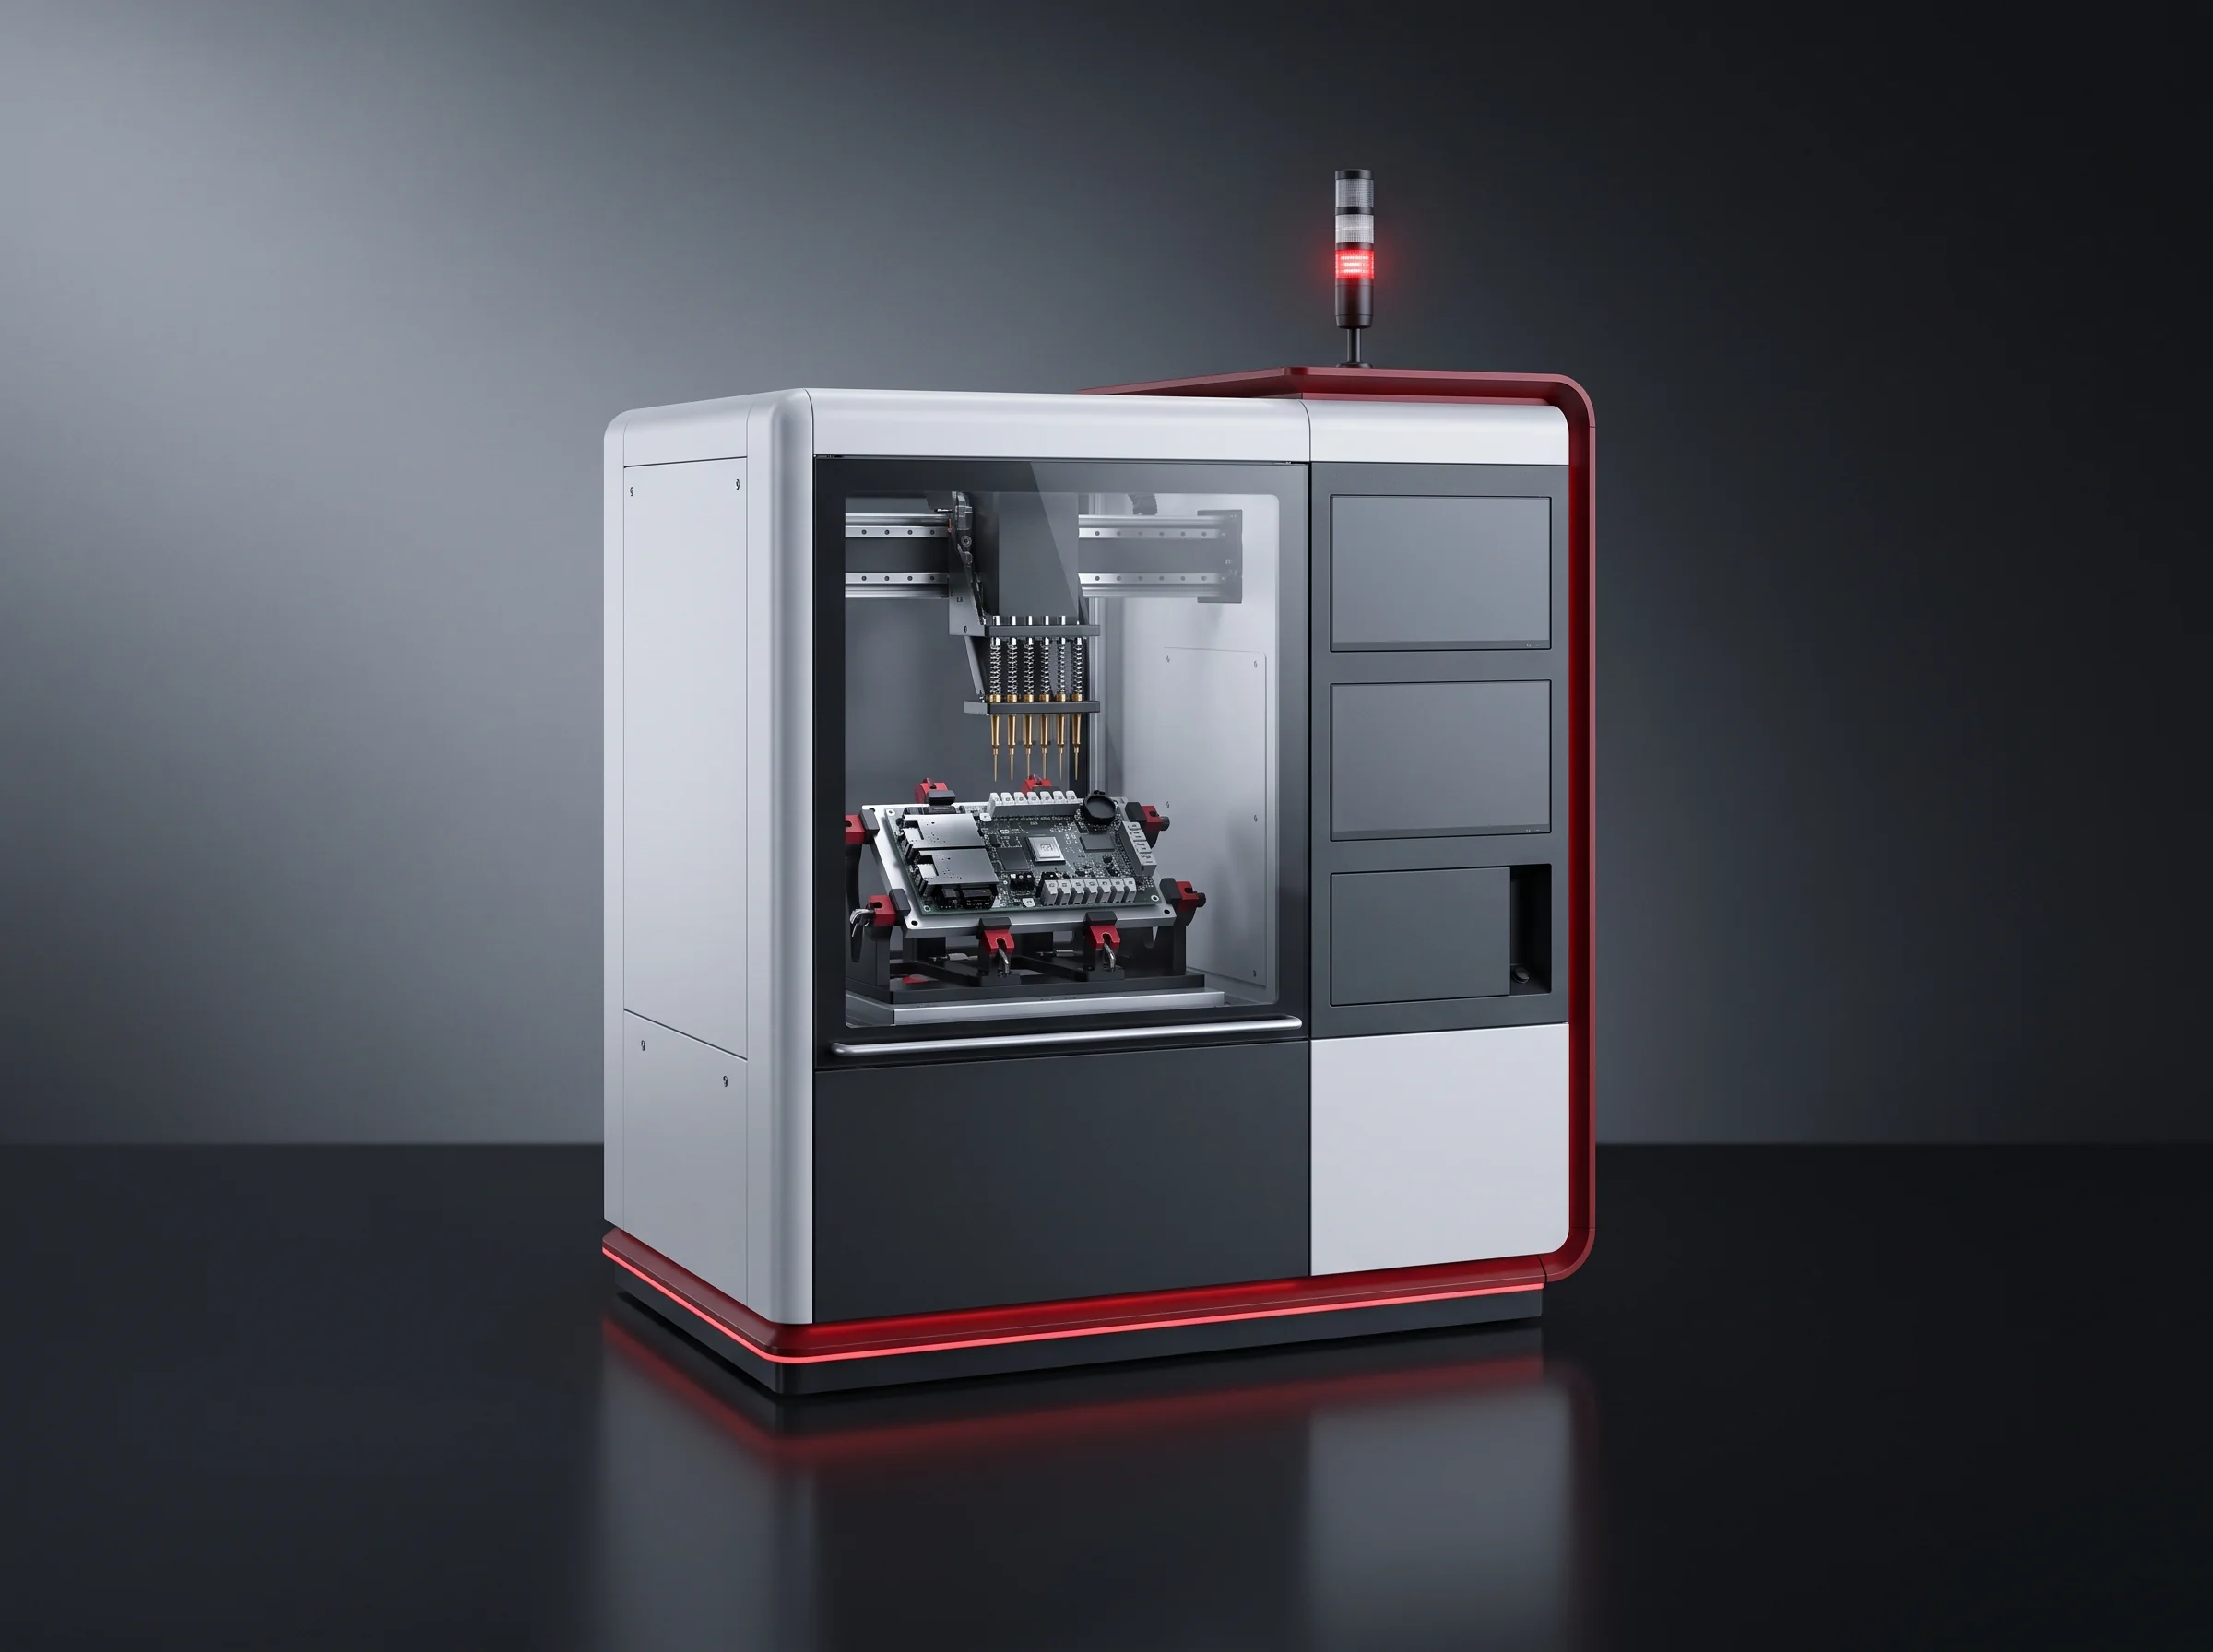
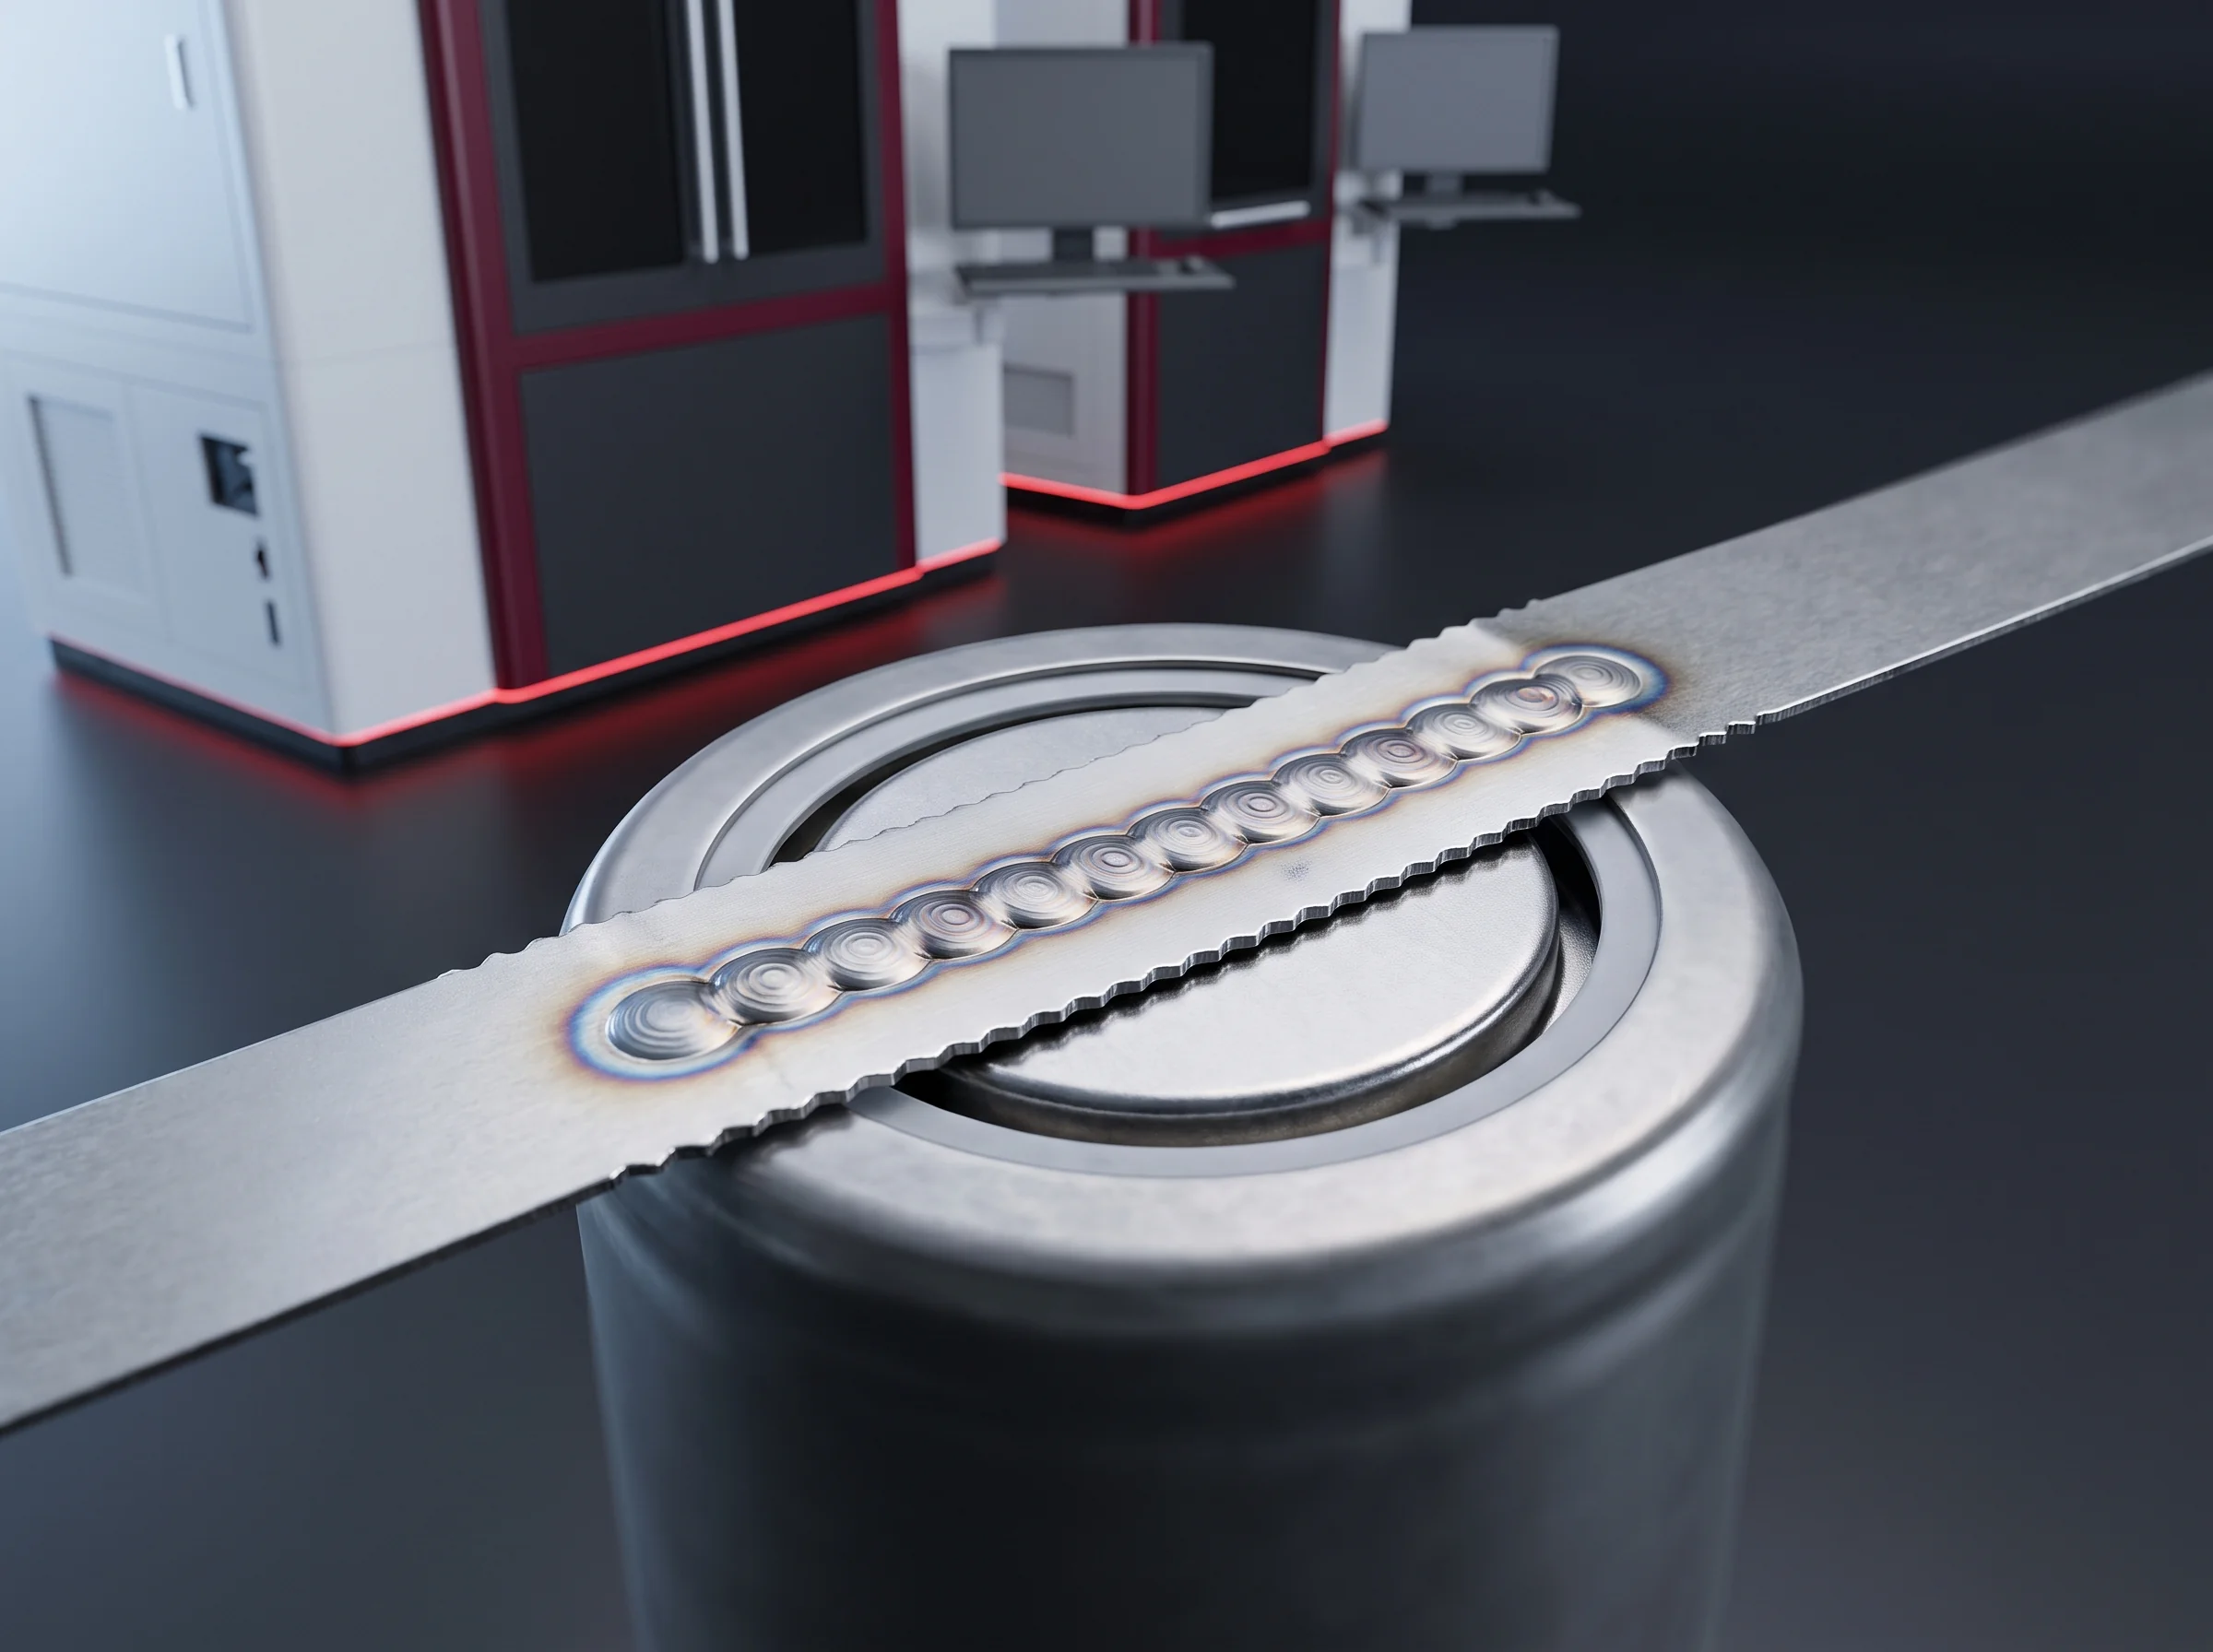
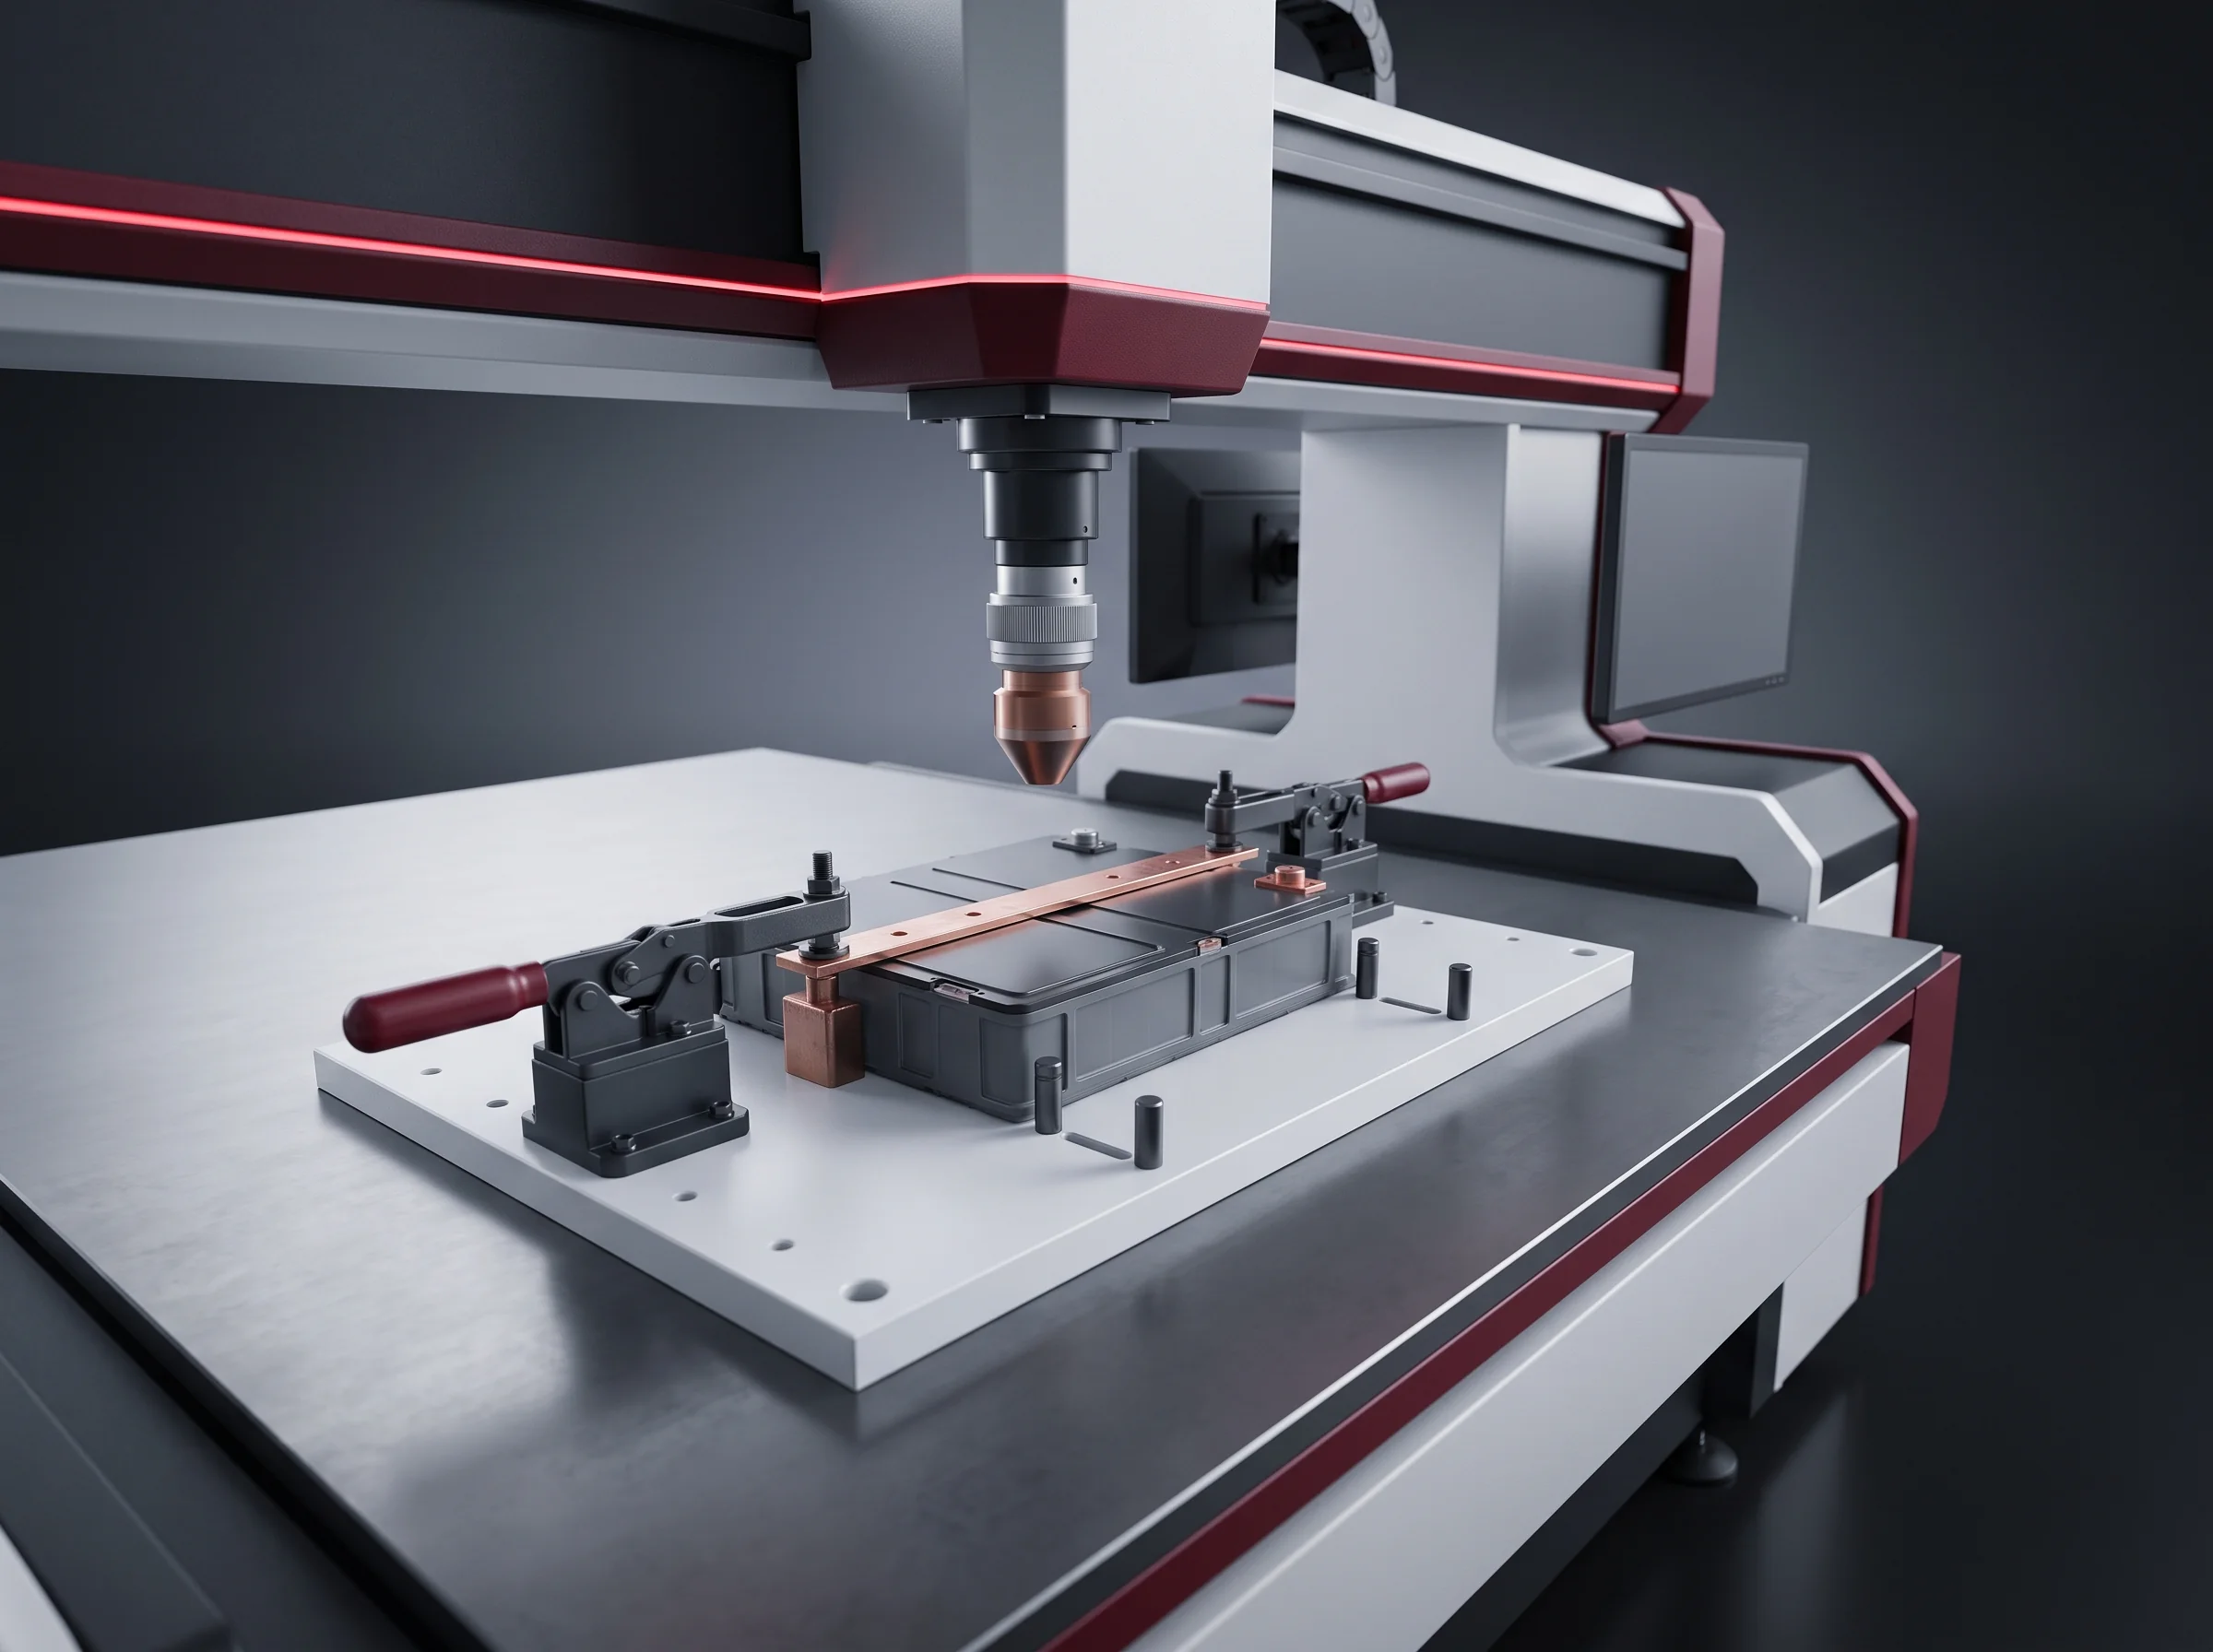
A three-axis gantry carries a galvanometer scanner over a 6 kW source and welds every busbar joint on a module that never leaves its carrier. What the surface hides — 1.0 mm of fusion under a 1.5 mm seam — is sectioned, pulled and written to the module number.
In-line, on the carrier
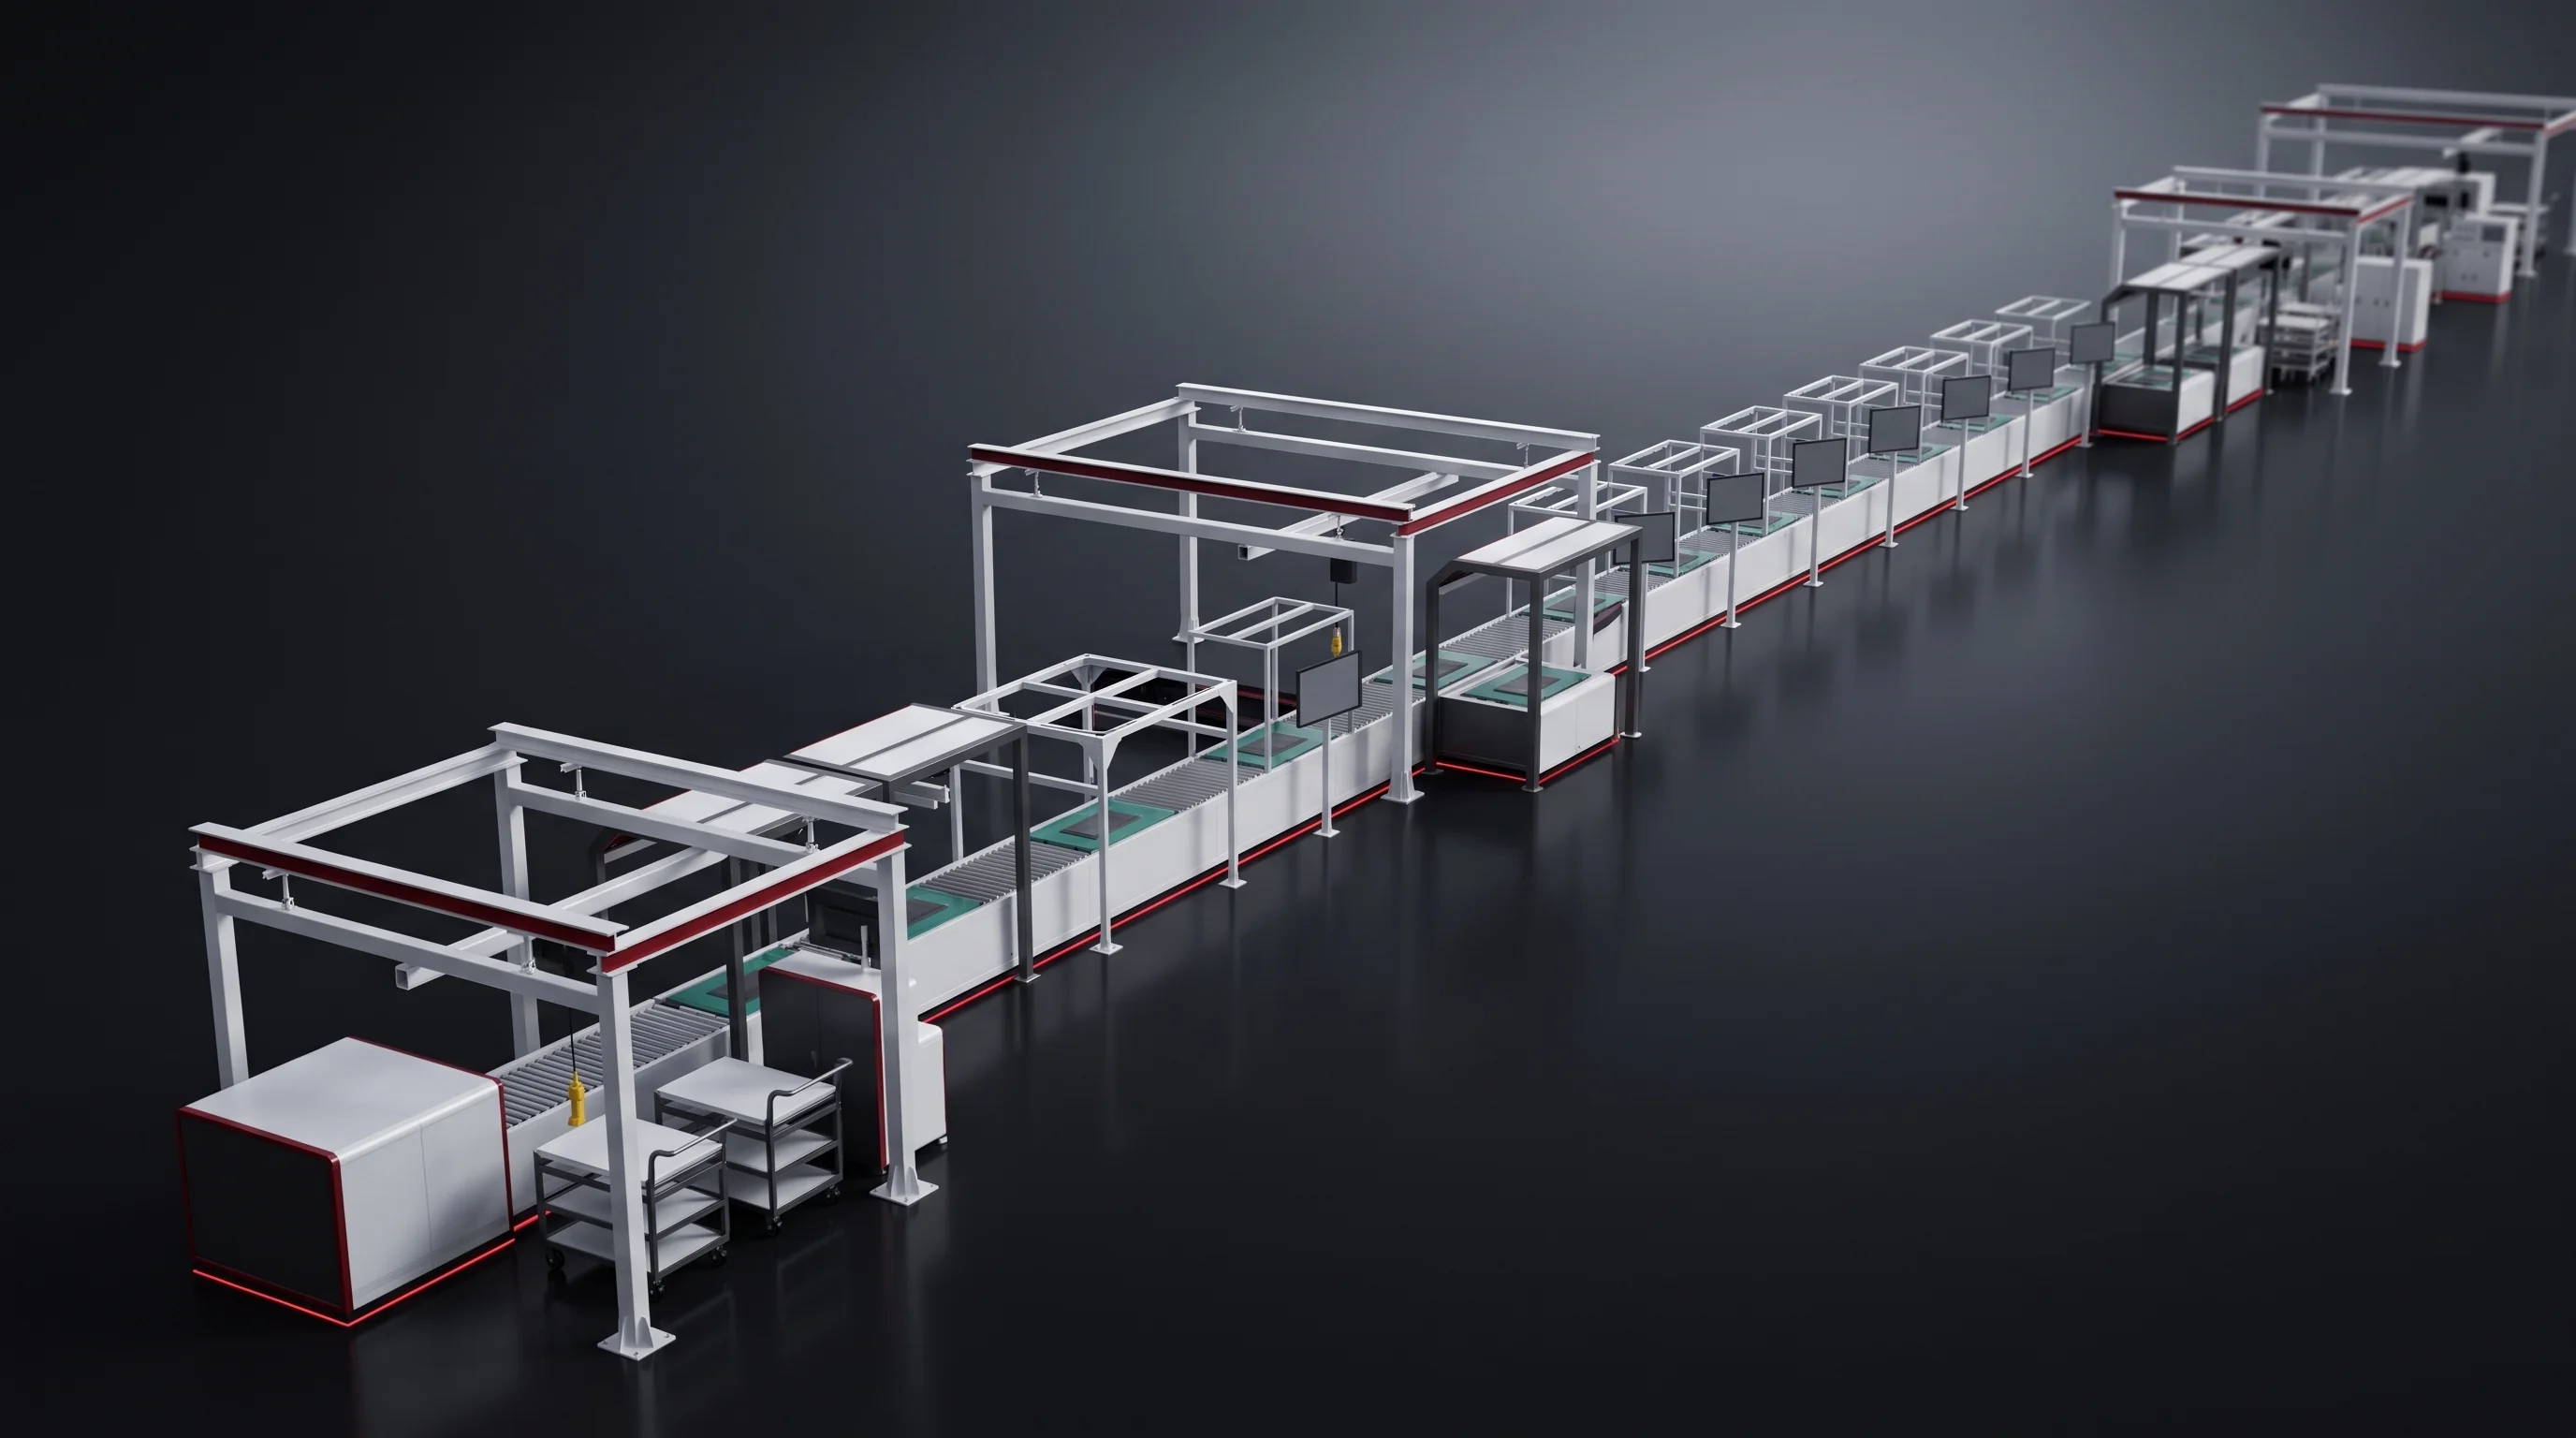
BLP-W6 is station 13 of the seventeen in the module segment. The module arrives located on its carrier, the gantry carries the scanner across it, each joint is welded where the station was told it would be, and the module continues to station 14 on the same carrier. Nothing is lifted, re-clamped or re-found in between.
Plants building a new module line, and engineering teams putting a busbar welding station into a line already running. Fully automatic on both configurations.
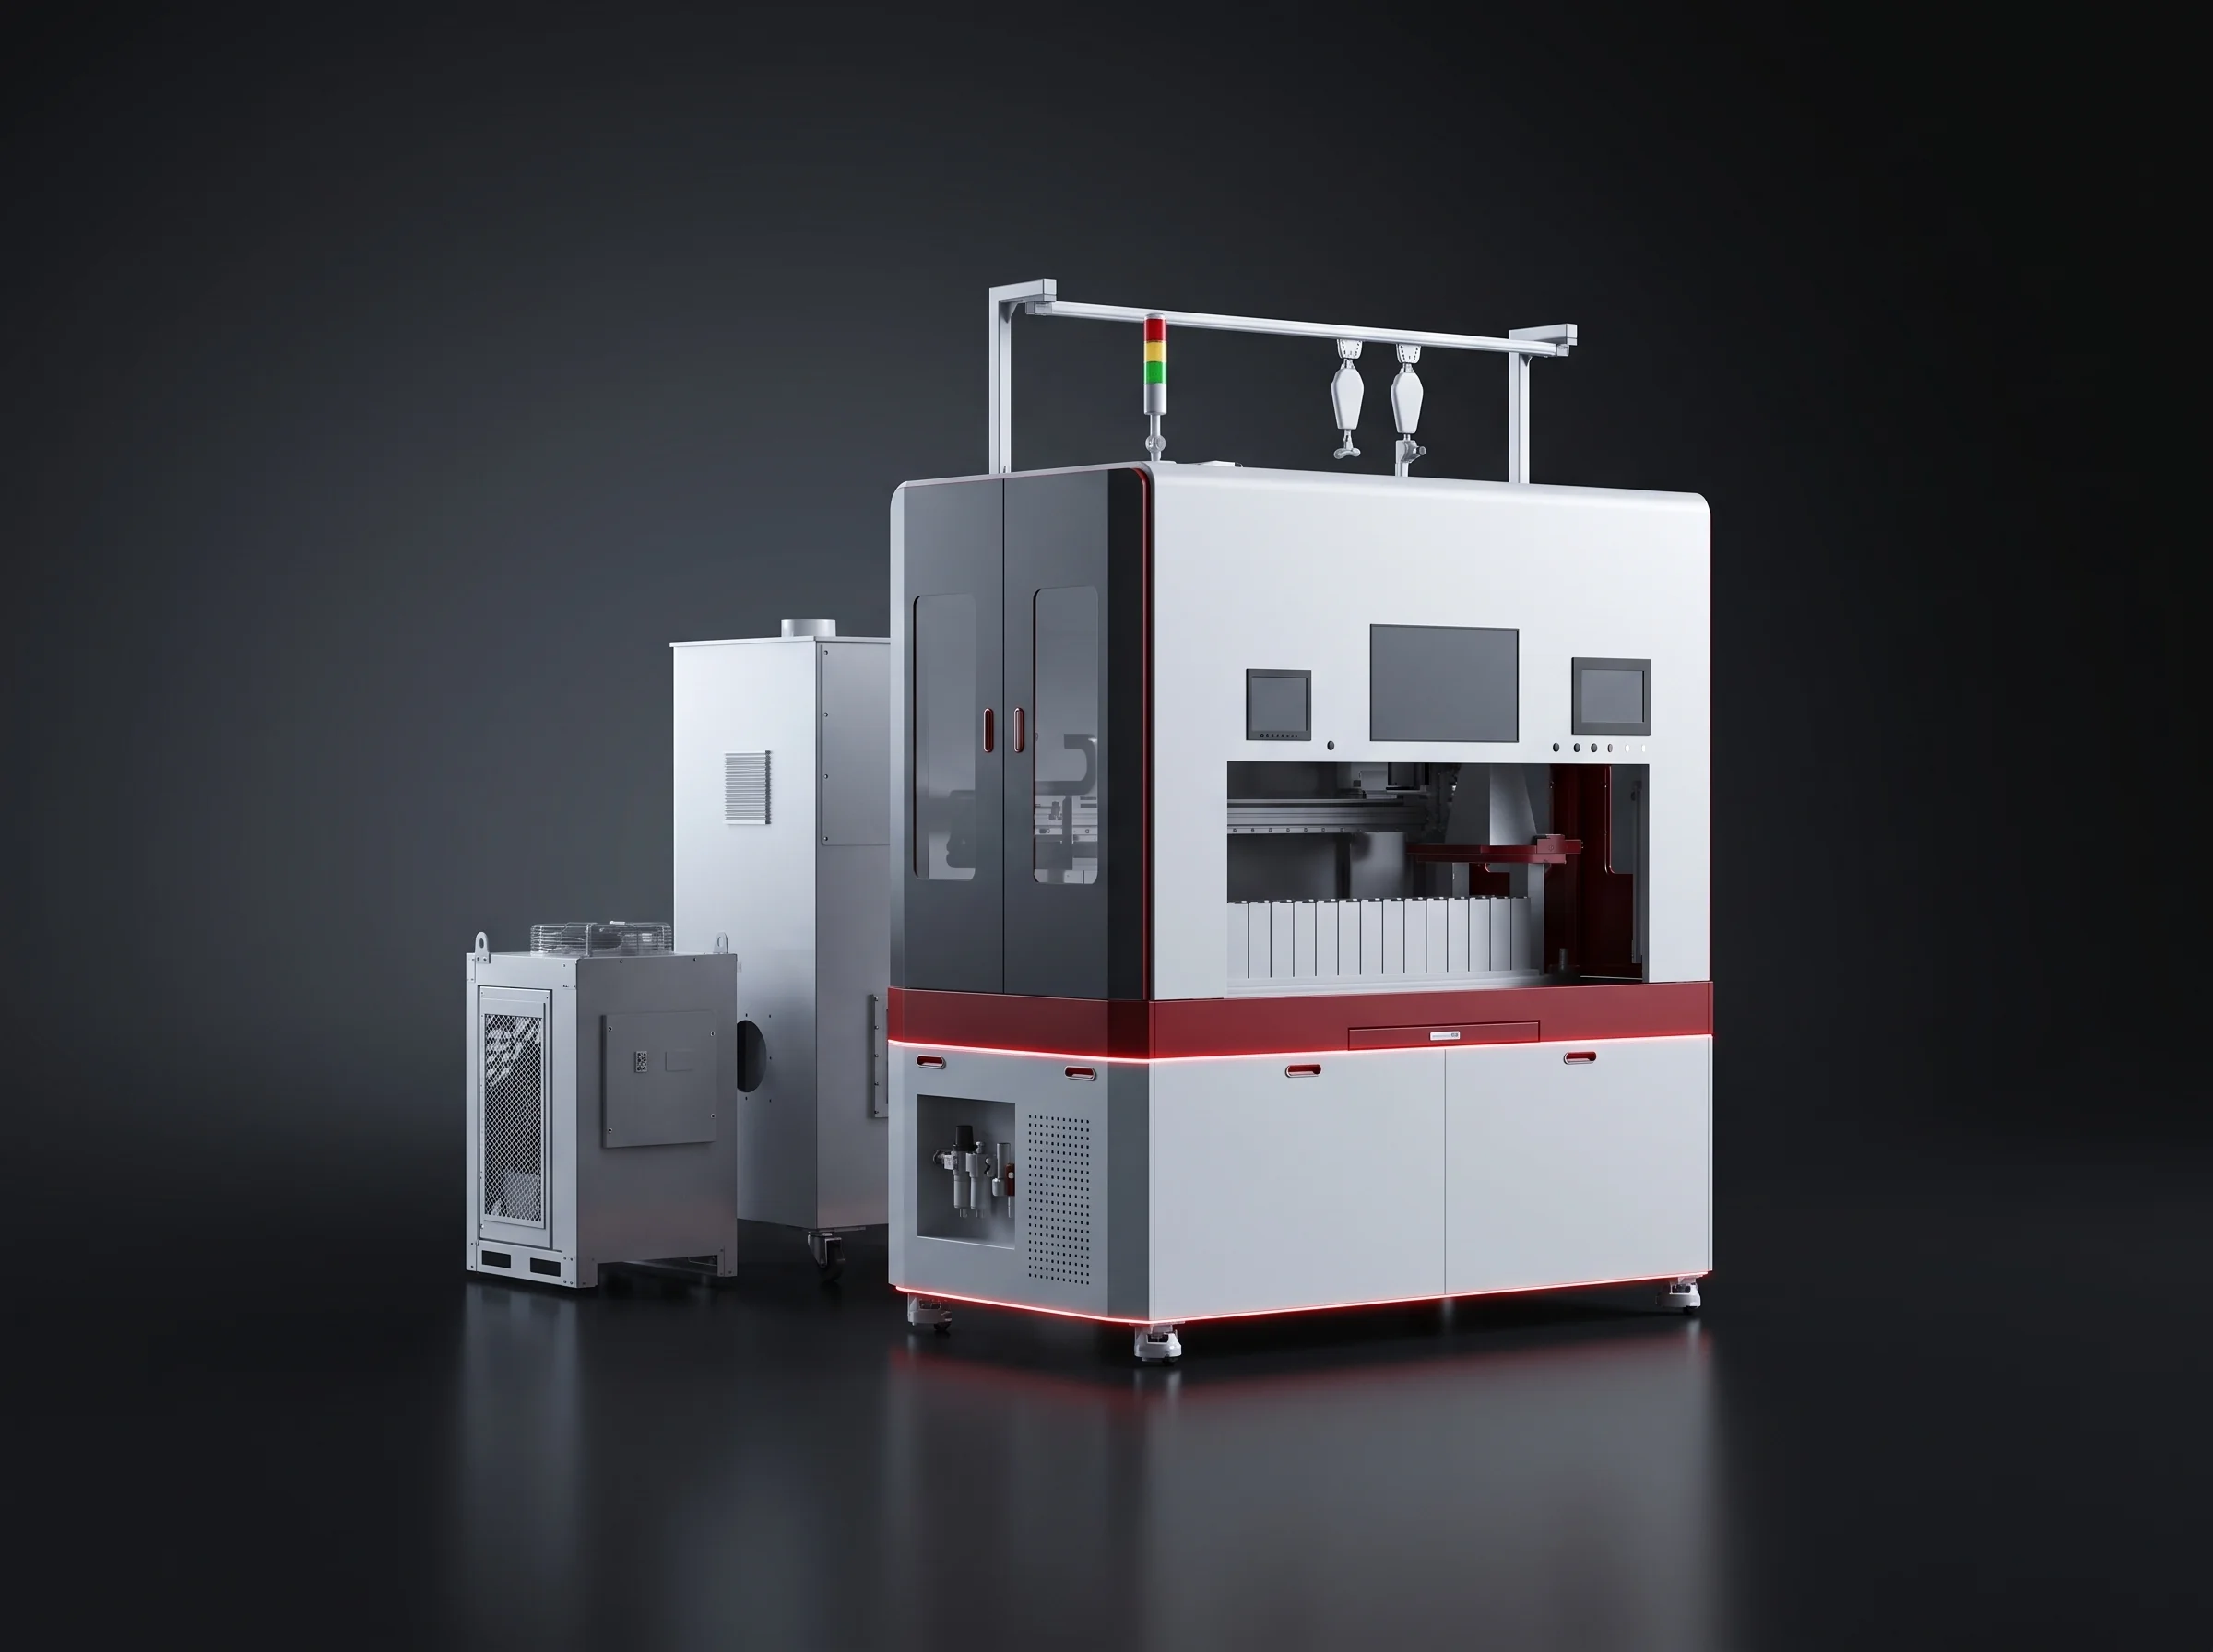
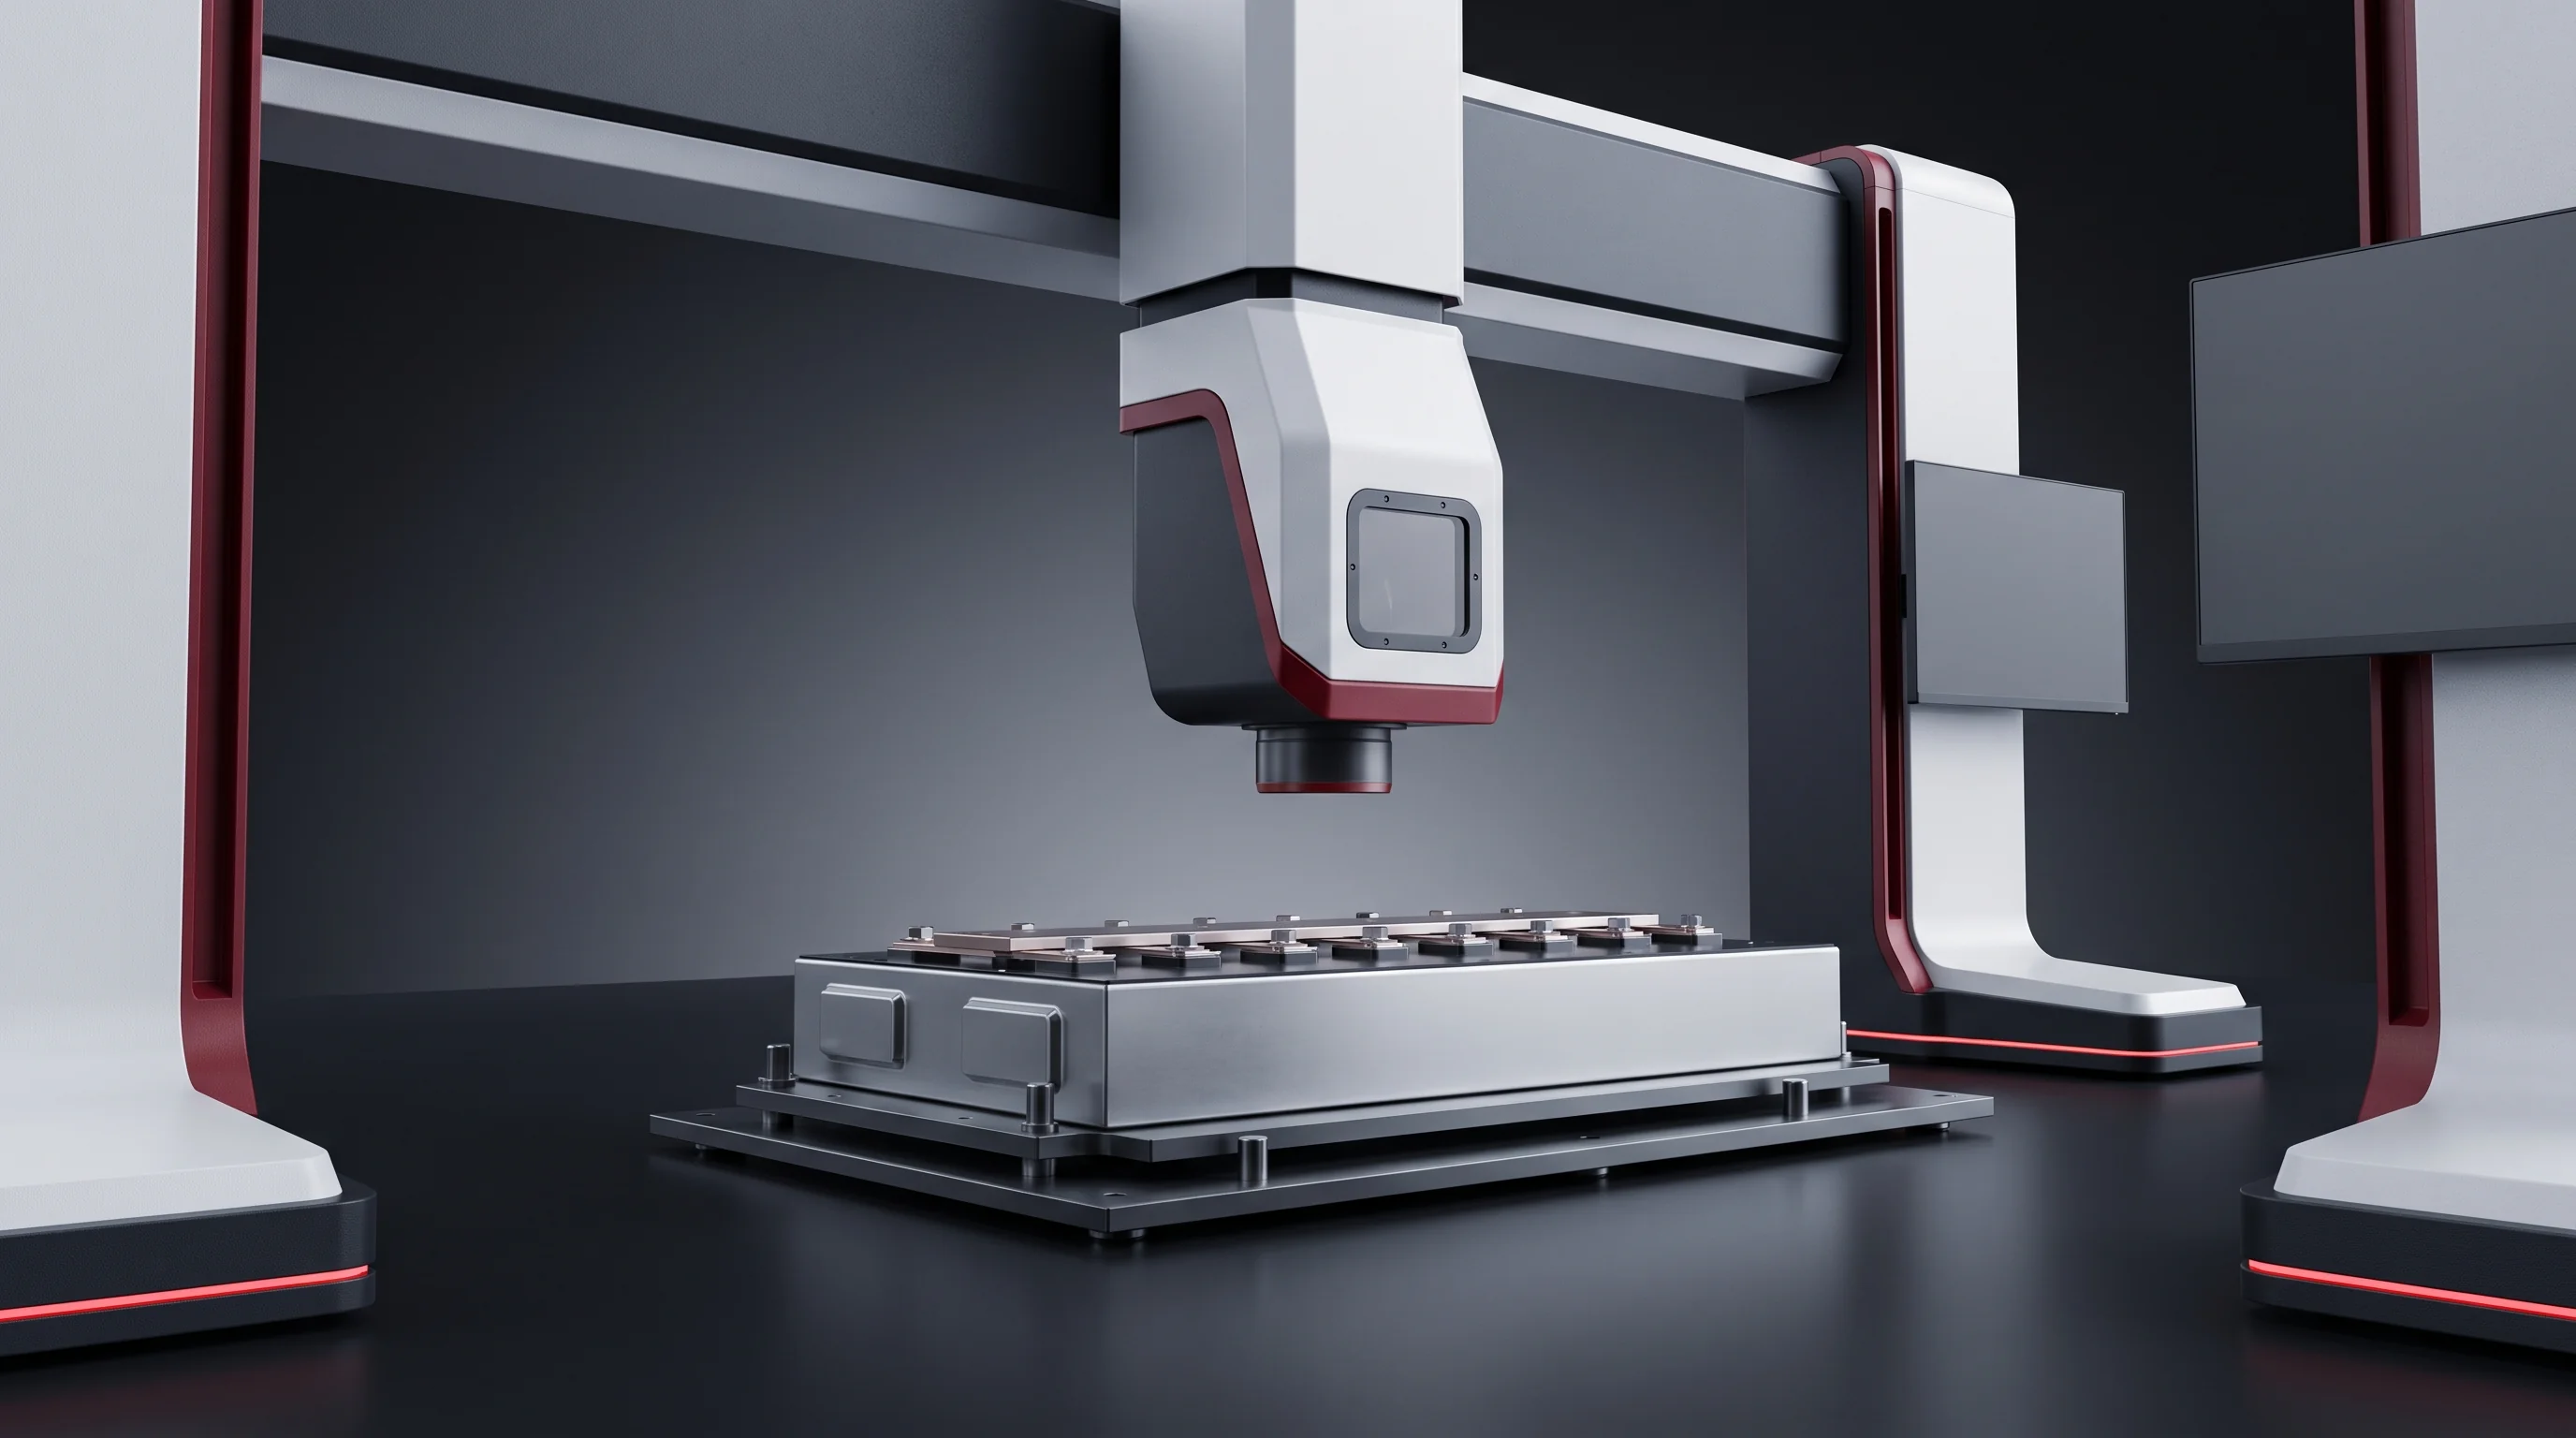
Stations 11 to 16
A busbar welder is bought as a machine and lives as a station. Almost everything it needs is decided before a module reaches it.
BLP-AD vision at 200–300 mm/s locates every terminal to ≤±0.2 mm, checks polarity, laser-cleans the faces.
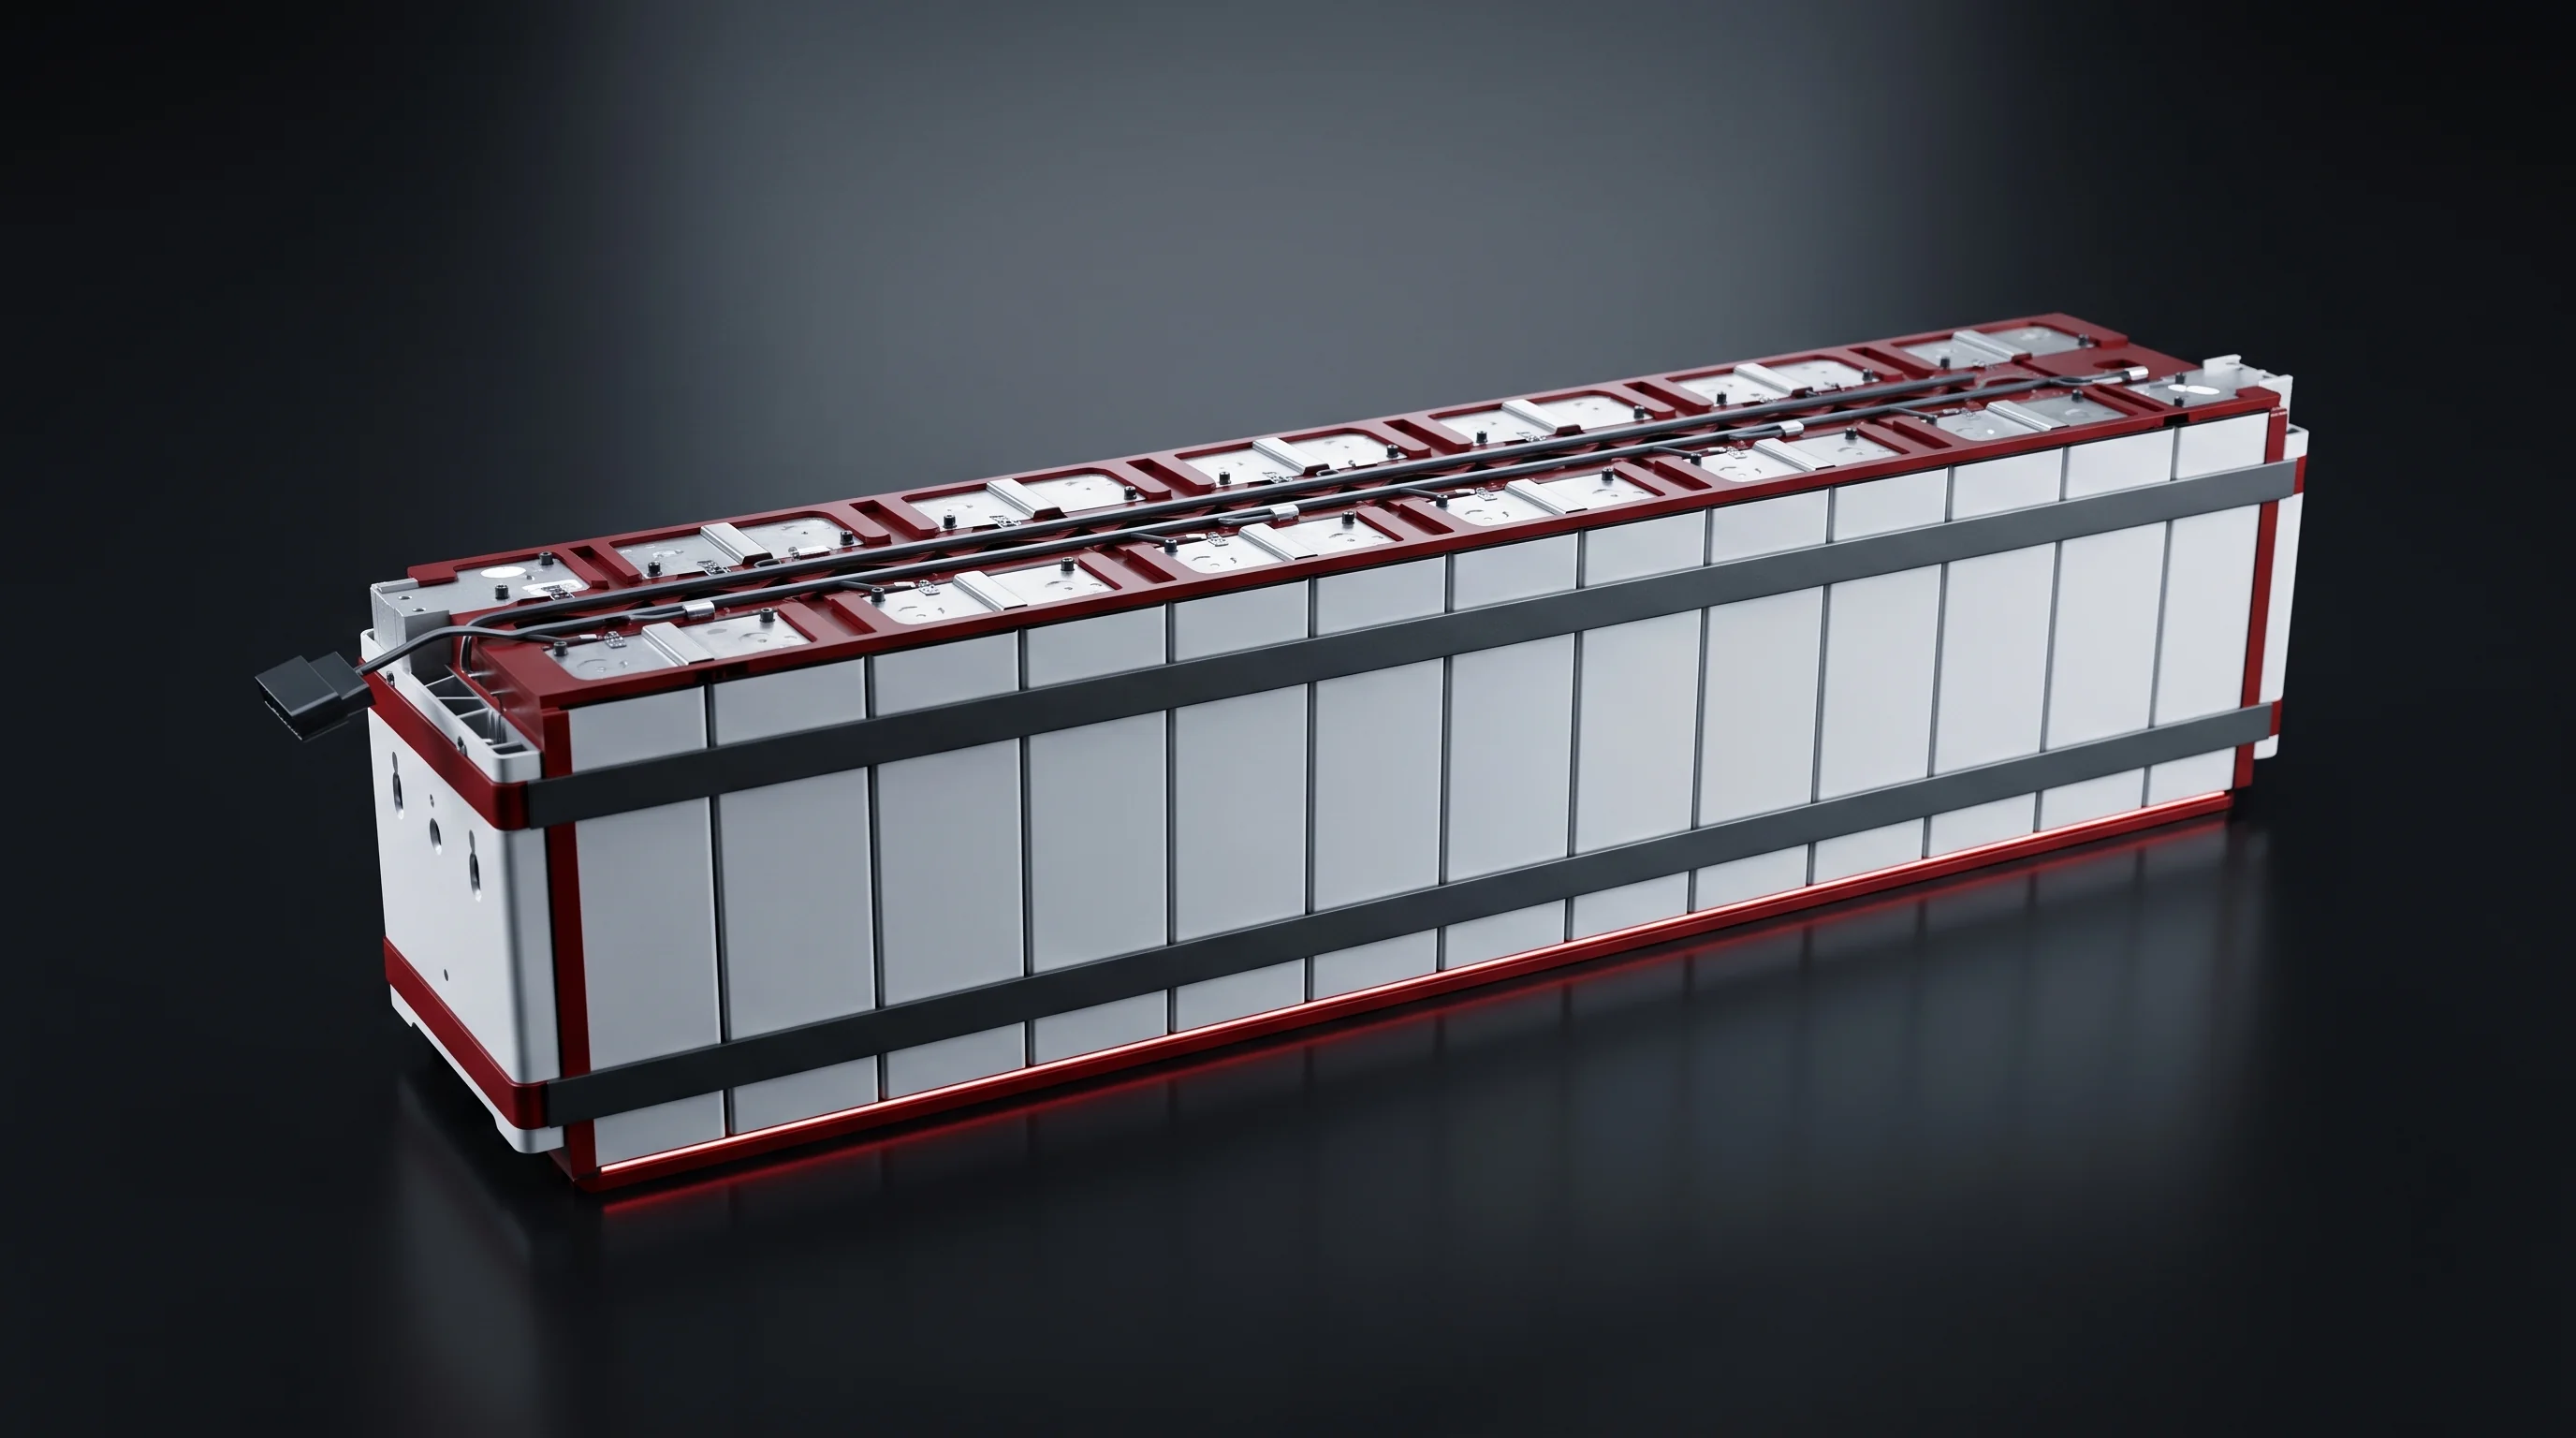
Busbar plate and CCS assembly seated on the module. Manual on the economy build, semi-automatic on the high-automation build.
Every joint welded on the carrier to the recipe of the part number; actuals recorded.
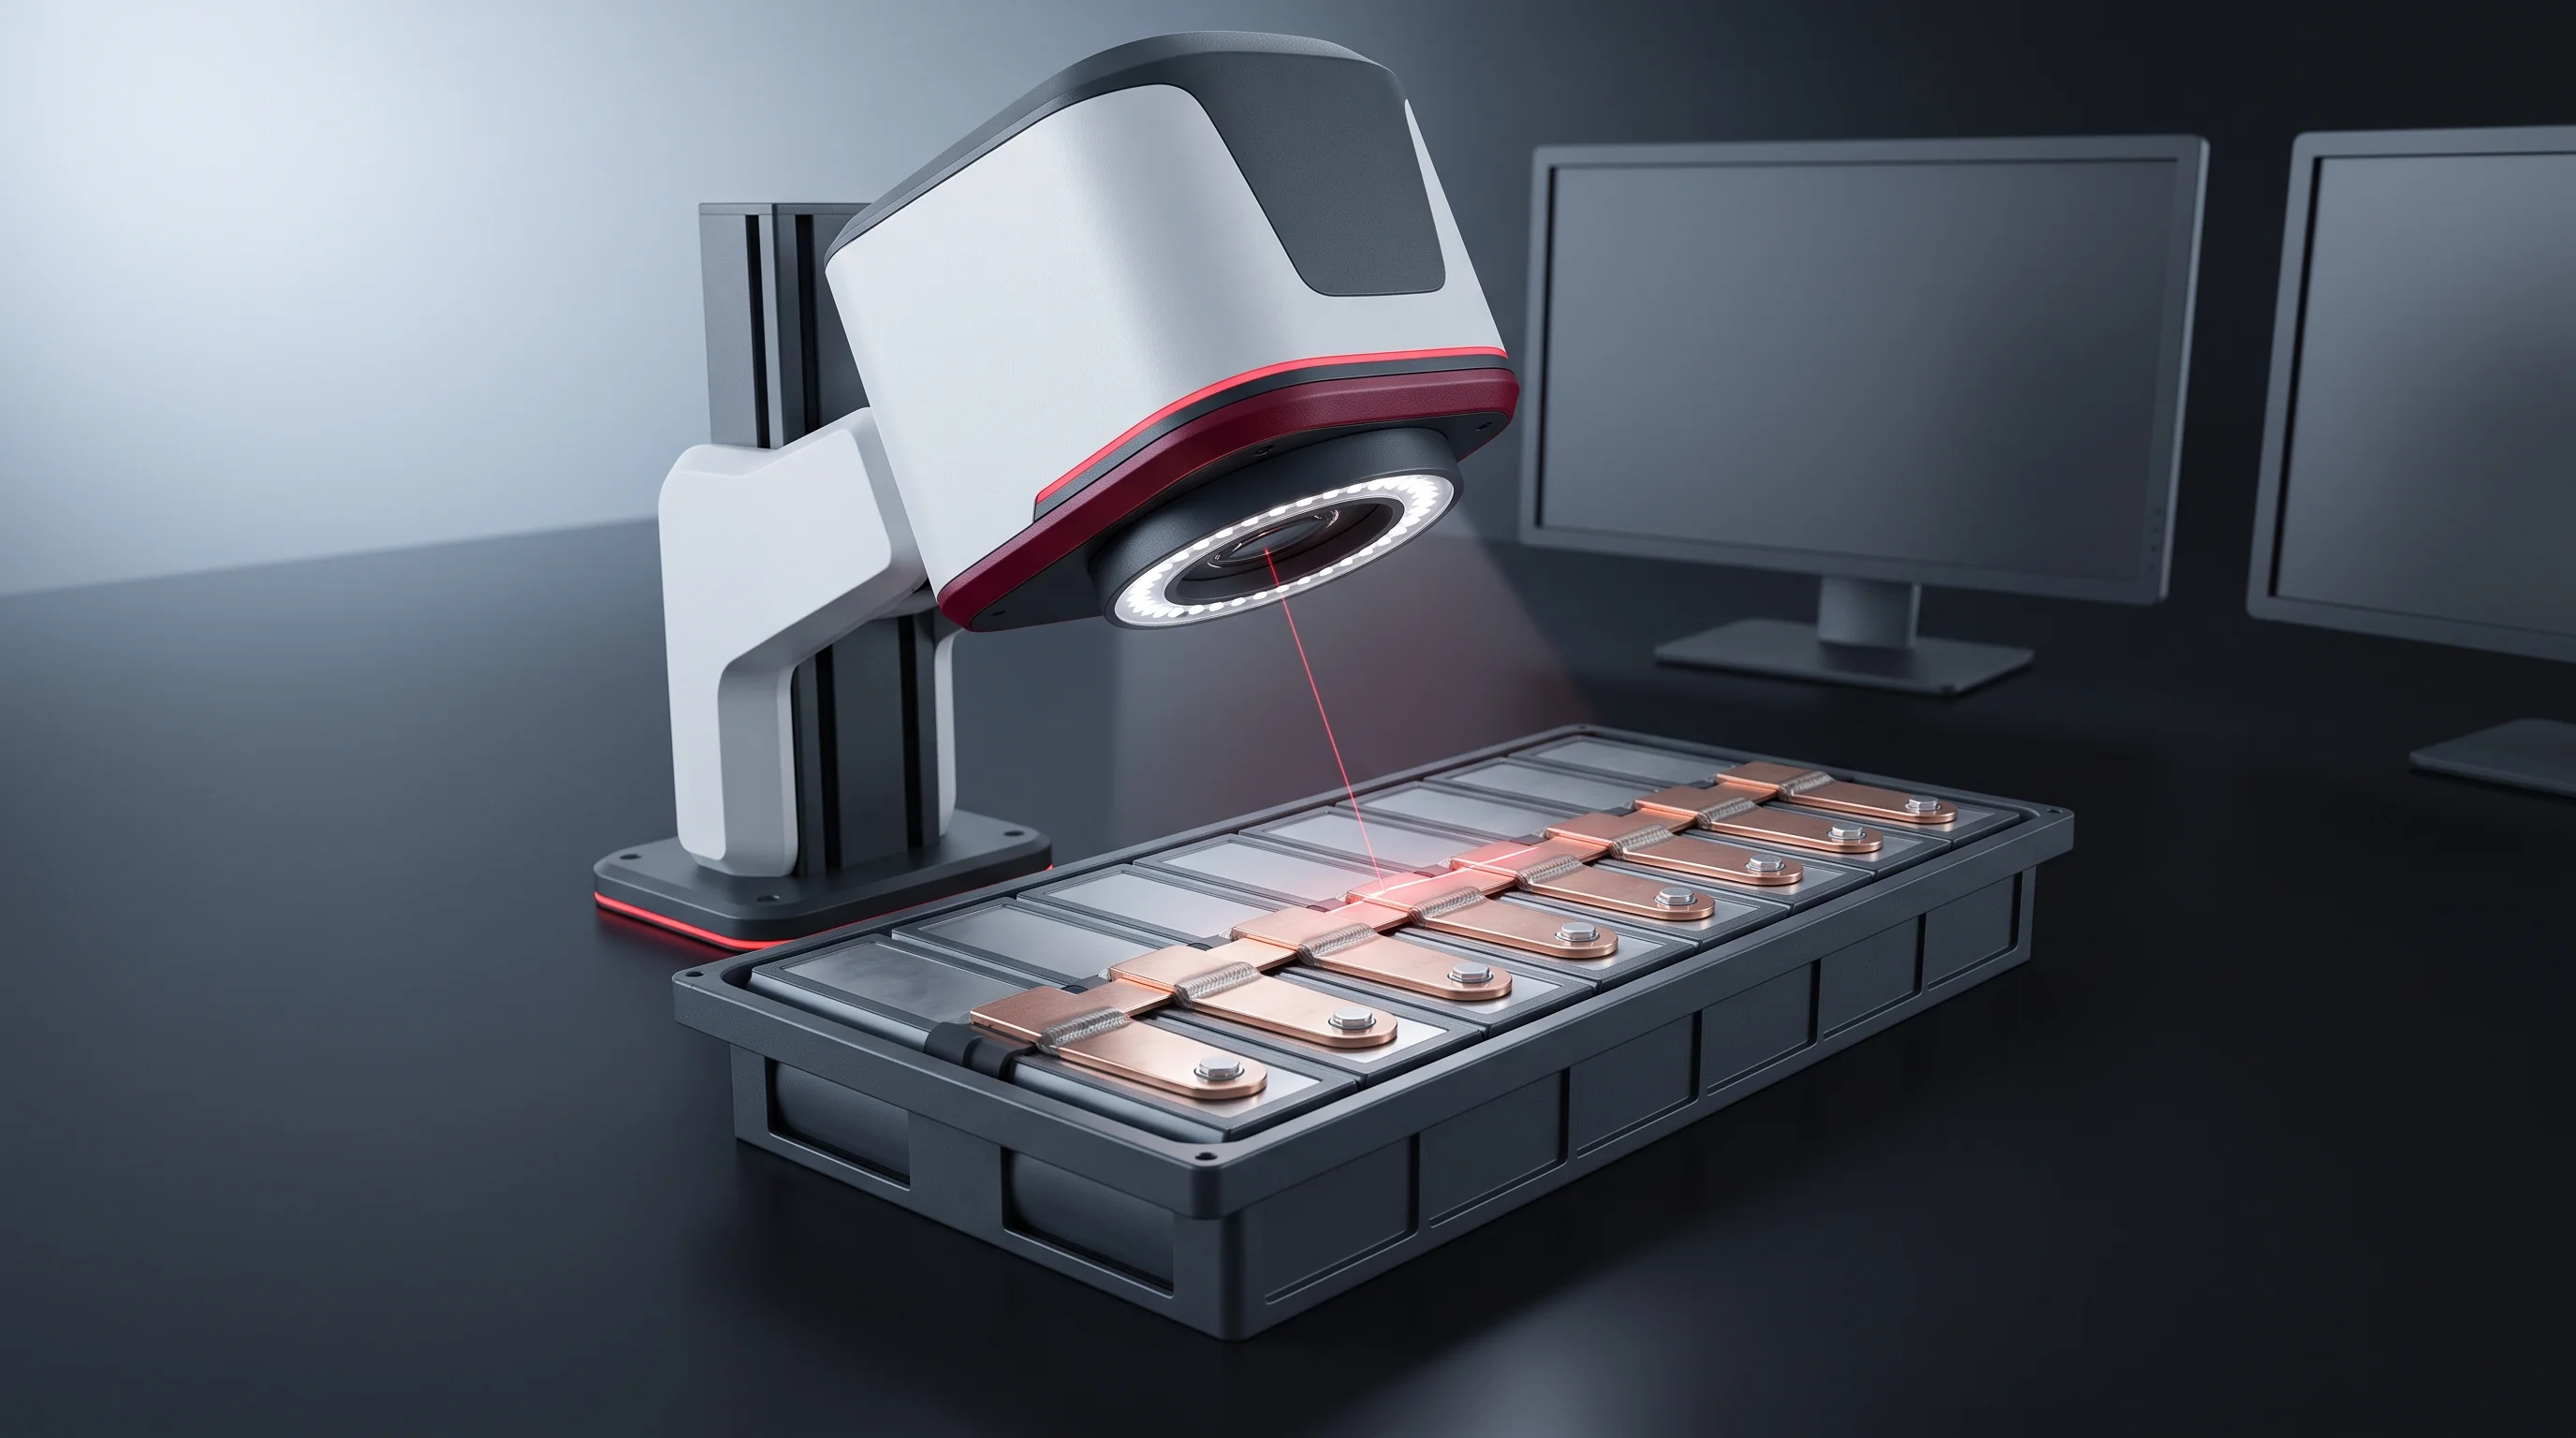
Fusion width measured on 100% of modules with seam appearance; written to the module number.
Manual re-check with the CCS communication test: cell voltages read back against the sorting record.
Insulation, hipot, total voltage, internal resistance, continuity — all measured through the joints made here.
This station is told where each joint is; it does not go looking for it. A weld criterion is only as repeatable as the datum it was measured against, and that datum is set one station earlier at terminal addressing. The ≤±0.2 mm figure upstream and the fusion figures here are the same argument.
What leaves is the module’s electrical path: everything the module and pack end-of-line tests measure is measured through these joints.
Nine lines, three ways of proving them
Two figures describe the machine and three describe the joint, obtained in three different ways. That difference decides what your inspector checks every shift and what only a sample can answer.
| Figure | Value | What it governs | Proved by |
|---|---|---|---|
| Laser source | 6 kW | Capability at the joint: room in the parameter window when your busbar is thicker or more reflective than a blueprint one. | machine |
| Weld speed | 50–100 mm/s | The window a recipe is written inside. Your point in it is settled against busbar material and section; the speed used is recorded per module. | machine |
| Fusion depth | ≥1.0 mm | The criterion under the surface. Held by first-article sectioning and by one sectioned module per shift. | section |
| Fusion width | ≥1.5 mm | The criterion checked on every module, at station 14, with weld appearance. | 100% visual |
| Joint pull strength | ≥1000 N | The destructive criterion. Proved on samples at qualification and again at site acceptance. | samples |
| Row configuration | Single / double | Both run here. What changes is the joint map and the fixture, not the mechanism or the criteria. | fixture |
| Motion | Gantry + scanner | How the beam reaches each joint while the module stays on its carrier. | machine |
| Automation level | AUTO | Automatic on the economy build and on the high-automation build. | line |
| Shielding gas | N₂ 0.5 MPa | Flow depends on the configuration; the flow delivered is recorded with the weld. | utility |
6 kW and 50–100 mm/s set the width of the window, not the point inside it.
Depth, width and pull strength are what your module gets. The red rows are the ones your quality plan is written around.
Width every module · depth by section · strength by sample
One method read three ways: prove strength on samples, lock the parameters, verify per module that the fusion still has the shape those parameters make.
The criterion your quality team works with day to day: it catches a joint drifting off the terminal before anything downstream sees it.
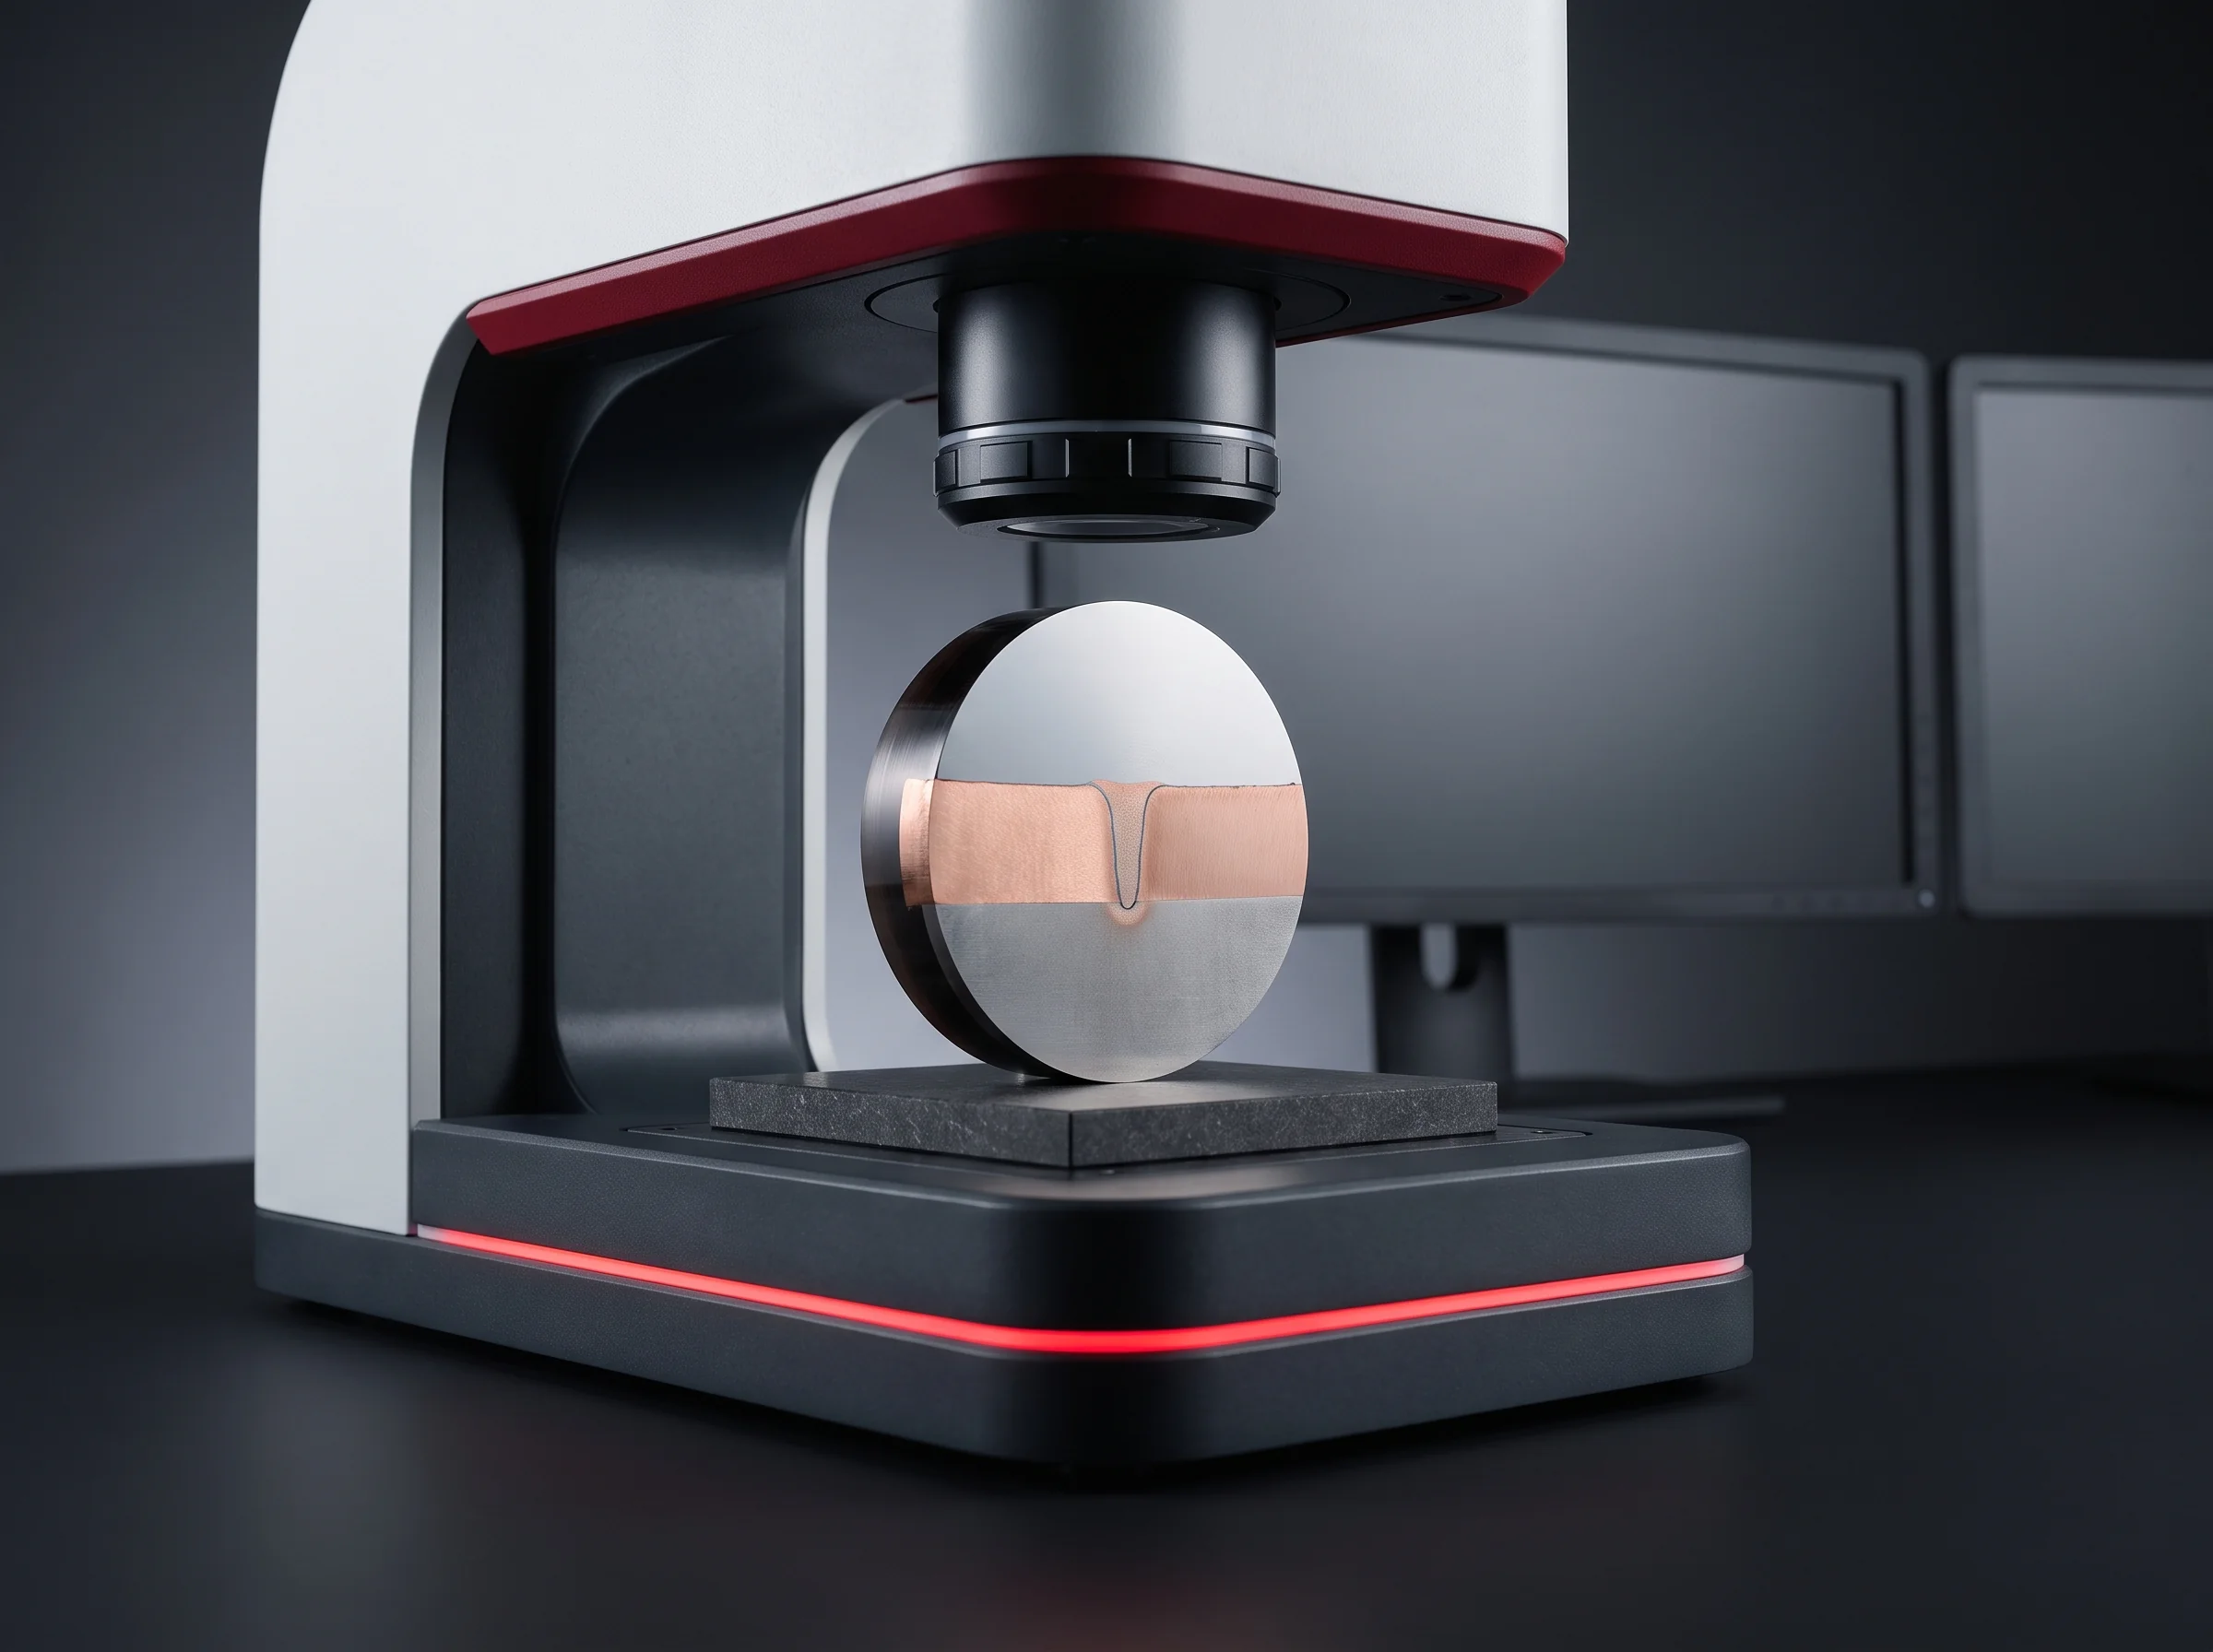
Depth is under a surface nobody can look at, so it is held two ways, kept together.
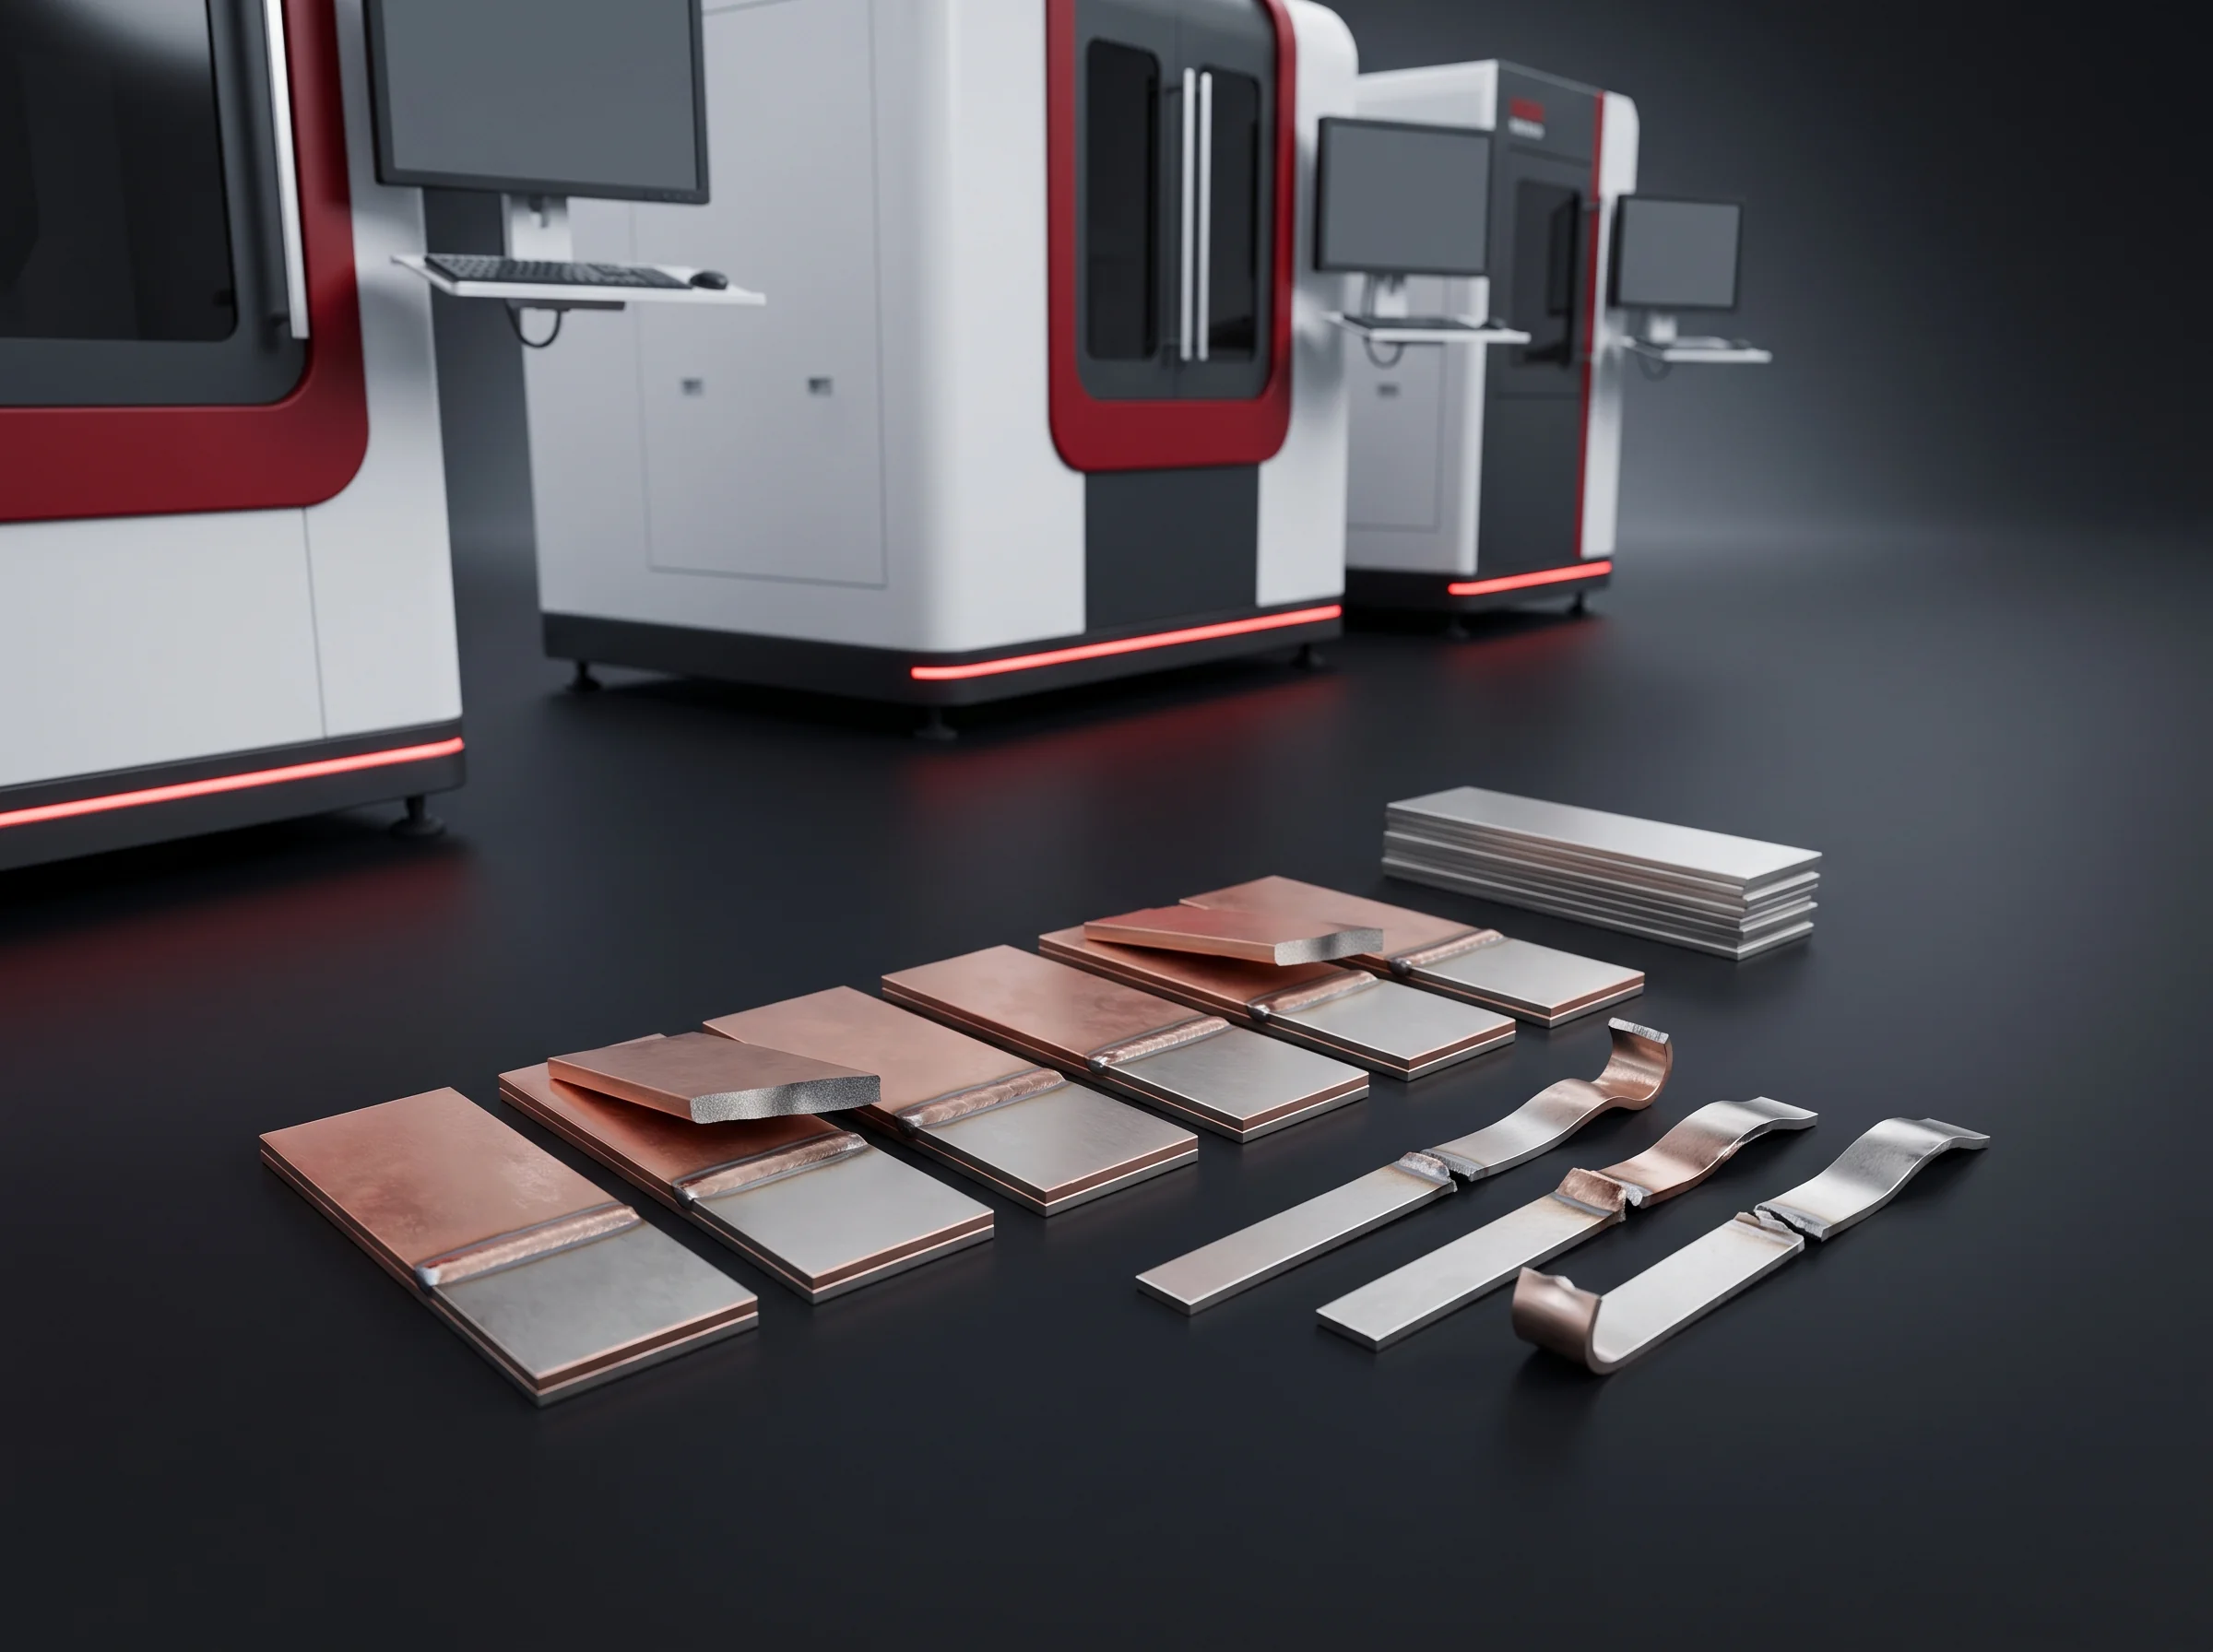
The test consumes the joint whether it passes or fails. Pulling every joint would not be an inspection plan, it would be a scrapping plan.
The window, not a verdict
Travel too fast and depth falls short; travel too slow and the seam spreads without gaining anything. The window exists because those two pull against each other. The point inside it is fixed by your busbar material and section at qualification, and stays fixed.
Sequence and timestamp
Every seam leaves with a sequence number and a timestamp attached to the module number. After this station, correcting anything under the busbar means cutting.
Never written on this station
A new busbar part’s recipe is born on the off-line gantry laser welding machine, away from the line and from takt, and moves into BLP-W6 unchanged.
Recipes are keyed to the busbar geometry, not to a shift, a batch or a machine. That is what makes rework honest: a module back for a repair weld gets the recipe of its original part number, not whatever is loaded at the time.
The recipe carries the parameters proved together — power, weld speed, defocus, nitrogen flow, seam order — and the station records what it delivered against them, by module number, over PROFINET. When the two agree and the station 14 width check passes, the module is released on evidence.
Three jobs, kept apart
A recipe that anyone can nudge stops being evidence the moment it is nudged. The station separates three jobs; the five days of training on your line after site acceptance are built the same way.
Three inputs
Three inputs are enough to say what this station would be in your line, what fixture has to be cut, and how the first article would be qualified. Reply inside 24 hours; the contact page has the direct address.
0.5 MPa at the interface
Shielding gas is supplied to the line at 0.5 MPa, and this station is where it is consumed. A line that welds more modules per hour uses more gas, so the flow is quoted per configuration.
Not a background service. Flow is qualified with the power and speed it was proved with, and recorded per module with them, so a gas problem shows up in the weld record before it shows up as porosity at station 14.
Solid = always drawn; light = the range a recipe may call for as joint count and takt rise.
Same mechanism, same criteria
Both run on this station. A criterion that relaxed when the work got harder was never a criterion.
Between busbar parts already qualified: a recipe call at the station and a first-piece check at station 14. No engineer, no off-line run.
A module type nobody has welded here goes the other way first: off-line first article, samples pulled, section examined, recipe signed, then the line. Station-by-station timing for both routes: cell compatibility and changeover.
Held by module number
When station 14 fails a module on fusion width or weld appearance, it is set aside with a complete account of how it was made. That account decides what happens next.
Recipe number, actual power, speed and defocus, nitrogen flow, and every seam’s sequence number and timestamp travel with it.
After this station a module cannot be taken apart without cutting. Adding heat before anyone knows what moved removes evidence instead of producing it.
By the engineer who holds recipe rights, to the recipe of the original part number — not adjusted on the spot.
A criterion not met is recorded with the station, measured value and criterion beside it; only the failed items are retested.
Same shape, a station wider: bracket back, hold what ran between, look at what actually moves.
Two measured runs, one set of documents
Factory acceptance runs in our 6,000 m² assembly workshop, on one of three bays where the line is stood up in its shipping configuration with your cells, busbars, end plates, housings and cooling plates. Site acceptance repeats it on your floor.
Your parts, with the recipes that will ship.
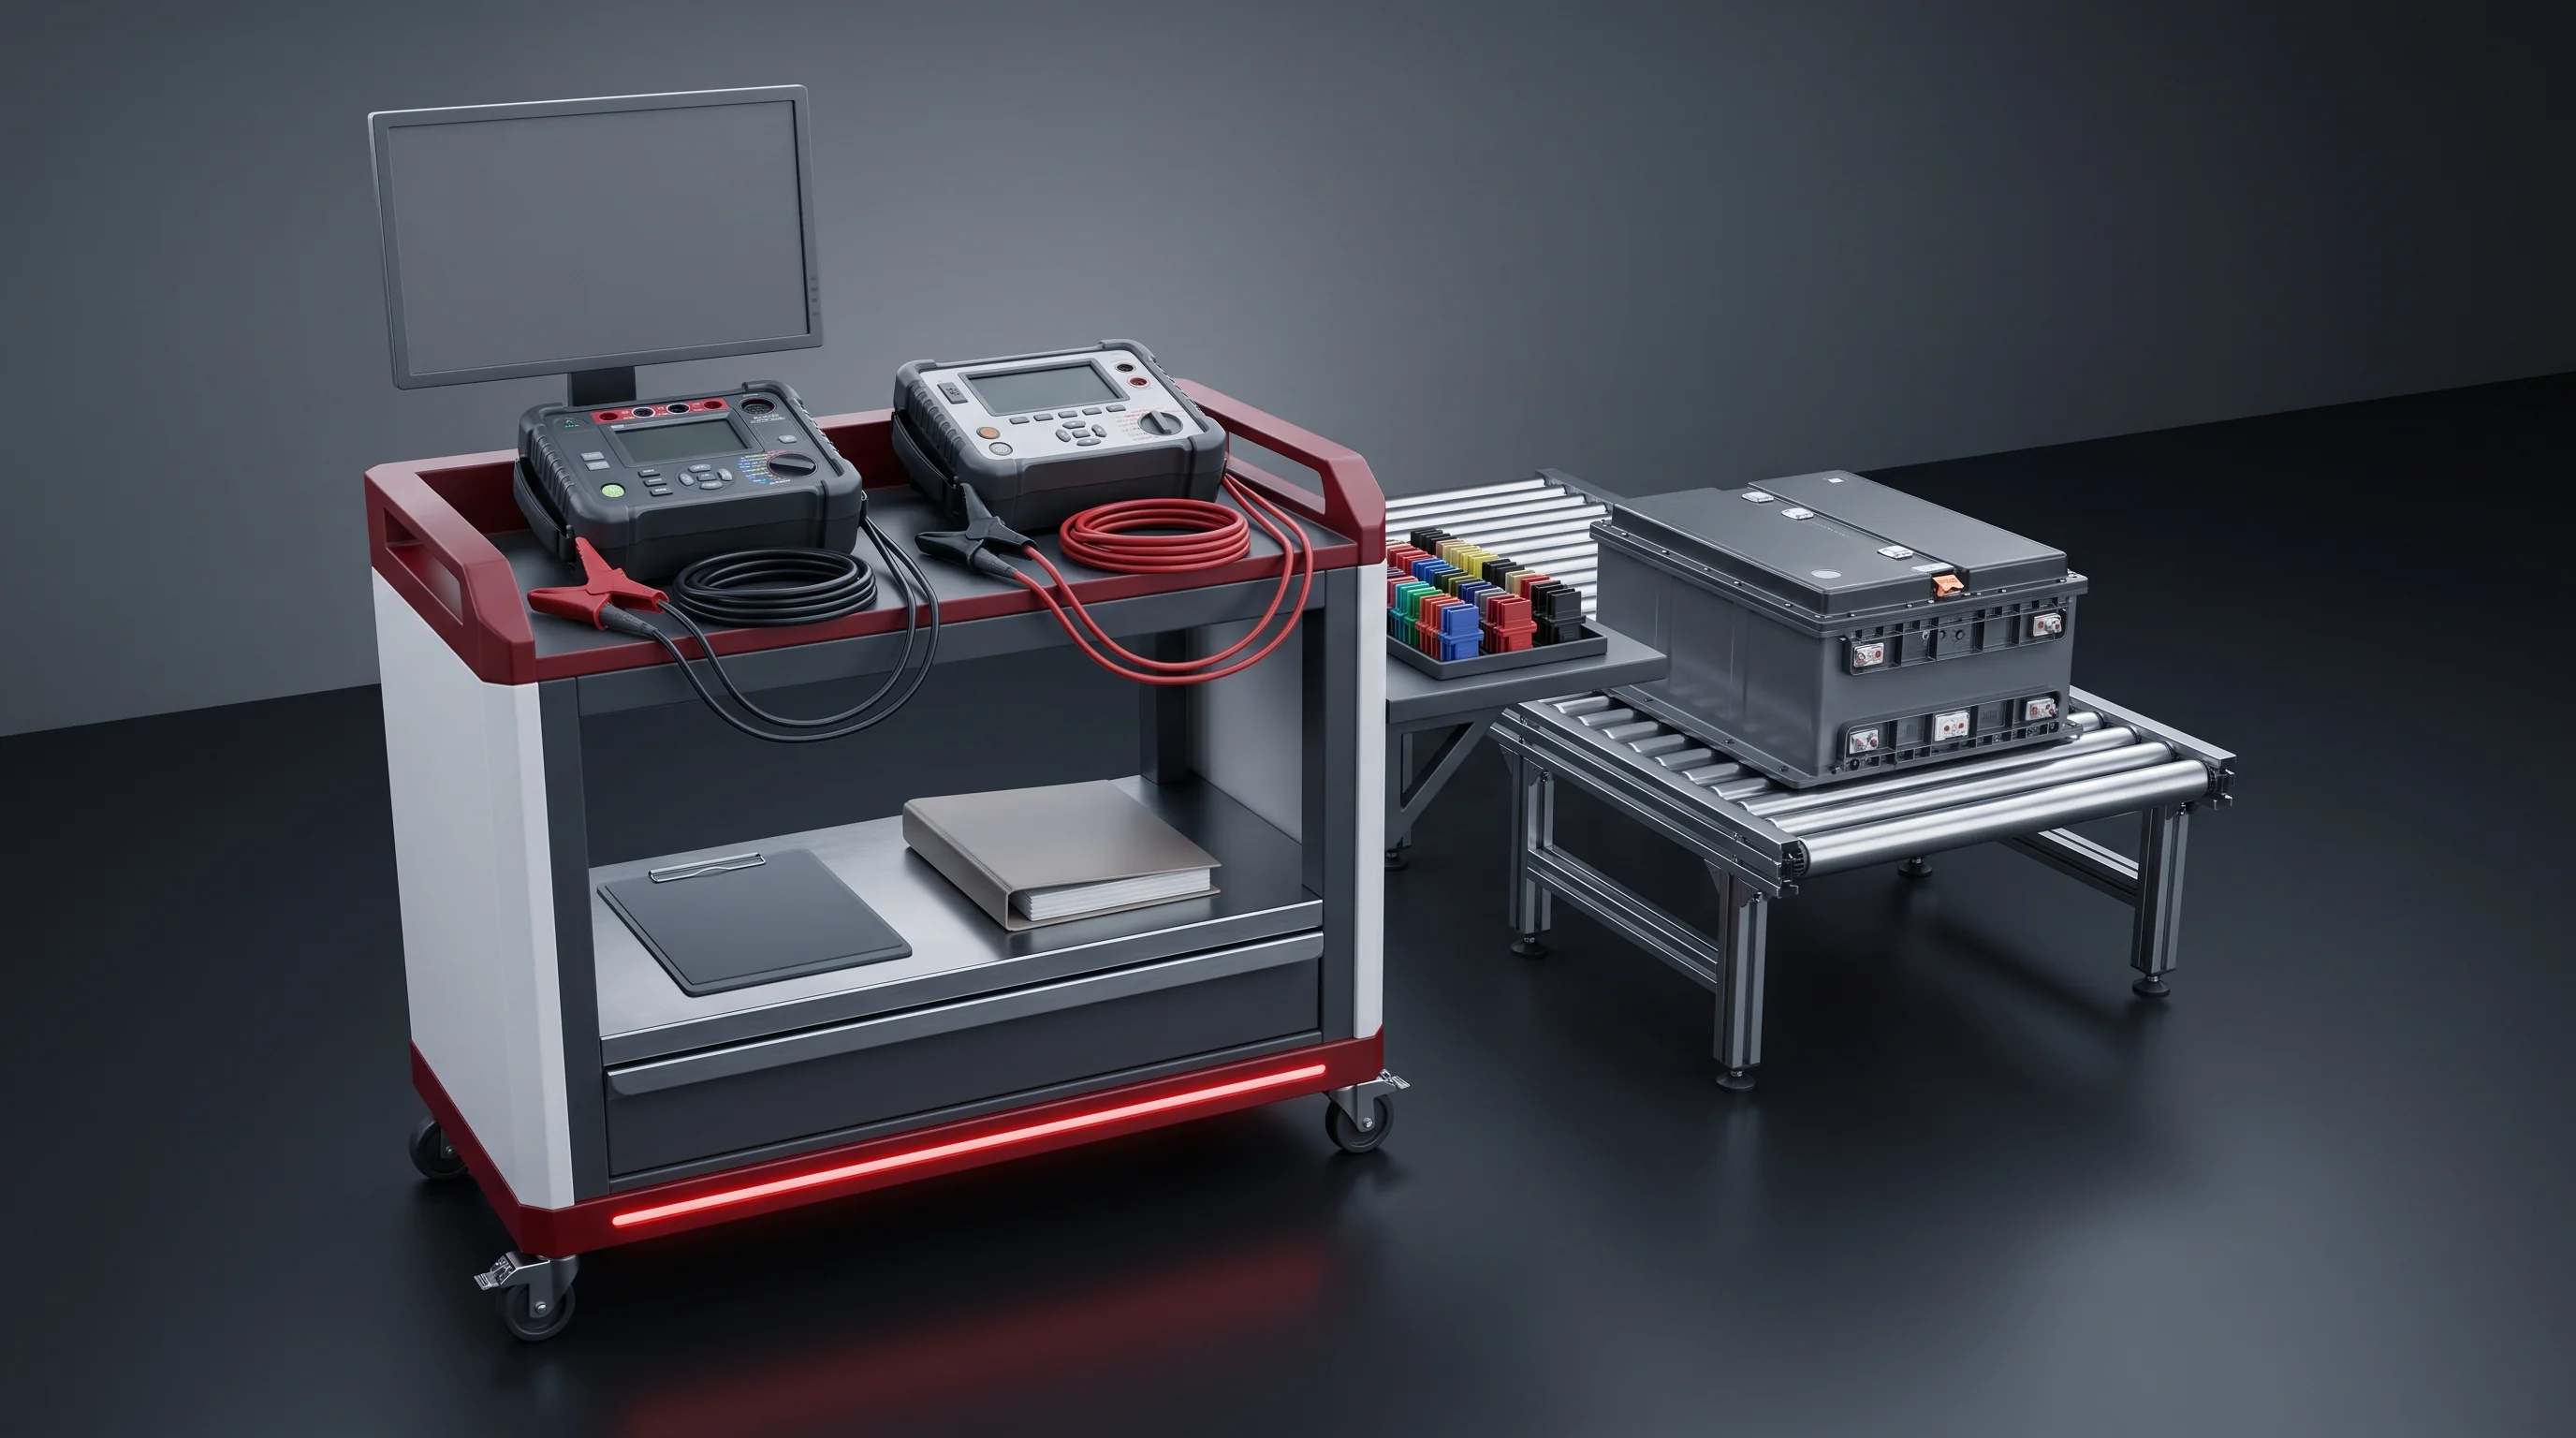
Values printed beside criteria, station by station, both sides countersigned.
Four inputs
With these, the reply carries the station scope, the fixture to be cut for your module, and how the first article would be qualified before anything runs in your line.
Envelope, terminal positions, row layout. A photograph of the print is enough to start.
Copper or aluminium, thickness and width at the joint, plating if any.
Single-row, double-row, or both on the same line.
Modules per hour at station 13, or the line PPM it has to keep up with.
Your enquiry, ready to send
If your email client opened, it is already in the message. If nothing opened, use one of the two routes below.
Start with the joint
Four inputs to our engineering team and the station scope, the fixture to be cut and the first-article plan come back within 24 hours. Behind it: 26 engineers and 40+ line segments into 12 countries, on the about page.