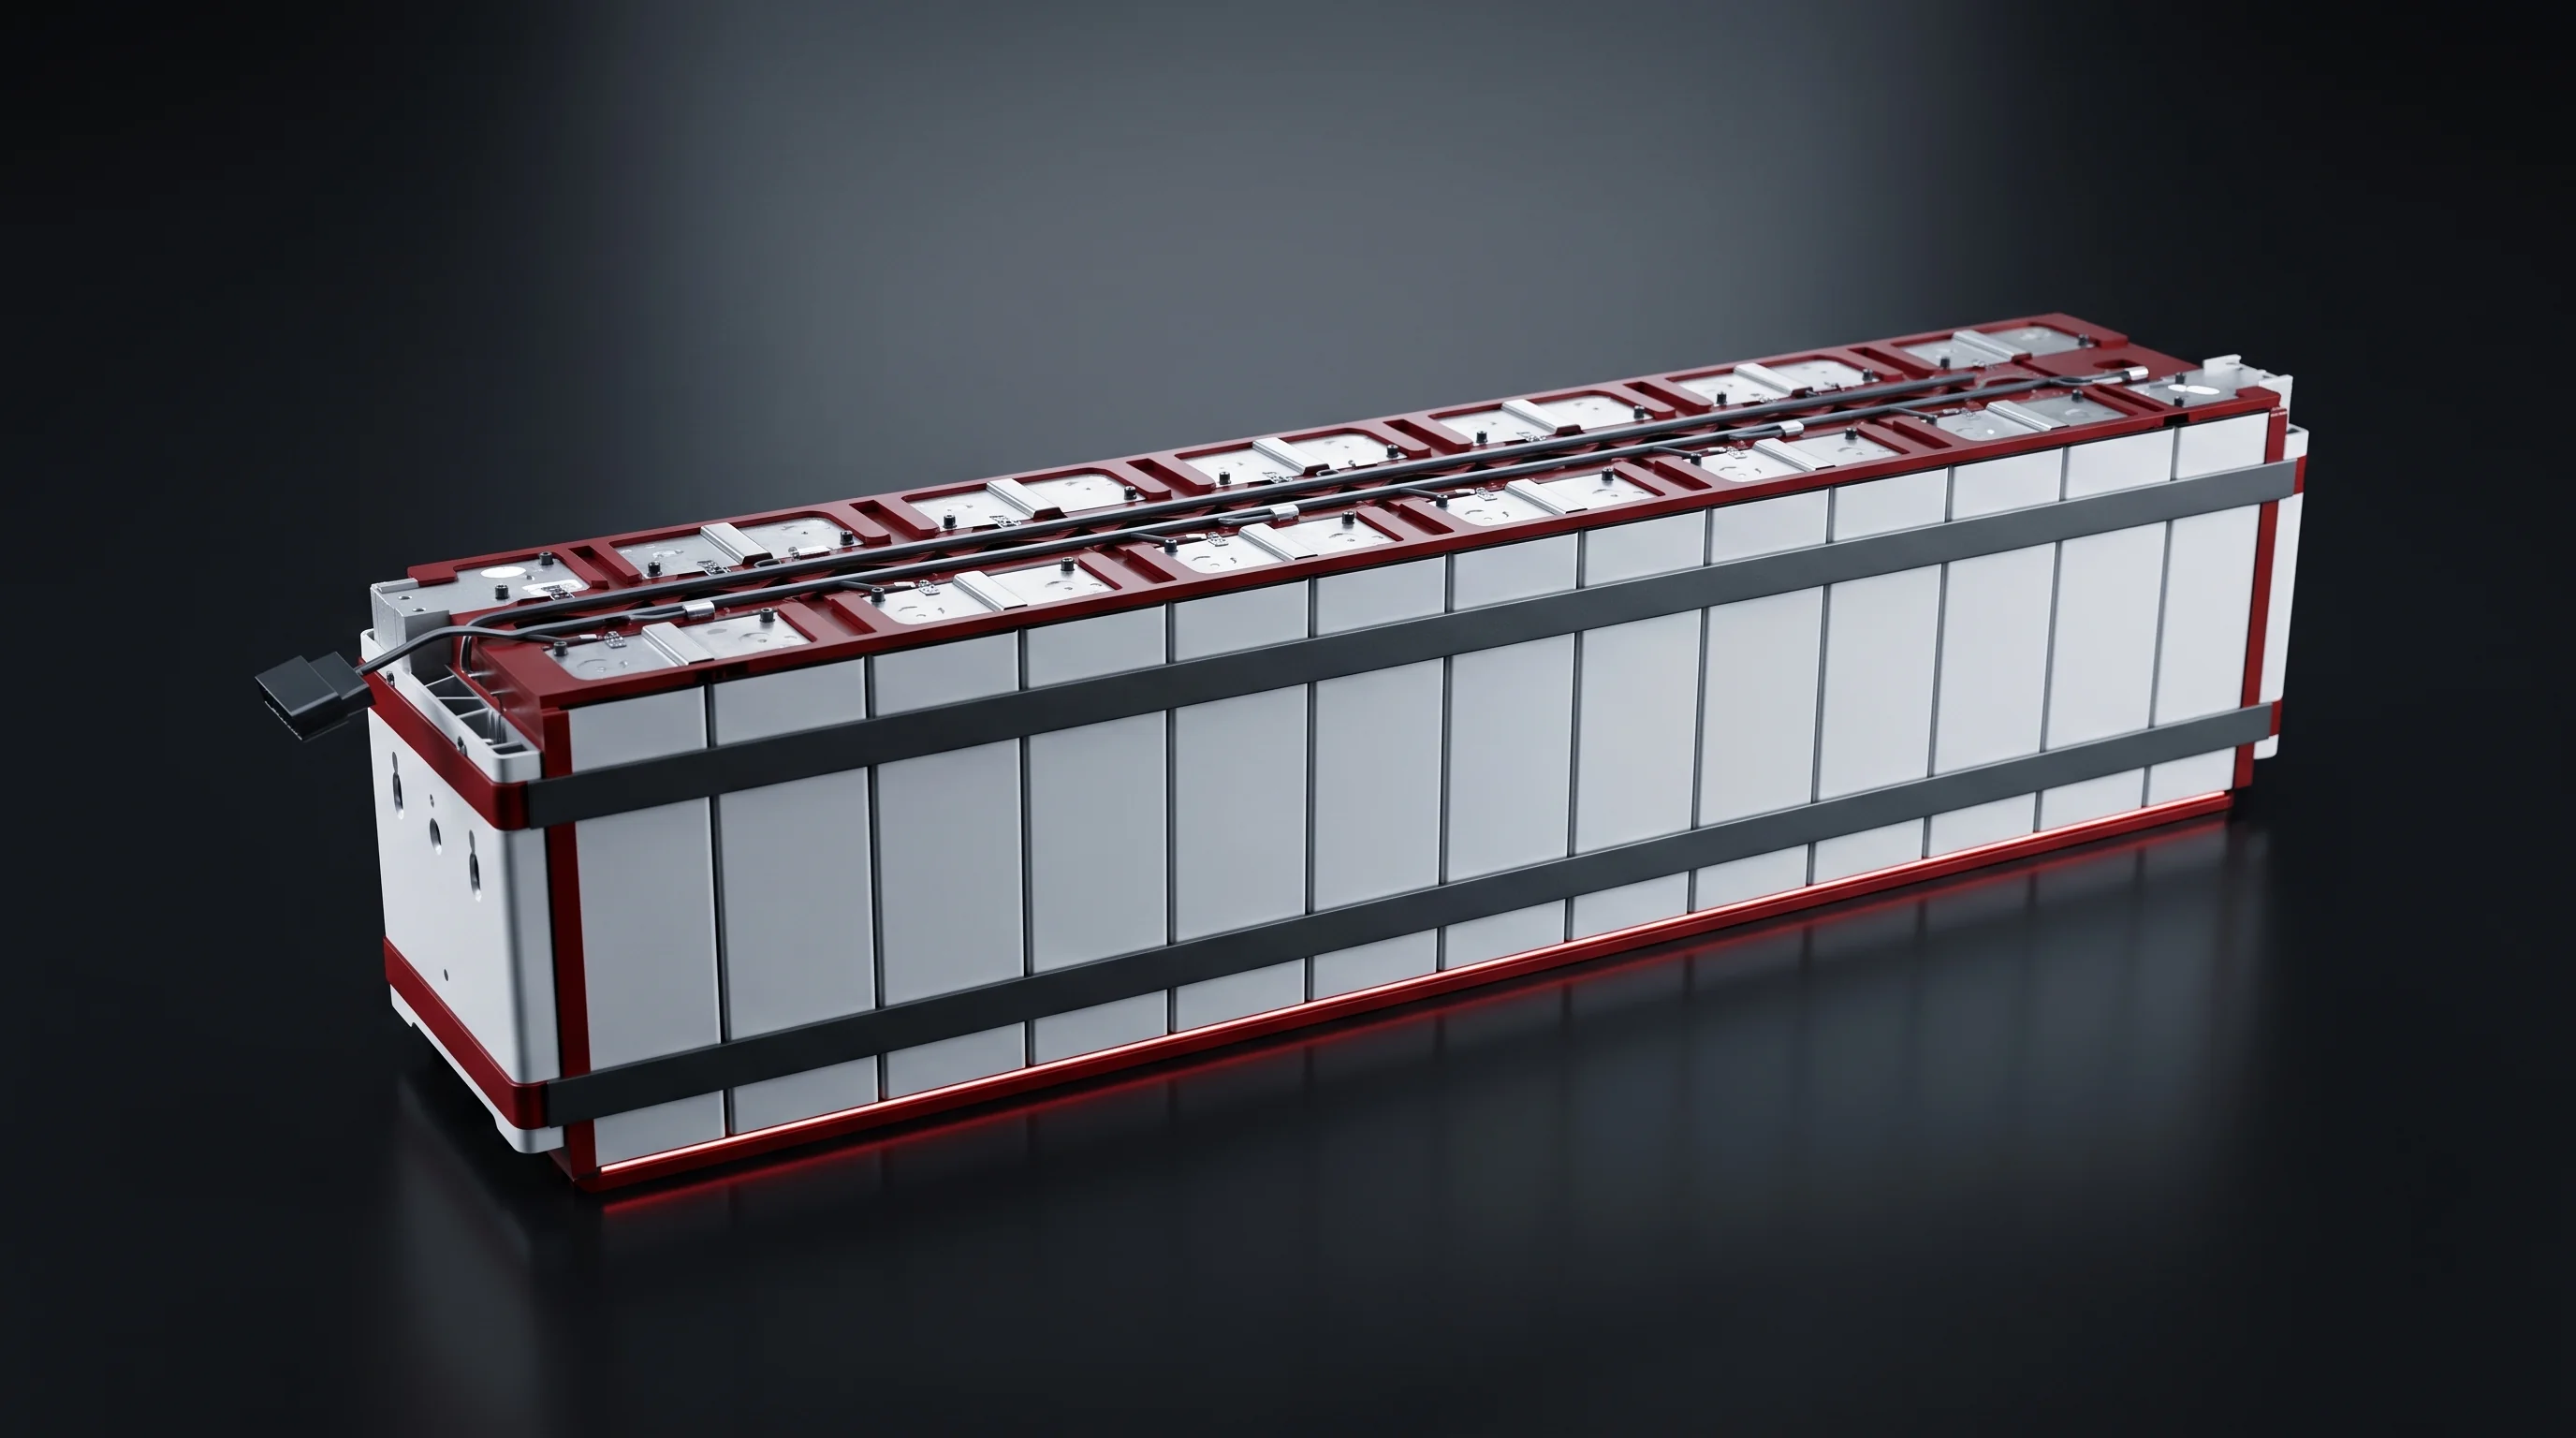
BLP-SP — stations 08 and 09, servo press
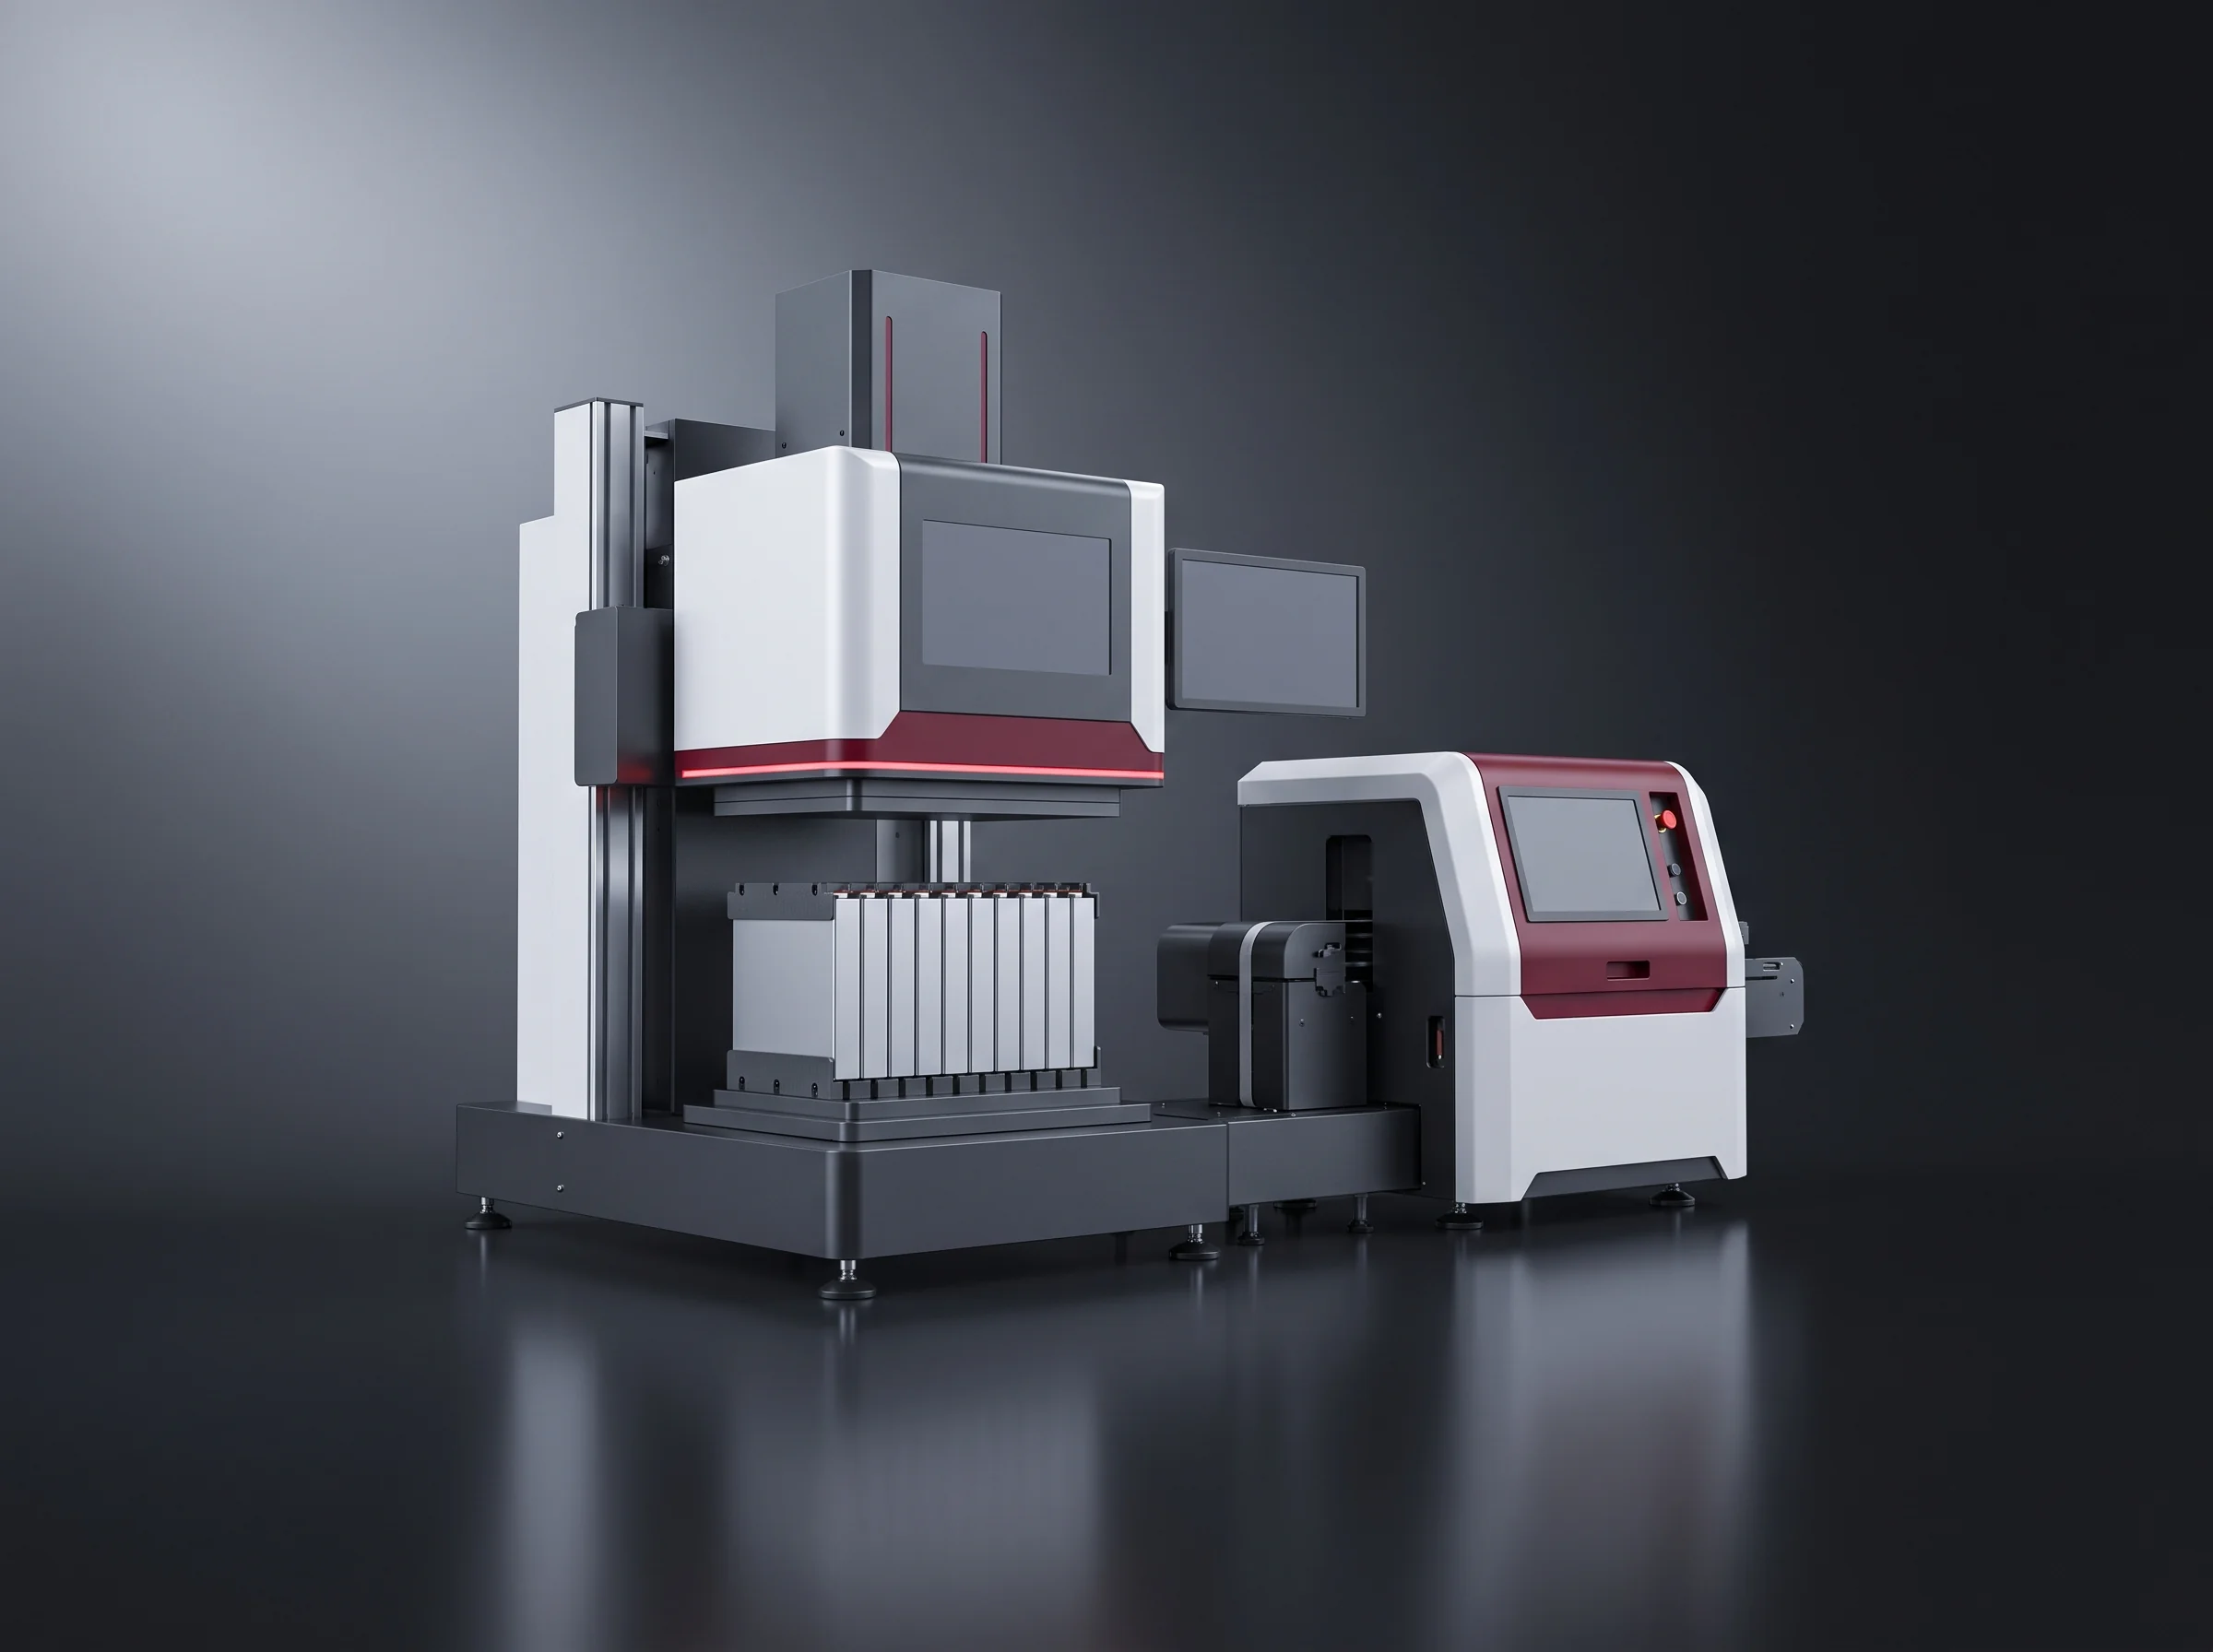
The BLP-SP Module Stacking And Pressing Station
A row of prismatic cells goes in; a module with a dimension comes out. The press closes the stack between 0 and 8000 N, writes the whole press as a force curve at 1 kHz, measures the module after release and bands it with steel. Every module leaves carrying its curve, its length and its recipe number.
- Approach
- Loading ramp
- Knee
- Dwell 0–60 s
- Release
- 0–8000 NServo force, resolved in 10 N steps
- ≤90 sOne module, banding counted in
- ±0.5 mmModule length after release
Stations 08 and 09
The Module Stacking And Pressing Station
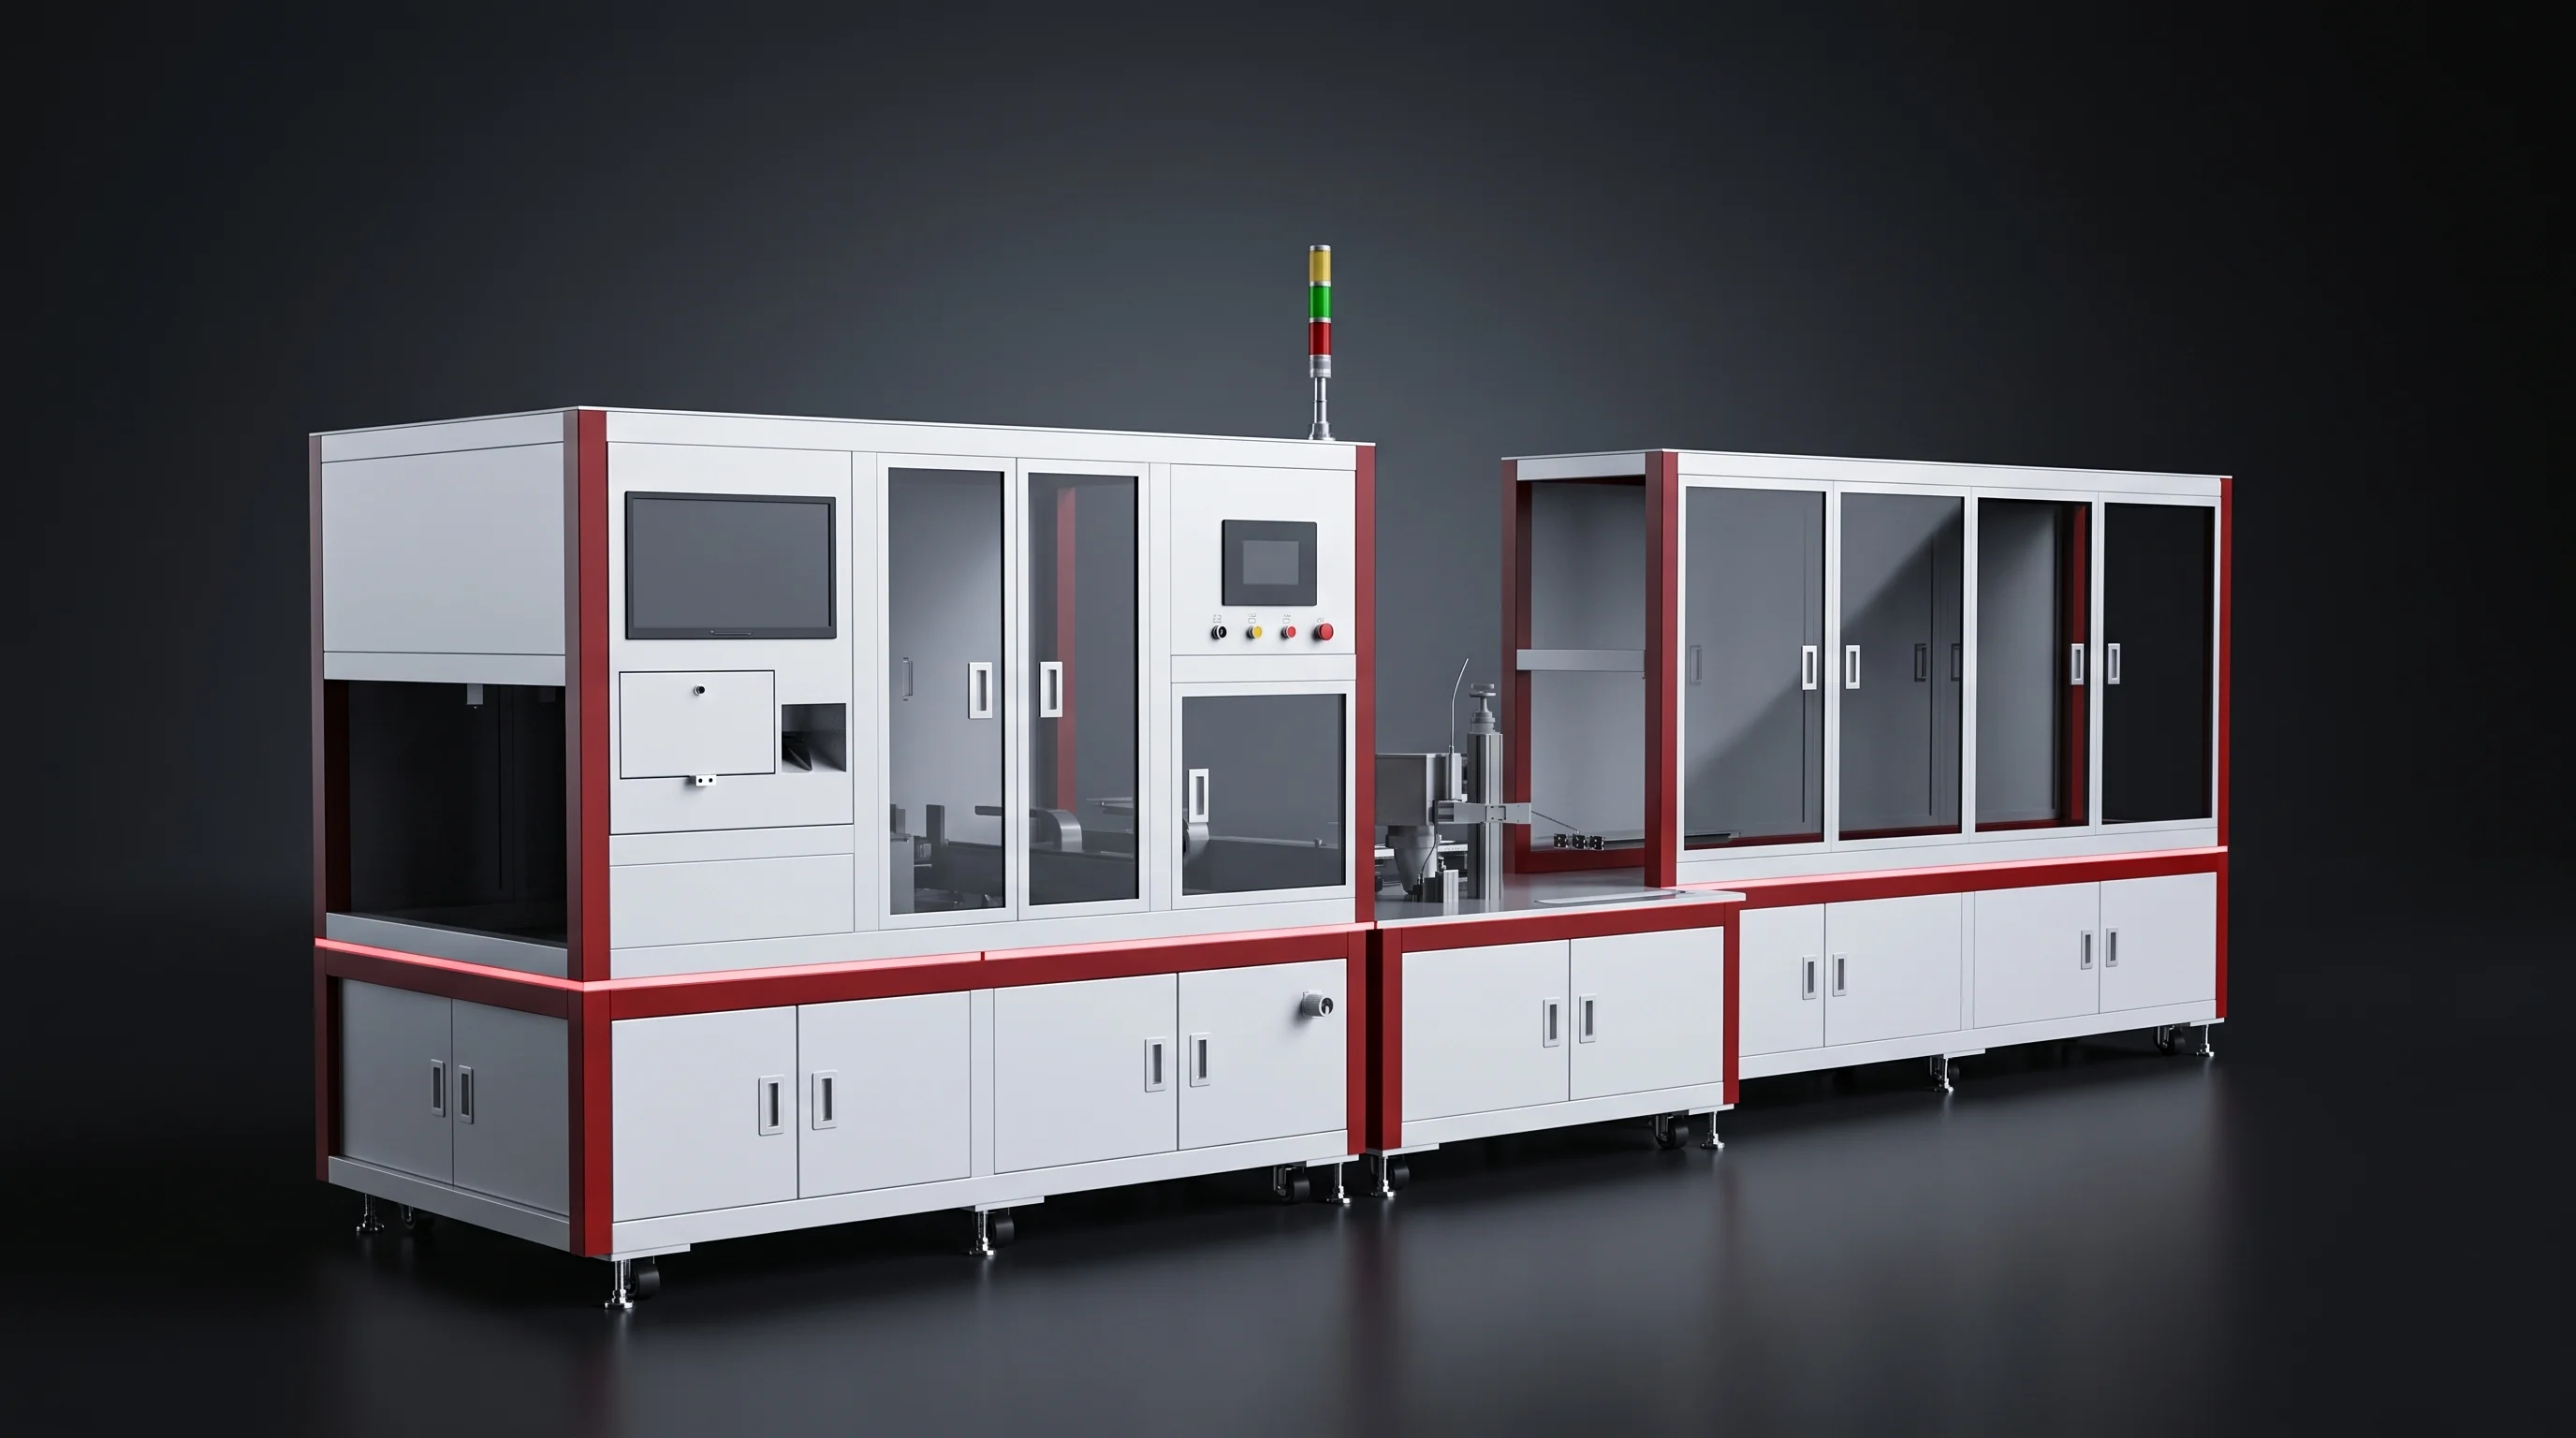
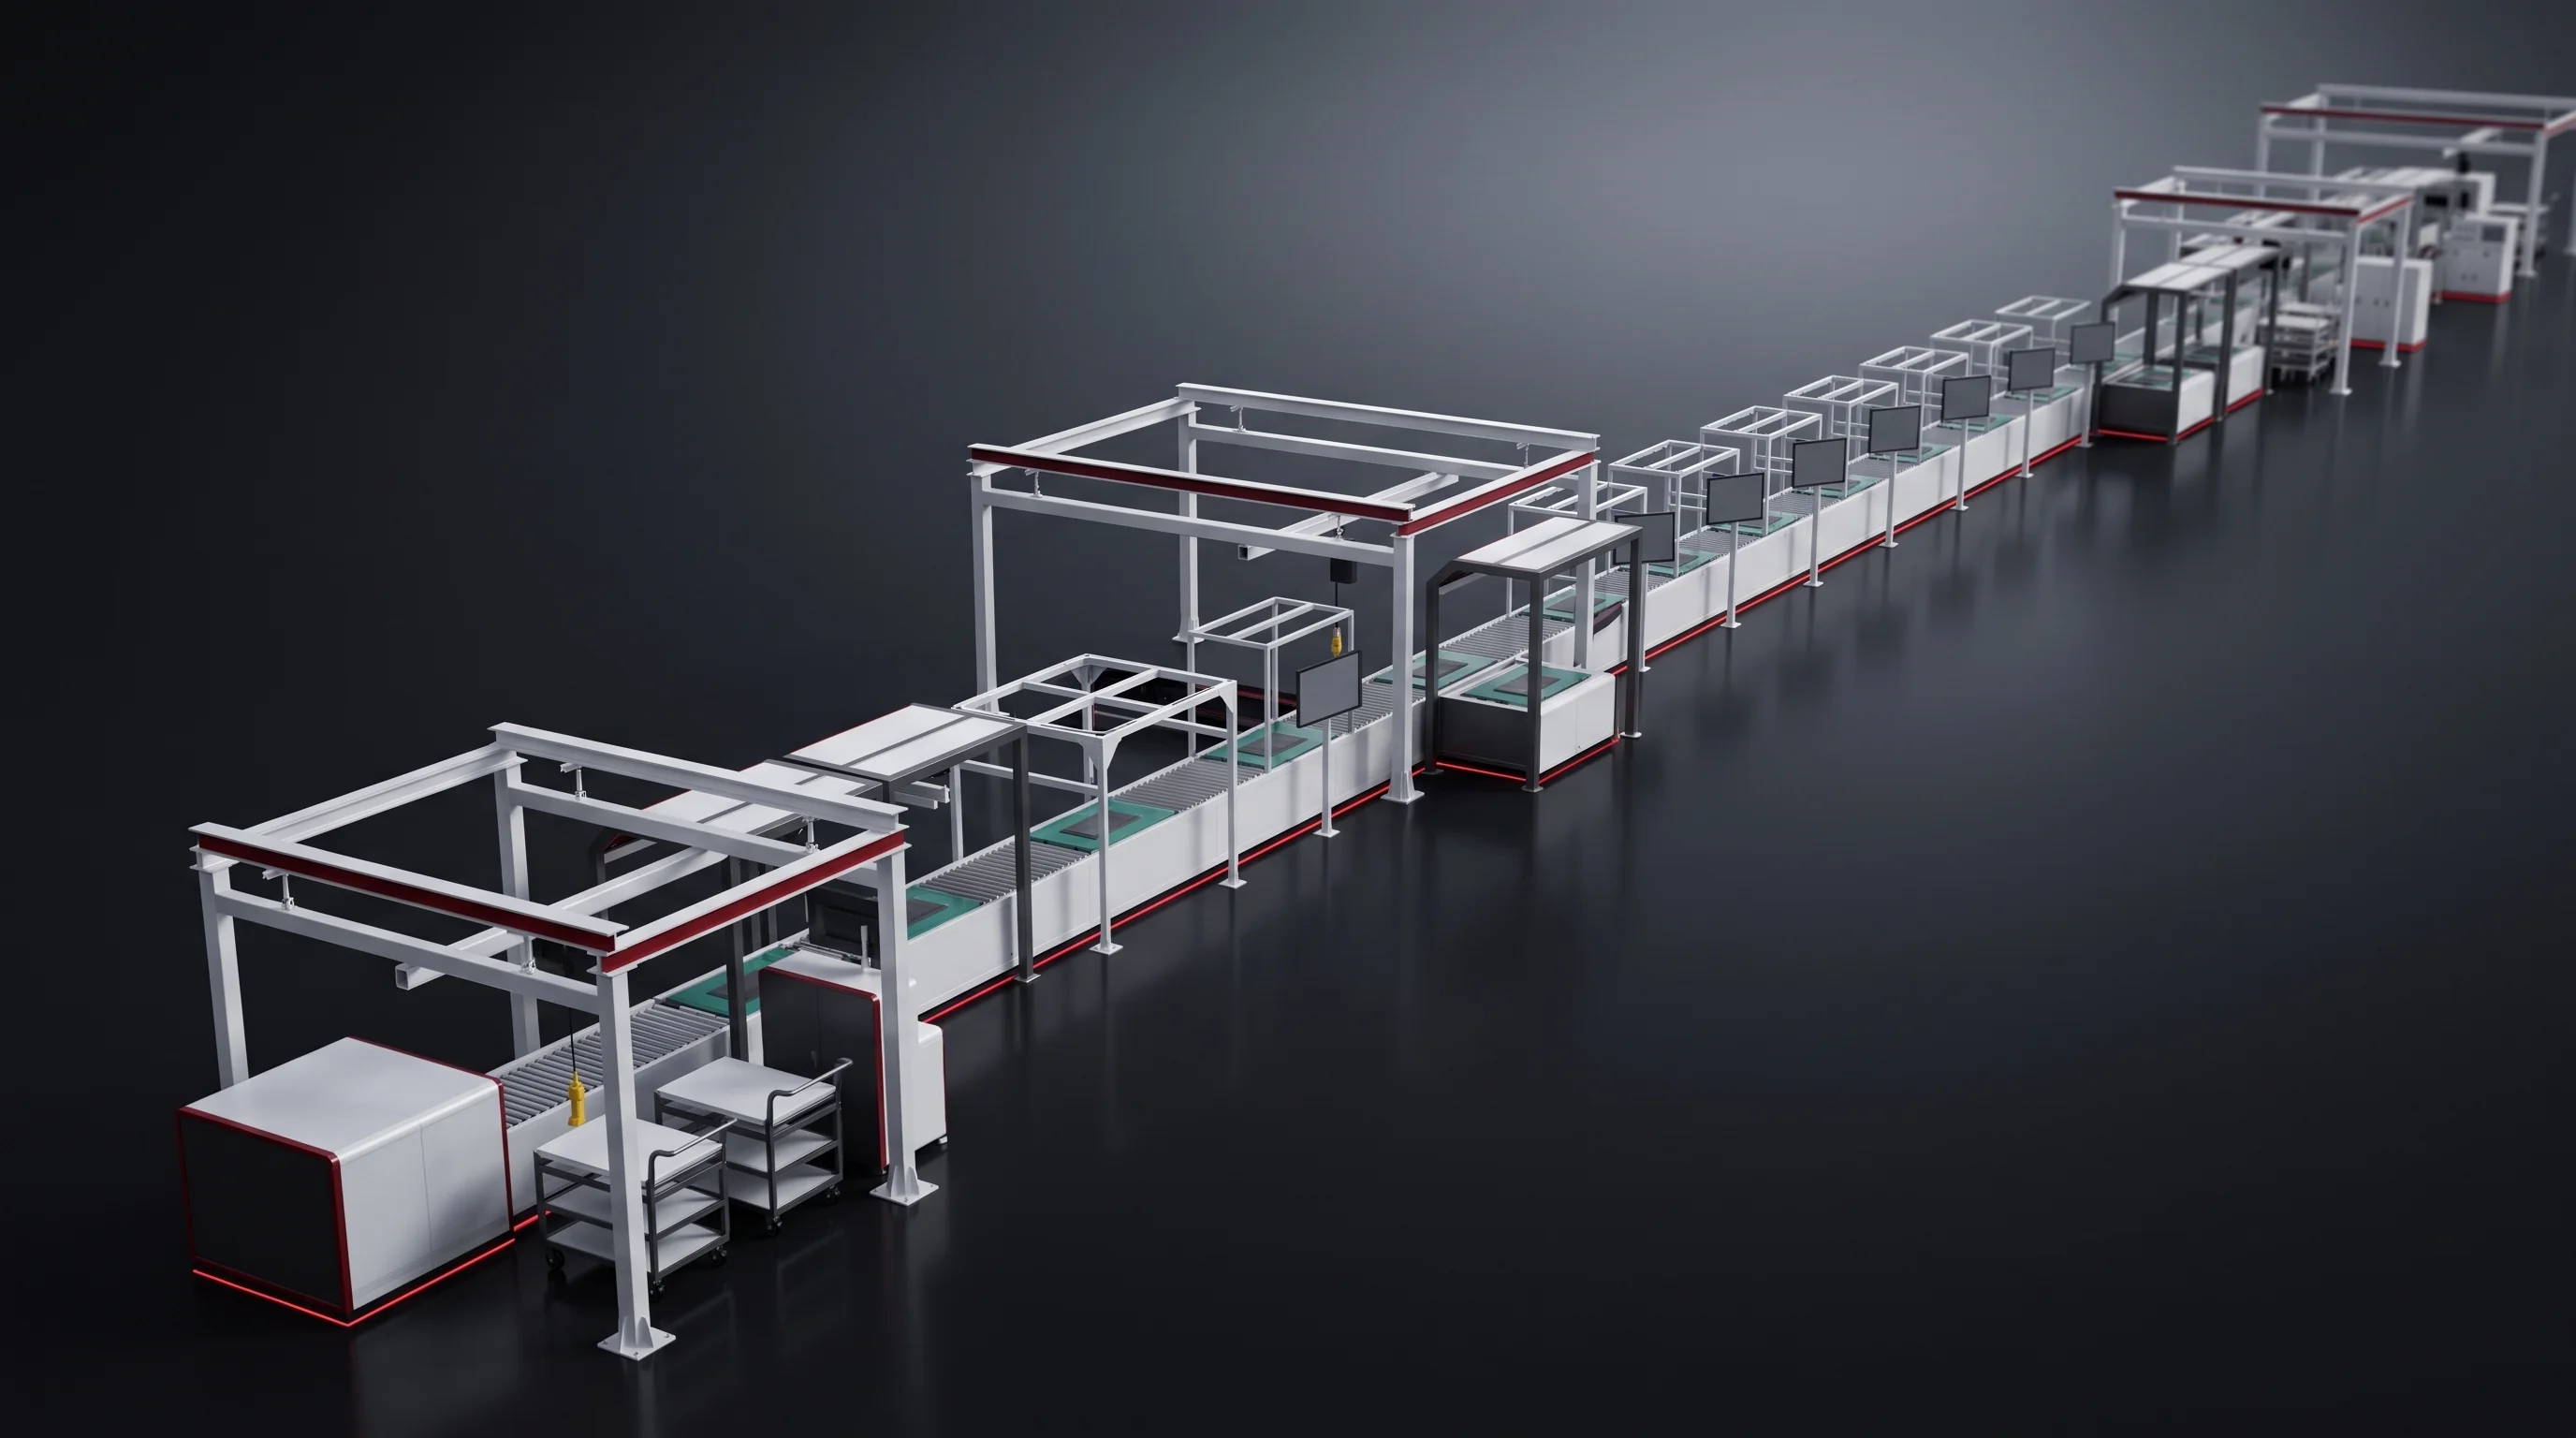
Seventeen stations make up the module segment. Two of them are this one: stacking, then pressing, shaping and steel banding.
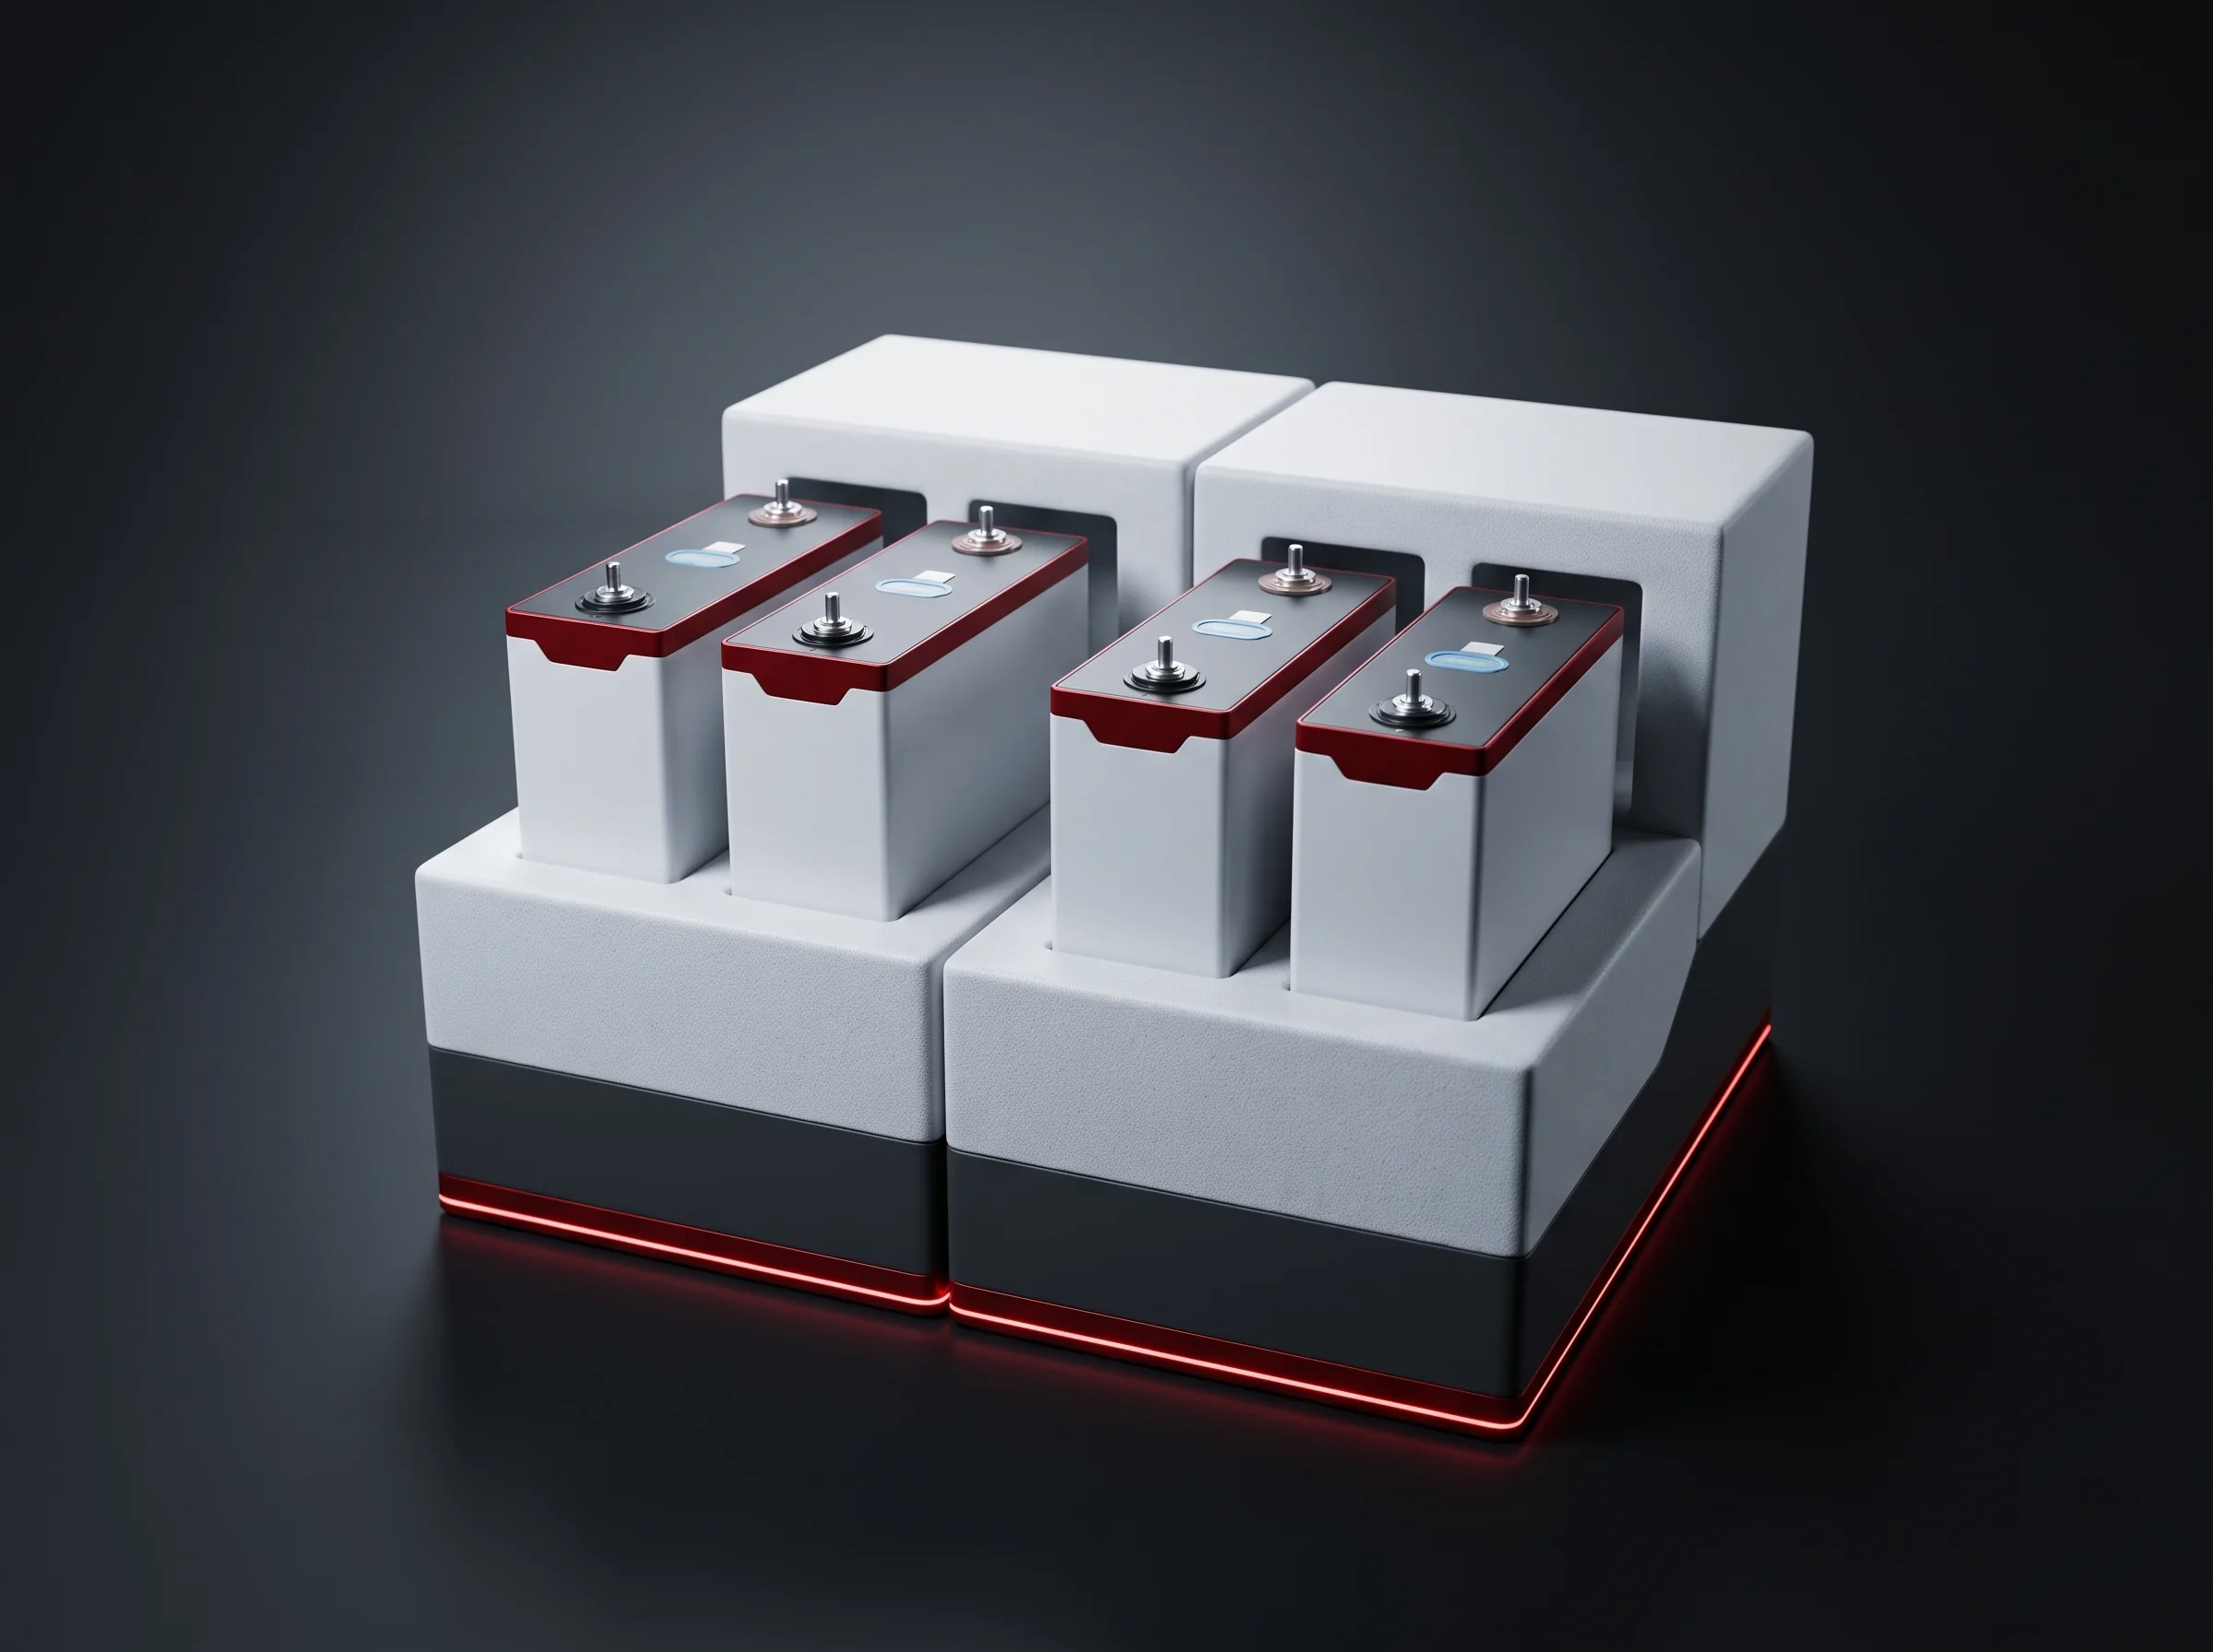
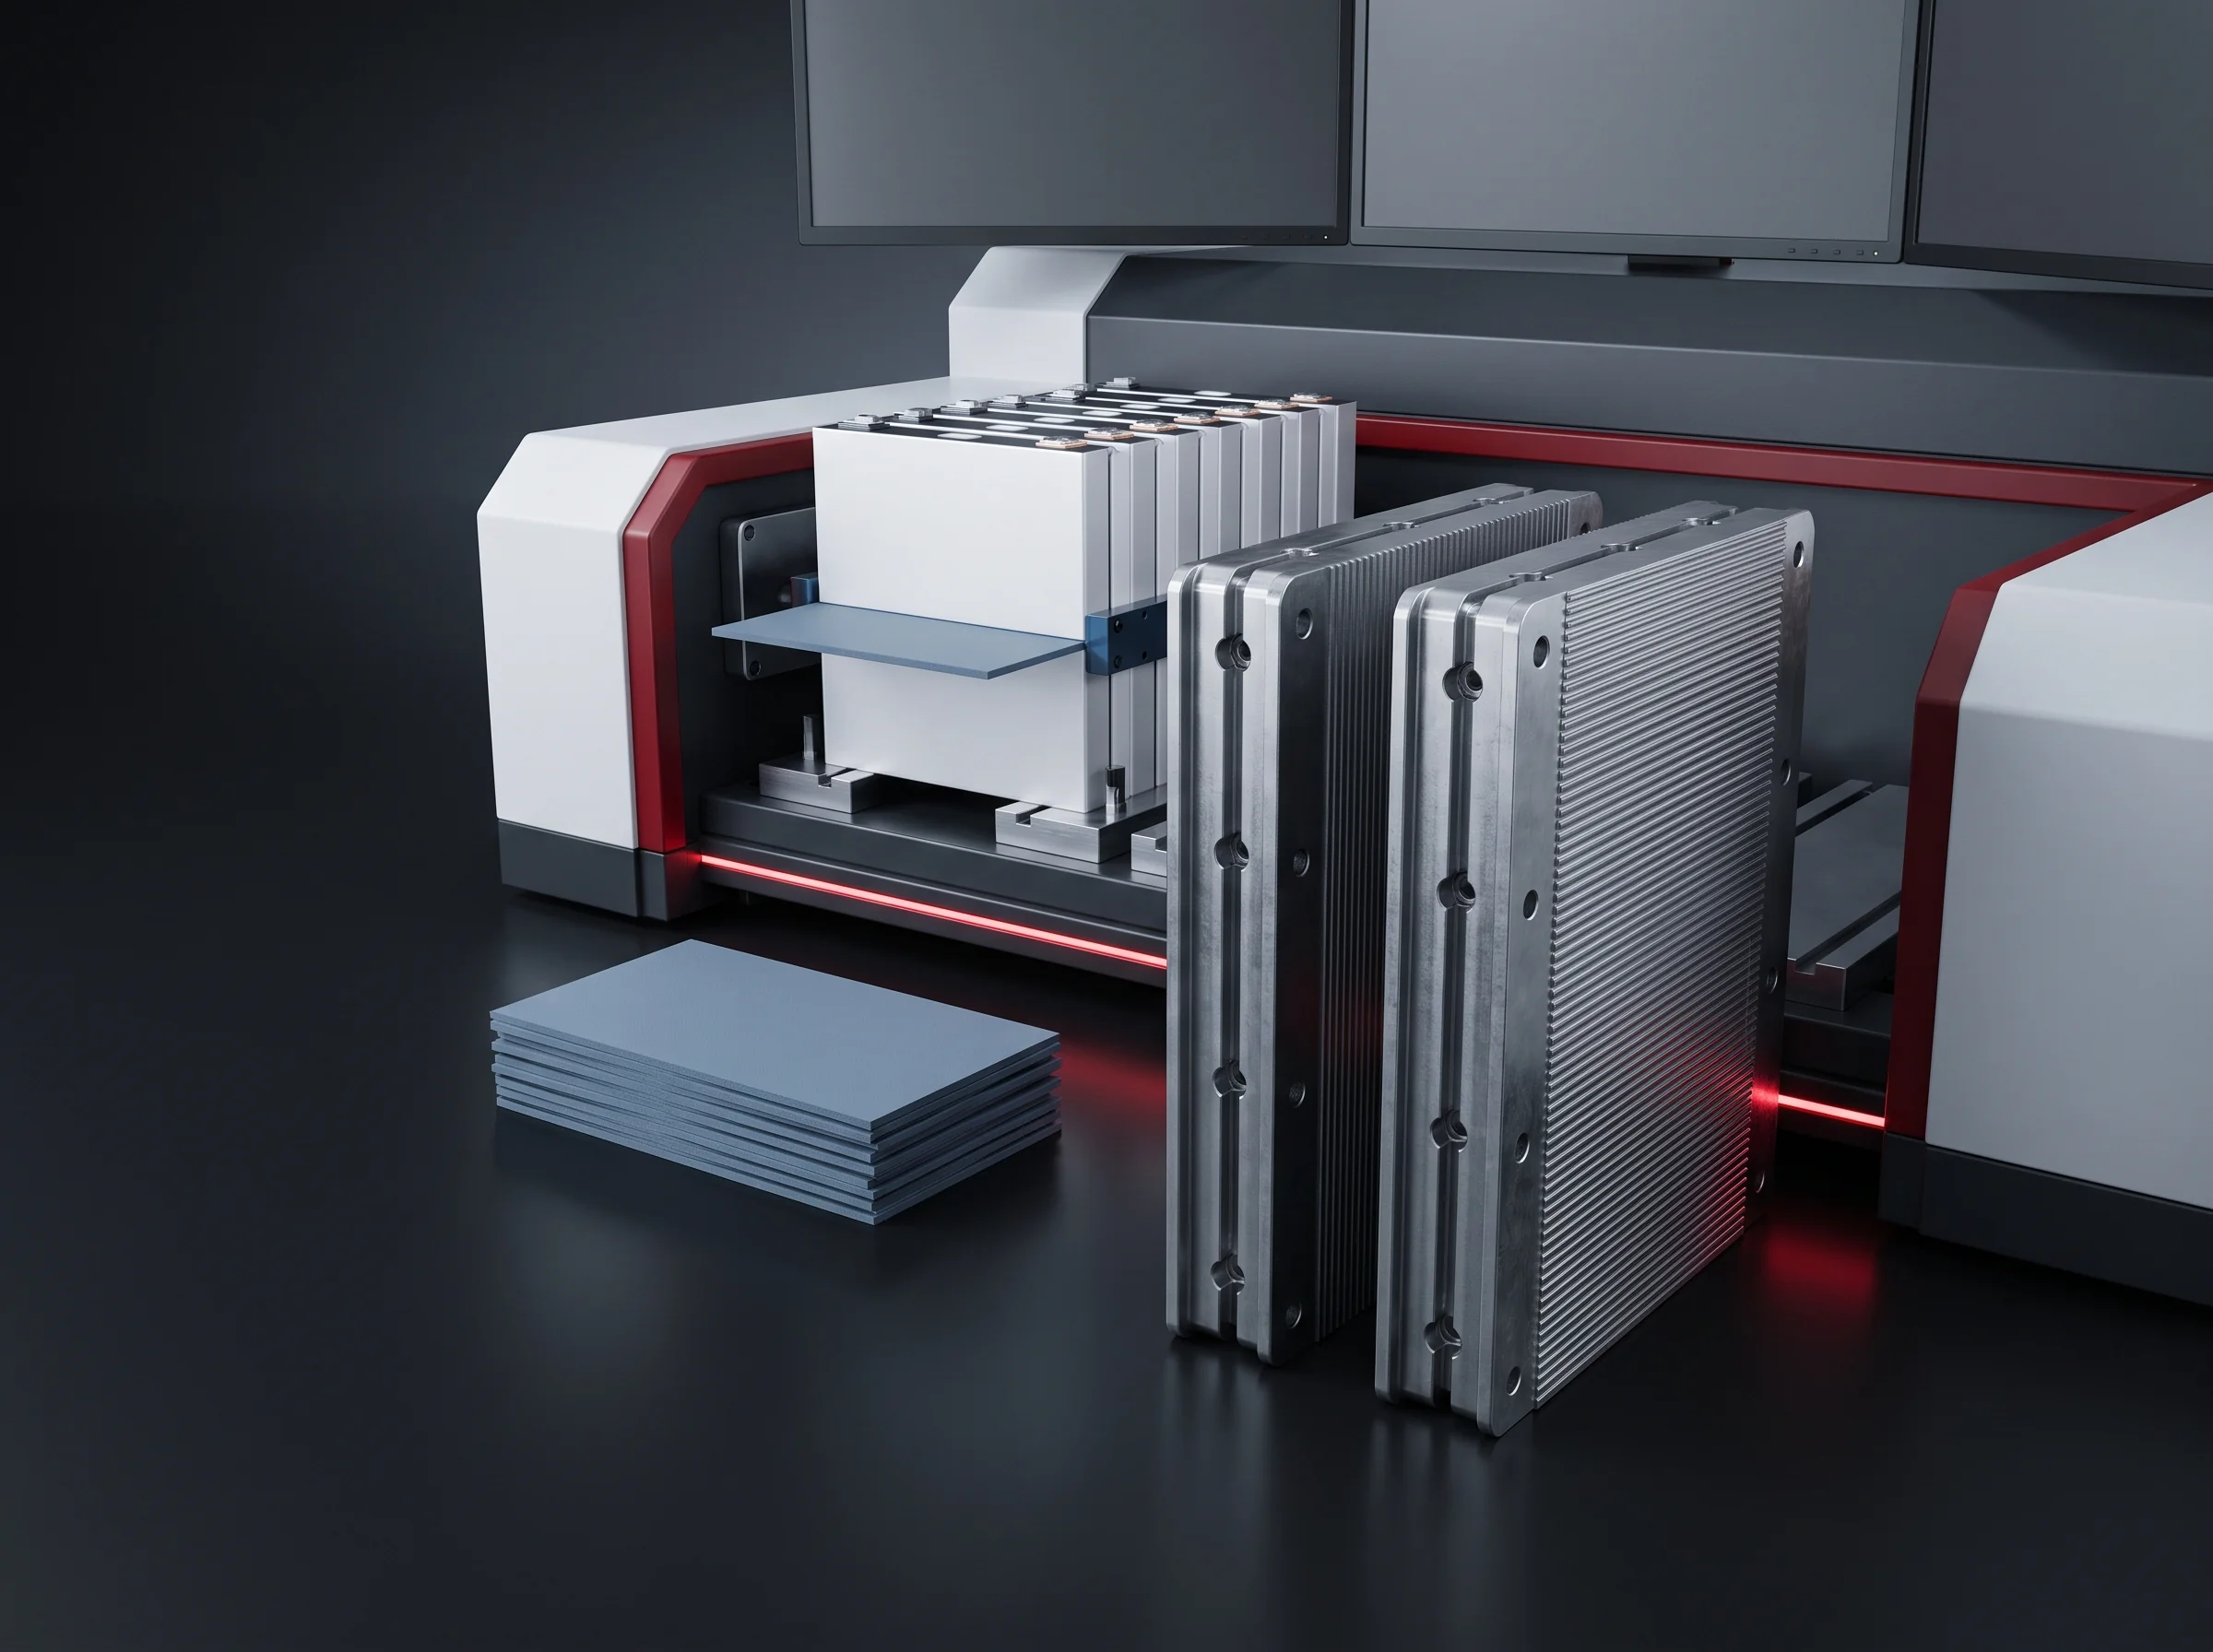
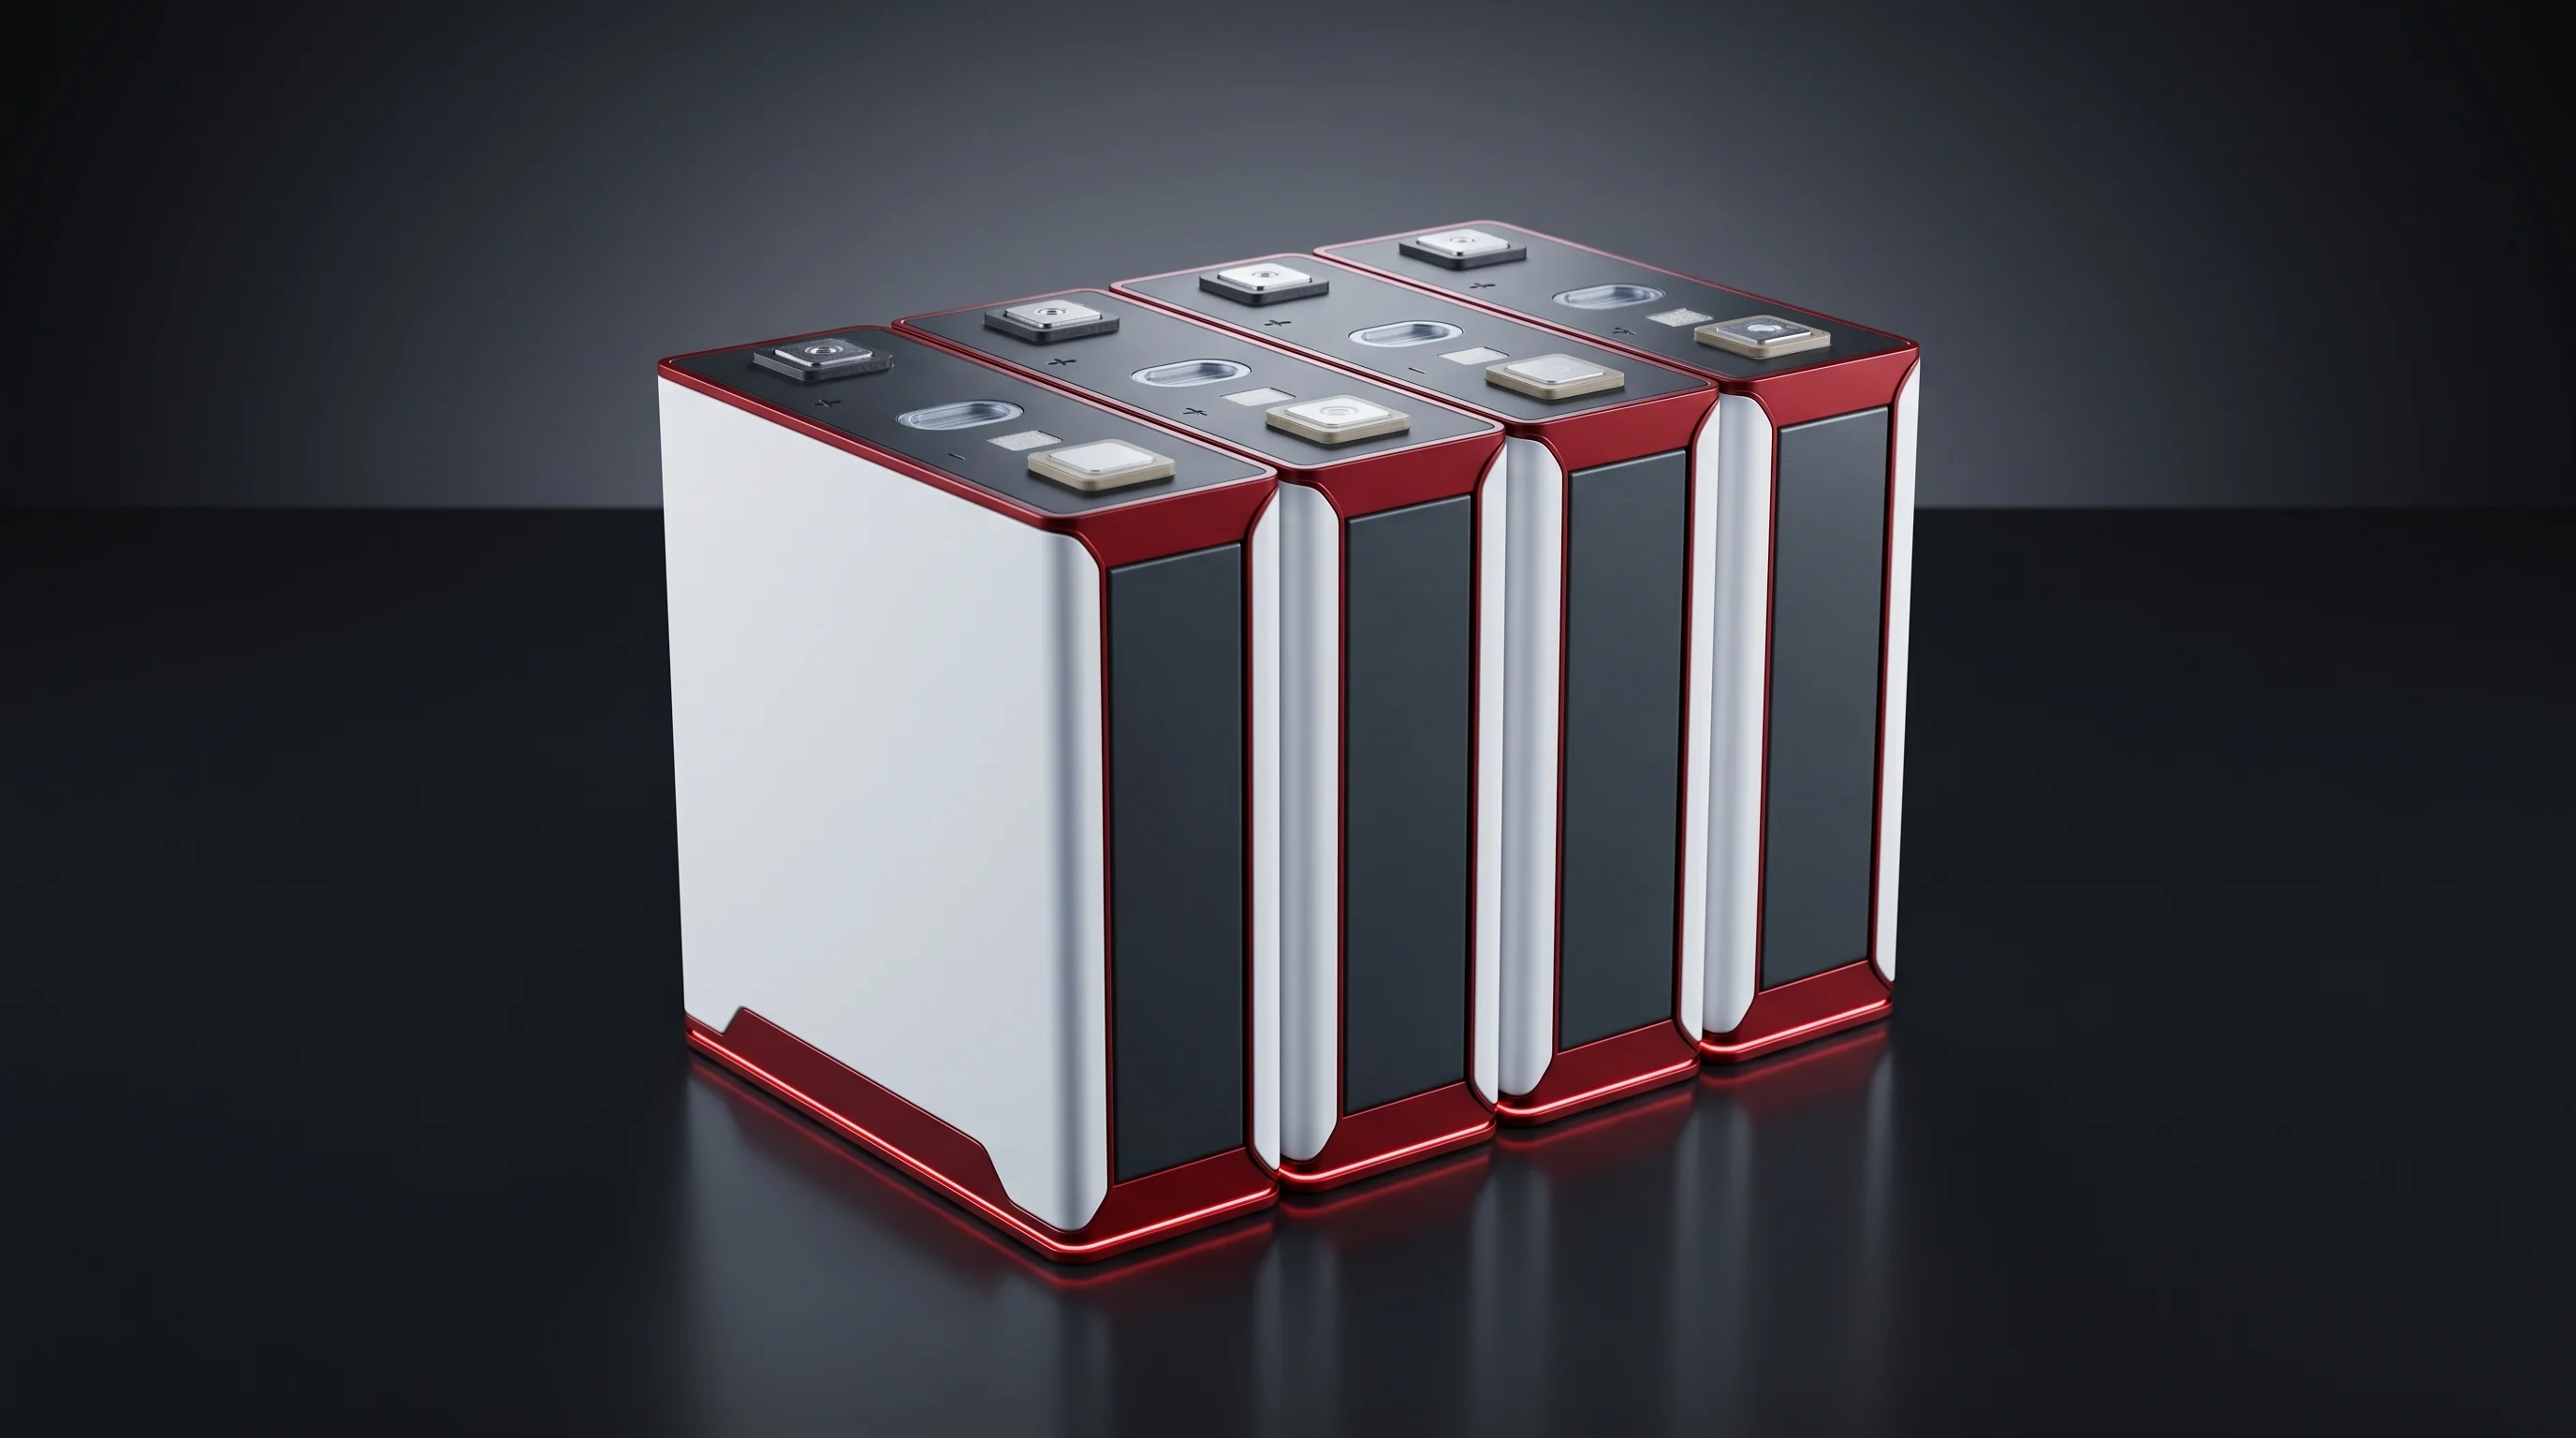
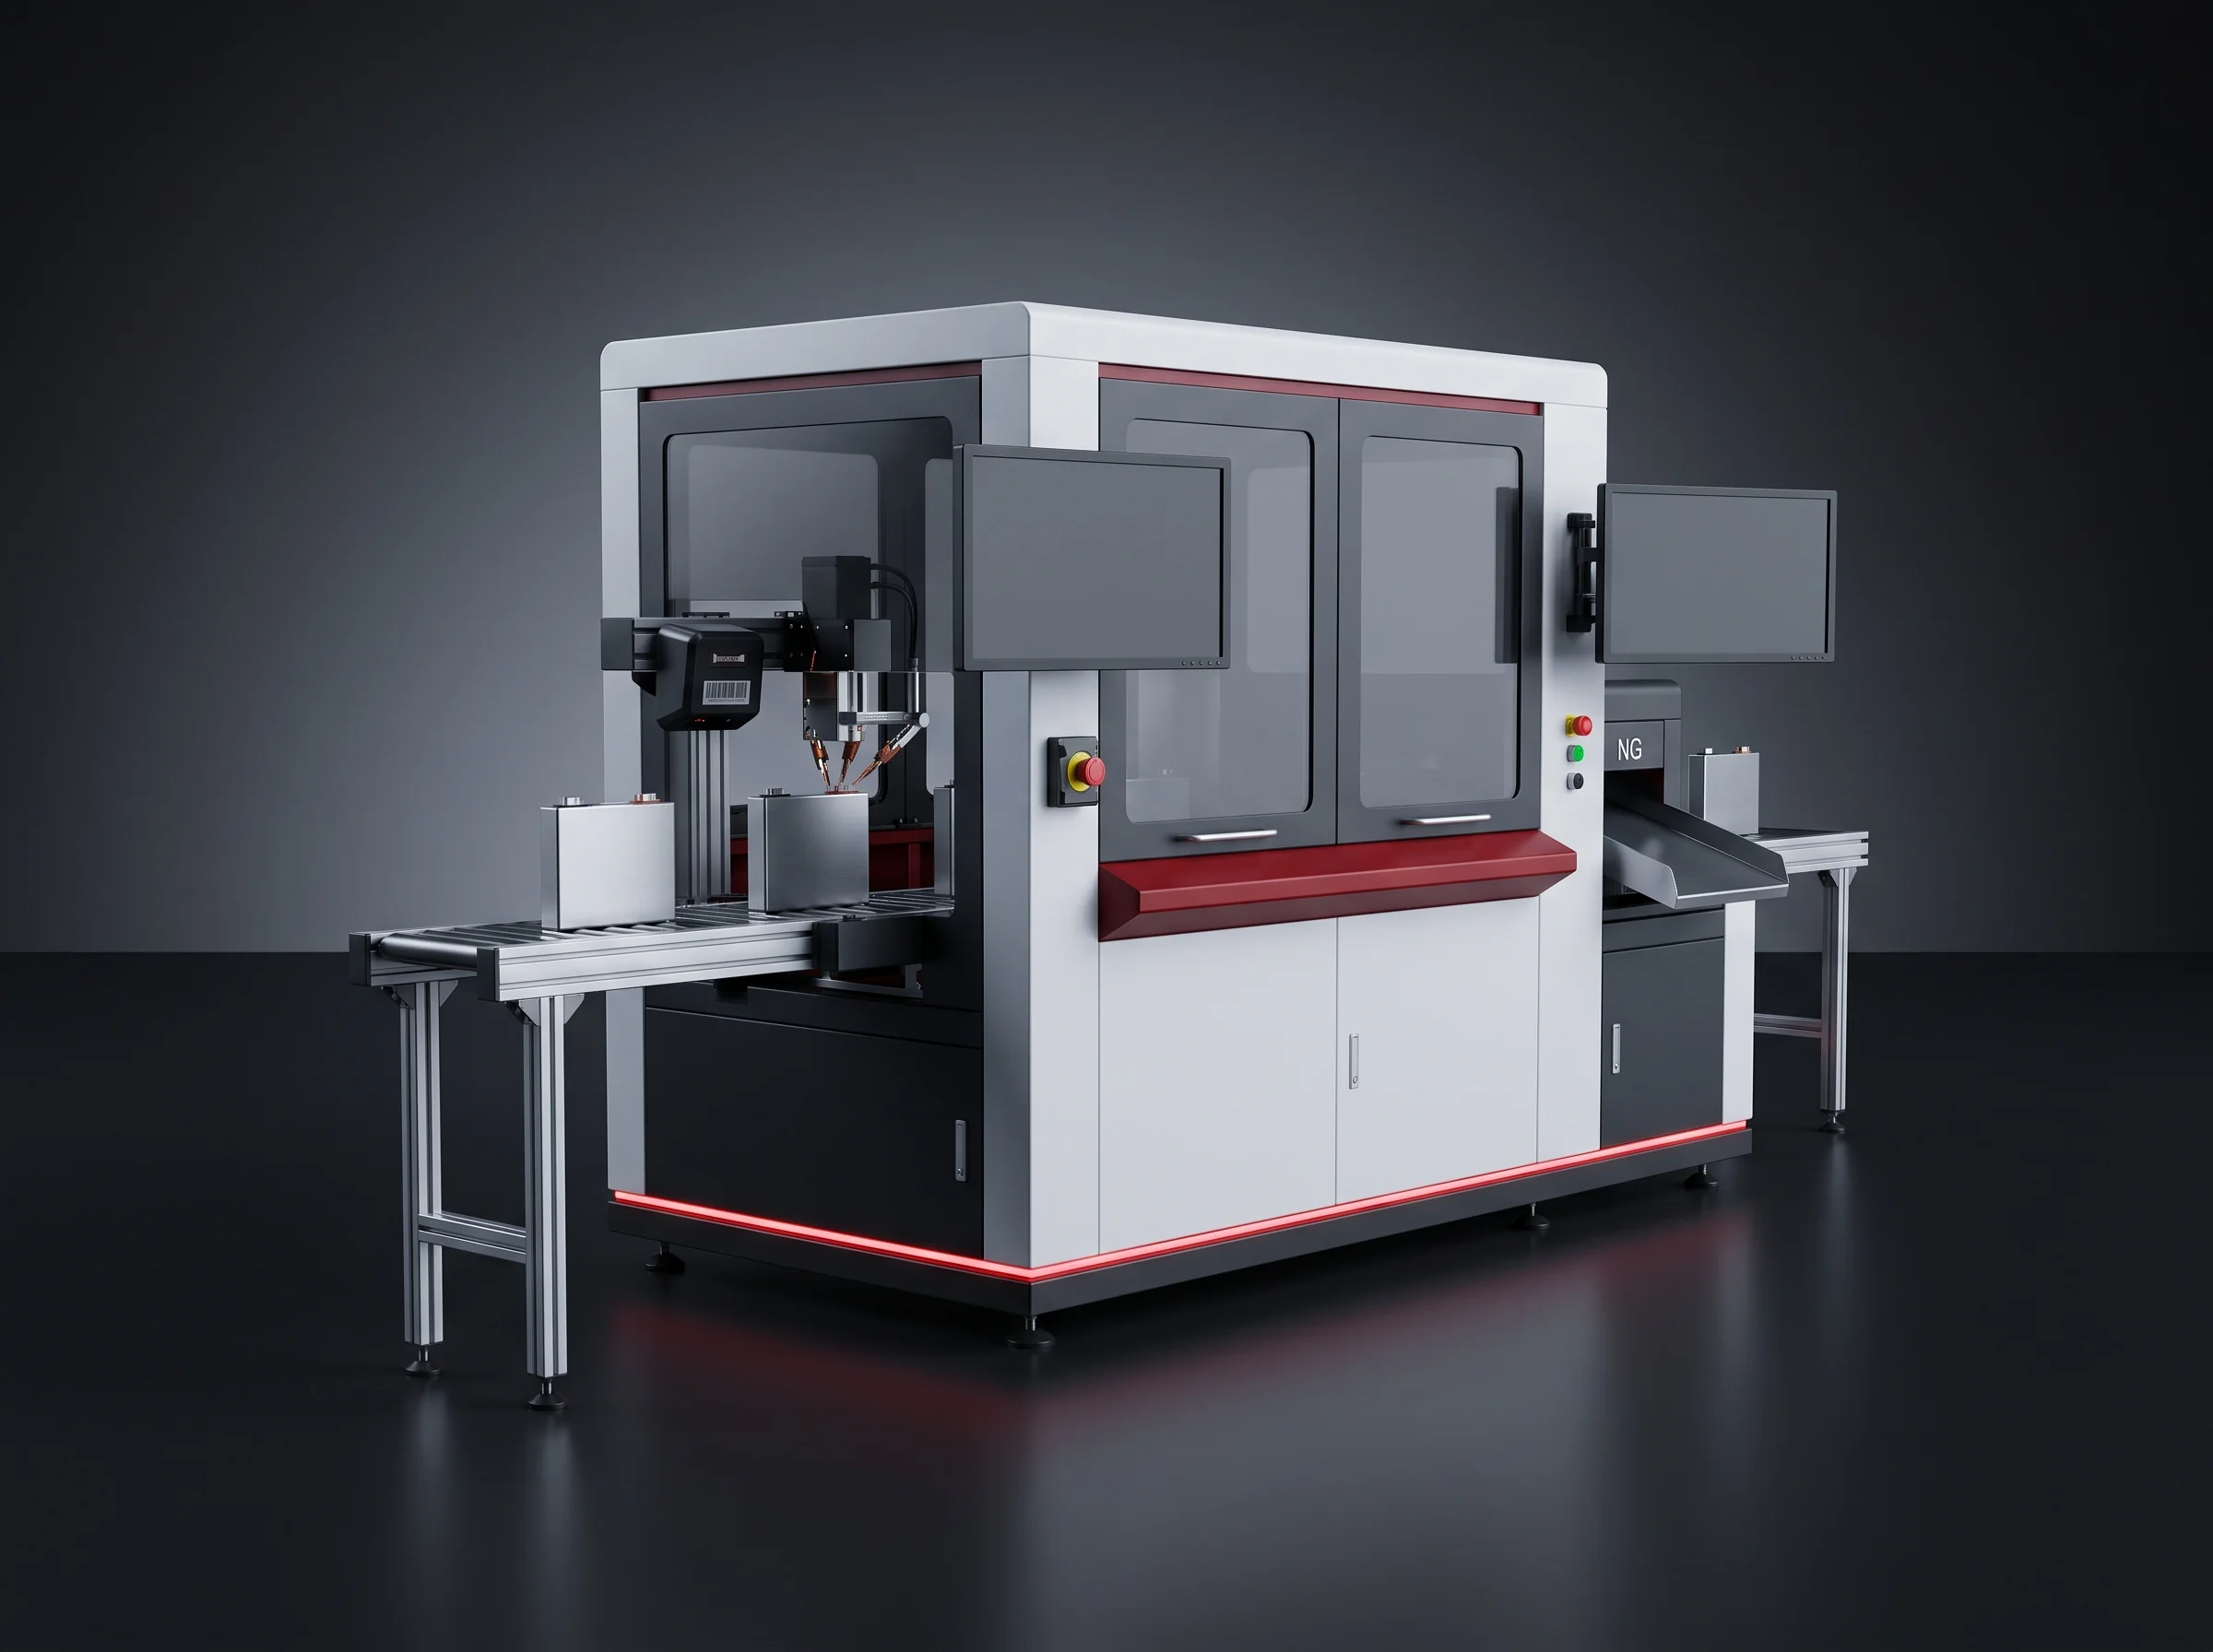
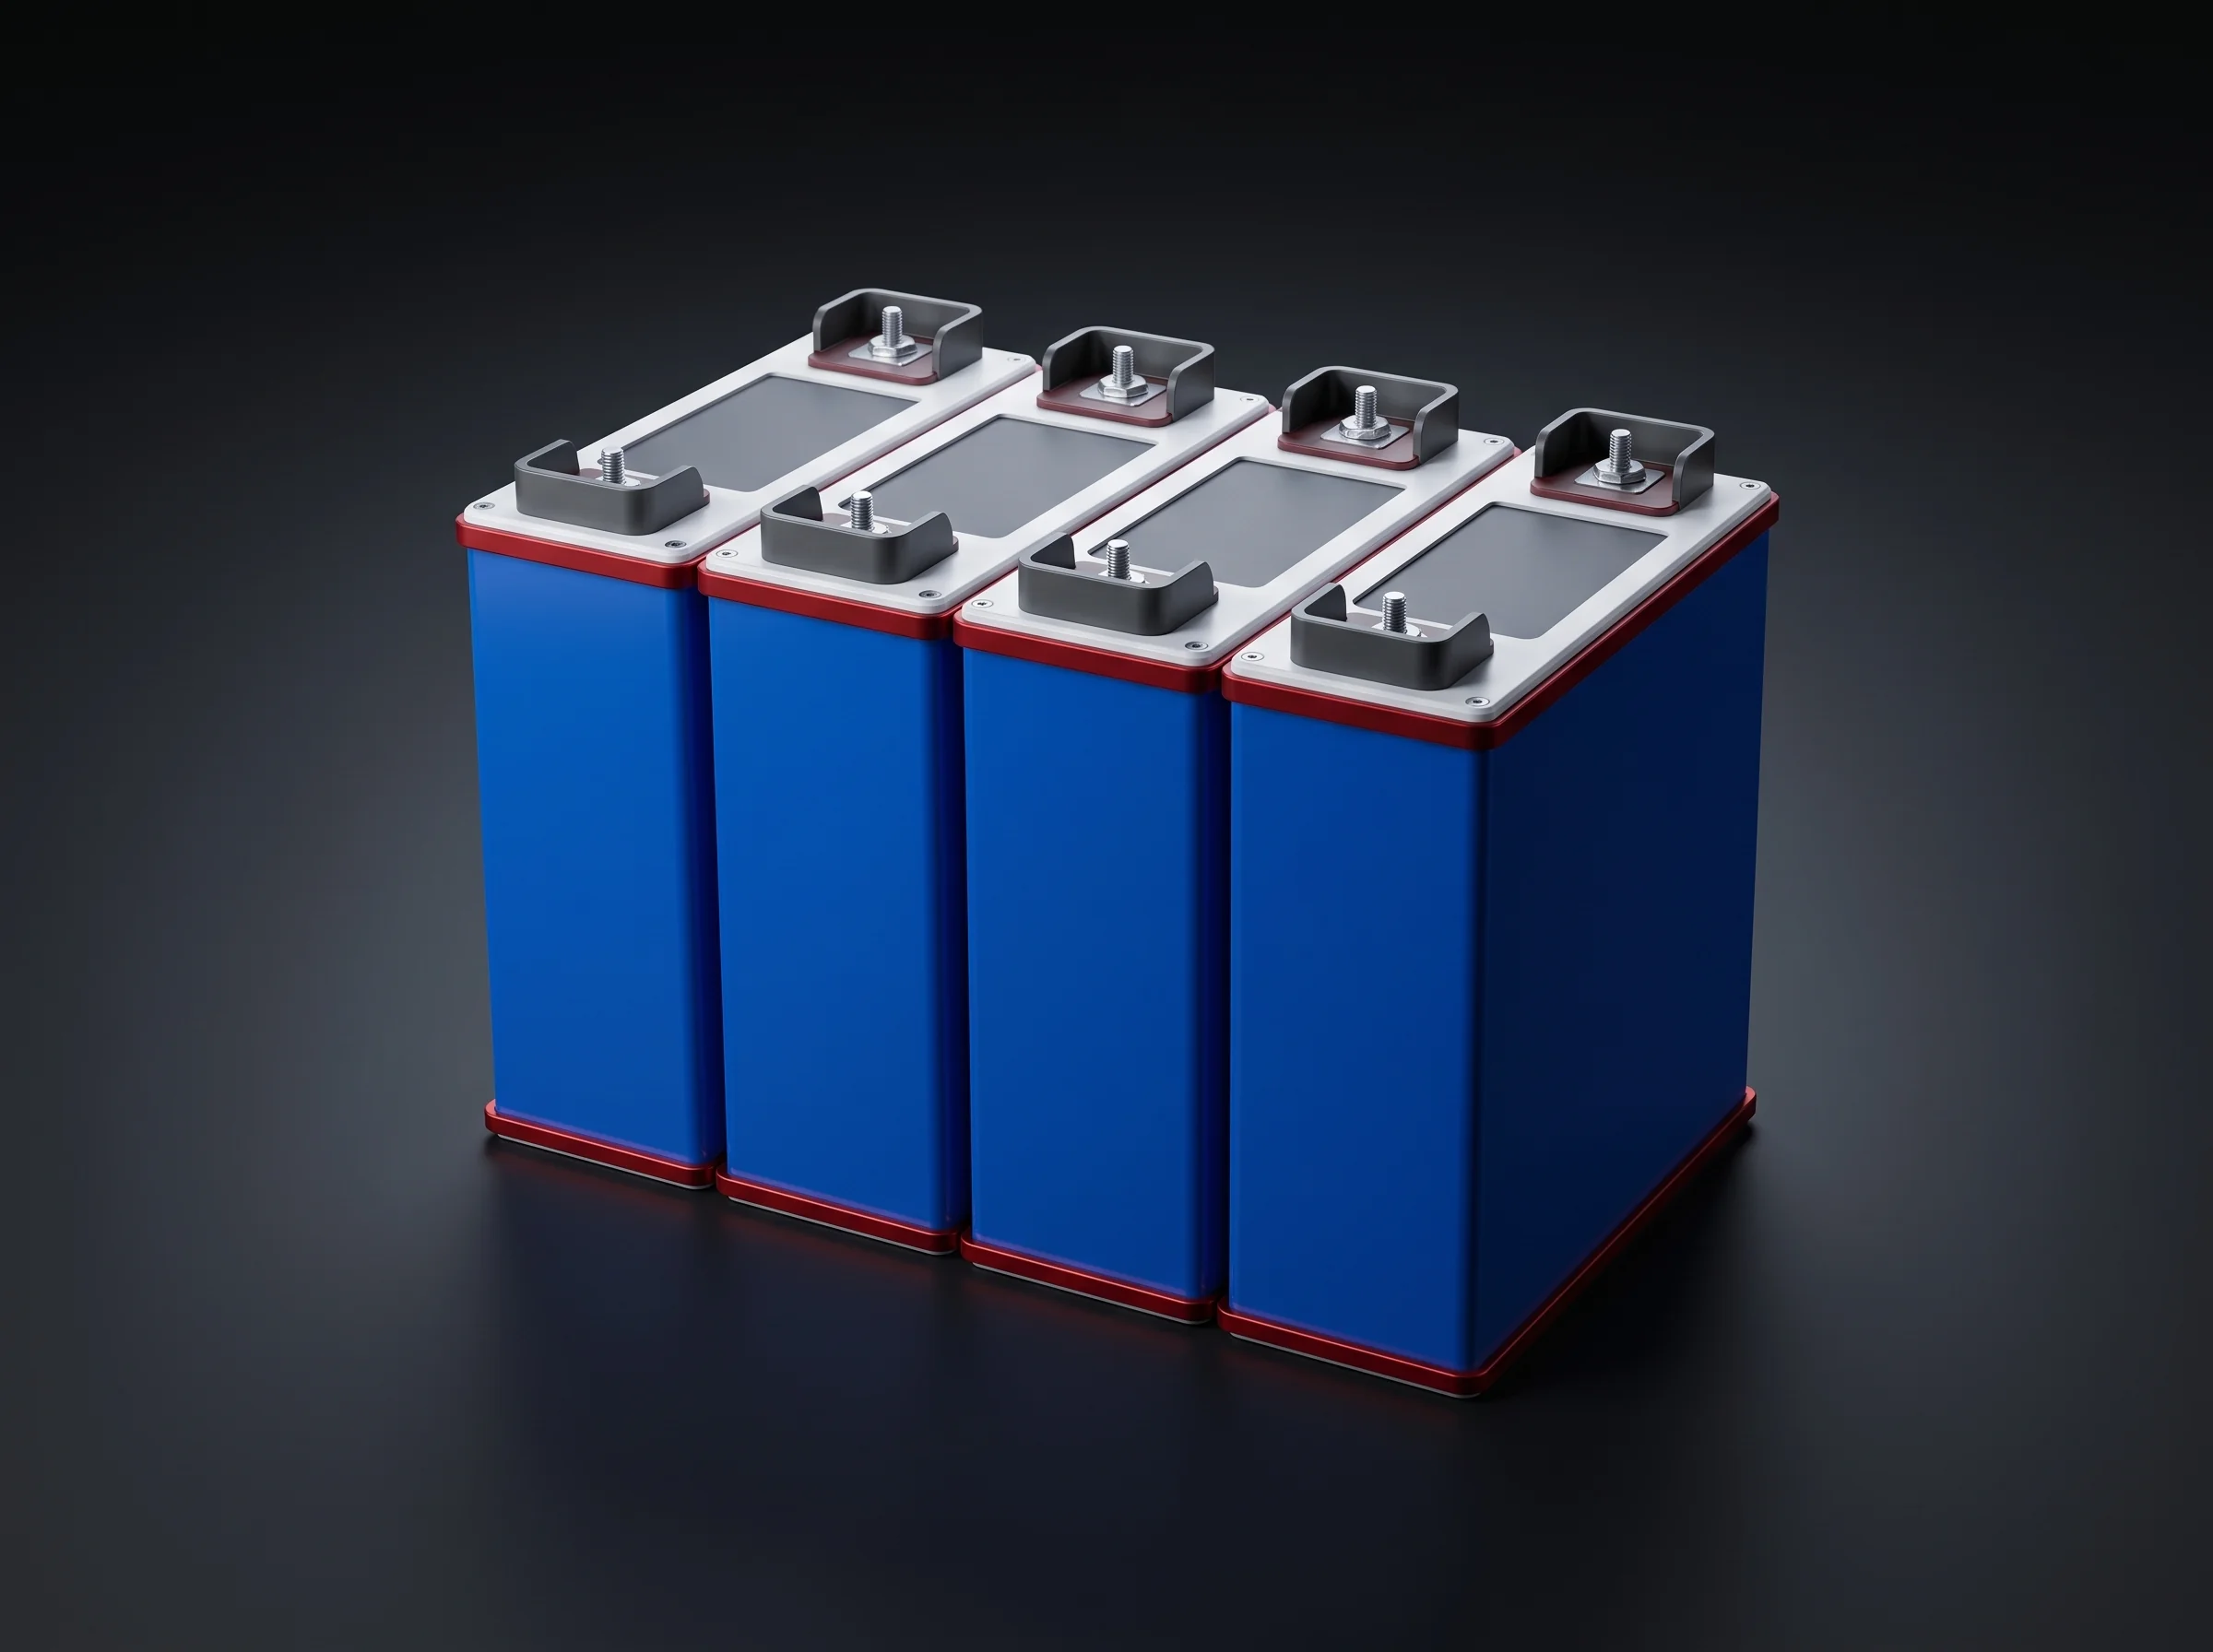
The stack arriving holds 8 to 24 prismatic cells, end plates and insulation sheets placed by the station ahead. The press takes it as final: closes it to a stored target force, holds it for the recipe dwell, measures the module, bands it, and hands it on for polarity and insulation testing.
The blueprint module
The module quoted against is a 1P13S at 978.4 × 178.9 × 205 mm, 100 kg or less, at 90 seconds or less per cycle with banding counted in. Others run on the same station inside the published span, on their own tooling and recipe.
Who reads this page
- Specifying a whole segment
- 17 stations
- Replacing one press
- 1 station
- Moving to a new module
- Tooling + recipe
- Reply on a drawing
- Within 24 h
Process and equipment engineers in module and pack plants. Send a module drawing and a recipe outline with a tooling list comes back inside a working day.
One cycle
One Module, Cycle By Cycle
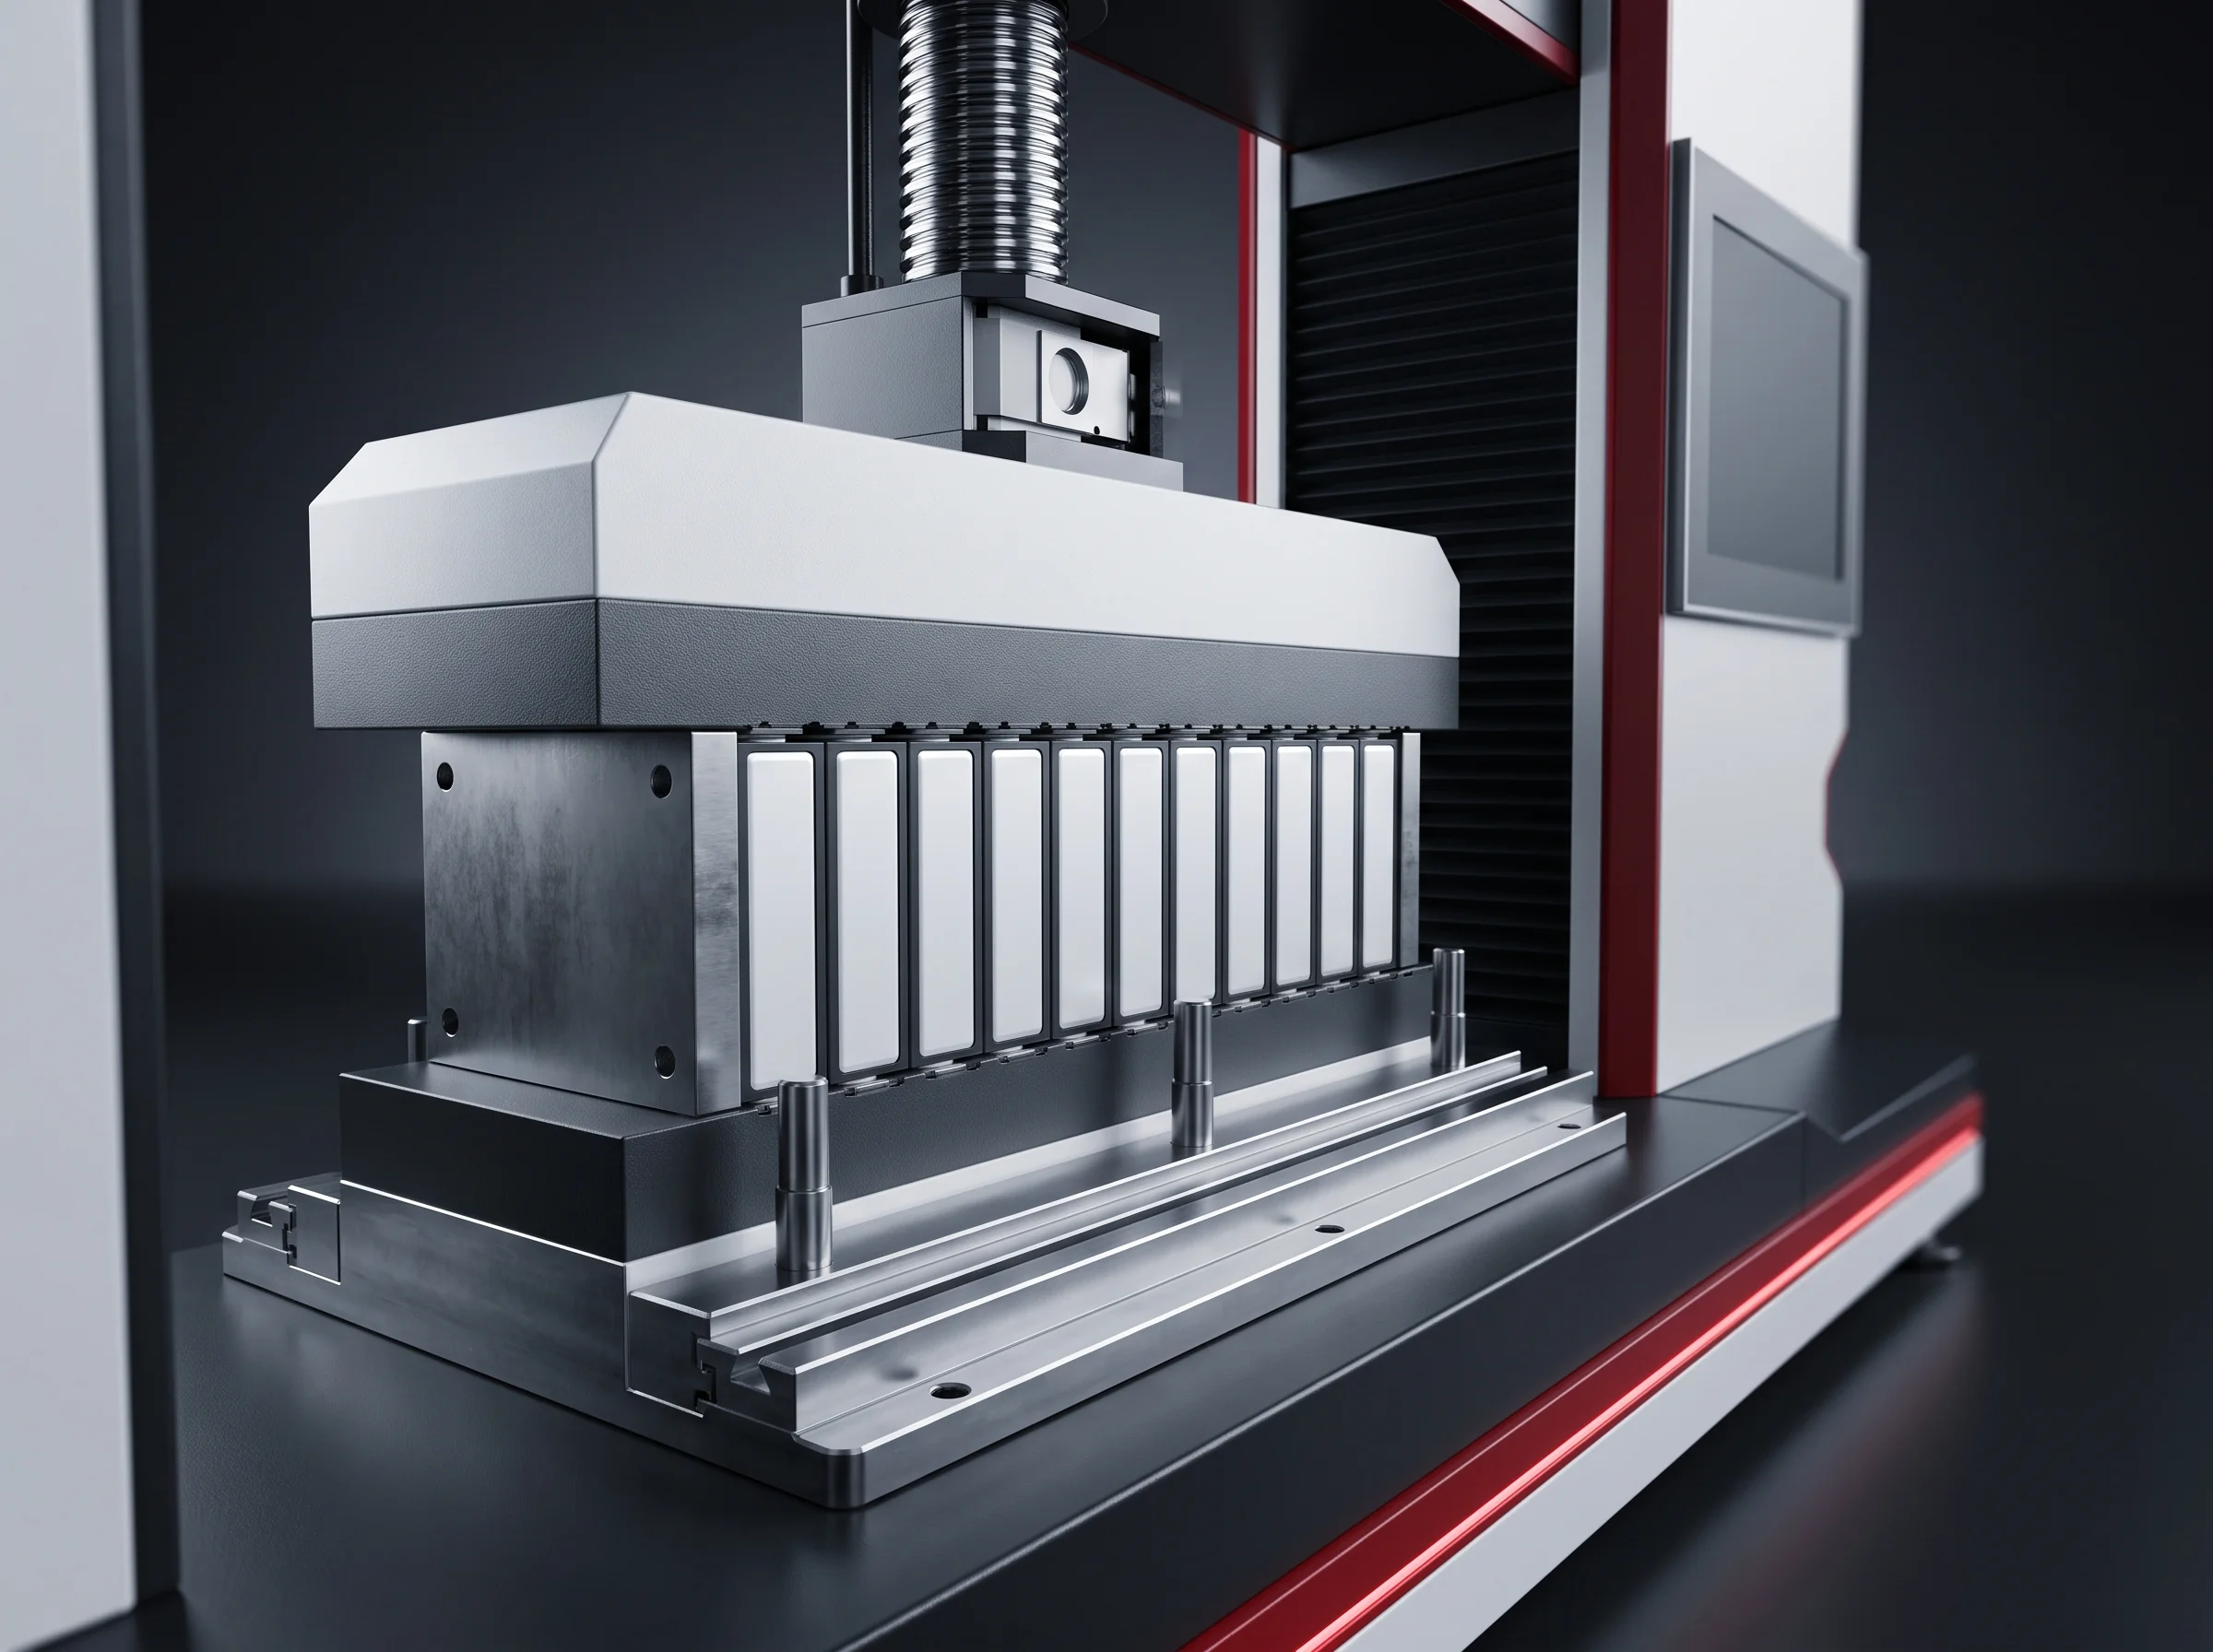
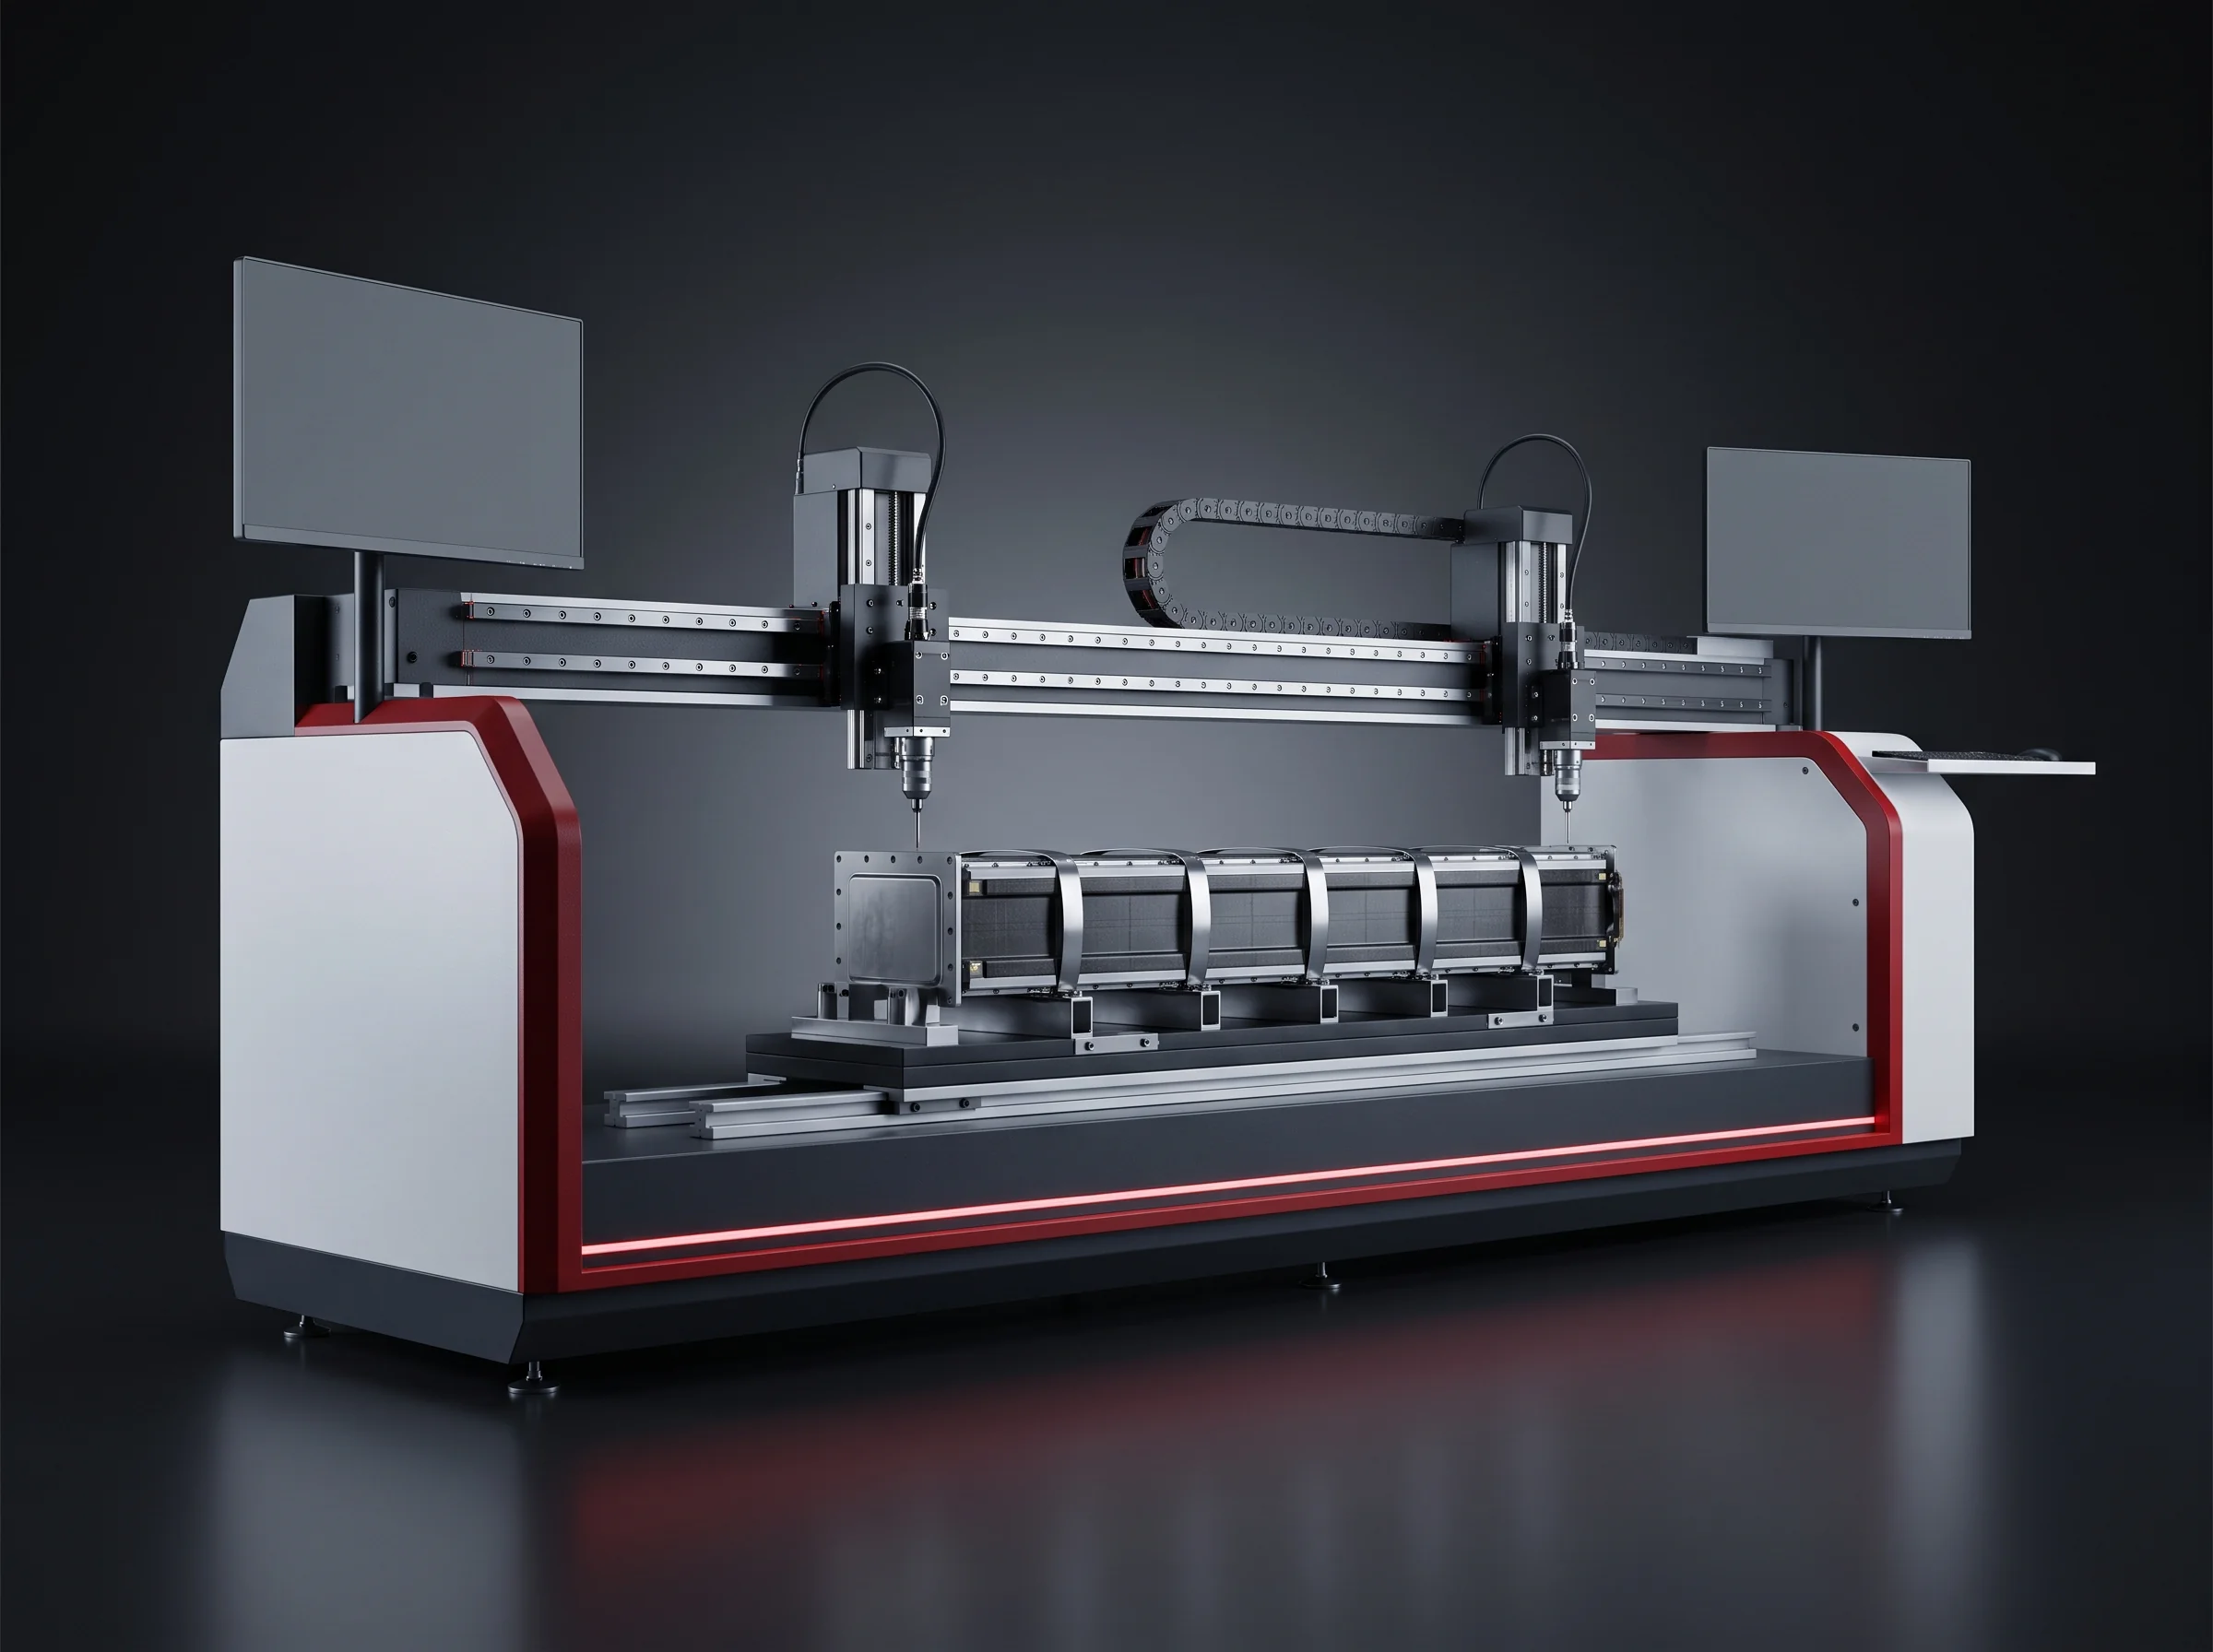
Five things happen between the handover in and the handover out; the recipe governs four of them.
Receive
Close
Hold
Measure
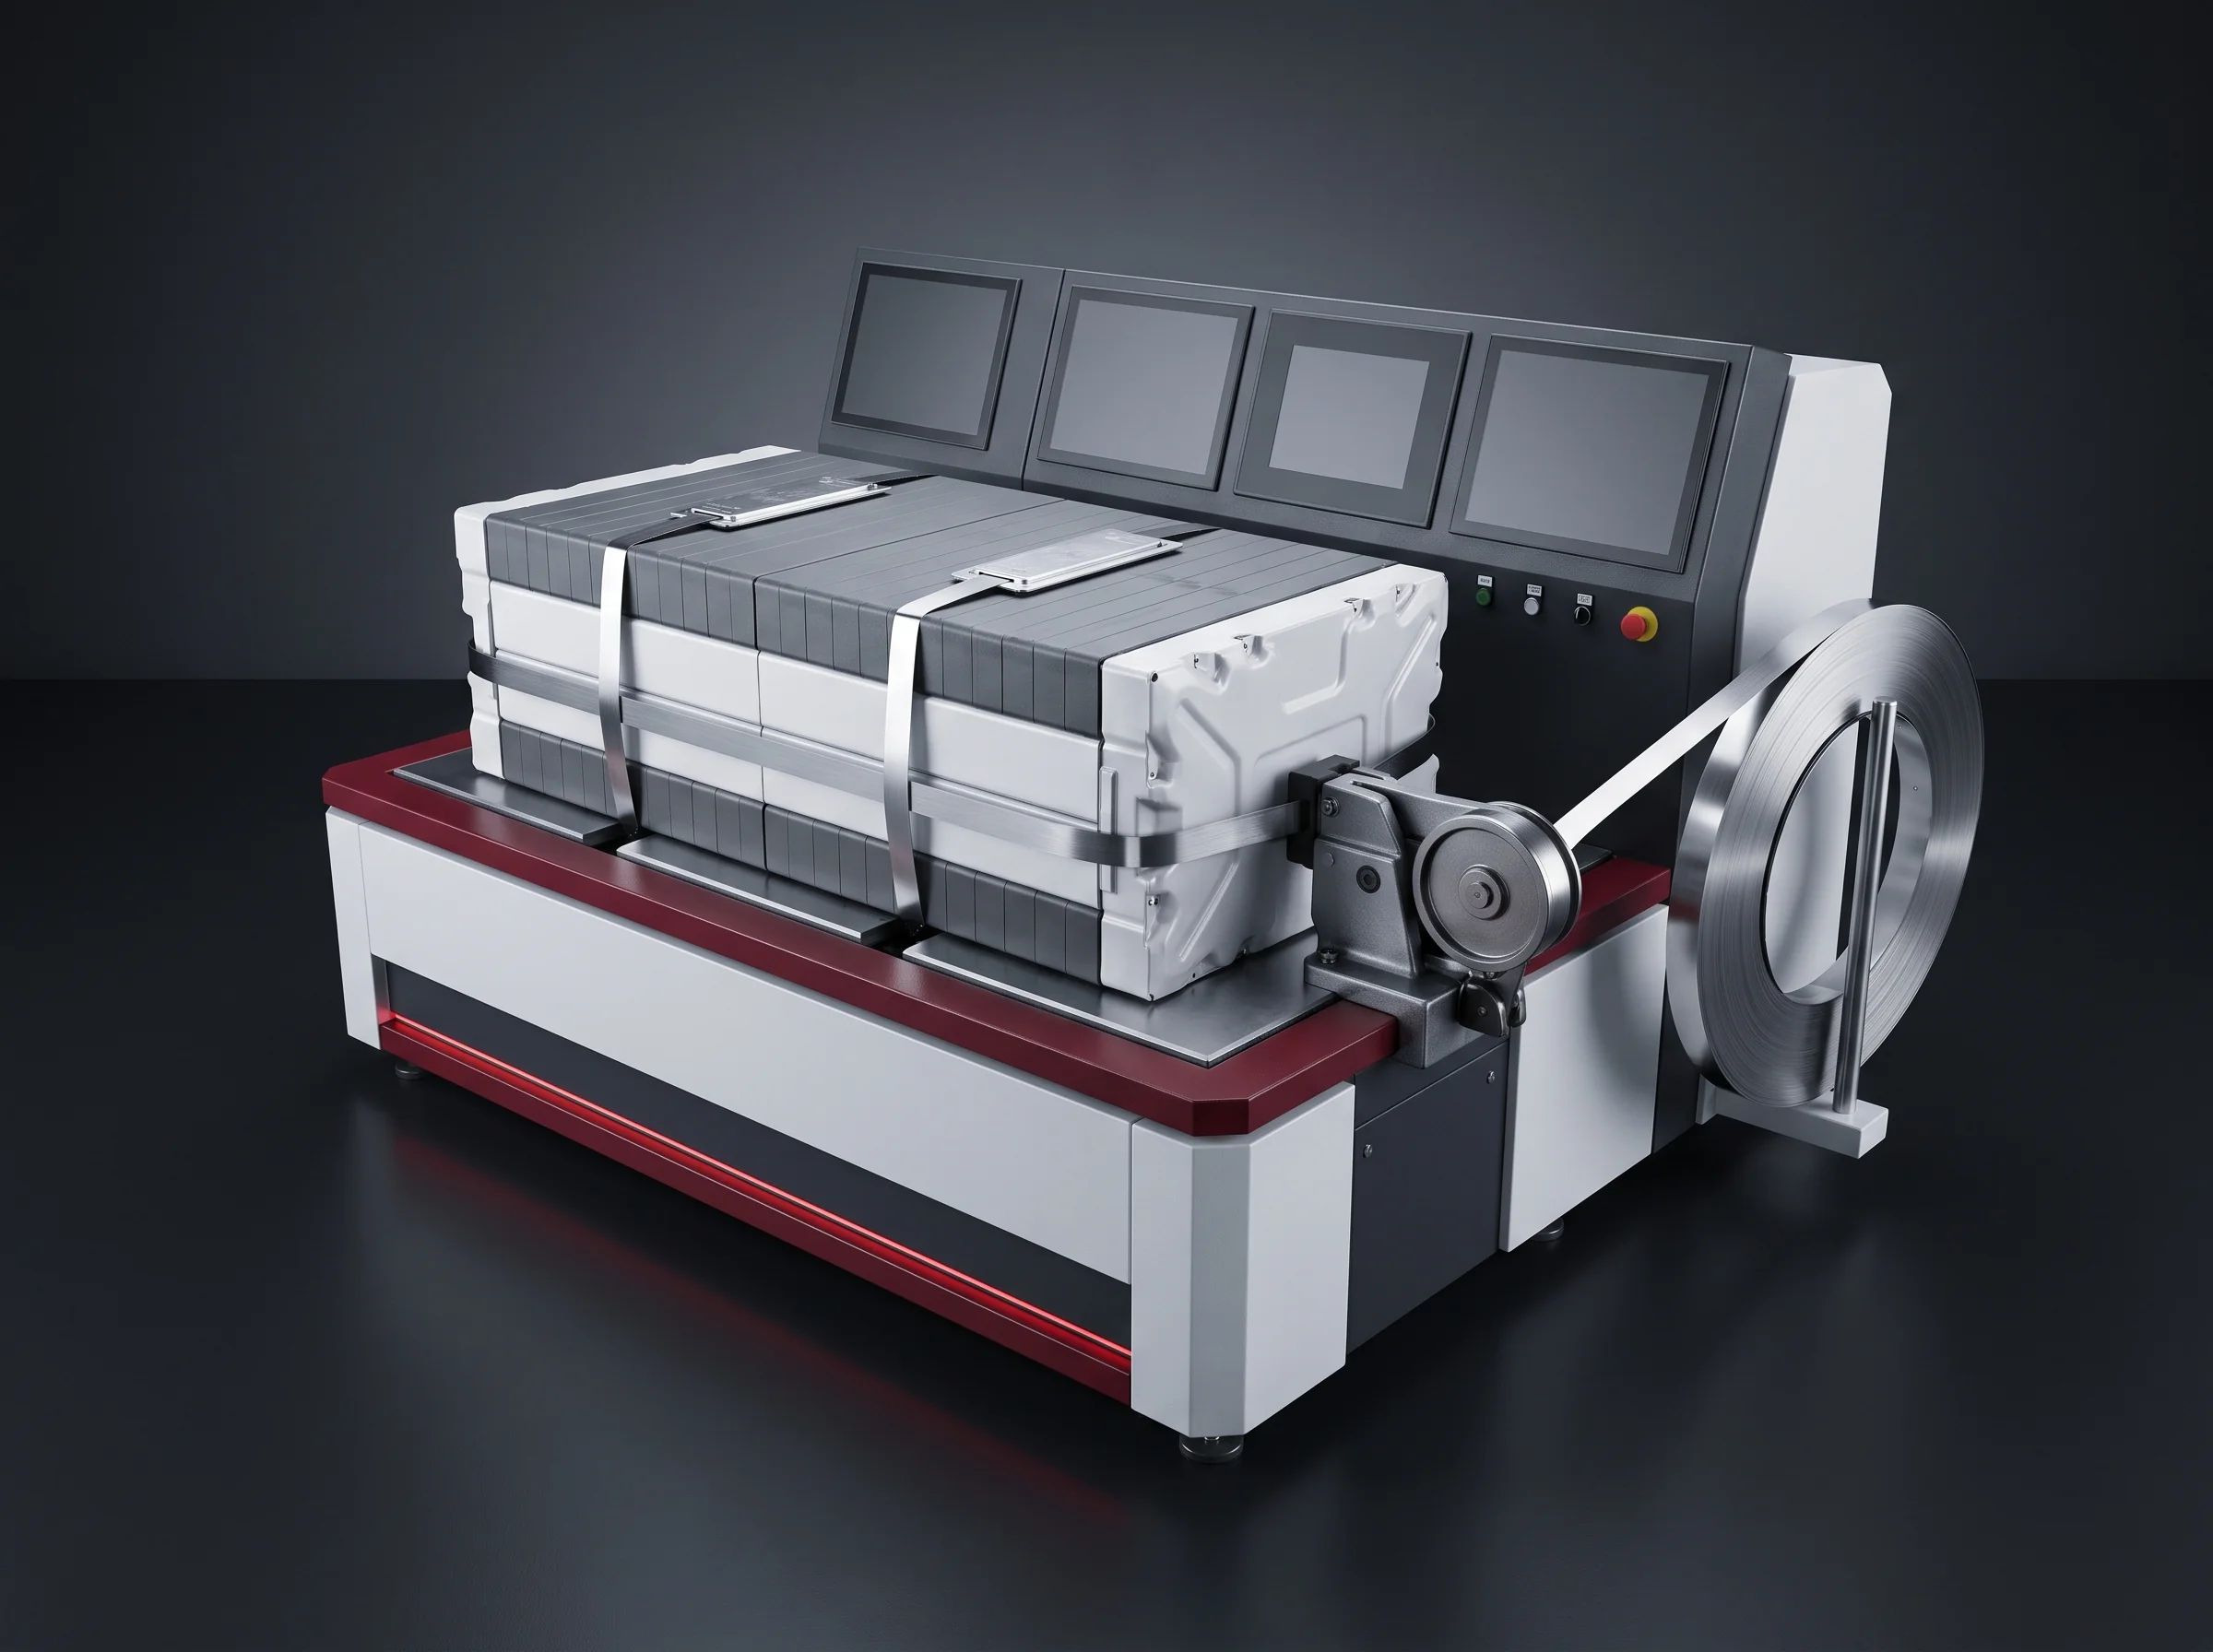
Band
Without the bands the stack relaxes and the module reaching the welder is a different length from the one measured — which is why banding sits inside this station.
Five figures the station is quoted on, before any is set against your own module.
- 0–8000 NServo pressing force
- 10 NForce resolution
- 1 kHzCurve sampling
- ±0.5 mmPost-press length
- ≤90 sCycle, banding in
Every figure, one table
The BLP-SP Datasheet
Rows marked at order are fixed when the station is built. The rest are recipe values, ranges or delivered dimensions — interface figures included.
| Item | Figure | Status |
|---|---|---|
| Pressing force | 0–8000 N, servo controlled, monitored live by pressure sensor | At order |
| Force resolution | 10 N | At order |
| Force curve | Recorded through the whole press, sampled at 1 kHz | At order |
| Dwell time | 0–60 s, set by recipe | Recipe |
| Pressing span | 300–1100 mm | At order |
| Cells per module | 8–24, blueprint module 1P13S | Per module |
| Post-press length measurement | ±0.1 mm | At order |
| Post-press module length tolerance | ±0.5 mm | Delivered |
| Cycle time | 90 s or less per module, 1P13S with banding counted in | Per module |
| Recipes | Stored by module type: target force, dwell, target length, banding passes | Recipe |
| Transfer height | 900 ± 50 mm, adjustable, set against your existing line | Adjustable |
| Module handover | Module travels on its fixture, handed over by BLP-CV conveyor | Interface |
| Communication | PROFINET. Force curve and post-press length uploaded to MES by module number | At order |
| Rated power | 8 kW | At order |
| Supply | 380 V / 50 Hz | Plant side |
| Compressed air | 0.5–0.7 MPa, 200 L/min or less | Plant side |
Seven rows built in
Force range, 10 N resolution, the 1 kHz curve, the span, the ±0.1 mm measurement, the PROFINET link and the 8 kW rating. A wider span is a different frame, not a setting.
Two rows carry the rest of this page: the 1 kHz curve, and the ±0.5 mm.
The record of one press
The Force Curve Of One Press
A press is an event with a duration, and one number describes neither part of it. The same peak reached fast and reached slowly leaves two different modules; a peak that holds through the dwell and one that decays through it leaves two more. So the station records the press rather than reporting it.
The slope
The knee
The dwell
Three quantities, one record
Force, platen position and time are sampled together at 1 kHz through the approach, the loading ramp and the whole dwell — roughly ninety thousand points across a ninety-second cycle. Force itself is read by load cell and the drive closes on that reading rather than on an inferred cylinder pressure.
What a curve outside its shape triggers
- The module is held at the station under its module number, not released and found later.
- It goes to the process engineer with its curve attached, rather than to a scrap note.
- Everything downstream assumes the stack has stopped moving — so a doubtful press is worth stopping here and nowhere else.
- The dwell on the record is the actual one, not the requested one: a hold cut short to make a takt shows on the curve.
Range, resolution, dwell
Force Range, Resolution And Dwell
Both ends of the range earn their place, and the step between them is why a target is met rather than approached.
Where your target sits is read off your drawing, written into a recipe and qualified on a first article.
Dwell is a module value
Dwell runs from 0 to 60 seconds, chosen for the module type rather than for the shift. The recorded dwell is the actual one, which is what makes a shortened hold visible afterwards.
Set by recipe
Read by load cell
Recorded as run
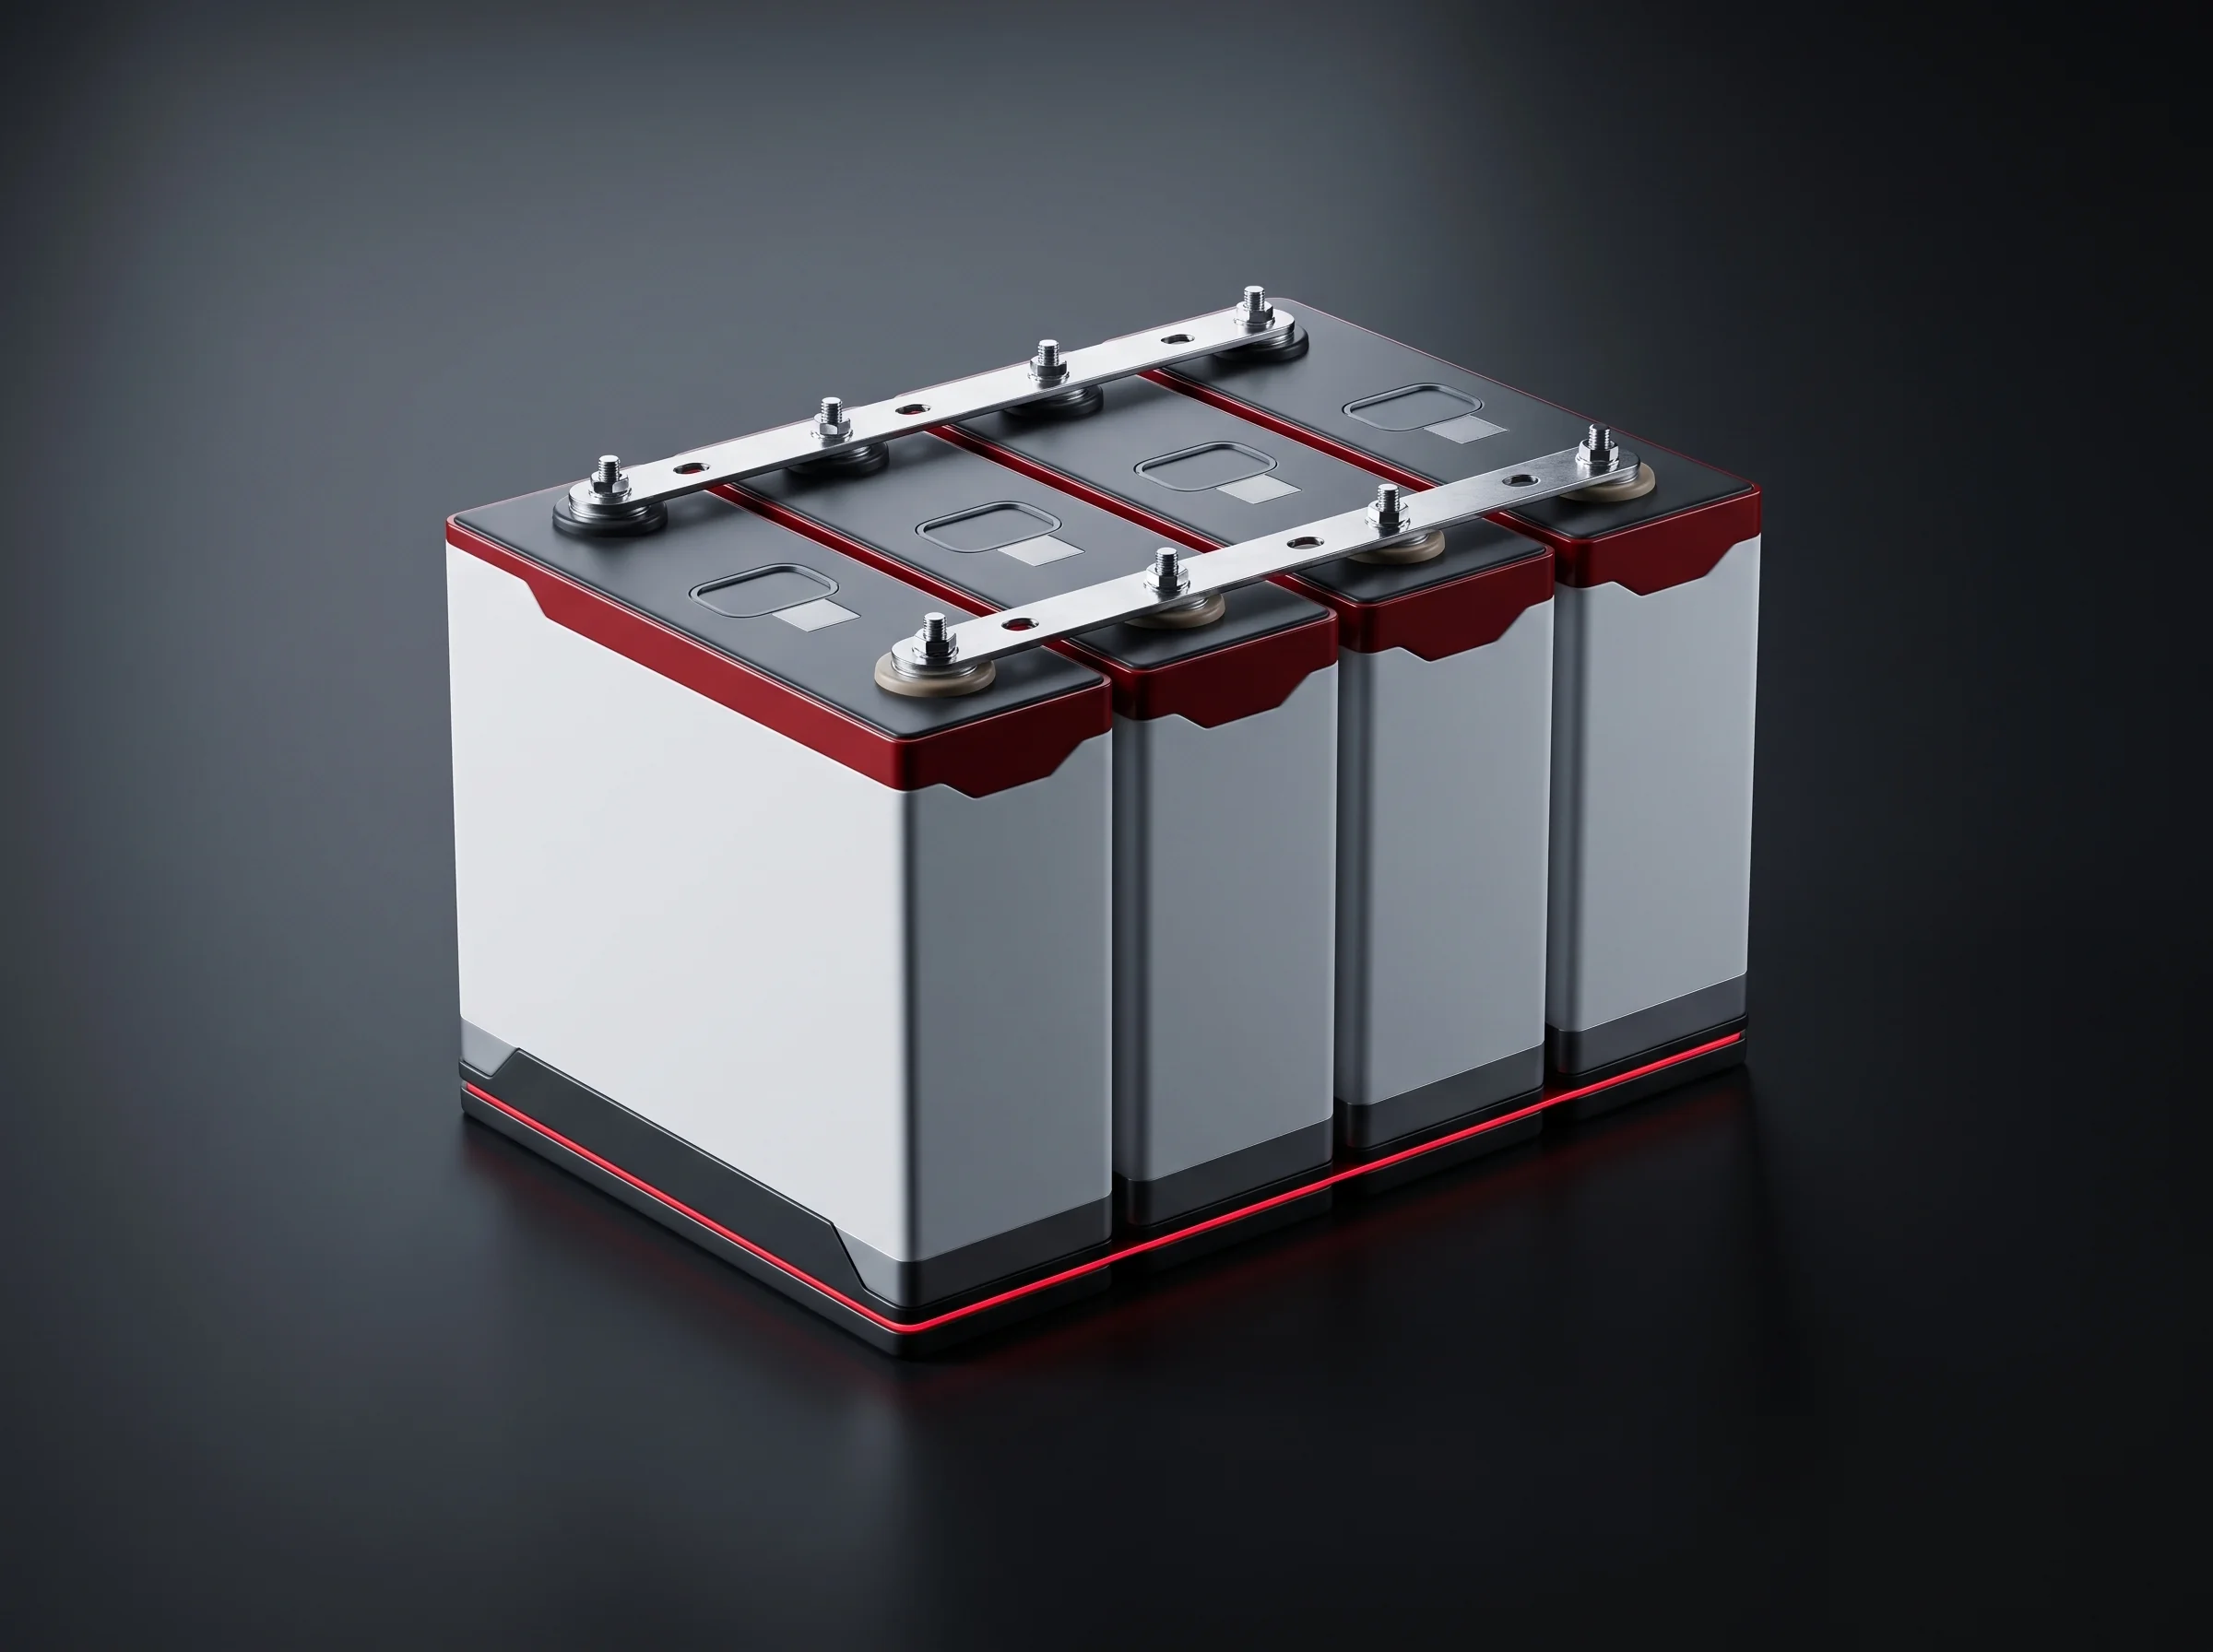
The number that leaves
The Length After The Press
Two length figures are published and they answer different questions. Reading one as the other is how a specification becomes an argument three months later.
Measured under load, the module is as short as it will ever be. Measured again after release, with the bands on, it settles to the length the enclosure was drawn for — and that settled number is the one judged.
Outside tolerance, it stays here
One that falls outside ±0.5 mm is held at the station rather than sent on, because every station after this one treats the length as already true.
What the next stations inherit
- Terminal addressing locates to ±0.2 mm on a module whose length is known.
- The busbar welding station welds a located part rather than a placed one, because the CCS assembly sat on a module of the expected length.
- Pack assembly bolts the module into an enclosure drawn for that dimension, fixing points where the drawing said.
- None of them re-measures it — which is why it is judged here.
Send The Module, Get The Recipe Back
Module drawing, cells per module, and the post-press length and tolerance you work to. Back comes the target force and dwell we would store, the tooling your module needs, and whether your module types share one set of it — within 24 hours.
Four items per module
Four Records Per Module Number
All four go out over PROFINET to your MES, indexed by module number, the moment the module leaves the station.
The force curve
The measured length
The recipe number
The banding passes
Records, not screens
A live pressure display tells the operator what is happening now. A stored curve tells your process engineer, six weeks from now, what happened to the module that came back from the field.
- Written per module rather than sampled per shift, so any module sits beside the hundred built either side of it.
- A press that drifts shows up as a shape moving across those records, long before it shows up as a module that fails.
Indexed by module number, over PROFINET.
Before the line ships
Acceptance On Your Own Modules
A batch of your modules is pressed and the spread of released lengths across that batch is handed over — not one good module, the distribution.
Three things fixed before the test
- Criteria firstPass criteria for force, dwell shape and released length, signed before any module is pressed.
- Your modulesYour own cells and end plates, on the tooling that ships with the station.
- Curves openedRecords are read together, module by module, rather than summarised in a report.
The station arrives with your module types already loaded as recipes, pressed and signed during acceptance.
Four values, three accounts
Recipes And The Three Accounts
A plant running three module types runs three recipes, selected by name rather than typed in at the start of a shift. Editing one is a different act from selecting one — and the station enforces that.
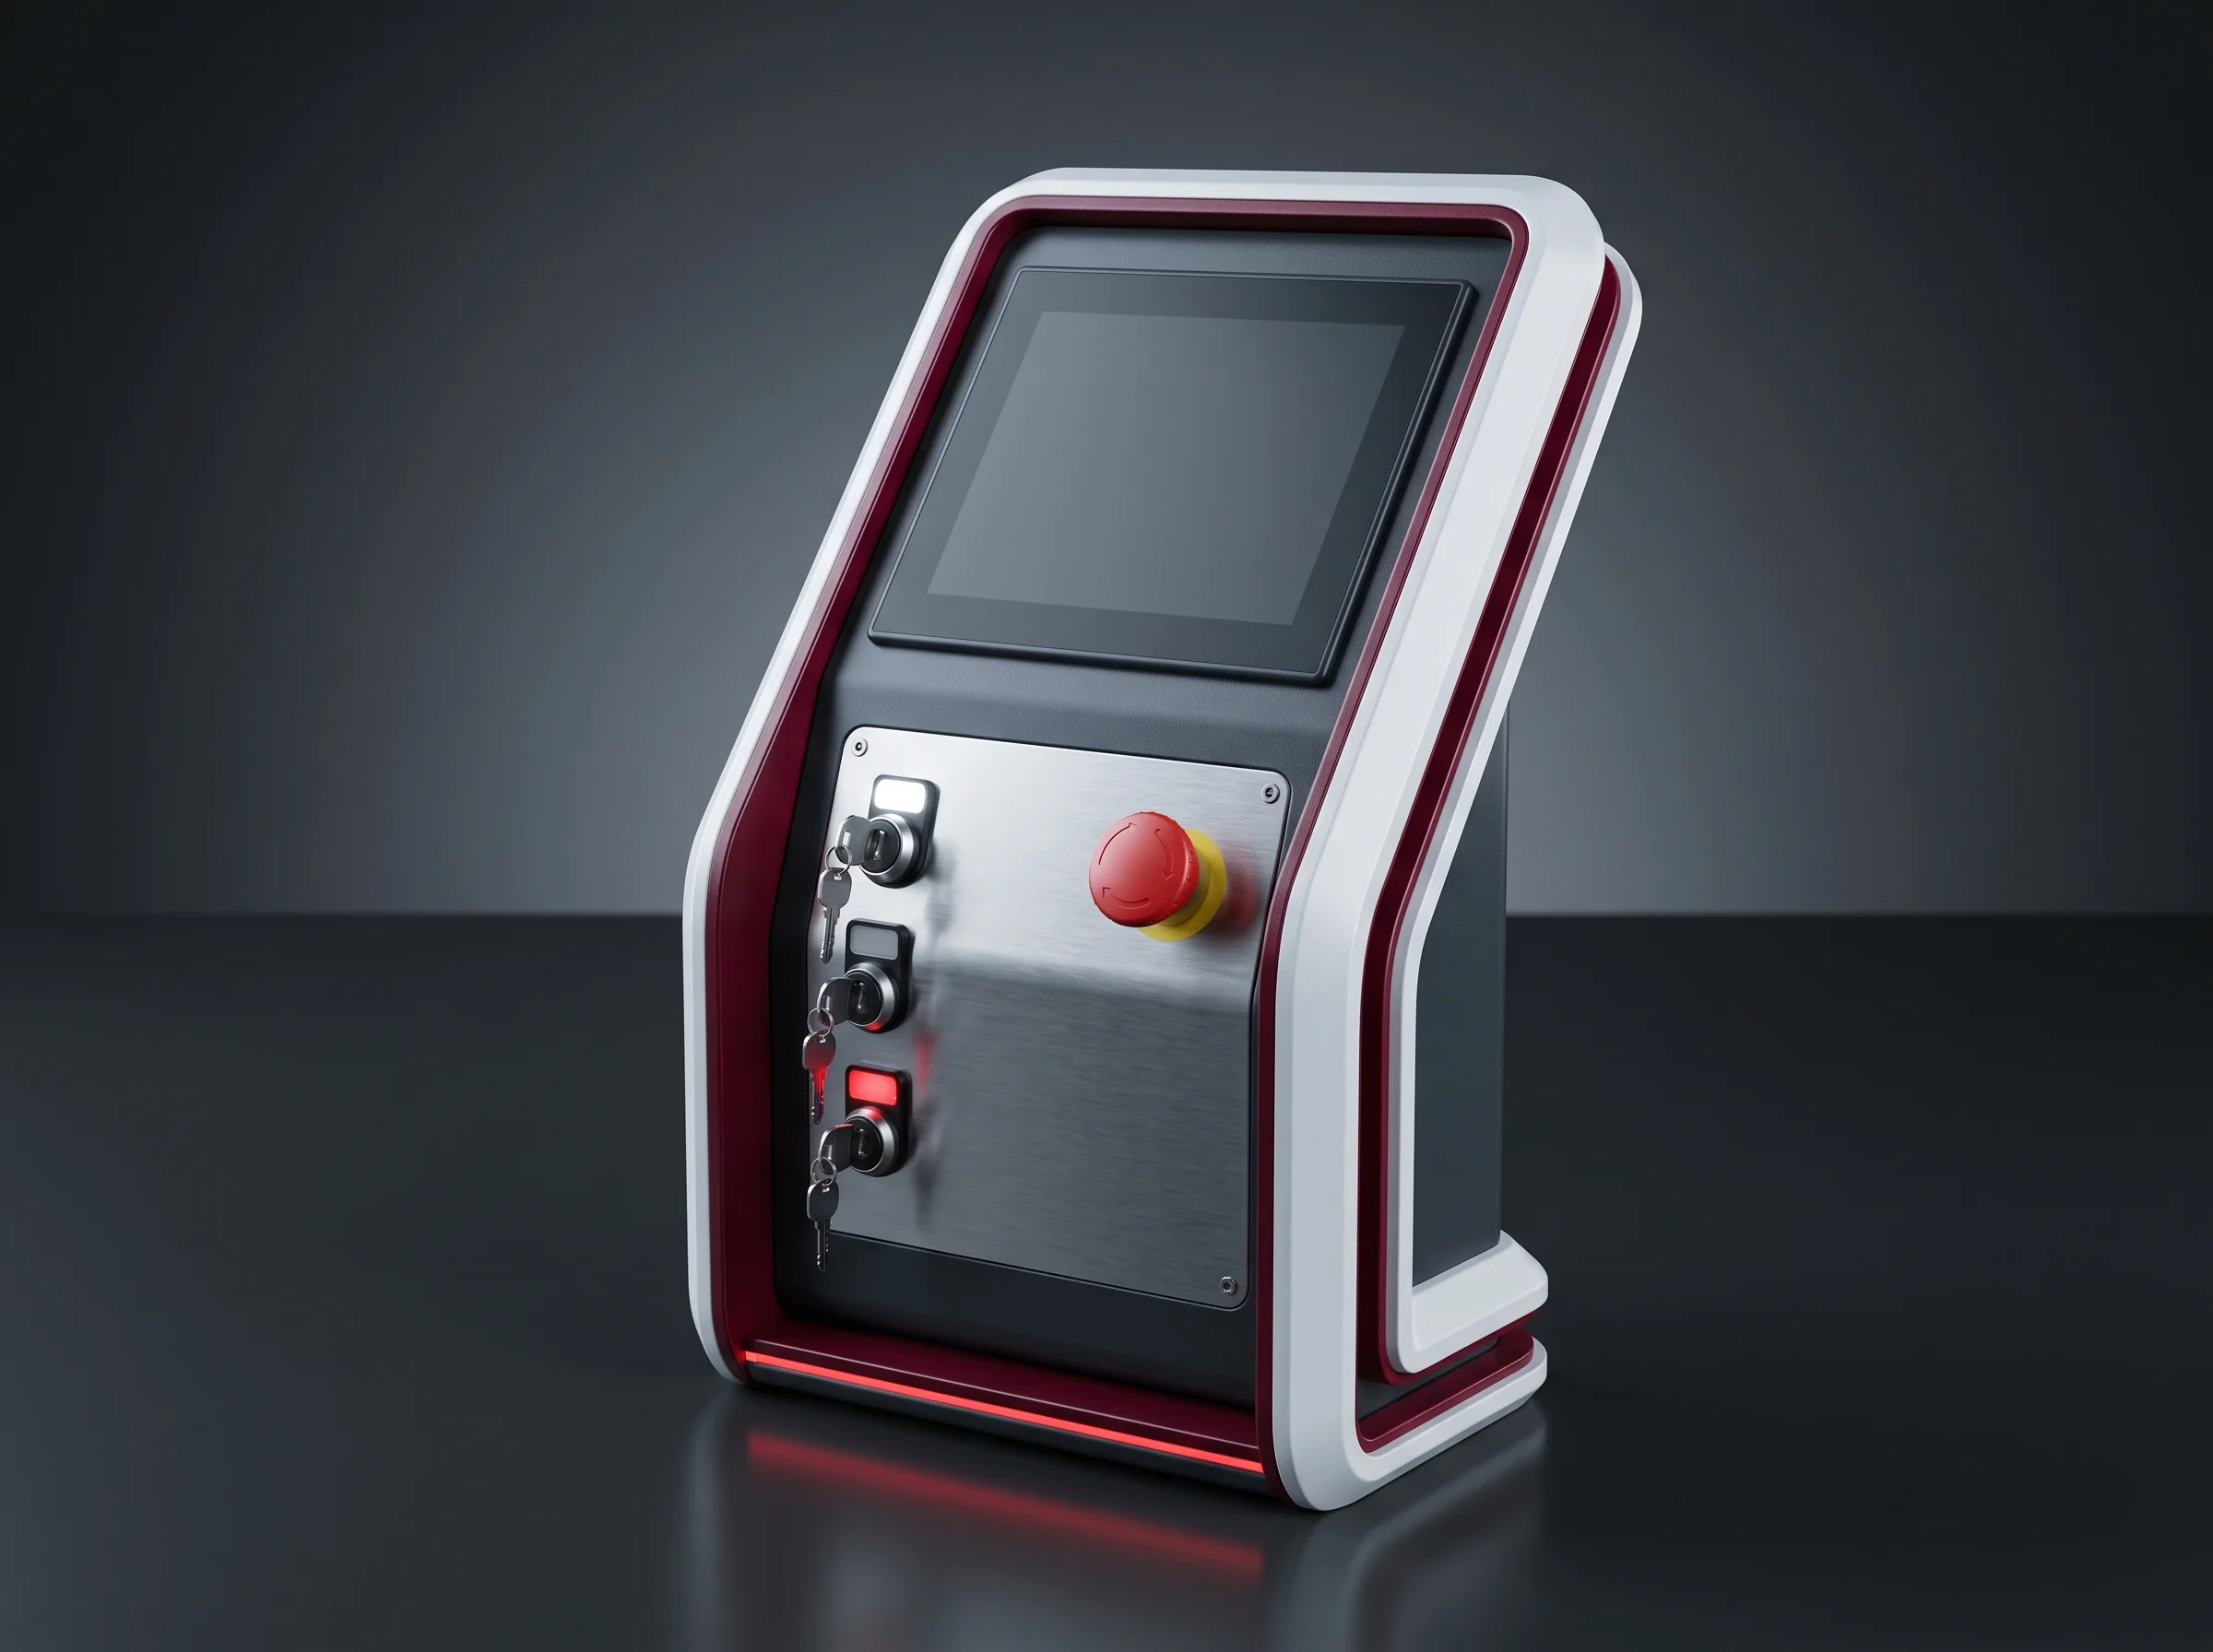
Selects and releases
Writes and edits
Signs it live
The four values a recipe holds
Traceable to the edit
Every change is kept with the item, the account and the time. A shift in module length three weeks after an edit is walked back to that edit rather than argued about.
- Operators are trained on selection, on the release, and on what to do with a held module.
- Process engineers on writing a recipe, reading curve shape, and qualifying a first article.
- Training is split the same way the accounts are, so the split survives the handover.
Semi-automatic, stated
Stacking, Pressing And Banding
Three things happen across stations 08 and 09, automated to different degrees. The pair is specified as semi-automatic because one of them needs a pair of hands every cycle.
Stacking
Pressing
Steel banding
Why it is published this way
Called fully automatic, you budget no labour for a position needing hands every cycle, and the shortfall turns up on your floor.
Called manual, you train for machine work the operator never touches, while band consistency — the skill that matters here — gets none.
- Upstream of the pressEnd plates and insulation sheets come from the station ahead; the press works on the stack as it arrives.
- Downstream of the bandsPolarity and insulation testing runs on a banded module. Here the press creates the dimension; the bands preserve it.
What fits, and what changes
Pressing Span And Module Length
Read a module against the span and you learn about this station; read it against the envelope and you learn about the line.
- 300–1100 mm — pressing span, this stationThis press
- 400–1200 mm long × 100–300 wide × 100–250 high — module envelopeThe line
- 978.4 × 178.9 × 205 mm, 1P13S blueprint moduleClears both
- 900 ± 50 mm transfer height, adjustable to your lineSet on site
Your module types are checked against both ranges at drawing stage, and you get a written finding: which run on one set of tooling, and which need their own.
A new module length is hardware plus one recipe
Press platens, the locating fixture and the banding stops are tooling cut for a module family. The recipe is written for the new type and qualified on a first article before it runs in volume.
Tooling is quoted per item, and the changeover picture across every station is on the cell compatibility and changeover page.
One station, on its own
A Stand-Alone Module Stacking Station
The interface figures exist so the press drops into a line we built, or a line somebody else built.
- 8 kWRated power
- 380 V / 50 HzSupply
- 0.5–0.7 MPaAir, ≤200 L/min
- 900 ± 50 mmTransfer height, adjustable
How a module gets in and out
Modules travel on their fixtures, handed over by BLP-CV conveyor at 200 kg or more and up to 20 m/min. Transfer height is set against the line you run, not fixed at our number.
How the record gets out
Control-side the station speaks PROFINET and pushes the force curve and post-press length to your MES by module number — into the system you already run.
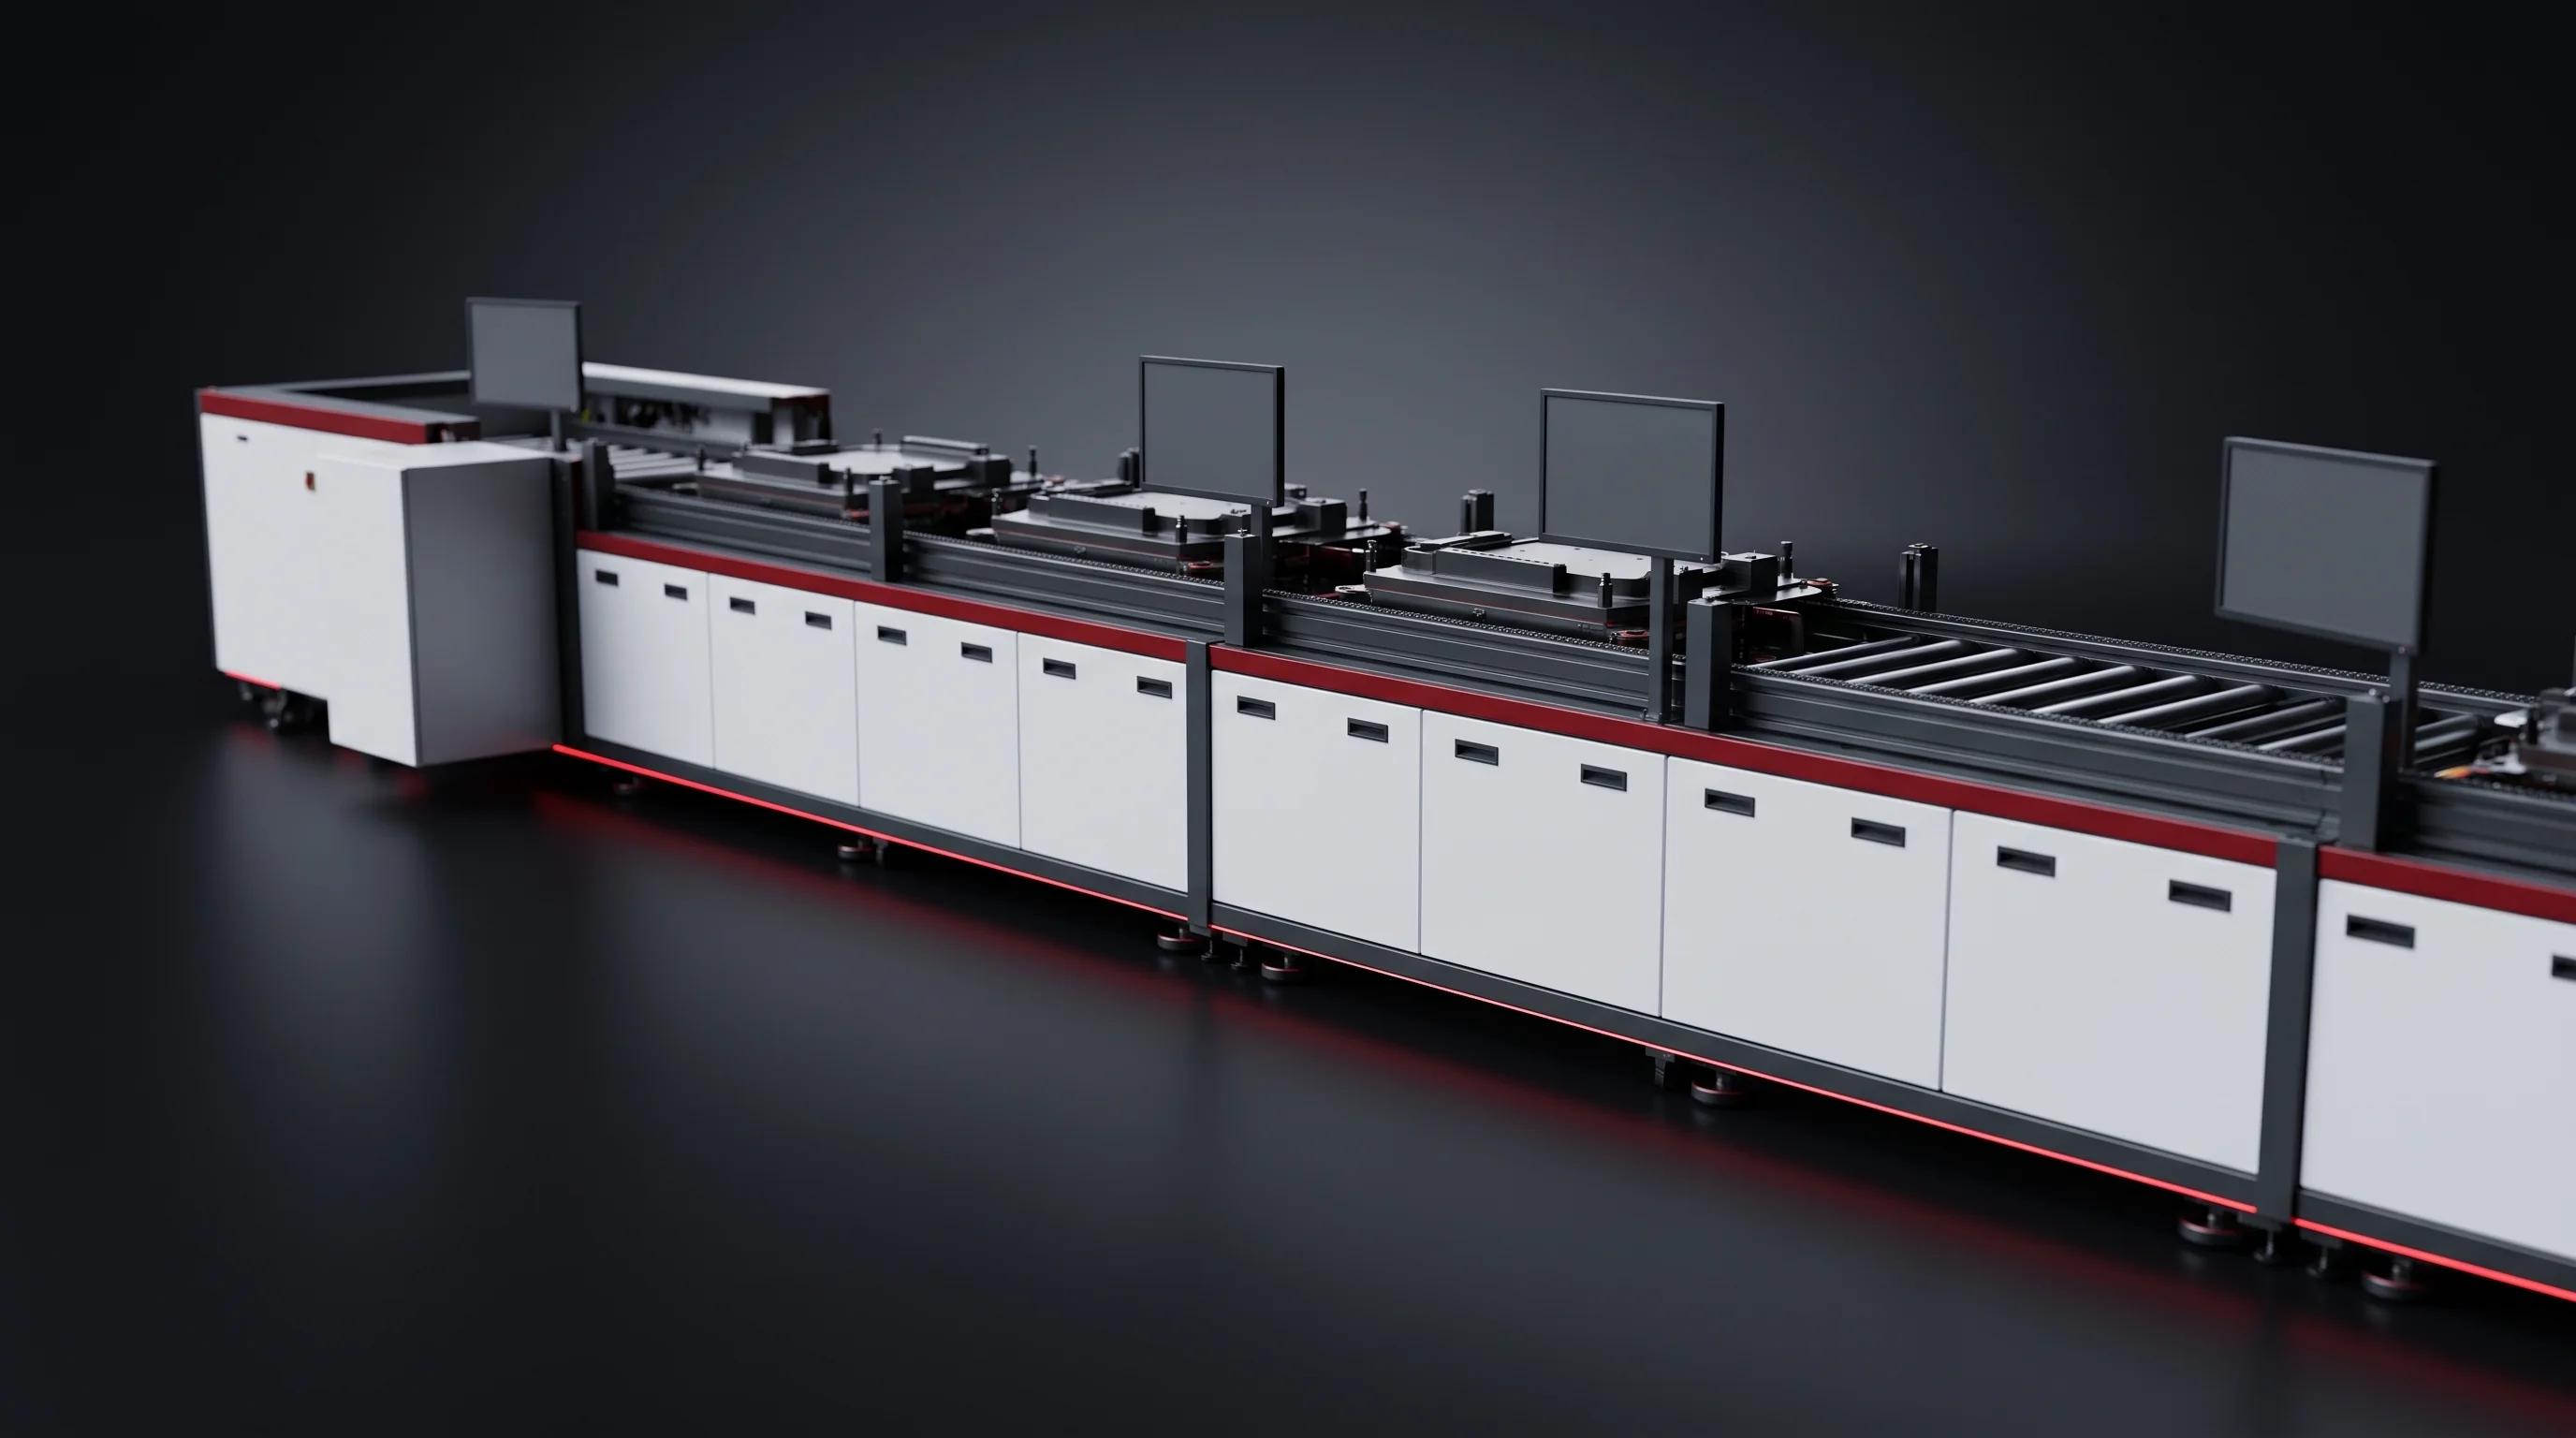
What the station needs from the line either side of it
Coming in
A stack with end plates and insulation sheets in place, on a fixture the conveyor can hand over.
Going out
A downstream position ready for a banded module, and a control system that accepts the record over PROFINET.
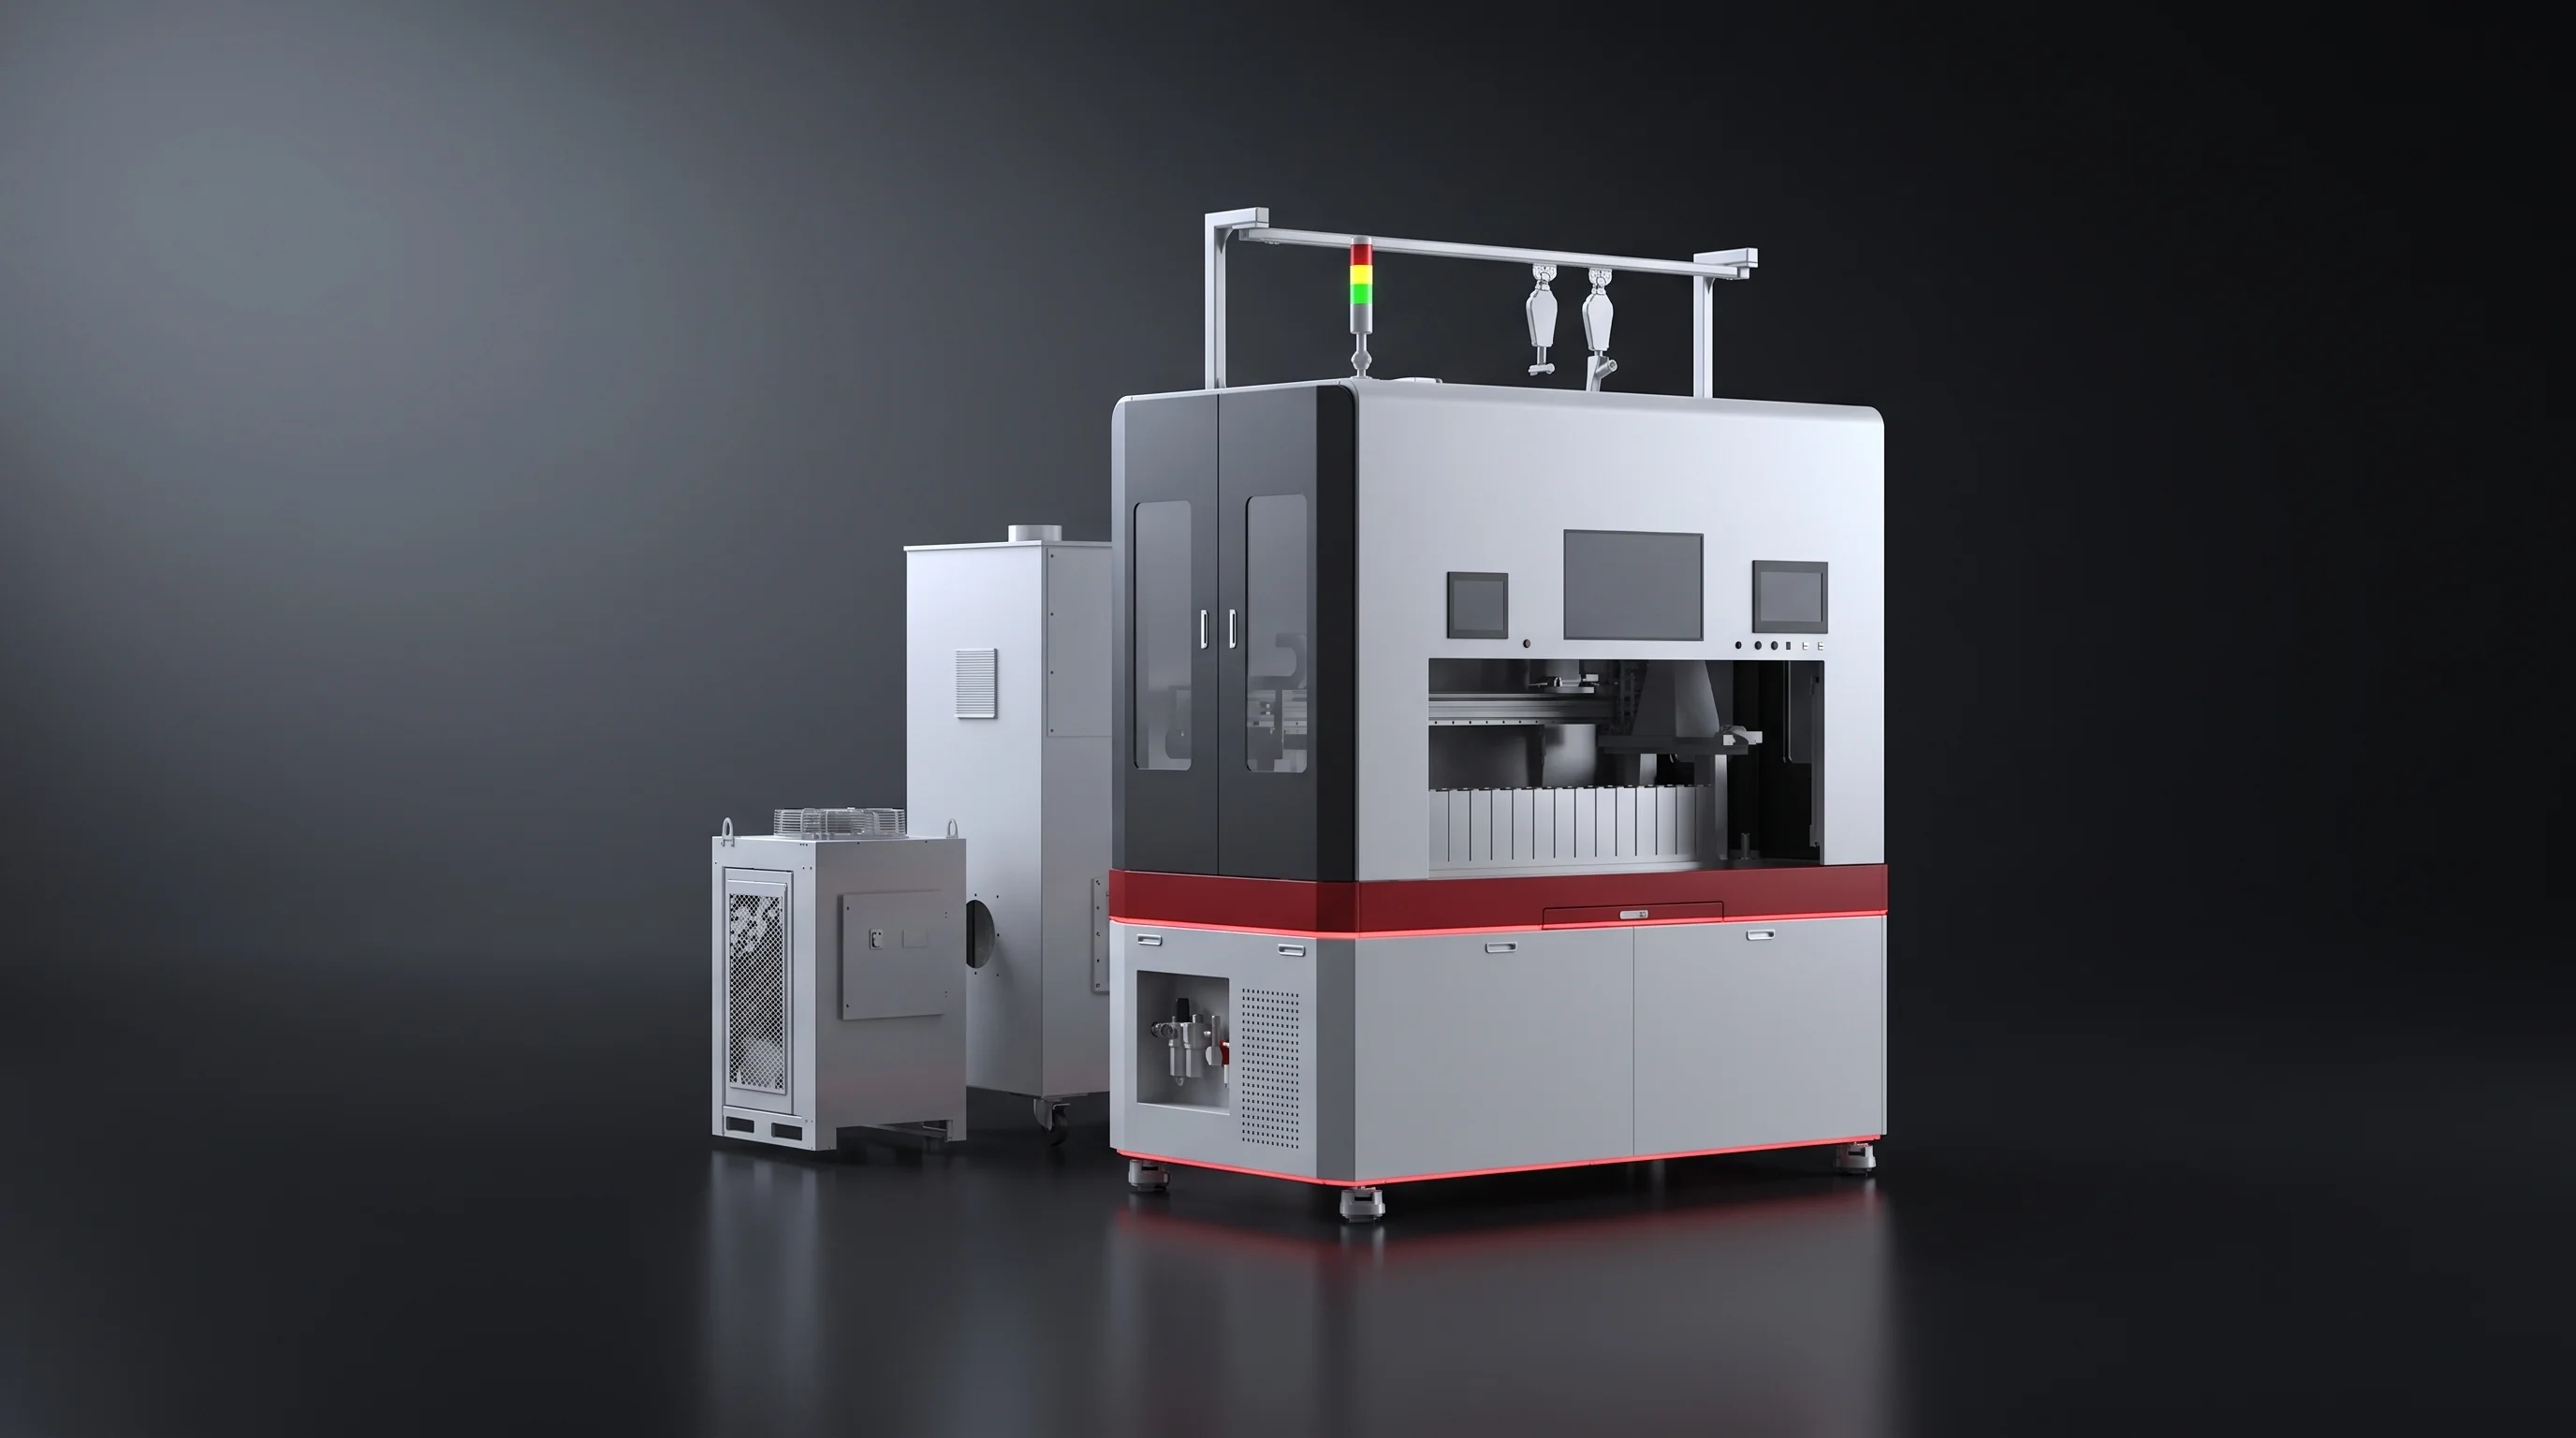
Three situations
Three Buyers Of The Module Stacking Station
Quoted the same way in all three. What differs is how much of the line around it is being decided at the same time.
Specifying a whole segment
Replacing the press in a running line
Moving a line onto a new module
The engineering group behind all three
26 engineers across mechanical, electrical and control, laser and vision process, and field installation, working out of a 6,000 m² assembly hall with three pre-assembly bays where a line is powered up before it ships.
Wear parts ship within 48 hours, remote diagnostics is available on the station, and the group holds ISO 9001, CE and RoHS. How projects run is on the about page.
- 26Engineers
- 6,000 m²Assembly hall
- 40+Line segments
- 12Countries
What a quote needs
Five Items For A Quote
Five items, and two more if the station joins a line you already run.
- The module drawingLength, width, height and end plate form.
- Cells per moduleAnywhere from 8 to 24, and the cell format they are.
- Length and toleranceThe post-press length you work to, and how tight.
- Target force and dwellIf you have them. If not, the drawing is enough.
- Takt and bandingYour takt, and whether banding is in scope here.
Joining an existing line, add two
- The transfer height you run at, so the 900 ± 50 mm is set against it.
- The control system it reports to, so curve and length land in the MES you already use.
To see it running first, send cell drawings, module and pack configuration and target takt two weeks ahead of a visit — the pre-assembly bay is set to your configuration when you arrive. Start on the contact page.
Back within 24 hours
- The target force and dwell we would store as your recipe.
- The tooling your module types need, and which share one set.
- How the station fits your handover height.
- How the record reaches your MES.
Your enquiry, ready to send
If your email client opened, it is already in the message. If nothing opened, use one of the two routes below.
Start a project
Send Your Module Drawing
Three required lines to our engineering team and the recipe we would store, the tooling your modules need and how the station meets your handover height come back within 24 hours. Behind it: 26 engineers and 40+ line segments delivered into 12 countries, on the about page.